
In my work as a casting engineer, I have often encountered challenges in producing high-quality gear shaft components, which are critical in various mechanical systems such as transmissions, industrial machinery, and automotive applications. The gear shaft, due to its complex geometry and high-strength requirements, demands precise casting techniques to avoid defects like shrinkage porosity and voids. This article details my experience in optimizing the casting process for a gear shaft steel casting, leveraging numerical simulation tools to enhance design and eliminate imperfections. Through this first-person account, I aim to share insights into the methodology, analysis, and improvements that led to a successful outcome.
The gear shaft in focus is typically made from high-strength steel grades, such as ZG42CrMo, which offers excellent toughness, fatigue resistance, and low-temperature impact properties. These attributes make it ideal for heavy-duty applications, but they also introduce difficulties during casting, as the material’s solidification behavior can lead to internal defects if not properly managed. In my project, the initial casting scheme, derived from traditional methods, resulted in significant shrinkage issues, prompting a thorough investigation and redesign. My goal was to use simulation software to visualize the process, identify root causes, and implement corrective measures, ultimately achieving a defect-free gear shaft production.
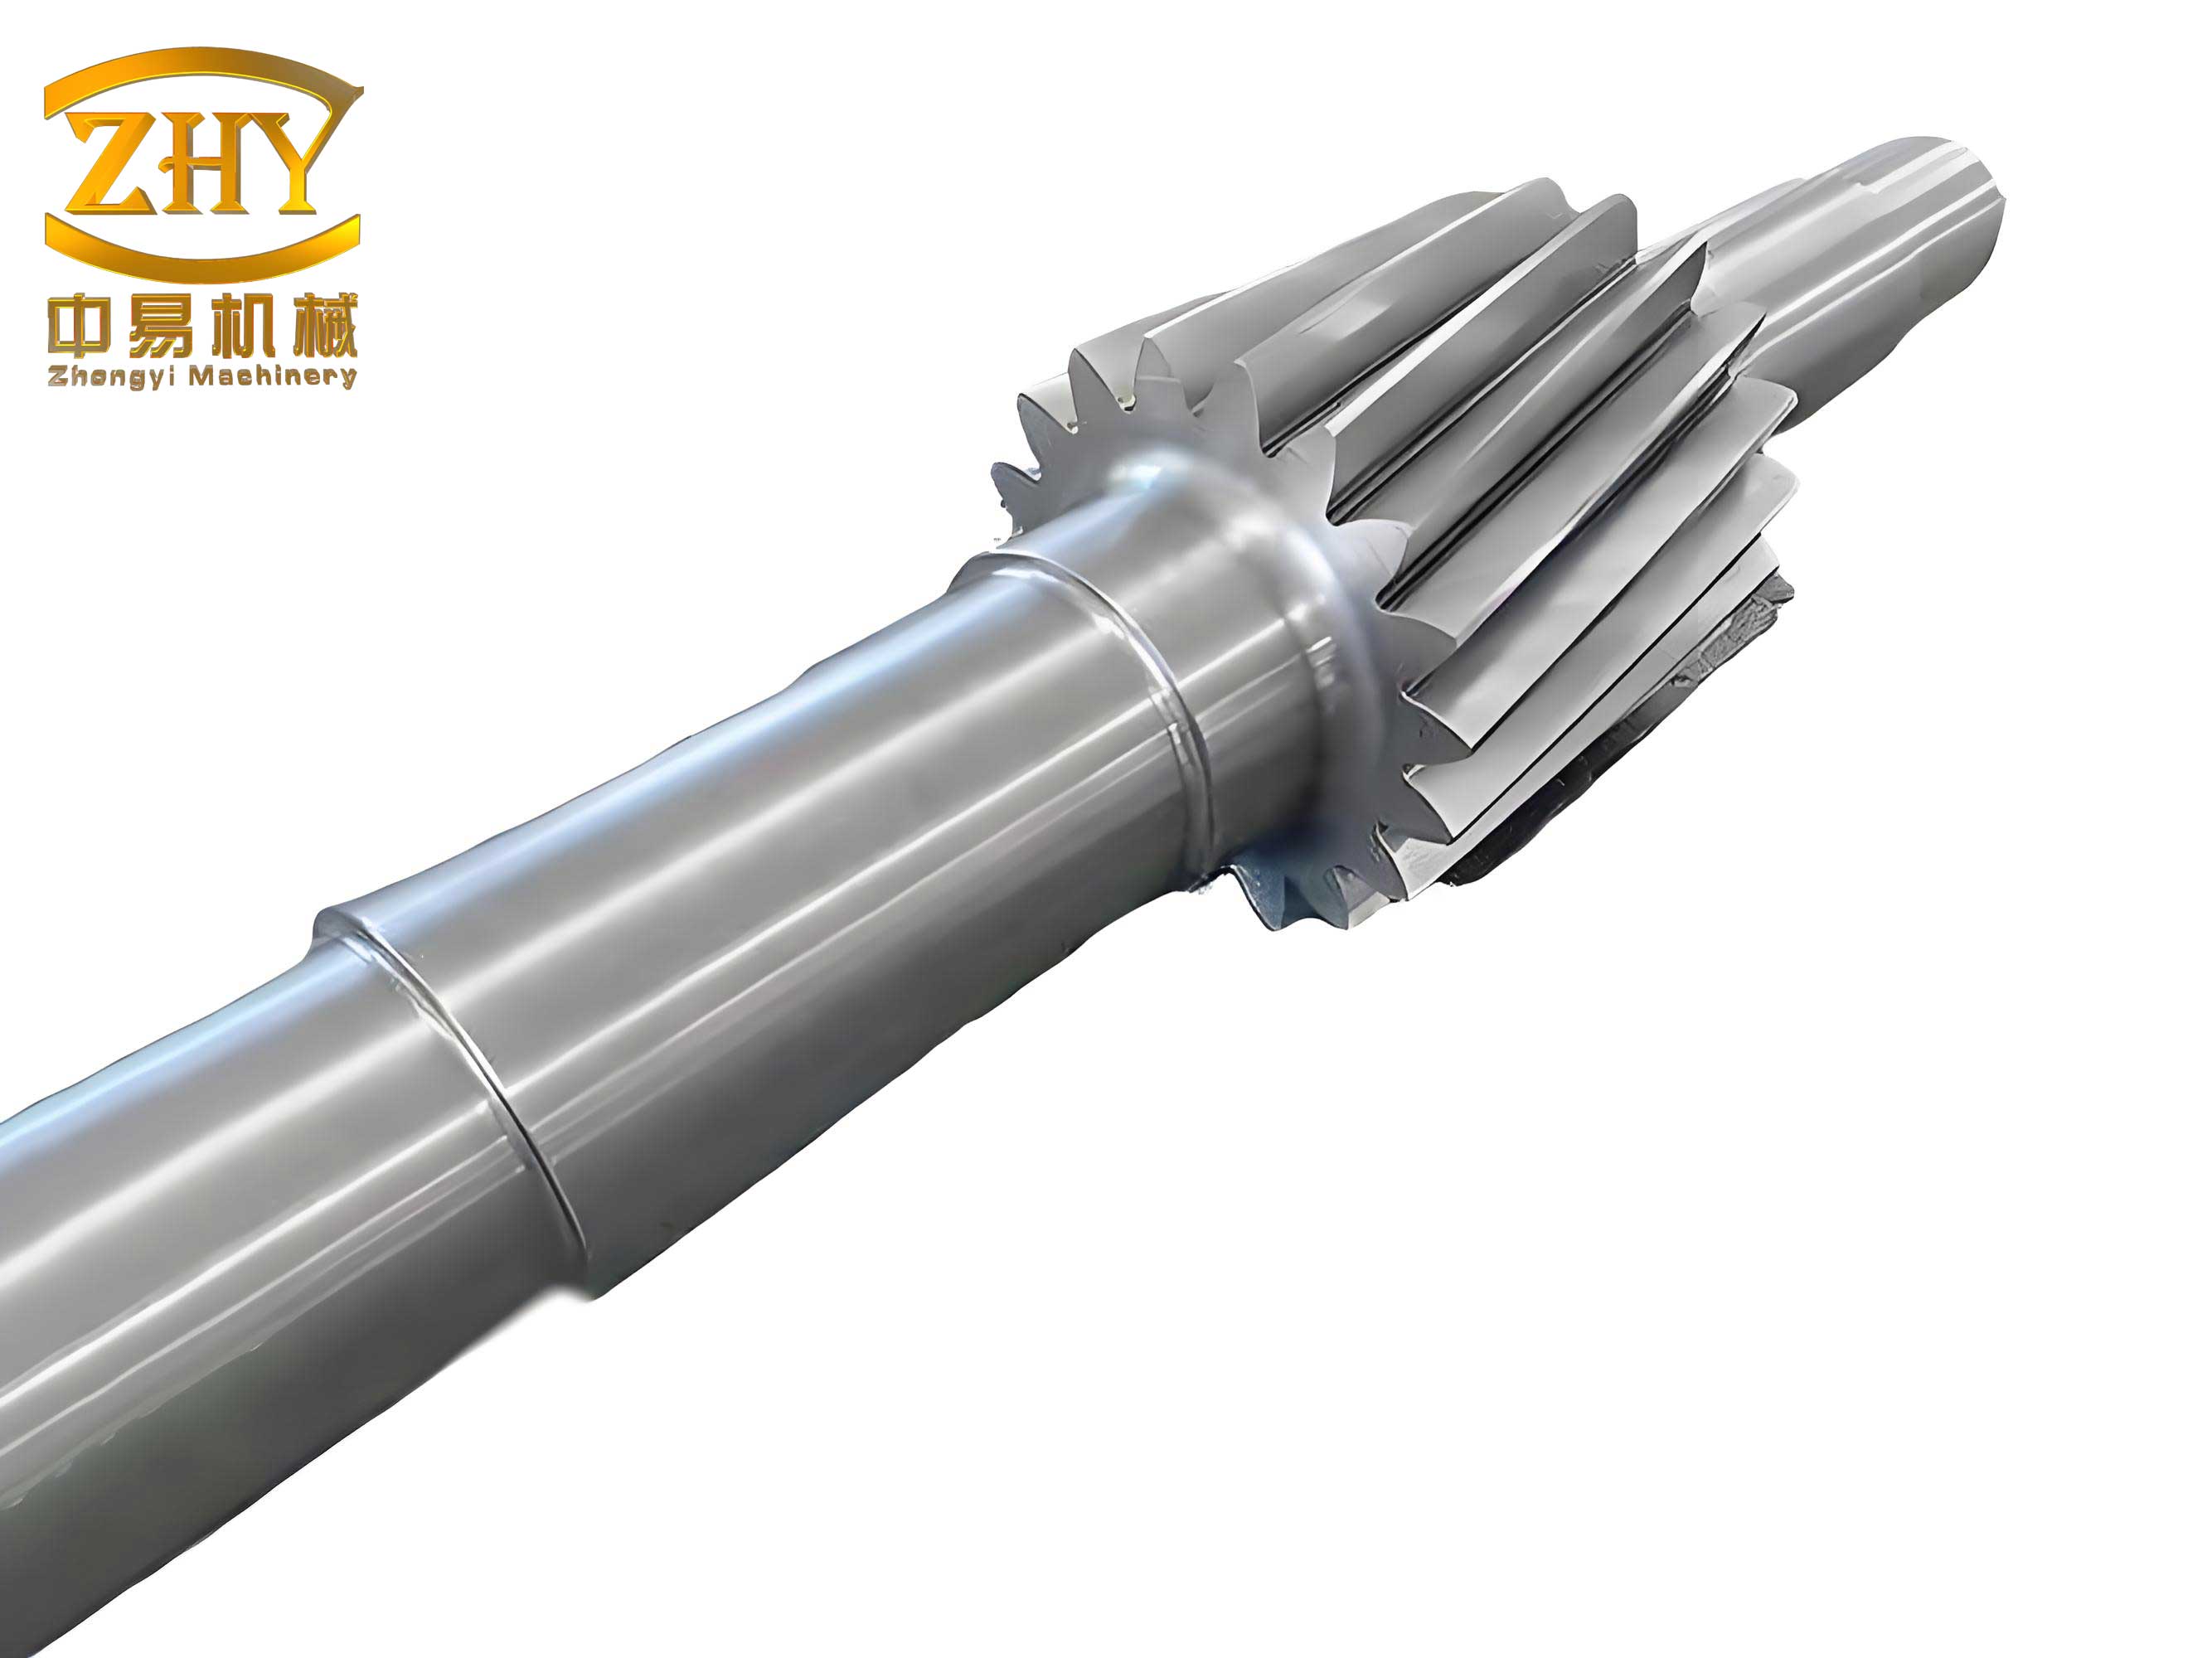
To begin, I will outline the original casting scheme for the gear shaft. The design involved a medium-pour closed gating system, with four gear shaft castings arranged in a single mold. The parting line was set at the midpoint of the gear shaft, and small features like holes and slots were omitted due to their dimensions. The gating system comprised one sprue, one runner, and four ingates, with cross-sectional area ratios defined as: $F_{\text{sprue}} : F_{\text{runner}} : F_{\text{ingate}} = (1.1 \text{ to } 1.2) : (0.8 \text{ to } 0.9) : 1$. Based on calculations, the areas were determined as $F_{\text{ingate}} = 3.95 \, \text{cm}^2$, $F_{\text{runner}} = 3.19 \, \text{cm}^2$, and $F_{\text{sprue}} = 4.35 \, \text{cm}^2$, leading to specific dimensions for each component. A waist-shaped riser was employed, with dimensions of 43 mm × 86 mm × 63 mm, providing a maximum feeding capacity of 3.0 kg. However, this initial setup proved inadequate, as defects persisted even after iterative adjustments in the foundry.
I have summarized the key parameters of the original gear shaft casting scheme in the table below, which highlights the design elements and their specifications:
| Component | Dimension/Value | Description |
|---|---|---|
| Gear Shaft Material | ZG42CrMo | High-strength steel with good hardenability |
| Gating System Ratio | $F_{\text{sprue}}:F_{\text{runner}}:F_{\text{ingate}} = 1.15:0.85:1$ | Area ratio for flow control |
| Ingate Area | $3.95 \, \text{cm}^2$ | Calculated from design ratios |
| Runner Dimensions | 20 mm × 15 mm × 20 mm | Rectangular cross-section |
| Sprue Radius | 31 mm | Cylindrical shape |
| Riser Type | Waist-shaped | 43 mm × 86 mm × 63 mm |
| Feeding Capacity | 3.0 kg | Maximum补缩量 |
| Pouring Temperature | 1540°C | Typical for steel casting |
| Mold Material | Resin Sand | Commonly used in foundries |
In my analysis, the solidification process is governed by thermal dynamics, which can be described using Fourier’s law of heat conduction. For the gear shaft casting, the heat transfer equation during solidification is expressed as: $$\frac{\partial T}{\partial t} = \alpha \nabla^2 T + \frac{L}{c_p} \frac{\partial f_s}{\partial t}$$ where $T$ is temperature, $t$ is time, $\alpha$ is thermal diffusivity, $L$ is latent heat, $c_p$ is specific heat, and $f_s$ is solid fraction. This equation helps in understanding how temperature gradients evolve, influencing defect formation in the gear shaft.
To diagnose the issues with the original gear shaft casting scheme, I employed ViewCast simulation software, integrating a 3D model created in Pro/E. The mesh was divided into approximately 1 million elements, with parameters set to mimic real-world conditions: pouring temperature at 1540°C, mold temperature at 23°C, and resin sand as the molding material. The simulation revealed the solidification sequence over time, highlighting critical stages where defects emerged. For instance, at $t = 50 \, \text{s}$, a positive temperature gradient existed near the riser, but as solidification progressed, the riser solidified prematurely by $t = 310 \, \text{s}$, leaving isolated liquid pockets in the gear shaft center. By $t = 570 \, \text{s}$, these pockets solidified last, causing shrinkage porosity and voids. The total solidification time was recorded as 606 s, which I found insufficient for proper feeding of the gear shaft.
The defect analysis indicated that the riser’s limited size and lack of insulation led to early solidification, cutting off the补缩通道. To quantify this, I calculated the feeding efficiency $\eta$ of the riser using: $$\eta = \frac{V_{\text{feeding}}}{V_{\text{riser}}} \times 100\%$$ where $V_{\text{feeding}}$ is the volume of metal fed to the gear shaft and $V_{\text{riser}}$ is the riser volume. In the original scheme, $\eta$ was low due to premature freezing, resulting in defects. The simulation output showed defect concentrations extending from the riser top into the gear shaft core, confirming the need for redesign.
Based on these findings, I proposed an optimized scheme for the gear shaft casting. The primary modifications included increasing the riser height by 20 mm to 83 mm and adding an insulation sleeve with a thickness of 13 mm. This aimed to prolong the riser’s liquid state, maintain a positive temperature gradient, and enhance feeding until the gear shaft fully solidified. The insulation material’s thermal properties were selected to reduce heat loss, effectively increasing the thermal modulus $M$ of the riser, defined as: $$M = \frac{V}{A}$$ where $V$ is volume and $A$ is surface area. A higher $M$ value improves feeding capacity, crucial for the gear shaft’s integrity.
I have compiled the optimized parameters in the following table, comparing them to the original gear shaft casting scheme:
| Parameter | Original Scheme | Optimized Scheme |
|---|---|---|
| Riser Height | 63 mm | 83 mm |
| Riser Type | Waist-shaped, uninsulated | Waist-shaped with insulation sleeve |
| Insulation Thickness | 0 mm | 13 mm |
| Calculated Feeding Efficiency $\eta$ | ~40% (estimated) | ~75% (estimated) |
| Solidification Time | 606 s | 949 s |
| Defect Presence in Gear Shaft | Significant shrinkage | None, defects moved to riser |
| Temperature Gradient at $t=300\, \text{s}$ | Negative in center | Positive throughout |
To validate the optimized gear shaft casting process, I re-ran the simulation with the updated 3D model. The results showed a marked improvement: the solidification time increased to 949 s, allowing for more gradual cooling. At $t = 10 \, \text{s}$, the insulation maintained higher temperatures in the riser, establishing a steady thermal gradient. By $t = 330 \, \text{s}$, the gear shaft ends solidified, but the riser remained liquid, continuing to feed the central regions. At $t = 630 \, \text{s}$, sequential solidification from bottom to top was evident, and by $t = 910 \, \text{s}$, the gear shaft was fully sound, with all defects relocated to the riser. The feeding efficiency improved substantially, as derived from the formula: $$\eta_{\text{optimized}} = \frac{\rho \cdot (V_{\text{riser}} – V_{\text{defect}})}{V_{\text{riser}}} \times 100\%$$ where $\rho$ is density, and $V_{\text{defect}}$ is negligible in the optimized gear shaft.
Furthermore, I analyzed the heat flux $q$ across the gear shaft during solidification, given by: $$q = -k \frac{dT}{dx}$$ where $k$ is thermal conductivity and $\frac{dT}{dx}$ is the temperature gradient. In the optimized scheme, the insulation reduced $q$ from the riser, preserving heat and extending feeding. This aligns with Chvorinov’s rule for solidification time $t_s$: $$t_s = C \left( \frac{V}{A} \right)^2$$ where $C$ is a constant dependent on mold material. By increasing the riser’s $V/A$ ratio via height and insulation, $t_s$ for the riser increased, ensuring it outlasted the gear shaft solidification.
In practical terms, the optimized gear shaft casting process offered several benefits. It reduced scrap rates, improved mechanical properties, and minimized post-casting repairs. The use of simulation allowed me to iterate designs virtually, saving time and resources compared to physical trial-and-error. For instance, I could adjust parameters like pouring temperature or gating dimensions dynamically. To illustrate, I derived an empirical formula for optimal riser height $H_{\text{opt}}$ based on gear shaft geometry: $$H_{\text{opt}} = H_{\text{original}} + \Delta H \cdot \left(1 – e^{-\frac{t_{\text{solid}}}{\tau}}\right)$$ where $\Delta H$ is the height increment, $t_{\text{solid}}$ is solidification time, and $\tau$ is a time constant from simulation data. This helped fine-tune the design for similar gear shaft projects.
Throughout this work, the gear shaft served as a focal point for applying advanced casting principles. By integrating simulation into the workflow, I achieved a robust process that can be adapted to other components. The key takeaway is that a systematic approach—combining traditional knowledge with modern tools—can resolve complex casting challenges. In conclusion, the optimized gear shaft casting scheme eliminated defects, enhanced productivity, and set a precedent for future innovations in foundry practices. My experience underscores the value of numerical simulation in achieving high-quality gear shaft productions, paving the way for more reliable and efficient manufacturing processes.