
The structural integrity and longevity of gear shafts are paramount in the reliable operation of heavy-duty machinery, such as shearers used in mining. In engineering practice, a significant proportion of component failures, ranging from 50% to 90%, can be attributed to material fatigue. For involute cylindrical gears, a common form of this failure is fatigue pitting, which predominantly initiates near the pitch line on the dedendum side of the tooth flank. While traditional design criteria often focus on static strength and stiffness verification, components frequently experience fatigue failure well before reaching their theoretical calculated life, even when meeting static requirements. This underscores the critical need for a comprehensive fatigue life assessment that accounts for realistic operating conditions.
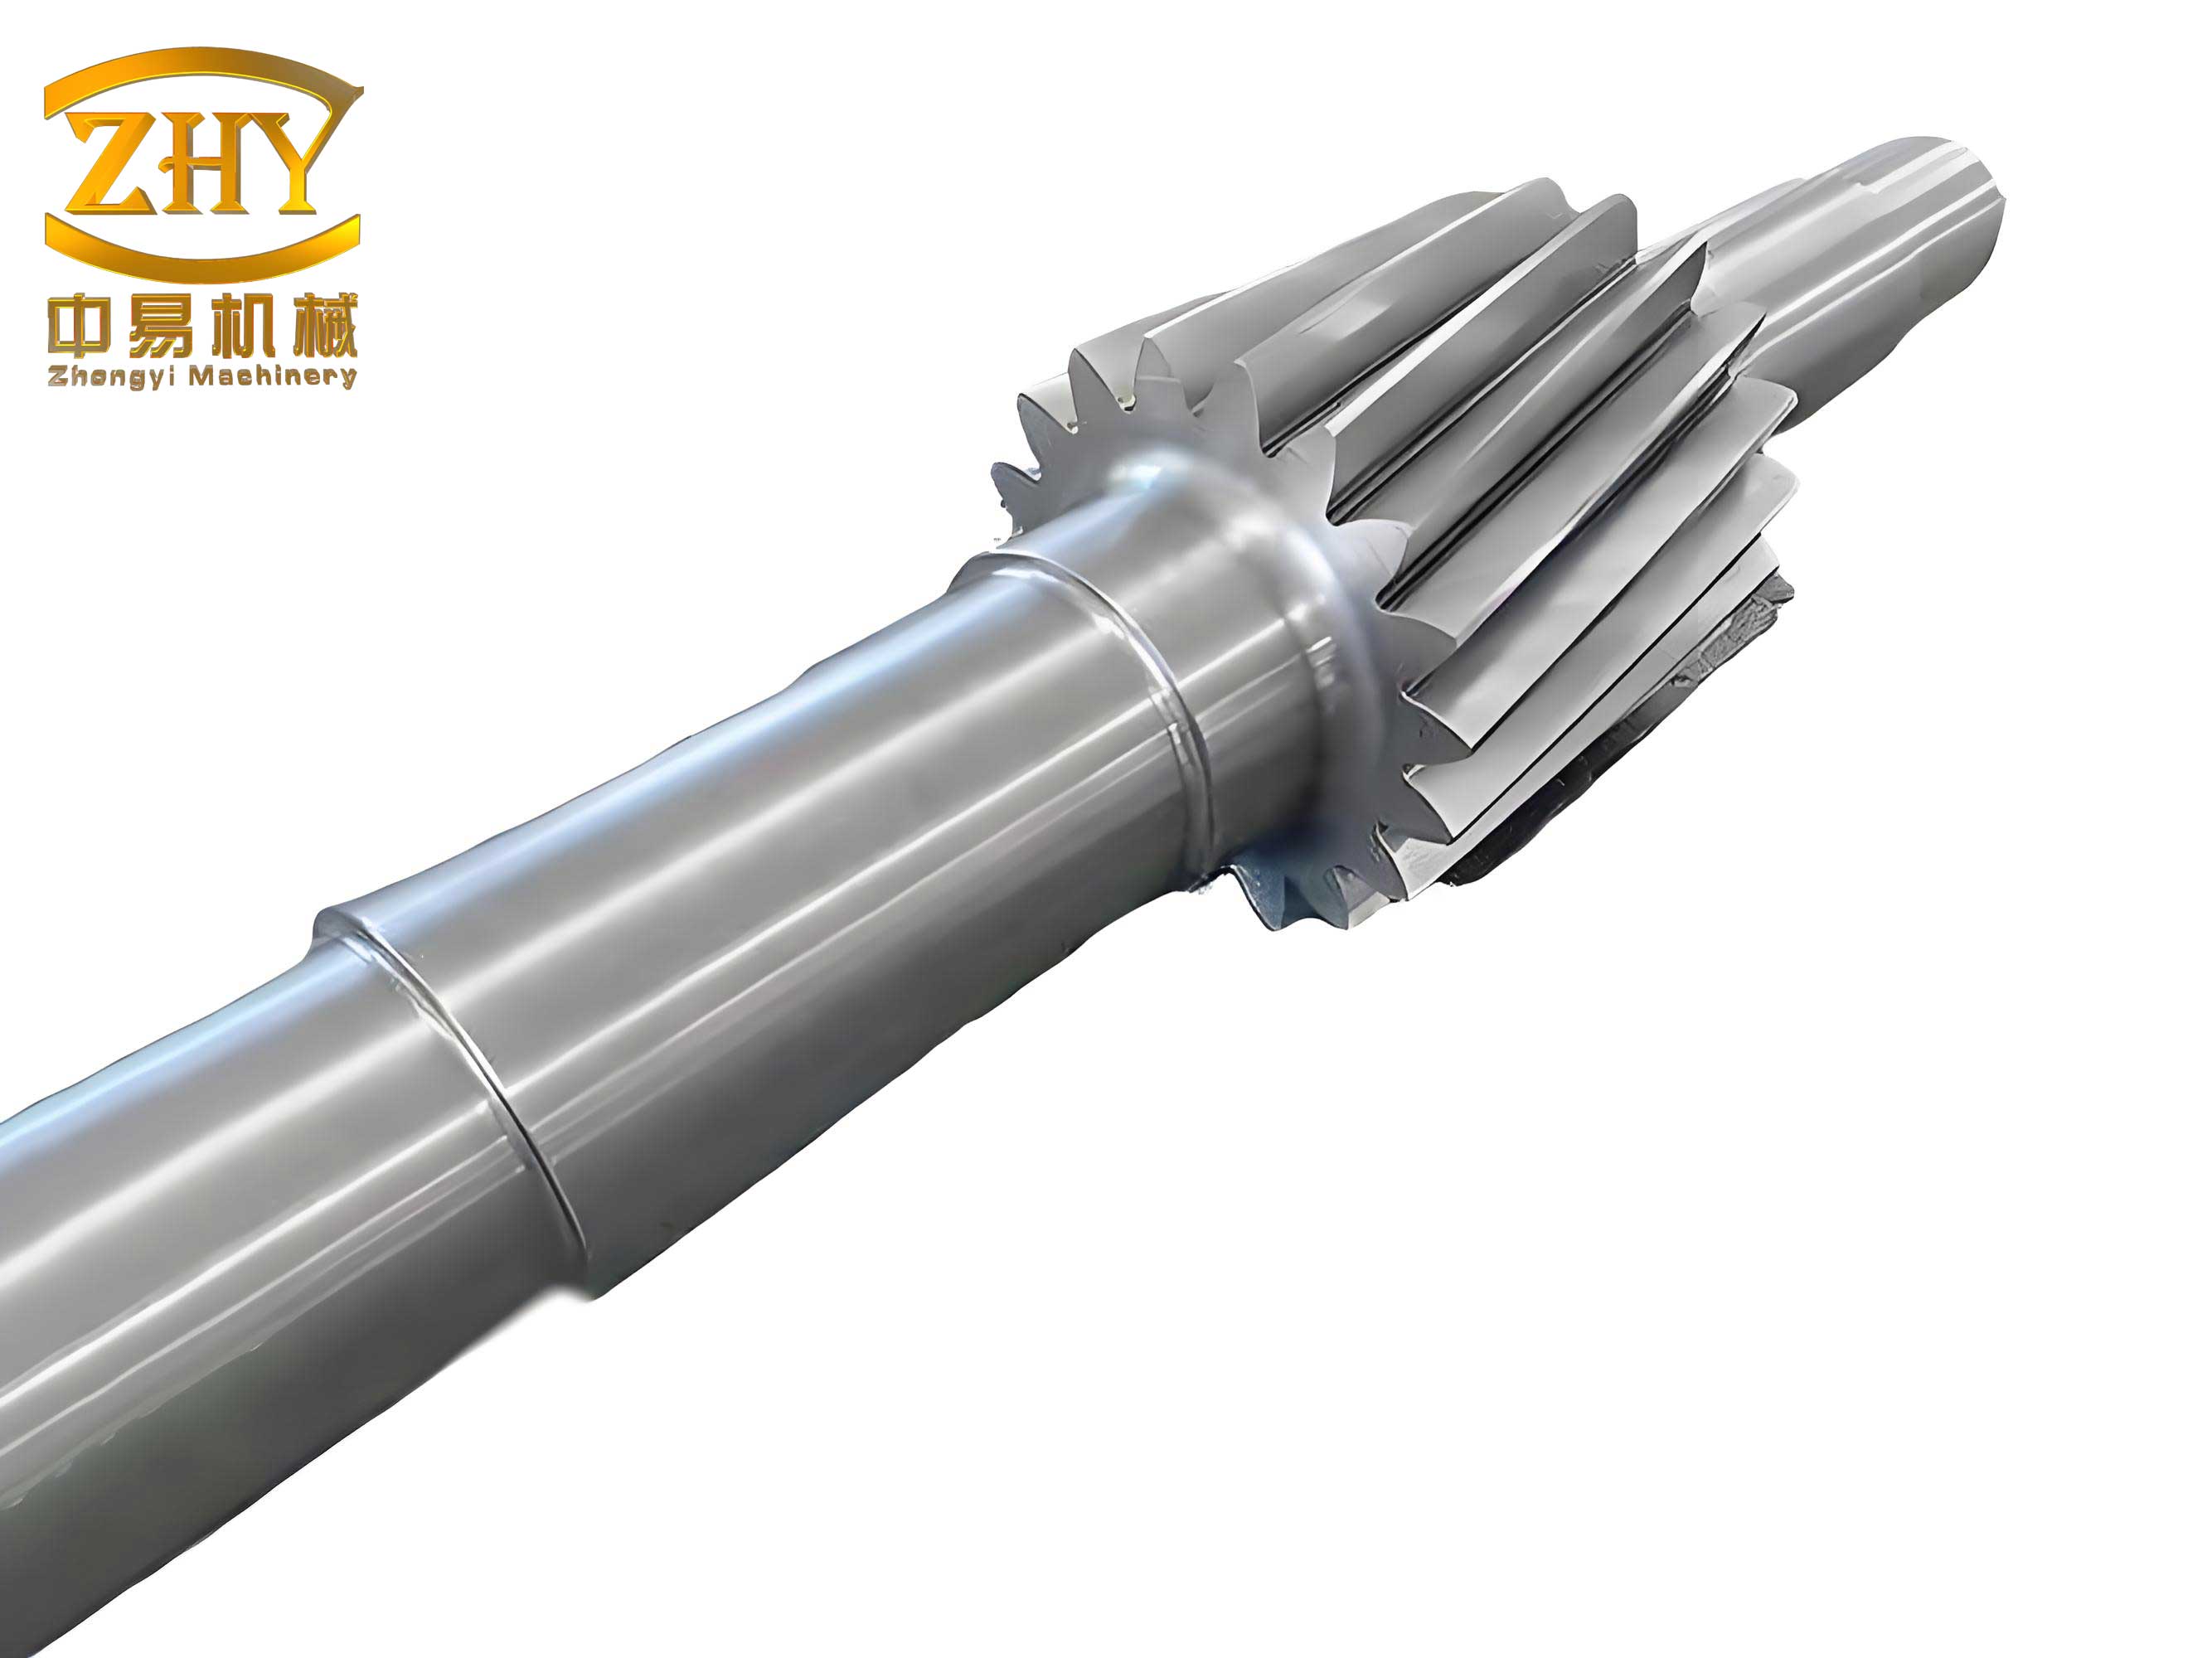
This article presents a rigorous methodology for the contact fatigue analysis of power transmission gear shafts. The approach integrates multi-body dynamics simulation to extract realistic load spectra with advanced finite element analysis (FEA) for detailed stress calculation and subsequent fatigue life prediction. The workflow employs a suite of engineering software: Pro/Engineer for parametric solid modeling, MATLAB for data processing and S-N curve generation, ADAMS for multi-body dynamic simulation under operational conditions, and ANSYS for nonlinear contact finite element analysis and fatigue life calculation. This integrated simulation framework ensures that the fatigue assessment of the gear shafts is based on accurate dynamic loads rather than simplified static assumptions.
Methodology for Integrated Analysis
1. Geometric Modeling and Simplification
The foundation of any accurate FEA is a precise geometric model. The three-dimensional model of the gear shafts and their mating gear is created parametrically in Pro/Engineer based on key design parameters: number of teeth \(z\), module \(m\), pressure angle \(\alpha\), addendum coefficient \(h_a^*\), dedendum coefficient \(h_f^*\), profile shift coefficient \(x\), face width \(w\), and center distance \(a\).
Contact analysis is a highly nonlinear problem requiring substantial computational resources. To achieve computational efficiency without compromising the accuracy of the stress field in the critical contact regions, a simplified model is adopted. According to Saint-Venant’s principle, the effects of localized loads diminish with distance. Therefore, a quarter-symmetry model of the gear pair is extracted for analysis. This simplification significantly reduces the number of elements while preserving the essential mechanics of the gear mesh interaction for the gear shafts.
2. Finite Element Model Development
The simplified Pro/Engineer model is seamlessly imported into ANSYS via a dedicated interface to prevent geometry translation errors. The finite element model is then developed with careful attention to element selection, meshing, and contact definition.
Element Properties and Material Definition: The gear shafts and the gear are meshed with SOLID185 elements, an 8-node brick element suitable for plasticity, creep, large deflection, and large strain capabilities. The material properties for the alloy steel used for the gear shafts are defined as follows:
| Material Property | Symbol | Value | Unit |
|---|---|---|---|
| Elastic Modulus | \(E\) | 210,000 | MPa |
| Poisson’s Ratio | \(\nu\) | 0.3 | – |
| Density | \(\rho\) | 7,850 | kg/m³ |
| Yield Strength | \(\sigma_y\) | 835 | MPa |
| Ultimate Tensile Strength | \(\sigma_u\) | 1,175 | MPa |
For the surface-to-surface contact between the teeth of the gear shafts and the mating gear, CONTA174 and TARGE170 elements are used to define the contact pair. A Coulomb friction model with a coefficient of \(\mu = 0.1\) is applied at the contacting interfaces.
Meshing Strategy: A balance between computational accuracy and cost is achieved through a graded mesh. Regions of high stress gradients, such as the fillet area at the root of the teeth on the gear shafts and the potential contact zones on the tooth flanks, are discretized with a finer mesh. Areas with lower stress variation are meshed more coarsely. The parameters for the meshing are summarized below:
| Region | Element Type | Approx. Size | Notes |
|---|---|---|---|
| Tooth Contact Zone | SOLID185 | 0.5 mm | Fine mesh for accuracy |
| Tooth Root & Fillet | SOLID185 | 0.8 mm | Fine mesh for stress concentration |
| Hub & Shaft Body | SOLID185 | 3.0 mm | Coarse mesh for efficiency |
| Contact Surfaces | CONTA174/TARGE170 | 0.6 mm | Matched with target surface |
Contact Pair Generation: The analysis anticipates two pairs of teeth to be in contact simultaneously due to the contact ratio. The contact pairs are efficiently generated using ANSYS’s contact wizard, which automatically identifies potential contact zones based on proximity and surface normals.
3. Load and Boundary Condition Definition
Accurately representing the operational loading is crucial. The driving torque for the gear shafts is not an assumed constant value but is extracted from a dynamic simulation of the complete shearer cutting drum drive train, modeled in ADAMS. The transmission chain includes the electric motor, several intermediate gear shafts, and the final output shaft. For a severe operating condition (cutting tough coal with a firmness coefficient of 3.11 at a haulage speed of 8 m/min), the dynamic simulation provides the time-history of the normal force \(f_n(t)\) on the tooth flank of the driving gear shafts.
The peak normal force from this history is identified as \(f_n^{max} = 1,085,100\,N\). This force is converted into the corresponding driving torque \(T\) for the static analysis snapshot:
$$ f_t = f_n^{max} \cdot \cos(\alpha) $$
$$ T = \frac{f_t \cdot d}{2} $$
where \(f_t\) is the tangential (circumferential) force, \(\alpha\) is the pressure angle, and \(d = m \cdot z\) is the reference diameter.
Applying a pure moment in a static analysis with solid elements (which lack rotational degrees of freedom) requires a specific technique. The node coordinate systems on the inner surface of the gear shafts hub are changed from Cartesian to cylindrical. In this system, the Y-direction represents the tangential (θ) direction. The total torque \(T\) is then applied as an equivalent set of tangential nodal forces \(F_Y\) on all nodes \(N\) of the hub’s inner surface with radius \(r_0\):
$$ F_Y = \frac{T}{r_0 \cdot N} $$
This creates the net rotational effect of the driving torque on the gear shafts.
Boundary conditions are applied to represent the mounting and reaction: the inner surface of the mating gear’s hub is fully constrained (all degrees of freedom fixed). For the driving gear shafts, nodes on the inner hub surface are constrained in the radial (X) and axial (Z) directions of the cylindrical coordinate system, but are free in the tangential (Y) direction where the force \(F_Y\) is applied.
4. Static Contact Analysis and Stress Results
The nonlinear contact problem is solved using the Newton-Raphson iterative algorithm. The convergence history confirms a stable and converged solution. The post-processing reveals the Von Mises stress distribution, which is used with the maximum shear stress theory (Tresca) or the distortion energy theory (Von Mises) to evaluate static strength.
The results indicate that the maximum stress concentrations occur precisely at the tooth contact regions, validating the model’s accuracy. For the specific gear shafts analyzed, which feature an integrated gear-and-spline geometry, a localized stress concentration also appears at the transition between the gear teeth and the spline. The calculated maximum Von Mises stress is \(\sigma_{vM}^{max} = 522.3\,MPa\). Comparing this to the material yield strength \(\sigma_y = 835\,MPa\) gives a static safety factor \(SF_{static}\):
$$ SF_{static} = \frac{\sigma_y}{\sigma_{vM}^{max}} = \frac{835}{522.3} \approx 1.60 $$
This confirms that the gear shafts meet the static strength requirement under the peak operational load.
5. Fatigue Life Prediction Using the Stress-Life Approach
Fatigue analysis predicts failure under cyclic loading at stresses below the ultimate tensile strength. ANSYS Fatigue Tool is employed, which is based on the Palmgren-Miner linear cumulative damage rule and the stress-life (S-N) method. The process focuses on the node identified with the highest stress (Node 841) as the critical location for crack initiation in the gear shafts.
Developing the Material S-N Curve: The fatigue endurance limit for the material at \(N=10^7\) cycles is \(\sigma_{e}=438\,MPa\). For a required survival probability of 99%, the P-S-N curve equation is expressed as:
$$ \log N_{99} = A – B \log \sigma_a $$
where \(\sigma_a\) is the stress amplitude. Using material test data, the coefficients are determined: \(A = 18.2666\) and \(B = 4.8617\). Thus:
$$ \log N_{99} = 18.2666 – 4.8617 \log \sigma_a $$
This equation is used in MATLAB to generate the complete S-N data points for input into ANSYS, as shown in the following table (excerpt):
| Stress Amplitude, \(\sigma_a\) (MPa) | Cycles to Failure, \(N_{99}\) |
|---|---|
| 992 | 5,000 |
| 618 | 50,000 |
| 334 | 1,000,000 |
| 251 | 4,000,000 |
| 212 | 9,000,000 |
| 180 | 20,000,000 |
| 149 | 50,000,000 |
Defining the Loading Spectrum: The fatigue life is highly dependent on the load history. The dynamic force \(f_n(t)\) from the ADAMS simulation, representing one full meshing cycle or a representative segment of operation, is analyzed. The stress history at Node 841 is derived via linear scaling from the static analysis result. This history is discretized into a series of constant amplitude loading blocks (load steps) for the fatigue analysis, capturing the essential peaks and valleys of the operational cycle.
| Load Step | Stress Ratio, \(R\) | Max Stress \(\sigma_{max}\) (MPa) | Min Stress \(\sigma_{min}\) (MPa) | Amplitude \(\sigma_a\) (MPa) | Number of Cycles per Block, \(n_i\) |
|---|---|---|---|---|---|
| 1 | 0.1 | 522.3 | 52.2 | 235.1 | 1 |
| 2 | 0.3 | 450.0 | 135.0 | 157.5 | 4 |
| 3 | 0.5 | 300.0 | 150.0 | 75.0 | 15 |
| 4 | 0.0 | 100.0 | 0.0 | 50.0 | 80 |
Fatigue Calculation and Damage Accumulation: The fatigue analysis computes the damage contributed by each load step \(i\) using the Miner’s Rule:
$$ D = \sum_{i=1}^{k} \frac{n_i}{N_i} $$
where \(n_i\) is the number of cycles applied at a given stress level, and \(N_i\) is the number of cycles to failure at that same stress level, interpolated from the S-N curve. Failure is predicted when the total cumulative damage \(D \geq 1\). The analysis also reports the fatigue life, which is the number of repetitions of the defined loading block required to reach \(D=1\).
Results and Discussion
The integrated simulation methodology provides a comprehensive assessment of the gear shafts‘ performance.
Static Analysis Result: The maximum equivalent stress was found to be 522.3 MPa, located at the gear-spline transition. This value is well below the yield strength (835 MPa), confirming a static safety factor of 1.60. The stress contour clearly shows the path of contact loading across the tooth flank, with secondary concentrations at the root fillet, aligning perfectly with theoretical expectations for loaded gear shafts.
Fatigue Analysis Result: The fatigue life calculation for the critical node (841) on the gear shafts yielded a life of \(N_{life} = 433,600\) repetitions of the defined operational loading block. Furthermore, the cumulative damage after a predefined service interval of 100,000 cycles was calculated:
$$ D_{100k} = 0.23 $$
Since \(D_{100k} < 1\), the analysis confirms that the gear shafts possess sufficient fatigue strength for the target service life under the investigated severe operating conditions. The primary failure mode is predicted to be subsurface-originated fatigue pitting, initiating in the region of highest alternating shear stress below the contact surface.
The table below summarizes the key performance indicators for the analyzed gear shafts:
| Assessment Criteria | Result | Requirement | Status |
|---|---|---|---|
| Max Von Mises Stress | 522.3 MPa | < 835 MPa (Yield) | PASS |
| Static Safety Factor | 1.60 | > 1.0 | PASS |
| Fatigue Life (Block Cycles) | 433,600 | > Target Life | PASS |
| Cumulative Damage @ 100k Cycles | 0.23 | < 1.0 | PASS |
Conclusion
This study demonstrates a robust and practical framework for the contact fatigue life evaluation of critical gear shafts in demanding applications. By integrating multi-body dynamics simulation with advanced nonlinear finite element analysis and fatigue post-processing, the method moves beyond simplistic static analysis. The key conclusions are:
- The dynamic loads extracted from a full system model in ADAMS provide a realistic and severe input for the stress analysis of the gear shafts, far superior to using nominal or theoretical torques.
- The static contact finite element analysis successfully identifies the stress concentrations in the gear shafts, both at the meshing teeth and at geometric transitions like the gear-to-spline interface, with a calculated safety factor confirming static integrity.
- Employing the stress-life approach with a statistically derived P-S-N curve (99% survival) allows for a conservative and reliable fatigue life prediction. The results indicate that the designed gear shafts meet both static and fatigue strength requirements for the specified heavy-duty operational cycle.
The methodology, encompassing Pro/E, MATLAB, ADAMS, and ANSYS, establishes a high-fidelity virtual prototyping loop. It has significant reference value for the design, evaluation, and failure analysis of gear shafts and similar load-bearing components where contact fatigue is a dominant failure mode. This approach enables engineers to optimize designs for weight, performance, and longevity before physical prototyping, reducing development time and cost while enhancing reliability.