
I have long been interested in the warm precision forging of straight bevel gears because these components are widely used in vehicles, machine tools, ships, and many other transmission systems. In my view, the central difficulty in the precision forging of straight bevel gears is not merely obtaining a complete tooth profile but obtaining a complete tooth profile while keeping the forging load, the strain and stress gradients, and the temperature gradients under control. When the tooth cavity is filled only by conventional open-die precision forging, the small end of the straight bevel gear often suffers from incomplete filling, and the die experiences severe local loading. This contradiction between tooth filling and die life is the main motivation for the present numerical study. I propose a central shunting precision forging process for straight bevel gears and compare it with traditional open precision forging using three-dimensional finite element simulation. The results show that central shunting is beneficial for the filling of straight bevel gears, and it reduces the forming load, the strain and stress differences along the tooth width, and the temperature difference along the tooth width.
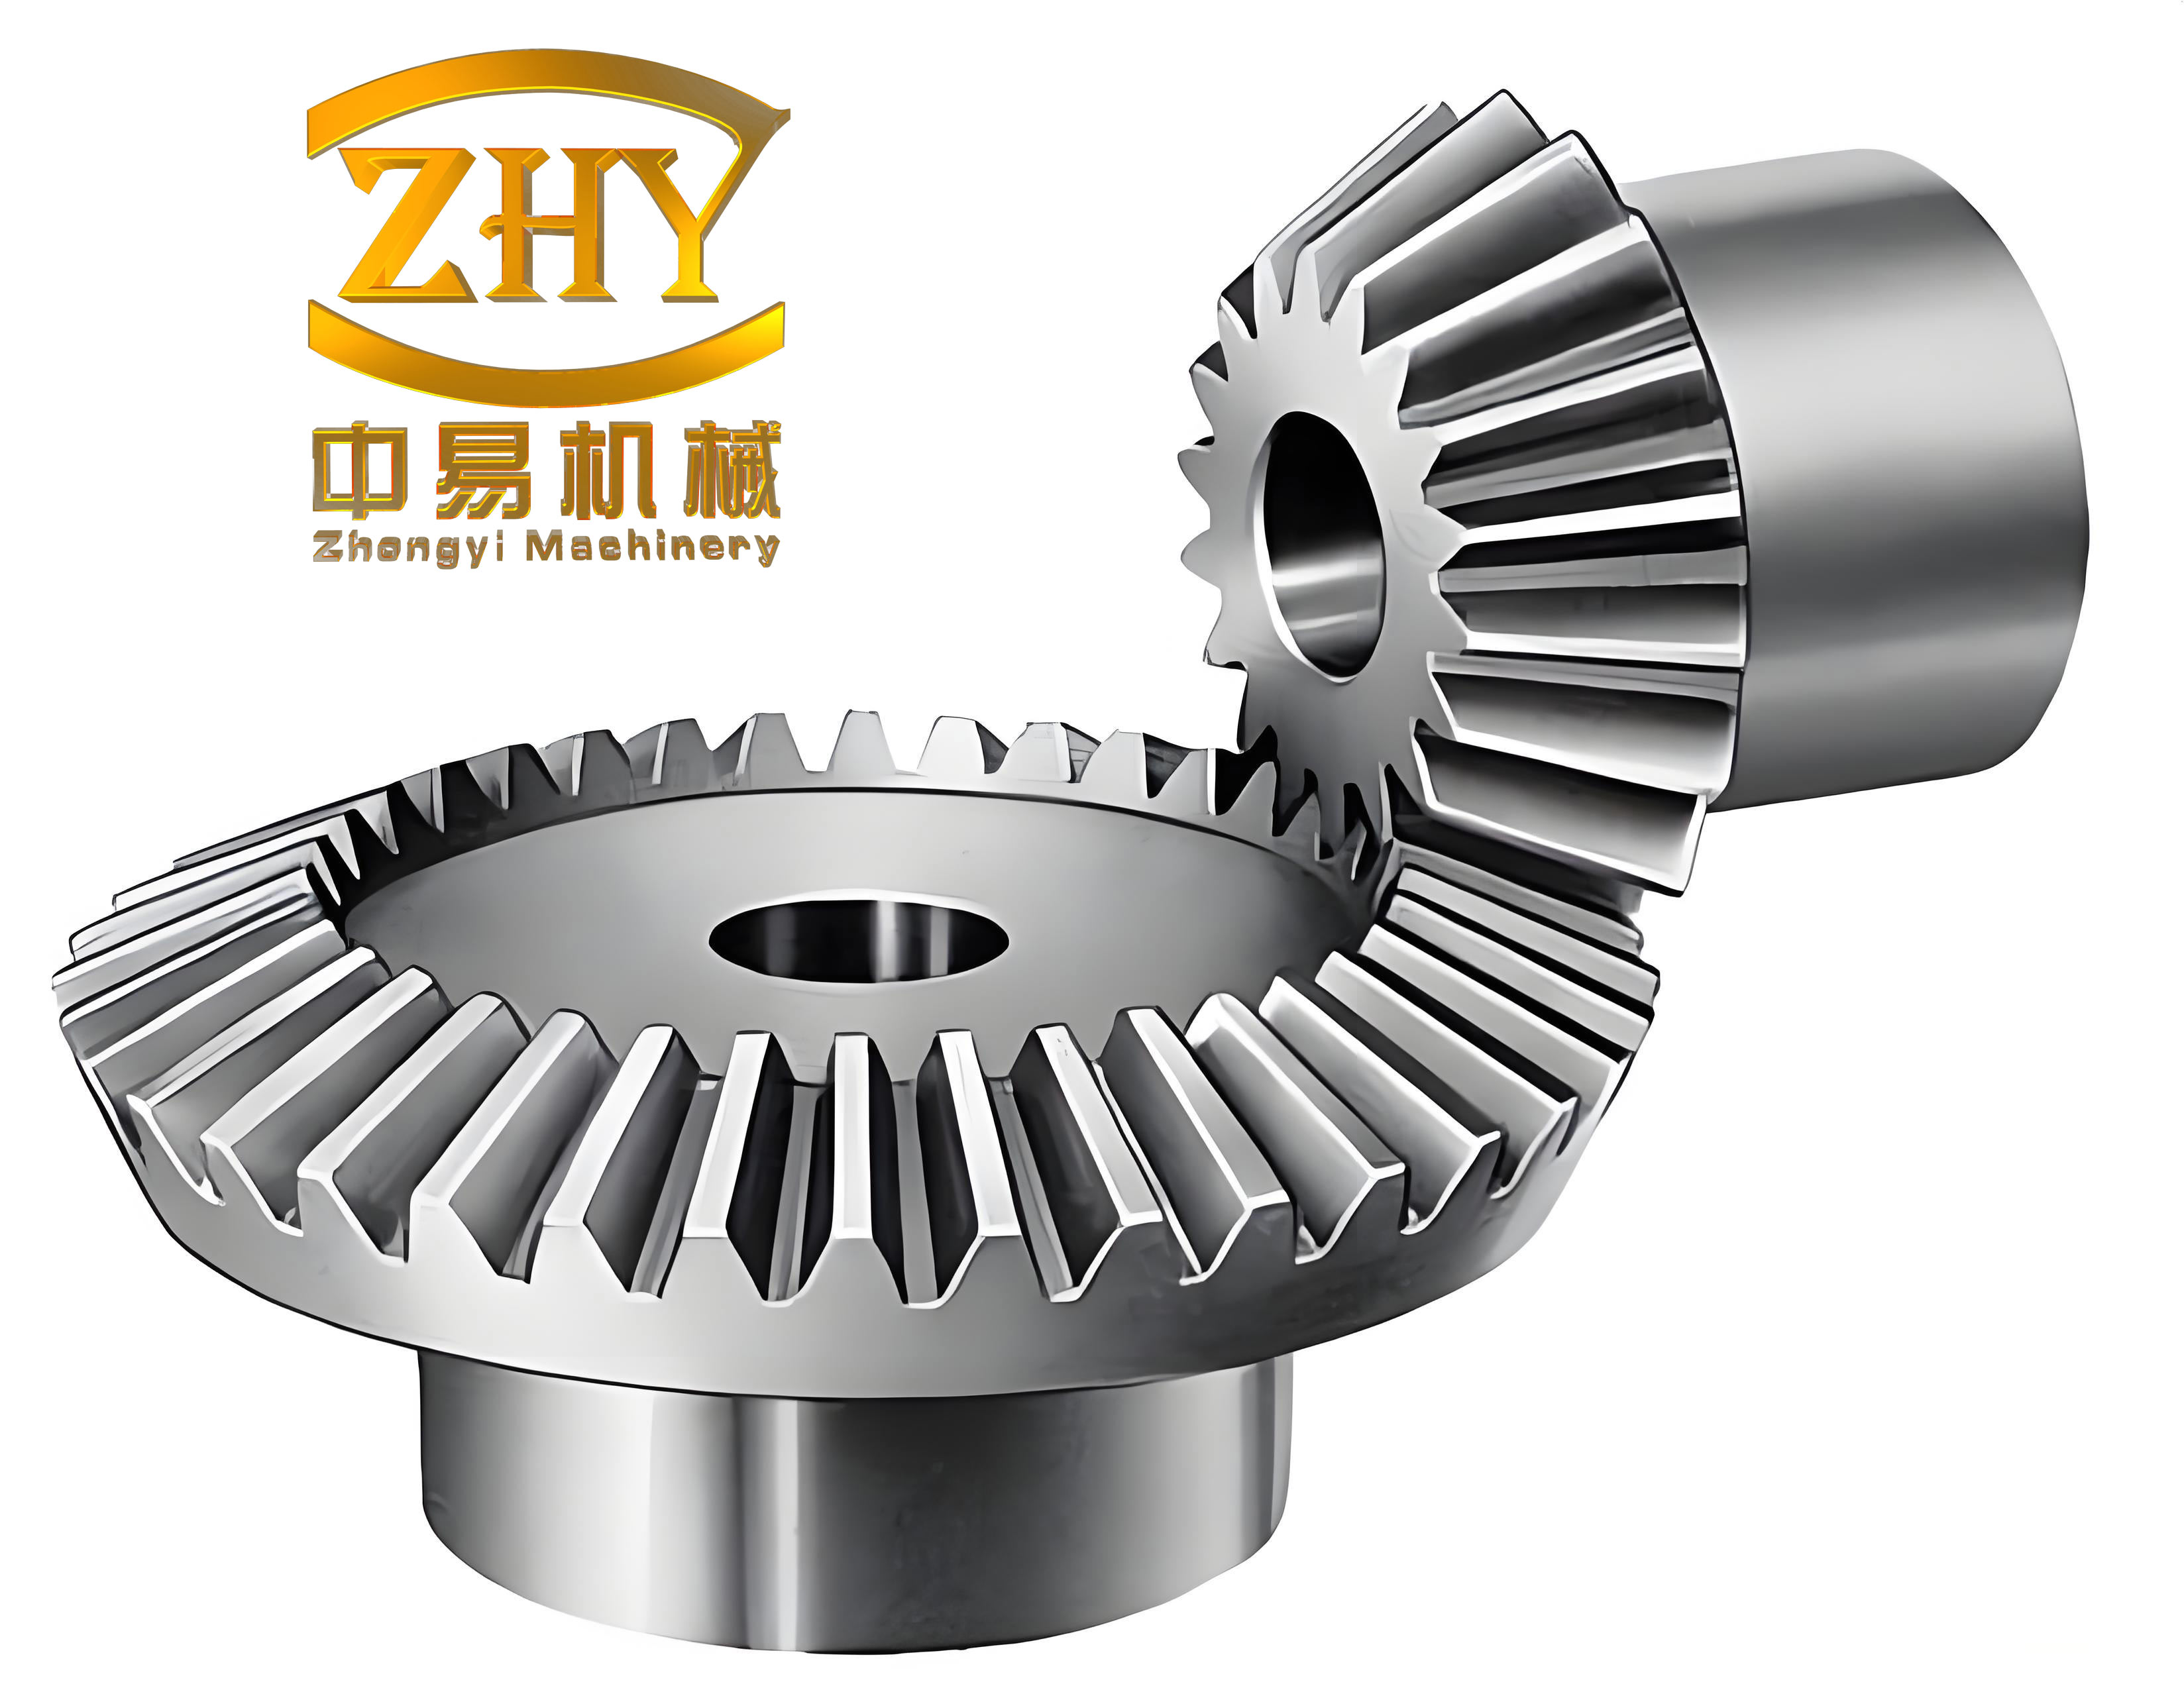
Straight bevel gears are especially sensitive to non-uniform metal flow because their teeth converge toward the small end. During warm forging, the small end cools faster than the large end, and the tooth cavity at the small end becomes difficult to fill. If I use a single open-die forging step, the material must simultaneously fill the tooth cavity and form flash. The flash region is often the only low-resistance flow path, so the material tends to flow outward rather than into the small-end tooth tips. As a result, the small-end tooth tips remain unfilled, while the die load rises sharply at the end of the stroke. This behavior is not acceptable for precision forging of straight bevel gears. I therefore introduce a central shunting region in the preform. The shunting region acts as a controlled low-resistance volume during final forging, allowing the material to flow into the tooth cavity while excess material can move into the central relief instead of only into the flash. The central shunting process can be regarded as a two-step precision forging route: pre-forging with an upper punch boss and final forging with a flat upper punch. The pre-forging step creates a central recess in the small-end face of the straight bevel gear blank, and the final forging step uses that recess as the shunting cavity.
The geometric parameters of the straight bevel gear investigated in my simulation are summarized in Table 1. The gear has 20 teeth, a module of 2.75 mm, and a pressure angle of 20°. The material is 18CrMnTi, a common carburizing steel for transmission gears. The basic dimensional relationships for a straight bevel gear can be expressed as follows.
$$d = m z$$
$$h_a = m$$
$$h_f = 1.25 m$$
$$\alpha = 20^\circ$$
Here, \(d\) is the pitch diameter, \(m\) is the module, \(z\) is the number of teeth, \(h_a\) is the addendum, \(h_f\) is the dedendum, and \(\alpha\) is the pressure angle. For the present straight bevel gear, \(d = 2.75 \times 20 = 55\) mm, \(h_a = 2.75\) mm, and \(h_f = 1.25 \times 2.75 = 3.4375\) mm. These values define the tooth height and provide the basis for the die cavity geometry. Because the gear is a straight bevel gear, the tooth thickness and tooth height vary along the cone distance. This variation is the reason why the small end is more difficult to fill than the large end.
| Parameter | Symbol | Value | Unit |
|---|---|---|---|
| Number of teeth | \(z\) | 20 | — |
| Module | \(m\) | 2.75 | mm |
| Pressure angle | \(\alpha\) | 20 | ° |
| Pitch diameter | \(d\) | 55 | mm |
| Addendum | \(h_a\) | 2.75 | mm |
| Dedendum | \(h_f\) | 3.4375 | mm |
| Material | — | 18CrMnTi | — |
I built the forging models in a CAD environment and then exported the die and billet geometries as STL files for the finite element solver. The pre-forging upper die includes an integrated boss, while the pre-forging lower die contains the tooth cavity. The final forging upper die is flat, and the final forging lower die contains the same tooth cavity as the open-die case. The traditional open precision forging process uses the final forging die set in a single stroke. In other words, the traditional open precision forging of straight bevel gears has no pre-forging recess and no central shunting volume. This difference is the core of my comparative study.
The finite element simulation was performed with DEFORM-3D. I used a three-dimensional rigid-plastic formulation coupled with heat transfer. The billet was discretized with approximately 80,000 elements. The initial forging temperature was 800 °C. The upper and lower dies were initially at 200 °C. The upper die moved downward at 50 mm/s. The friction coefficient between the billet and the dies was 0.25, and I assumed good lubrication. The heat transfer coefficient between the billet and the air was 0.02 N/(s·mm·°C). The heat transfer coefficient between the billet and the dies was 5 N/(s·mm·°C). These parameters are listed in Table 2.
| Simulation parameter | Symbol | Value | Unit |
|---|---|---|---|
| Initial billet temperature | \(T_0\) | 800 | °C |
| Initial die temperature | \(T_d\) | 200 | °C |
| Upper die velocity | \(v\) | 50 | mm/s |
| Friction coefficient | \(\mu\) | 0.25 | — |
| Billet-air heat transfer coefficient | \(h_{\text{air}}\) | 0.02 | N/(s·mm·°C) |
| Billet-die heat transfer coefficient | \(h_{\text{die}}\) | 5 | N/(s·mm·°C) |
| Number of elements | \(N_e\) | 80,000 | — |
| Material | — | 18CrMnTi | — |
For the constitutive response of 18CrMnTi at warm forging temperatures, I used a thermo-viscoplastic flow stress model of the following general form.
$$\sigma = K \varepsilon^n \dot{\varepsilon}^m \exp\left(\frac{Q}{RT}\right)$$
Here, \(\sigma\) is the flow stress, \(\varepsilon\) is the effective strain, \(\dot{\varepsilon}\) is the effective strain rate, \(T\) is the absolute temperature, \(Q\) is the activation energy, \(R\) is the universal gas constant, and \(K\), \(n\), and \(m\) are material constants. The exponential term captures the thermal softening effect, which is important because the small end of a straight bevel gear can cool significantly during forging. The strain-rate sensitivity term is also important because the upper die moves at a relatively high speed, and the local strain rate in the tooth cavity can vary strongly from the large end to the small end. In my simulation, the flow stress is updated at each time step according to the local temperature and strain rate.
The heat transfer during forging is governed by the transient heat conduction equation.
$$\rho c_p \frac{\partial T}{\partial t} = \nabla \cdot (k \nabla T) + \dot{q}$$
where \(\rho\) is density, \(c_p\) is specific heat, \(k\) is thermal conductivity, and \(\dot{q}\) is the internal heat generation rate due to plastic deformation. The internal heat generation is related to the plastic work rate by
$$\dot{q} = \beta \sigma \dot{\varepsilon}$$
where \(\beta\) is the Taylor-Quinney coefficient, often taken between 0.8 and 1.0 for metal forming. This term is responsible for the temperature rise in the tooth region, especially at the large end where the local strain is high. At the same time, heat is lost to the dies and to the environment. The competition between plastic heating and die chilling determines the final temperature field. In my results, the central shunting process produces a more balanced competition than the traditional open process, and this balance helps the straight bevel gear tooth cavity fill more uniformly.
The forming load is obtained by integrating the normal and shear stresses over the contact area between the billet and the die.
$$F = \int_A \sigma_n \, dA + \int_A \tau \, dA$$
Here, \(\sigma_n\) is the normal contact stress, \(\tau\) is the shear friction stress, and \(A\) is the instantaneous contact area. In practice, the load-displacement curve is more informative than a single force value because it shows when the tooth cavity begins to resist filling. I therefore recorded the load-time curves for pre-forging, final forging, and traditional open forging. The load comparison is one of the most important outputs of my study because it directly reflects the benefit of central shunting for straight bevel gears.
Figure 4 in the original study showed the load-time curves for central shunting pre-forging and final forging, while Figure 5 showed the load-time curve for traditional open precision forging. In my analysis, I summarize those curves numerically in Table 3. The pre-forging maximum load is 5.44 MN, the final forging maximum load is 5.15 MN, and the traditional open forging maximum load is 9.09 MN. The maximum load of the central shunting route is therefore governed by the pre-forging step, and it is substantially lower than the traditional open forging load. The load reduction can be calculated as follows.
$$R_F = \frac{F_{\max,\text{open}} – F_{\max,\text{central}}}{F_{\max,\text{open}}} \times 100\%$$
Using the values above,
$$R_F = \frac{9.09 – 5.44}{9.09} \times 100\% \approx 40.2\%$$
If I compare the traditional open forging load with the final forging load of the central shunting route, the reduction is even larger.
$$R_F’ = \frac{9.09 – 5.15}{9.09} \times 100\% \approx 43.3\%$$
This reduction is significant for the precision forging of straight bevel gears because lower forming load means lower die stress, less press capacity required, and potentially longer die life. I also observed that the traditional open forging load rises sharply at the end of the stroke, whereas the central shunting loads rise more gradually. The sharp rise in the open process is a sign that the tooth cavity is nearly closed and the material has no easy escape path. The central recess in the shunting process provides an additional flow path, so the load does not spike as severely.
| Process | Stage | Maximum load \(F_{\max}\) / MN | Load reduction relative to open forging / % |
|---|---|---|---|
| Central shunting precision forging | Pre-forging | 5.44 | 40.2 |
| Central shunting precision forging | Final forging | 5.15 | 43.3 |
| Traditional open precision forging | Single stroke | 9.09 | — |
The equivalent strain field provides a direct measure of deformation homogeneity. In the central shunting process, the pre-forging and final forging stages produce a relatively uniform strain distribution along the tooth width. The average equivalent strain in the final forging is about 2.1, and the difference between the maximum and minimum values along the tooth width is small. In the traditional open forging process, the strain distribution is much less uniform. The maximum equivalent strain is concentrated near the small end and the tooth root, while the middle of the tooth width experiences lower strain. The maximum strain difference is close to 2.2. This large difference indicates that the material in different regions of the straight bevel gear undergoes very different amounts of plastic deformation.
The equivalent strain can be written as
$$\bar{\varepsilon} = \int \sqrt{\frac{2}{3} d\varepsilon_{ij} d\varepsilon_{ij}}$$
where \(d\varepsilon_{ij}\) is the plastic strain increment tensor. The equivalent stress, often used to compare with the flow stress, is
$$\sigma_{\text{eq}} = \sqrt{\frac{1}{2}\left[(\sigma_1-\sigma_2)^2 + (\sigma_2-\sigma_3)^2 + (\sigma_3-\sigma_1)^2\right]}$$
where \(\sigma_1\), \(\sigma_2\), and \(\sigma_3\) are the principal stresses. I used these definitions to evaluate the stress and strain fields in the straight bevel gear forgings. In the central shunting pre-forging stage, the maximum equivalent stress appears near the small-end tooth tip, followed by the large-end tooth tip. In the final forging stage, the maximum equivalent stress appears near the large-end tooth tip and is about 500 MPa. The stress difference along the tooth width is small. In the traditional open forging process, the maximum equivalent stress is close to 900 MPa and appears at the small-end tooth tip. The stress distribution is highly non-uniform, with alternating high-stress and low-stress regions along the tooth width. Such a non-uniform stress field increases the risk of residual stress, stress concentration, and premature failure of the straight bevel gear.
| Quantity | Central shunting precision forging | Traditional open precision forging |
|---|---|---|
| Average equivalent strain in final tooth | ≈ 2.1 | Non-uniform, with large local variation |
| Maximum strain difference along tooth width | Small | ≈ 2.2 |
| Maximum equivalent stress | ≈ 500 MPa | ≈ 900 MPa |
| Stress distribution along tooth width | Relatively uniform | Highly non-uniform |
| Typical high-stress location | Large-end tooth tip in final forging | Small-end tooth tip |
The temperature field is another critical factor in the warm precision forging of straight bevel gears. In the central shunting process, the pre-forging temperature field shows the highest temperature at the large-end tooth profile, around 870 °C, while the small-end face is the coolest region. The overall temperature difference along the tooth width is relatively small, and the temperature is about 800 °C over much of the tooth. In the final forging stage, the highest temperature is again at the large-end tooth profile and the flash region, approaching 900 °C. This temperature rise is caused by plastic deformation heating. Because the central recess provides a shunting path, the small-end temperature after final forging is more uniform than after pre-forging. In the traditional open forging process, the maximum temperature reaches nearly 950 °C at the large-end and small-end tooth tips, while the minimum temperature in the middle region can fall to about 280 °C. The temperature difference along the tooth width is therefore very large.
The temperature uniformity can be quantified by a simple index.
$$\Delta T = T_{\max} – T_{\min}$$
$$U_T = \frac{T_{\max} – T_{\min}}{T_{\text{avg}}} \times 100\%$$
For the central shunting process, the temperature difference along the tooth width is on the order of 100 °C, whereas for the traditional open process it can exceed 600 °C. A large temperature difference is harmful for several reasons. First, it causes non-uniform flow stress, so some regions flow easily while others resist deformation. Second, it produces residual thermal stresses after cooling. Third, it increases the thermal load on the die, especially at the small end where the die surface is in contact with cooler and harder material. For straight bevel gears, the small end is already the most difficult region to fill, and a large temperature difference makes the problem worse. The central shunting process reduces this problem by allowing the material to flow into the tooth cavity before the small end becomes too cold and too strong.
| Temperature quantity | Central shunting precision forging | Traditional open precision forging |
|---|---|---|
| Maximum temperature | ≈ 900 °C | ≈ 950 °C |
| Minimum temperature | ≈ 800 °C | ≈ 280 °C |
| Temperature difference along tooth width | ≈ 100 °C | > 600 °C |
| Dominant heating mechanism | Plastic deformation heating | Plastic deformation heating and severe local chilling |
| Dominant cooling mechanism | Die chilling and air convection | Die chilling and air convection |
The forming quality of the straight bevel gear is the final and most visible indicator of process performance. In my simulation, the central shunting process produces a pre-forged gear with a completely filled tooth profile. The final forged gear also has a completely filled tooth profile, with a smooth and full tooth surface, a symmetric tooth profile, and a small, uniform flash. In contrast, the traditional open precision forging produces a gear with lower tooth accuracy. The tooth tips are not completely filled, and the filling is non-uniform. The tooth surface is not full or smooth, and the small-end tooth profile is especially asymmetric and severely deformed. The flash is larger and non-uniform. These observations confirm that the central shunting process is more suitable for the precision forging of straight bevel gears.
The filling ratio can be defined as
$$\eta_{\text{fill}} = \frac{A_{\text{filled}}}{A_{\text{cavity}}} \times 100\%$$
where \(A_{\text{filled}}\) is the filled area of the tooth cavity and \(A_{\text{cavity}}\) is the total tooth cavity area. In the central shunting process, \(\eta_{\text{fill}}\) approaches 100% for both the pre-forged and final forged straight bevel gears. In the traditional open process, \(\eta_{\text{fill}}\) is lower, particularly at the small end. The flash ratio can be defined as
$$\eta_{\text{flash}} = \frac{V_{\text{flash}}}{V_{\text{forging}}} \times 100\%$$
where \(V_{\text{flash}}\) is the flash volume and \(V_{\text{forging}}\) is the forged gear volume. The central shunting process produces a smaller and more uniform flash, which means that less material is wasted and less trimming is required. This is another practical advantage for the precision forging of straight bevel gears.
| Quality indicator | Central shunting precision forging | Traditional open precision forging |
|---|---|---|
| Tooth profile filling | Complete | Incomplete, especially at small end |
| Tooth surface smoothness | Good | Poor |
| Tooth profile symmetry | Good | Poor at small end |
| Flash size | Small and uniform | Large and non-uniform |
| Overall forming quality | High | Low |
The mechanism behind these improvements can be explained by the material flow behavior. In a conventional open precision forging of straight bevel gears, the billet is compressed between the upper punch and the lower die. The material near the small end must flow radially outward and simultaneously fill the tooth cavity. The tooth cavity is narrow, and the small end has a high surface-to-volume ratio, so it loses heat quickly. As the small-end material cools, its flow stress increases. The material then prefers to flow into the flash rather than into the small-end tooth cavity. This is why the small-end tooth tips remain unfilled and why the load rises sharply at the end of the stroke. In the central shunting process, the pre-forged recess reduces the resistance in the central region. During final forging, the material can flow into the central recess as well as into the tooth cavity. This additional flow path lowers the hydrostatic pressure in the central region and changes the stress state in the tooth cavity. The material is therefore more likely to fill the small-end tooth cavity before the flash becomes the dominant flow path. The central recess acts as a temporary reservoir and distributes the deformation more evenly along the tooth width.
I can express the effect of the shunting volume on the local pressure with a simplified relation. If the shunting volume is \(V_s\) and the tooth cavity volume is \(V_c\), then the flow resistance ratio can be approximated as
$$R_{\text{flow}} \propto \frac{V_c}{V_c + V_s}$$
When \(V_s = 0\), as in the traditional open process, the flow resistance ratio is highest. When \(V_s > 0\), as in the central shunting process, the flow resistance ratio is lower, and the material has more freedom to move into the tooth cavity. Of course, the actual flow behavior is three-dimensional and temperature-dependent, but this simple relation captures the essential idea. The central shunting process does not eliminate the flash, but it delays the dominance of flash flow and allows the tooth cavity to fill more completely.
The die life is also affected by the forming load and the temperature field. The die stress scales with the contact pressure, which in turn scales with the forming load and the contact area.
$$\sigma_{\text{die}} \propto \frac{F_{\max}}{A_{\text{contact}}}$$
Because the central shunting process reduces \(F_{\max}\), the die stress is reduced for a given contact area. In addition, the temperature difference along the tooth width is smaller, so the thermal stress on the die is lower. The combination of lower mechanical stress and lower thermal stress should improve the die life for the precision forging of straight bevel gears. This is important because the die cost is a major part of the total cost in gear forging. A process that can fill the tooth cavity and reduce the die load is therefore highly desirable.
The thermal stress in the die can be approximated by
$$\sigma_{\text{th}} = E \alpha_T \Delta T$$
where \(E\) is the elastic modulus of the die material, \(\alpha_T\) is the coefficient of thermal expansion, and \(\Delta T\) is the local temperature difference. A smaller \(\Delta T\) directly reduces \(\sigma_{\text{th}}\). In the traditional open process, the large temperature difference along the tooth width produces a large thermal stress, which can lead to die cracking or premature wear. In the central shunting process, the smaller temperature difference reduces this risk. The mechanical stress is also lower because the forming load is lower. Therefore, the central shunting process addresses both the filling and the die life problems at the same time.
From a process design perspective, the central shunting process requires careful control of the pre-forging recess. If the recess is too small, it will not provide enough shunting volume, and the final forging will behave like a traditional open forging. If the recess is too large, the pre-forging load may increase, and the final forging may not have enough material to fill the tooth cavity. The optimal recess volume depends on the tooth cavity volume, the flash geometry, the friction condition, and the temperature field. I would recommend a systematic parametric study to determine the best recess depth and diameter for a given straight bevel gear. In my simulation, the recess produced by the upper punch boss is sufficient to improve tooth filling and reduce the load, but it does not create an excessive amount of material waste. The pre-forged recess is closed or nearly closed during final forging, so the final gear geometry is not compromised.
The strain rate in the tooth cavity can be estimated by
$$\dot{\varepsilon} \approx \frac{v}{h}$$
where \(v\) is the die velocity and \(h\) is the instantaneous height of the deforming region. Near the end of the stroke, \(h\) becomes small, so the strain rate becomes large. This is one reason why the load rises sharply in the traditional open process. In the central shunting process, the shunting volume allows the material to continue flowing without a correspondingly large increase in strain rate in the tooth cavity. The load curve is therefore smoother, and the final load is lower. The strain-rate sensitivity of 18CrMnTi also means that a lower strain rate reduces the flow stress, which further reduces the load. This is a positive feedback effect that favors the central shunting process.
The temperature rise due to plastic deformation can be estimated by
$$\Delta T_{\text{plastic}} = \frac{\beta}{\rho c_p} \int \sigma \, d\varepsilon$$
If the deformation is concentrated in a small region, the local temperature rise can be large. In the traditional open process, the small-end tooth tip experiences severe local deformation, so the local temperature rise is high. At the same time, the small-end surface loses heat to the die, so the net temperature can be either high or low depending on the local balance. In my simulation, the traditional open process shows a very wide temperature range, from about 280 °C to about 950 °C. This wide range is undesirable. In the central shunting process, the deformation is more distributed, so the local temperature rise is more moderate, and the temperature range is narrower. The more uniform temperature field helps the material flow and reduces the thermal load on the die.
I also considered the effect of friction. The friction coefficient was set to 0.25 in my simulation. Friction affects the material flow by resisting sliding at the die-billet interface. In the tooth cavity, friction can prevent the material from reaching the small-end tooth tip. In the central shunting process, the central recess reduces the contact area in the central region and changes the friction path. The material can flow into the recess with less resistance, and the friction in the tooth cavity is partially relieved. This is another reason why the central shunting process improves filling. If the lubrication is poor, the benefit of central shunting may be reduced, but it should still be present as long as the recess provides a low-resistance flow path.
The friction stress can be described by the constant shear friction model.
$$\tau = m_f k$$
where \(m_f\) is the friction factor and \(k\) is the shear yield strength. In my simulation, the friction coefficient was 0.25, which corresponds to a moderate friction condition. A lower friction coefficient would reduce the load in both processes, but it would not eliminate the fundamental difference between them. The central shunting process has an inherent advantage because it changes the geometry of the flow path, not just the friction condition. This geometric advantage is robust and should be effective over a range of lubrication conditions.
The material flow in the central shunting process can be divided into three stages. In the first stage, the upper punch compresses the billet, and the material begins to flow radially outward. The central recess is not yet fully formed, so the deformation is similar to open forging. In the second stage, the recess forms, and the material near the center has an additional flow path. The tooth cavity begins to fill. In the third stage, the tooth cavity is nearly full, and the material continues to flow into the recess and the flash. The load rises more slowly than in the open process because the recess is still available. In the traditional open process, there is no second stage with a central flow path. The material can only flow into the tooth cavity and the flash. Once the flash becomes the easier path, the tooth cavity filling slows down or stops. This stage-based description helps explain why the central shunting process produces better filling and lower load.
The volume conservation during forging can be written as
$$V_0 = V_{\text{forging}} + V_{\text{flash}} + V_{\text{shunt}}$$
where \(V_0\) is the initial billet volume, \(V_{\text{forging}}\) is the final forging volume, \(V_{\text{flash}}\) is the flash volume, and \(V_{\text{shunt}}\) is the volume of the central recess that remains unfilled or is later closed. In an ideal precision forging process, \(V_{\text{shunt}}\) should be minimized in the final part, but during deformation it provides the necessary flow path. The pre-forging step creates a controlled \(V_{\text{shunt}}\), and the final forging step reduces it by allowing the material to flow back into the tooth cavity. This is a key design principle for the central shunting precision forging of straight bevel gears.
The effective strain rate sensitivity can be expressed as
$$m = \frac{\partial \ln \sigma}{\partial \ln \dot{\varepsilon}}$$
For warm forging of 18CrMnTi, \(m\) is positive, so a lower strain rate reduces the flow stress. The central shunting process tends to reduce the local strain rate in the tooth cavity because the material can flow into the recess. This is beneficial for reducing the load. The strain rate in the traditional open process is higher near the end of the stroke, so the flow stress is higher, and the load is higher. This is another mechanism by which central shunting improves the process.
The temperature dependence of the flow stress can be expressed as
$$\frac{\partial \sigma}{\partial T} < 0$$
for most metals in the warm forging range. A higher temperature reduces the flow stress. In the traditional open process, the small end is cooler, so its flow stress is higher. In the central shunting process, the small end is not as cool because the deformation is more distributed and the shunting volume helps maintain material flow. Therefore, the small-end flow stress is lower, and the tooth cavity fills more easily. The temperature effect and the geometric effect reinforce each other. This is a significant advantage for the precision forging of straight bevel gears.
The die contact area changes during forging. In the early stage, the contact area is small, and the load is low. In the later stage, the contact area increases, and the load rises. In the central shunting process, the contact area in the central region is reduced by the recess, so the load does not rise as much. In the traditional open process, the contact area increases continuously, and the load rises steeply. The contact area can be approximated by
$$A_{\text{contact}} = A_0 + \Delta A$$
where \(A_0\) is the initial contact area and \(\Delta A\) is the increase due to deformation. The central shunting process modifies \(\Delta A\) by allowing the material to flow into the recess instead of only spreading outward. This reduces the rate of contact area growth and therefore reduces the load.
The flash geometry also plays a role. In the traditional open process, the flash is often large and non-uniform. The flash acts as a resistance to material flow because it must be extruded through a narrow gap. The flash resistance increases as the flash becomes thinner. This is why the load rises sharply at the end of the stroke. In the central shunting process, the central recess provides an alternative path, so the flash does not have to accommodate all the excess material. The flash can be smaller and more uniform, and the load is lower. The flash thickness can be related to the flash resistance by
$$p_{\text{flash}} \propto \frac{1}{t_{\text{flash}}}$$
where \(p_{\text{flash}}\) is the pressure required to extrude the flash and \(t_{\text{flash}}\) is the flash thickness. A thinner flash requires higher pressure. The central shunting process helps avoid an excessively thin flash by providing another flow path, so the pressure does not spike.
The strain and stress differences along the tooth width can be summarized by the following indices.
$$\Delta \varepsilon = \varepsilon_{\max} – \varepsilon_{\min}$$
$$\Delta \sigma = \sigma_{\max} – \sigma_{\min}$$
In the central shunting process, both \(\Delta \varepsilon\) and \(\Delta \sigma\) are small. In the traditional open process, both are large. A large \(\Delta \sigma\) indicates a high risk of residual stress and distortion after forging. A large \(\Delta \varepsilon\) indicates non-uniform work hardening and possible local property differences. For straight bevel gears, uniform properties along the tooth width are desirable because the gear must transmit load smoothly across the entire tooth. The central shunting process therefore has a metallurgical advantage as well as a forming advantage.
The residual stress after forging can be estimated from the temperature and stress history. If the temperature difference is large, the thermal contraction during cooling is non-uniform, and residual stresses develop. The residual stress is roughly proportional to the temperature difference and the elastic modulus.
$$\sigma_{\text{res}} \propto E \alpha_T \Delta T$$
By reducing \(\Delta T\), the central shunting process reduces \(\sigma_{\text{res}}\). This is important for the dimensional accuracy of straight bevel gears. A gear with high residual stress may distort during heat treatment or during service. The central shunting process produces a more uniform temperature field and a more uniform stress field, so the final gear should have better dimensional stability.
The forging load can also be related to the flow stress and the projected area.
$$F \approx \sigma_{\text{flow}} A_{\text{projected}} \Phi$$
where \(\Phi\) is a constraint factor that depends on friction and geometry. In the traditional open process, the constraint factor is high because the material is constrained by the flash and the tooth cavity. In the central shunting process, the constraint factor is lower because the central recess provides an additional flow path. This is why the load is lower even though the flow stress and projected area may be similar. The central shunting process effectively reduces the geometric constraint, which is the main source of the high load in precision forging of straight bevel gears.
The strain path in the central shunting process is also more favorable. The material experiences a combination of compression, radial flow, and tangential flow. The central recess allows some material to flow inward, which reduces the amount of outward flow required. This changes the strain path from a predominantly outward flow to a more balanced flow. A balanced strain path reduces the risk of cracking and improves the final microstructure. For straight bevel gears, the small-end tooth tip is the most critical region. A balanced strain path helps the small-end tooth tip fill without excessive local strain. This is perhaps the most important benefit of the central shunting process.
The temperature field also affects the microstructure. Warm forging at around 800 °C can produce a fine-grained microstructure if the strain and temperature are well controlled. If the temperature is too low, the material may not recrystallize fully, and the flow stress may be high. If the temperature is too high, grain growth may occur. The central shunting process keeps the temperature more uniform, so the microstructure is more uniform. This is beneficial for the subsequent carburizing heat treatment of 18CrMnTi. A uniform microstructure helps ensure uniform hardness and wear resistance after heat treatment.
The die temperature also affects die life. The die surface temperature depends on the contact time, the contact pressure, and the heat transfer coefficient. In the traditional open process, the small end is in contact with cooler material for a longer time, so the die surface can be subjected to large thermal gradients. In the central shunting process, the contact conditions are more uniform, so the die temperature is more uniform. This reduces the thermal fatigue of the die. Thermal fatigue is a common failure mode in warm forging dies, and reducing the temperature gradient is an effective way to extend die life.
The die stress can be estimated by a thick-walled cylinder model or by finite element analysis. In my study, I used the finite element results to compare the die stress indirectly through the forming load and the contact pressure. The central shunting process reduces the maximum forming load by about 40% to 43%, which should translate into a similar reduction in die stress. This is a major economic benefit because die life is often the limiting factor in the precision forging of straight bevel gears.
The process window for central shunting precision forging should be established based on the billet temperature, the die temperature, the die velocity, and the lubrication condition. My simulation used a billet temperature of 800 °C, a die temperature of 200 °C, and a die velocity of 50 mm/s. These conditions are representative of warm forging. If the billet temperature is too low, the flow stress will be high, and the load will increase. If the billet temperature is too high, oxidation and grain growth may occur. An intermediate temperature is therefore preferred. The die velocity affects the strain rate and the temperature rise. A higher die velocity increases the strain rate and the load, but it also generates more heat. A lower die velocity reduces the load but may increase the heat loss to the dies. The optimal die velocity depends on the gear size and the press capacity. In my simulation, 50 mm/s provided a reasonable balance.
The lubrication condition affects the friction and the heat transfer. Good lubrication reduces friction and prevents sticking, but it can also affect the heat transfer between the billet and the die. In my simulation, I assumed good lubrication with a friction coefficient of 0.25. If the lubrication is poor, the friction coefficient may be higher, and the load may increase. The central shunting process is still beneficial because it changes the flow path, but the absolute load may be higher. Therefore, lubrication should be carefully controlled in production.
The pre-forging recess geometry is a key design variable. I used an upper punch boss to create the recess. The boss diameter and height determine the recess volume. If the recess volume is too small, the shunting effect is weak. If the recess volume is too large, the pre-forging load may increase, and the final forging may not completely close the recess. I recommend optimizing the recess volume by simulation and experiment. A good starting point is to set the recess volume to about 10% to 20% of the tooth cavity volume. This range provides sufficient shunting without excessive material waste. The exact value depends on the tooth geometry and the flash design.
The flash design is also important. A smaller flash reduces material waste but increases the flash resistance. A larger flash reduces the flash resistance but increases material waste and trimming cost. The central shunting process allows a smaller flash because the recess provides an additional flow path. This is a significant advantage for precision forging of straight bevel gears. I would recommend using a flash land that is wide enough to control the flow but not so wide that the load increases excessively. The optimal flash design can be found by simulation.
The die material should be selected based on the warm forging temperature and the load. For warm forging of 18CrMnTi at around 800 °C, a hot-work die steel with good thermal fatigue resistance is suitable. The die surface should be polished to reduce friction and prevent sticking. A surface coating such as a nitride or a hard coating can further improve die life. The central shunting process reduces the load and the temperature gradient, so it can extend the life of even a standard die material. However, the best results are obtained when the die material, the coating, and the lubrication are all optimized together.
The numerical simulation approach I used can be applied to other straight bevel gears with different modules and tooth counts. The basic principles remain the same. The central shunting process is most beneficial when the small end is difficult to fill, which is typically the case for straight bevel gears with small modules and long tooth widths. For larger modules, the tooth cavity is wider, and the filling difficulty may be lower. However, the load reduction benefit may still be significant. Therefore, the central shunting process should be considered for a wide range of straight bevel gears.
The simulation results can be used to design the pre-forging die and the final forging die. The pre-forging die should include the boss that creates the recess. The final forging die should be the same as the open forging die, except that the pre-forged recess is present in the billet. The process sequence is therefore simple: pre-forge with the boss, then final forge with the flat punch. This two-step sequence is easy to implement on a forging press with two stations. It does not require a complex die mechanism. This is a practical advantage for industrial production of straight bevel gears.
The energy consumption of the central shunting process is lower than that of the traditional open process because the forming load is lower. The energy required for forging can be estimated by
$$E = \int F \, ds$$
where \(F\) is the forming load and \(s\) is the stroke. A lower load over a similar stroke means lower energy consumption. In addition, the lower load reduces the wear on the press and the dies. The central shunting process is therefore more sustainable and more economical. For mass production of straight bevel gears, even a small reduction in energy per part can lead to significant savings.
The production rate of the central shunting process is comparable to that of the traditional open process. The pre-forging and final forging steps can be performed in sequence on the same press or on two presses. The additional pre-forging step adds a small amount of time, but the lower load may allow a higher production rate because the press can run faster. The net effect depends on the specific equipment and the part size. In many cases, the central shunting process can be implemented without a significant loss of productivity.
The quality of the final straight bevel gear depends on the accuracy of the die cavity and the control of the forging parameters. The central shunting process improves the filling, but it does not eliminate the need for precise die manufacturing. The die cavity should be machined to the required tolerance, and the die surfaces should be polished. The billet temperature should be controlled within a narrow range. The lubrication should be consistent. With these controls, the central shunting process can produce straight bevel gears with high precision and good surface finish.
In summary, my numerical simulation shows that the central shunting precision forging process is an effective method for the precision forging of straight bevel gears. It improves tooth filling, reduces the forming load, reduces the strain and stress differences along the tooth width, and reduces the temperature difference along the tooth width. These benefits are achieved by introducing a pre-forging recess that acts as a shunting volume during final forging. The process is practical and can be implemented with a simple two-step die sequence. The results provide a theoretical basis for solving the contradiction between tooth filling and die life in the precision forging of straight bevel gears.
The following conclusions can be drawn from my study.
First, the central shunting precision forging process can completely fill the tooth cavity of a straight bevel gear, including the small-end tooth tip. The traditional open precision forging process cannot fill the small-end tooth tip completely and produces a non-uniform tooth profile.
Second, the central shunting process reduces the maximum forming load from about 9.09 MN to about 5.44 MN, a reduction of about 40.2%. If the final forging load is compared, the reduction is about 43.3%. This lower load reduces the required press capacity and the die stress.
Third, the central shunting process produces a more uniform equivalent strain and equivalent stress distribution along the tooth width. The maximum equivalent stress is about 500 MPa, compared with about 900 MPa for the traditional open process. The strain difference along the tooth width is also much smaller.
Fourth, the central shunting process produces a more uniform temperature field. The temperature difference along the tooth width is about 100 °C, compared with more than 600 °C for the traditional open process. The more uniform temperature field reduces the risk of residual thermal stress and improves the filling behavior.
Fifth, the central shunting process produces a smaller and more uniform flash, which reduces material waste and trimming cost. The tooth surface is smoother and the tooth profile is more symmetric.
Sixth, the central shunting process can be implemented as a two-step forging sequence with a pre-forging boss and a flat final forging punch. This makes the process practical for industrial production of straight bevel gears.
Seventh, the central shunting process addresses both the tooth filling problem and the die life problem. The lower load and the more uniform temperature field reduce the mechanical and thermal loads on the die. This can extend die life and reduce production cost.
Eighth, the optimal design of the pre-forging recess and the flash should be determined by simulation and experiment. A recess volume of about 10% to 20% of the tooth cavity volume is a reasonable starting point. The flash should be small but sufficient to control the flow.
Ninth, the central shunting process is applicable to a wide range of straight bevel gears, especially those with small modules and long tooth widths where the small-end filling problem is most severe.
Tenth, the numerical simulation approach used in this study can be extended to other precision forging processes and other gear types. The combination of three-dimensional finite element analysis and process optimization is a powerful tool for improving forging quality and reducing cost.
I believe that the central shunting precision forging process represents a significant advance in the precision forging of straight bevel gears. It provides a practical way to overcome the trade-off between tooth filling and die life. With further optimization of the recess geometry, the flash design, and the process parameters, the central shunting process can be used in industrial production to manufacture high-quality straight bevel gears at lower cost and with higher efficiency.
For future work, I would recommend experimental validation of the simulation results, including measurements of the forming load, the temperature field, and the final gear geometry. I would also recommend studying the effect of different recess shapes, such as a spherical recess or a conical recess, on the material flow. In addition, the effect of the die coating and the lubrication on the filling behavior should be investigated. Finally, the fatigue life and the load-carrying capacity of the forged straight bevel gears should be evaluated to confirm that the central shunting process does not compromise the mechanical properties. These studies would further strengthen the case for the central shunting precision forging of straight bevel gears.
In conclusion, my numerical simulation demonstrates that the central shunting precision forging process is a promising technology for the precision forging of straight bevel gears. It improves filling, reduces load, homogenizes strain, stress, and temperature, and reduces flash. The process is practical, economical, and suitable for industrial application. It provides a theoretical and practical basis for solving the long-standing contradiction between tooth filling and die life in the precision forging of straight bevel gears.