
The continuous advancement in mechanical power transmission systems demands higher load capacity, efficiency, and longevity from core components. Among these, spiral bevel gears are critical elements for transmitting power between intersecting shafts, commonly found in automotive differentials, aerospace actuators, and heavy industrial machinery. Traditional spiral bevel gears with involute or circular-arc profiles, while effective, often face limitations in bending strength at the root and contact stress concentration. A promising evolution in this field is the application of the double-circular-arc tooth profile to spiral bevel gears, offering a significant performance enhancement.
Double-circular-arc spiral bevel gears feature a tooth profile composed of two conjugate circular arcs on a single tooth flank—a convex arc and a concave arc. This unique geometry fundamentally alters the contact characteristics during meshing. Unlike the typical line contact of conventional gears, this design facilitates multi-point and multi-pair contact patterns under load. The concave profile inherently increases the root thickness, dramatically improving bending strength and resistance to fatigue failure. Consequently, these gears exhibit superior load-bearing capacity and extended service life compared to standard spiral bevel gears, making them ideal for high-performance applications. However, the complex spatial curvature of their tooth surfaces presents a formidable challenge for accurate geometric modeling and precise manufacturing using conventional methods.
This article presents a comprehensive methodology for the digital design and virtual manufacturing of double-circular-arct spiral bevel gears, leveraging the power of virtual prototyping technology. The core of this approach lies in creating a fully integrated digital thread—from parametric three-dimensional modeling to simulated machining processes—within a virtual environment. This eliminates the dependency on costly and time-consuming physical prototypes in the initial design phases, allowing for rapid iteration, optimization, and validation before any metal is cut.
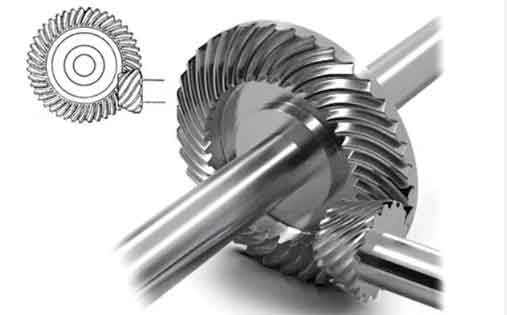
Fundamentals of Double-Circular-Arc Spiral Bevel Gear Design
The design of double-circular-arc spiral bevel gears originates from the basic rack principle, similar to their cylindrical counterparts. The tooth profile is defined in the normal plane of an imaginary basic rack. For this study, the standardized GB/T 12759-1991 profile is adopted due to its advantageous characteristics: a low addendum, a thick root section, and minimal heat treatment distortion. The primary geometric parameters for a sample gear pair are summarized in Table 1.
| Parameter | Pinion | Gear | Unit |
|---|---|---|---|
| Number of Teeth (z) | 12 | 37 | – |
| Module (m) | 6 | 6 | mm |
| Shaft Angle (Σ) | 90° | deg | |
| Pressure Angle (α) | 30° | deg | |
| Spiral Angle (β) | 35° | deg | |
| Face Width (b) | 46 | mm | |
| Pitch Diameter (d) | 72 | 222 | mm |
| Cutter Diameter | 228.6 | mm | |
The mathematical foundation for generating the tooth surface of double-circular-arc spiral bevel gears is based on the theory of gearing and coordinate transformations. The process simulates the machining action of a face-mill cutter with a double-circular-arc profile. The surface of each tooth flank is generated as the envelope of the family of cutter surfaces relative to the gear blank during a simulated roll motion. Key coordinate systems include the machine tool setting system \( S_m(X_m, Y_m, Z_m) \), the cradle system \( S_c(X_c, Y_c, Z_c) \), and the gear blank system \( S_g(X_g, Y_g, Z_g) \). The locus of the cutter center \( \mathbf{r}_c^{(c)}(u, \theta_c) \) and the unit normal vector \( \mathbf{n}_c^{(c)} \) are defined in the cradle system. Through a series of rotational transformations representing the machine root angle, offset, and the rolling motion between the imaginary generating gear (cradle) and the work gear, the family of cutter surfaces in the gear coordinate system is obtained. The meshing condition, governed by the equation of contact, is given by:
$$ \mathbf{n} \cdot \mathbf{v}^{(gc)} = 0 $$
where \( \mathbf{n} \) is the common normal vector at the contact point and \( \mathbf{v}^{(gc)} \) is the relative velocity between the cutter and the gear blank. Solving this equation simultaneously with the coordinate transformation yields the mathematical model of the generated tooth surface \( \mathbf{r}_g(u, \phi_c) \), where \( u \) is a surface parameter and \( \phi_c \) is the cradle rotation angle. This complex surface is the target for our digital modeling.
Virtual Prototyping Technology: A Paradigm Shift
Virtual prototyping (VP) represents a revolutionary shift from the traditional design-manufacture-test cycle. It is a simulation-based method that enables the creation, testing, and iterative refinement of a product’s digital mock-up under realistic operating conditions. For complex mechanical components like spiral bevel gears, VP offers unparalleled advantages. Designers and engineers can analyze assembly fit, perform motion simulation, conduct finite element analysis for stress and deformation, and simulate the entire manufacturing process—all before committing to physical production.
The benefits are manifold: a drastic reduction in development time and cost, the ability to explore and optimize numerous design alternatives rapidly, early detection of potential design flaws or manufacturing issues, and ultimately, a higher quality and more reliable product. In the context of double-circular-arc spiral bevel gears, where physical prototyping is exceptionally difficult and expensive, virtual prototyping is not just an advantage but a necessity for practical development and application.
Digital 3D Modeling of the Gear Tooth Surface
Accurate 3D geometric modeling is the cornerstone of the virtual prototyping process. For double-circular-arc spiral bevel gears, we employ a parametric, feature-based Computer-Aided Design (CAD) software to construct the model based on the mathematical surface generation principle described earlier. The process mimics the hypothetical generation process using a phantom crown gear.
The modeling sequence is as follows:
- Cutter Model Creation: The double-circular-arc profile of the face-mill cutter is sketched based on the basic rack parameters. This profile is then revolved around the cutter axis to create a solid 3D model of the cutter head, representing the cutting edges.
- Gear Blank Model Creation: The basic conical shape of the gear blank is created by revolving a sketch containing the gear’s back cone, front cone, and inner geometry.
- Simulation of the Generation Motion: The relative positioning between the cutter model and the gear blank model is established according to the machine setup parameters (cutter tilt, offset, sliding base, etc.). The Boolean subtraction operation is used to simulate the material removal of a single tooth space. This operation is performed at a specific instant of the roll cycle, effectively “cutting” one tooth slot into the blank.
- Pattern Completion: Using the circular pattern feature, the single cut tooth space is replicated around the gear axis according to the number of teeth, resulting in a complete, geometrically accurate 3D solid model of the double-circular-arc spiral bevel gear.
This digital model precisely encapsulates the complex curvature of the tooth flanks, including the transition between the convex and concave arcs, and serves as the master geometry for all subsequent virtual analyses and manufacturing simulations.
Virtual Machining Simulation and Process Analysis
With a validated digital model in hand, the next phase in the virtual prototyping workflow is to simulate its manufacture. This step is crucial for verifying the feasibility of the chosen machining strategy, detecting potential collisions, optimizing tool paths, and validating the final part geometry. For spiral bevel gears, which are typically produced on specialized gear cutting machines (e.g., Gleason or Klingelnberg), we can simulate the process using a 5-axis CNC machining center in a virtual environment, offering flexibility for prototyping or small-batch production.
A dedicated CNC simulation software (like VERICUT) is utilized. The core activities in this phase are:
- Virtual Machine Tool Build: A detailed 3D model of a 5-axis machining center (e.g., a V850-5AX type) is constructed or imported into the simulation environment. This model includes all critical kinematic components: the machine bed, linear X, Y, Z axes, rotary A and C axes, spindle, tool holder, fixtures, and the control system. The machine’s kinematic chain and post-processor are defined to interpret G-code correctly.
- Tooling Definition: A set of cutting tools required for the operation is defined. For roughing and finishing the complex tooth surfaces of spiral bevel gears, a combination of flat-end mills and ball-nose end mills is typically used. Their parameters are detailed in Table 2.
| Tool ID | Tool Type | Diameter / Radius | Material | Purpose |
|---|---|---|---|---|
| TX1 | Flat End Mill | Ø12 mm | Carbide | Roughing, slotting |
| TX2 | Ball-Nose End Mill | R5 mm | Carbide | Semi-finishing |
| TX3 | Ball-Nose End Mill | R3 mm | Carbide | Finishing |
| TX4 | Ball-Nose End Mill | R2 mm | Carbide | Fine finishing, root fillet |
- Workpiece and Fixture Setup: The gear blank (a simple conical cylinder) is mounted in the virtual workspace. The digital design model of the finished spiral bevel gear is used as the “stock” reference model for the simulation to check against.
- Toolpath Generation and Simulation: CAM software is used to generate multi-axis toolpaths. For a spiral bevel gear tooth slot, this involves complex 5-axis simultaneous motion to follow the curved surface. The generated NC code is loaded into the virtual machine controller. The simulation then runs, visually animating the material removal process step-by-step. The software calculates the in-process workpiece geometry, checks for gouging, collisions between tool/holder/fixture/machine, and verifies the final machined shape against the design model.
The simulation provides a powerful visual and analytical verification. Engineers can observe the cutting process, measure clearances, and ensure that the complex motion required to produce the double-circular-arc profile on the spiral bevel gears is executed correctly and safely. Any errors in the toolpath or machine setup can be identified and corrected in the virtual realm, preventing costly mistakes on the actual machine tool.
Performance Evaluation and Advantages of the Integrated Approach
The virtual prototyping platform enables not just manufacturing validation but also preliminary performance analysis of the designed double-circular-arc spiral bevel gears. While detailed FEA for contact stress requires specialized gear software, basic comparisons can be inferred from the geometry. The primary advantages confirmed through this digital approach are:
- Enhanced Load Capacity: The double-circular-arc profile inherently provides a larger root fillet and thicker tooth core compared to a standard involute spiral bevel gear of similar size. This directly translates to higher resistance to bending stress. The multi-point contact pattern distributes the load over a larger area on the tooth flank, reducing contact (Hertzian) stress.
- Improved Lubrication: The conjugate convex-concave contact creates favorable conditions for the formation of an elastohydrodynamic lubrication (EHL) film, reducing friction and wear.
- Reduced Noise and Vibration: The gradual engagement and multi-pair contact characteristic can lead to smoother transmission of motion and torque, potentially resulting in lower noise and vibration levels compared to conventional designs.
The integrated digital design and virtual manufacturing approach itself offers significant systemic advantages, as summarized in Table 3.
| Aspect | Traditional Physical Prototyping | Virtual Prototyping-Based Approach |
|---|---|---|
| Development Cycle Time | Long (weeks/months for machining, testing, redesign) | Short (days for model iteration and simulation) |
| Cost | High (material, specialized machine time, labor) | Low (primarily software and engineering time) |
| Design Iterations | Limited by cost and time; risky changes | Virtually unlimited; encourages optimization |
| Error Detection | Late stage, during physical test or assembly | Early stage, during design and simulation |
| Manufacturing Validation | Post-process, after NC code is run on machine | Pre-process, via virtual machining simulation |
| Risk | High risk of scrap and rework | Minimized risk before physical commitment |
Conclusion and Future Perspectives
This article has detailed a systematic and effective methodology for the digital design and virtual manufacturing of high-performance double-circular-arc spiral bevel gears. By integrating parametric 3D CAD modeling based on precise gear generation theory with advanced virtual machining simulation within a virtual prototyping framework, a complete digital thread is established. This approach successfully addresses the core challenge of accurately defining and validating the complex geometry of these advanced spiral bevel gears.
The virtual prototyping platform allows for the rapid creation, evaluation, and refinement of designs without the need for physical prototypes. It enables engineers to simulate the entire machining process, verifying toolpaths, avoiding collisions, and ensuring the manufacturability of the complex tooth forms. This significantly de-risks the development process, reduces lead time and cost, and accelerates the transition from concept to a validated, production-ready design.
The future of this field points towards even tighter integration. The next steps involve coupling the geometric model directly with high-fidelity finite element analysis (FEA) for precise stress, strain, and thermal prediction under load, and with multi-body dynamics (MBD) software for system-level noise, vibration, and harshness (NVH) analysis. Furthermore, the validated virtual machining process can be directly linked to adaptive manufacturing systems, closing the loop between digital design and physical production. The adoption of this comprehensive digital approach is pivotal for advancing the application of double-circular-arc spiral bevel gears and other complex mechanical components, driving innovation in high-power-density transmission systems across industries such as aerospace, automotive, and energy.