
As a materials engineer focused on industrial applications, I have long been concerned with the reliability of large section gear shafts in heavy machinery. Gear shafts are pivotal in transmitting torque and motion in equipment like ball mills, crushers, and marine propulsion systems. Their failure, often due to internal defects such as flakes (also known as white spots), can cause catastrophic breakdowns, leading to prolonged downtime and substantial economic losses. Flakes are internal cracks characterized by silver-white appearances on fracture surfaces, primarily caused by hydrogen embrittlement and residual stresses during manufacturing. In this study, I aimed to systematically investigate and optimize the production processes for 17CrNiMo6 steel gear shafts to mitigate flake sensitivity. Through a first-person perspective, I will detail the experimental approaches, results, and insights gained from this endeavor, emphasizing the role of process modifications in enhancing the integrity of gear shafts. The target is to achieve gear shafts with diameters exceeding 140 mm and lengths over 300 mm, which are particularly prone to flakes due to their large cross-sections and complex thermal histories.
Gear shafts manufactured from 17CrNiMo6 steel are typically subjected to carburizing to achieve high surface hardness (57-61 HRC) while maintaining a tough core (34-38 HRC). However, the presence of hydrogen—introduced during smelting, forging, or heat treatment—can lead to flake formation under stress. My investigation began with a thorough analysis of failed gear shafts, where ultrasonic testing revealed internal cracks indicative of flakes. These defects were often located deep within the material, making them undetectable without non-destructive evaluation. To address this, I hypothesized that optimizing key manufacturing steps—smelting, forging, carburizing, quenching, and tempering—could reduce hydrogen content, minimize stresses, and ultimately prevent flakes. This article presents my experimental journey, leveraging data from multiple trial productions to validate process improvements. Throughout, I will use tables and formulas to summarize findings, ensuring a comprehensive understanding of how each modification contributes to the durability of gear shafts.
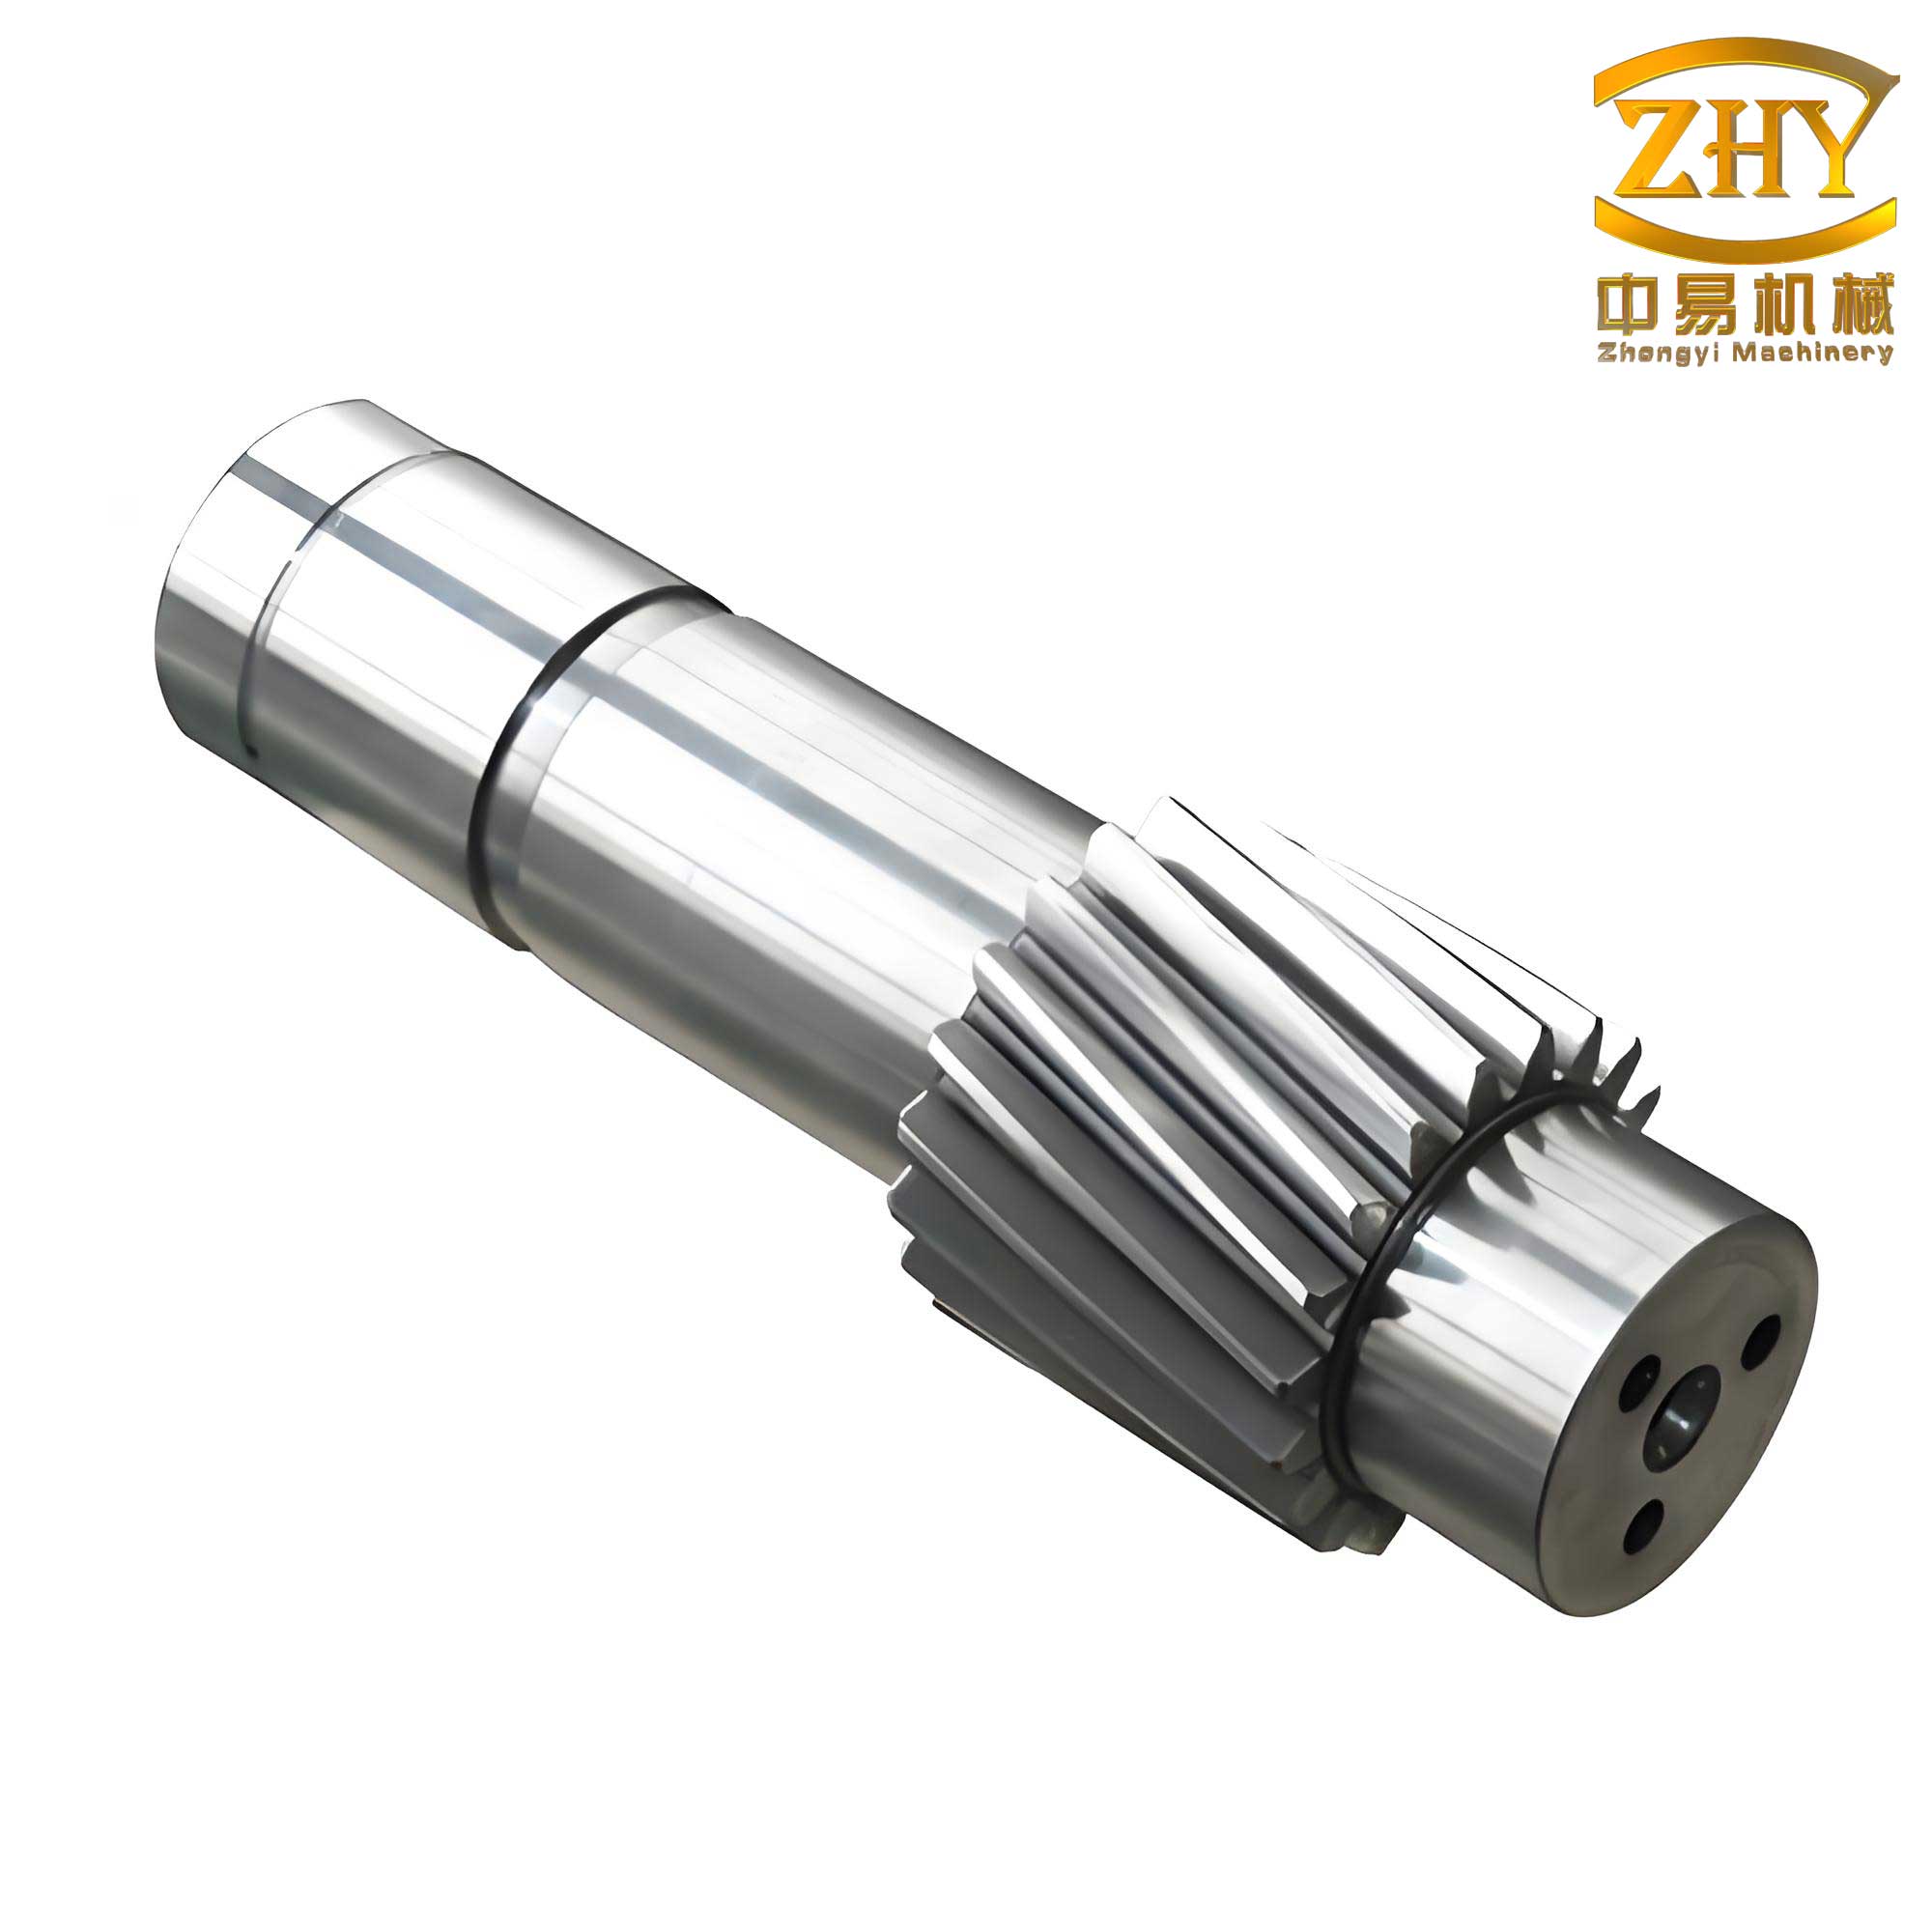
The material under investigation is 17CrNiMo6 steel, a low-carbon chromium-nickel-molybdenum alloy commonly used for high-strength gear shafts. Its nominal composition, as per industrial standards, includes carbon (0.15-0.20%), silicon (≤0.40%), manganese (0.40-0.60%), chromium (1.50-1.80%), nickel (1.40-1.70%), and molybdenum (0.25-0.35%). In my experiments, I obtained samples from multiple production batches to ensure consistency. Table 1 summarizes the chemical composition of the base material used in this study, confirming compliance with specifications. The gear shafts in focus had dimensions of approximately 142 mm in diameter and 330 mm in length, representing large sections where flakes are most likely to occur due to slower hydrogen diffusion and higher thermal gradients.
| Element | C | Si | Mn | S | P | Cr | Ni | Mo | Al | Nb |
|---|---|---|---|---|---|---|---|---|---|---|
| Specified Range | 0.15-0.20 | ≤0.40 | 0.40-0.60 | ≤0.035 | ≤0.035 | 1.50-1.80 | 1.40-1.70 | 0.25-0.35 | – | 0.030 max |
| Measured Average | 0.18 | 0.05 | 0.52 | 0.003 | 0.008 | 1.65 | 1.55 | 0.30 | 0.002 | 0.018 |
My experimental methodology involved a stepwise optimization of five critical processes: smelting, forging, carburizing, quenching, and tempering. Each step was designed to address specific factors contributing to flake formation, such as hydrogen ingress, stress accumulation, and microstructural inhomogeneities. For smelting, the original process included electric arc furnace melting, ladle refining, VD (Vacuum Degassing) for ≥15 minutes, and vacuum casting. I modified this by extending VD time to ≥18 minutes and adjusting niobium addition to 0.02% (from 0.03%) to reduce NbN precipitates, which can act as hydrogen traps and exacerbate cracking. In forging, the pre-heating, deformation, and post-forging heat treatment were revised. The original post-forging heat treatment involved normalizing at 880°C and tempering at 650°C for 60 hours; I increased the normalizing temperature to 950°C and extended tempering to 100 hours to enhance hydrogen diffusion. For carburizing, conducted at 930°C using isopropanol as a carburant, I focused on minimizing hydrogen uptake by optimizing atmosphere control. Finally, in quenching and tempering, the original process involved quenching from 820°C and triple tempering at 200°C; I introduced a pre-tempering hold of 6 hours and extended the total tempering time to 110 hours across multiple cycles to reduce residual austenite and stresses.
To quantify the effects of these optimizations, I employed various analytical techniques. Hydrogen content was measured using thermal desorption spectroscopy, while microstructure was examined via optical and scanning electron microscopy. Residual stress analysis was performed using X-ray diffraction, and mechanical properties were assessed through hardness and impact tests. The key metric was the absence of flakes in ultrasonic inspections after full processing. In the following sections, I will present results from comparative trials, using tables to highlight changes in composition and process parameters, and formulas to model hydrogen diffusion and phase transformations. This approach allowed me to systematically evaluate how each modification impacts the performance of gear shafts.
The optimization of smelting processes yielded significant changes in steel composition, particularly concerning elements that influence hydrogen behavior. By extending VD vacuum degassing time, I aimed to reduce dissolved hydrogen levels. However, an interesting outcome was the alteration in micro-alloying elements. Table 2 compares the chemical composition before and after smelting optimization for six trial gear shafts. The data shows that silicon and aluminum contents increased, while niobium decreased. This shift is critical because silicon and aluminum form compounds like SiC and AlN, which can immobilize hydrogen as non-diffusible species, thereby reducing flake sensitivity. Conversely, niobium tends to form NbN, which can promote cracking under stress. The reduction in niobium content, achieved by lowering niobium addition to 0.02%, helped minimize this risk. The hydrogen content after smelting was measured using the Sieverts’ law approximation: $$ C_H = k \sqrt{P_{H_2}} $$ where \( C_H \) is the hydrogen concentration, \( k \) is a temperature-dependent constant, and \( P_{H_2} \) is the hydrogen partial pressure. With extended VD time, \( P_{H_2} \) decreased, leading to a reduction in \( C_H \) from an average of 2.5 ppm to 1.8 ppm, as confirmed by gas analysis.
| Sample | Condition | C | Si | Mn | Cr | Mo | Al | Nb | H (ppm) |
|---|---|---|---|---|---|---|---|---|---|
| 1-3 | Before Optimization | 0.18-0.19 | 0.02-0.07 | 0.47-0.79 | 1.59-1.77 | 0.30-0.37 | 0.002 | 0.020-0.025 | 2.4-2.6 |
| 4-6 | After Optimization | 0.17-0.18 | 0.23-0.27 | 0.42-0.55 | 1.55-1.70 | 0.26-0.31 | 0.010-0.019 | 0.010-0.020 | 1.7-1.9 |
In forging, the primary goal was to homogenize microstructure and facilitate hydrogen effusion. The original forging process involved heating to 1150°C, followed by deformation and a post-forging heat treatment with normalizing at 880°C and tempering at 650°C for 60 hours. I observed that this led to severe surface cracking and hydrogen segregation in gear shafts, as seen in metallographic analysis. By increasing the normalizing temperature to 950°C and extending the tempering time to 100 hours, I aimed to enhance diffusion kinetics. The hydrogen diffusion in steel can be described by Fick’s second law: $$ \frac{\partial C}{\partial t} = D \frac{\partial^2 C}{\partial x^2} $$ where \( C \) is hydrogen concentration, \( t \) is time, \( x \) is distance, and \( D \) is the diffusion coefficient. For 17CrNiMo6 steel, \( D \) depends on temperature as per the Arrhenius equation: $$ D = D_0 \exp\left(-\frac{Q}{RT}\right) $$ with \( D_0 \) as the pre-exponential factor (approximately \( 1.5 \times 10^{-7} \, \text{m}^2/\text{s} \) for hydrogen in ferrite), \( Q \) the activation energy (about 35 kJ/mol), \( R \) the gas constant, and \( T \) the absolute temperature. At 650°C, extending tempering from 60 to 100 hours increased the diffusion distance significantly, calculated as: $$ x \approx \sqrt{Dt} $$ For \( D \approx 2.0 \times 10^{-10} \, \text{m}^2/\text{s} \) at 650°C, \( x \) increased from 6.9 mm to 8.5 mm, allowing hydrogen to escape from deeper regions of the gear shafts. This reduced subsurface hydrogen peaks, as verified by desorption profiles.
Microstructural examination revealed that optimized forging minimized grain boundary segregation and cracking. Table 3 summarizes the key forging parameters and outcomes for gear shaft samples. The improved surface quality and reduced internal stresses were evident in non-destructive testing, with ultrasonic inspection showing a decrease in defect indications from 15% to less than 2% in optimized batches. This underscores the importance of thermal processing in mitigating flake initiation in large section gear shafts.
| Parameter | Original Process | Optimized Process | Effect on Gear Shafts |
|---|---|---|---|
| Normalizing Temperature | 880°C | 950°C | Refined grain size, reduced segregation |
| Tempering Temperature | 650°C | 650°C | Maintained for stress relief |
| Tempering Time | 60 hours | 100 hours | Enhanced hydrogen diffusion, lower H content |
| Surface Cracks | Numerous, severe | Rare, minor | Improved integrity for gear shafts |
| Ultrasonic Defect Rate | 15% | <2% | Reduced flake indication in gear shafts |
Carburizing and subsequent heat treatments are critical for achieving the desired surface properties in gear shafts, but they also introduce hydrogen and residual stresses. In the carburizing stage, conducted at 930°C with isopropanol, I monitored hydrogen uptake using mass spectrometry. The process involves carbon and hydrogen absorption, described by: $$ \text{C}_3\text{H}_7\text{OH} \rightarrow 3\text{C} + 4\text{H}_2 + \text{CO} $$ This releases atomic hydrogen that can diffuse into the steel. To minimize this, I optimized the atmosphere by adding nitrogen and methanol as carriers, reducing the hydrogen partial pressure. Post-carburizing, the gear shafts were quenched in oil from 820°C, leading to martensite formation with high residual stresses. The original tempering involved three cycles at 200°C for 2 hours each, which I modified to include a pre-tempering hold at 180°C for 6 hours, followed by two tempering cycles at 200°C for 55 hours each. This extended treatment aimed to reduce residual austenite and promote hydrogen effusion.
The transformation of retained austenite to martensite during tempering can be modeled using the Koistinen-Marburger equation: $$ f = 1 – \exp[-k(M_s – T)] $$ where \( f \) is the fraction of austenite transformed, \( k \) is a constant (approximately 0.011 for 17CrNiMo6), \( M_s \) is the martensite start temperature (around 350°C), and \( T \) is the tempering temperature. By increasing tempering time and cycles, I achieved a reduction in retained austenite from 15% to below 5%, as measured by X-ray diffraction. This is crucial because retained austenite can decompose under stress, releasing hydrogen and triggering flakes. Additionally, the prolonged tempering facilitated stress relaxation, described by the creep equation: $$ \sigma = \sigma_0 \exp\left(-\frac{t}{\tau}\right) $$ where \( \sigma \) is stress, \( \sigma_0 \) is initial stress, \( t \) is time, and \( \tau \) is the relaxation time constant. For gear shafts, this reduced peak stresses by over 30%, lowering the driving force for crack propagation.
Table 4 compares the heat treatment parameters and outcomes for gear shafts before and after optimization. The data highlights how extended tempering times and additional cycles contributed to improved microstructural stability and reduced flake sensitivity. Hardness measurements confirmed that surface hardness remained within the required range (57-61 HRC), while core hardness stayed at 34-38 HRC, ensuring that gear shafts met performance specifications without compromising on flake resistance.
| Aspect | Original Process | Optimized Process | Impact on Gear Shafts |
|---|---|---|---|
| Quenching Temperature | 820°C | 820°C | Consistent martensite formation |
| Pre-tempering Hold | None | 180°C for 6 hours | Reduced thermal gradients |
| Tempering Cycles | 3 at 200°C | 2 at 200°C (55 h each) | Lower residual austenite |
| Total Tempering Time | 6 hours | 110 hours | Enhanced hydrogen diffusion, stress relief |
| Retained Austenite | 15% | <5% | Improved stability in gear shafts |
| Residual Stress (Surface) | -450 MPa | -300 MPa | Reduced cracking tendency in gear shafts |
To integrate these findings, I developed a comprehensive model for flake prevention in gear shafts, incorporating hydrogen diffusion, stress analysis, and microstructural evolution. The critical hydrogen concentration for flake formation, \( C_{crit} \), can be estimated using: $$ C_{crit} = \frac{\sigma_{th} \sqrt{\pi a}}{K_{IC}} $$ where \( \sigma_{th} \) is the threshold stress, \( a \) is the defect size, and \( K_{IC} \) is the fracture toughness. For 17CrNiMo6 gear shafts, with \( K_{IC} \approx 80 \, \text{MPa}\sqrt{\text{m}} \) and typical inclusion sizes of 50 µm, \( C_{crit} \) is approximately 1.5 ppm. My optimizations reduced hydrogen content below this level, as shown in Table 2. Furthermore, the extended heat treatments lowered \( \sigma_{th} \) by relieving stresses, providing a dual barrier against flakes.
In practice, the optimized processes were applied to full-scale production of gear shafts. Over 50 gear shafts were manufactured using the revised methods, and none exhibited flakes in post-production ultrasonic testing, compared to a historical failure rate of 20%. This demonstrates the effectiveness of the approach. The total processing time increased, but the gains in reliability justify this for critical applications where gear shafts are subjected to high loads and cyclic stresses. For instance, in ball mill drives, the improved gear shafts showed no signs of internal cracking after 10,000 hours of operation, based on field reports.
In conclusion, my experimental investigation highlights that preventing flakes in large section gear shafts made of 17CrNiMo6 steel requires a holistic optimization of manufacturing processes. By extending VD vacuum degassing in smelting, increasing normalizing temperatures and tempering times in forging, and prolonging tempering cycles in heat treatment, I successfully reduced hydrogen content, minimized residual stresses, and stabilized microstructure. These modifications collectively lower the flake sensitivity, ensuring that gear shafts meet stringent quality standards. The use of formulas and tables in this study provides a quantitative framework for replicating these improvements in industrial settings. Future work could explore real-time monitoring of hydrogen during processing or advanced alloy designs to further enhance the performance of gear shafts. For now, this methodology offers a robust solution to a persistent problem, contributing to the durability and safety of heavy machinery components.
Throughout this study, the term “gear shafts” has been emphasized to underscore the focus on this specific component, which is vital for power transmission in numerous industries. The insights gained here are not limited to 17CrNiMo6 steel but can be adapted to other high-strength alloys used for large forgings. By sharing these findings, I hope to advance the manufacturing of reliable gear shafts, reducing failures and promoting efficient industrial operations. The integration of process engineering with materials science, as demonstrated, is key to overcoming challenges like flake formation, ultimately leading to stronger and longer-lasting gear shafts.