
As a researcher specializing in failure analysis of heavy machinery components, I recently investigated a critical cracking incident involving a wind turbine gear shaft. The gear shaft, a central component in the powertrain’s reliability, was manufactured from 18CrNiMo7-6 steel and had undergone a standard carburizing, quenching, and tempering heat treatment process. The failure manifested as a severe longitudinal crack discovered after tempering, leading to the complete fracture of the component. This analysis details the systematic investigation undertaken to determine the root cause of this catastrophic failure in the gear shaft.
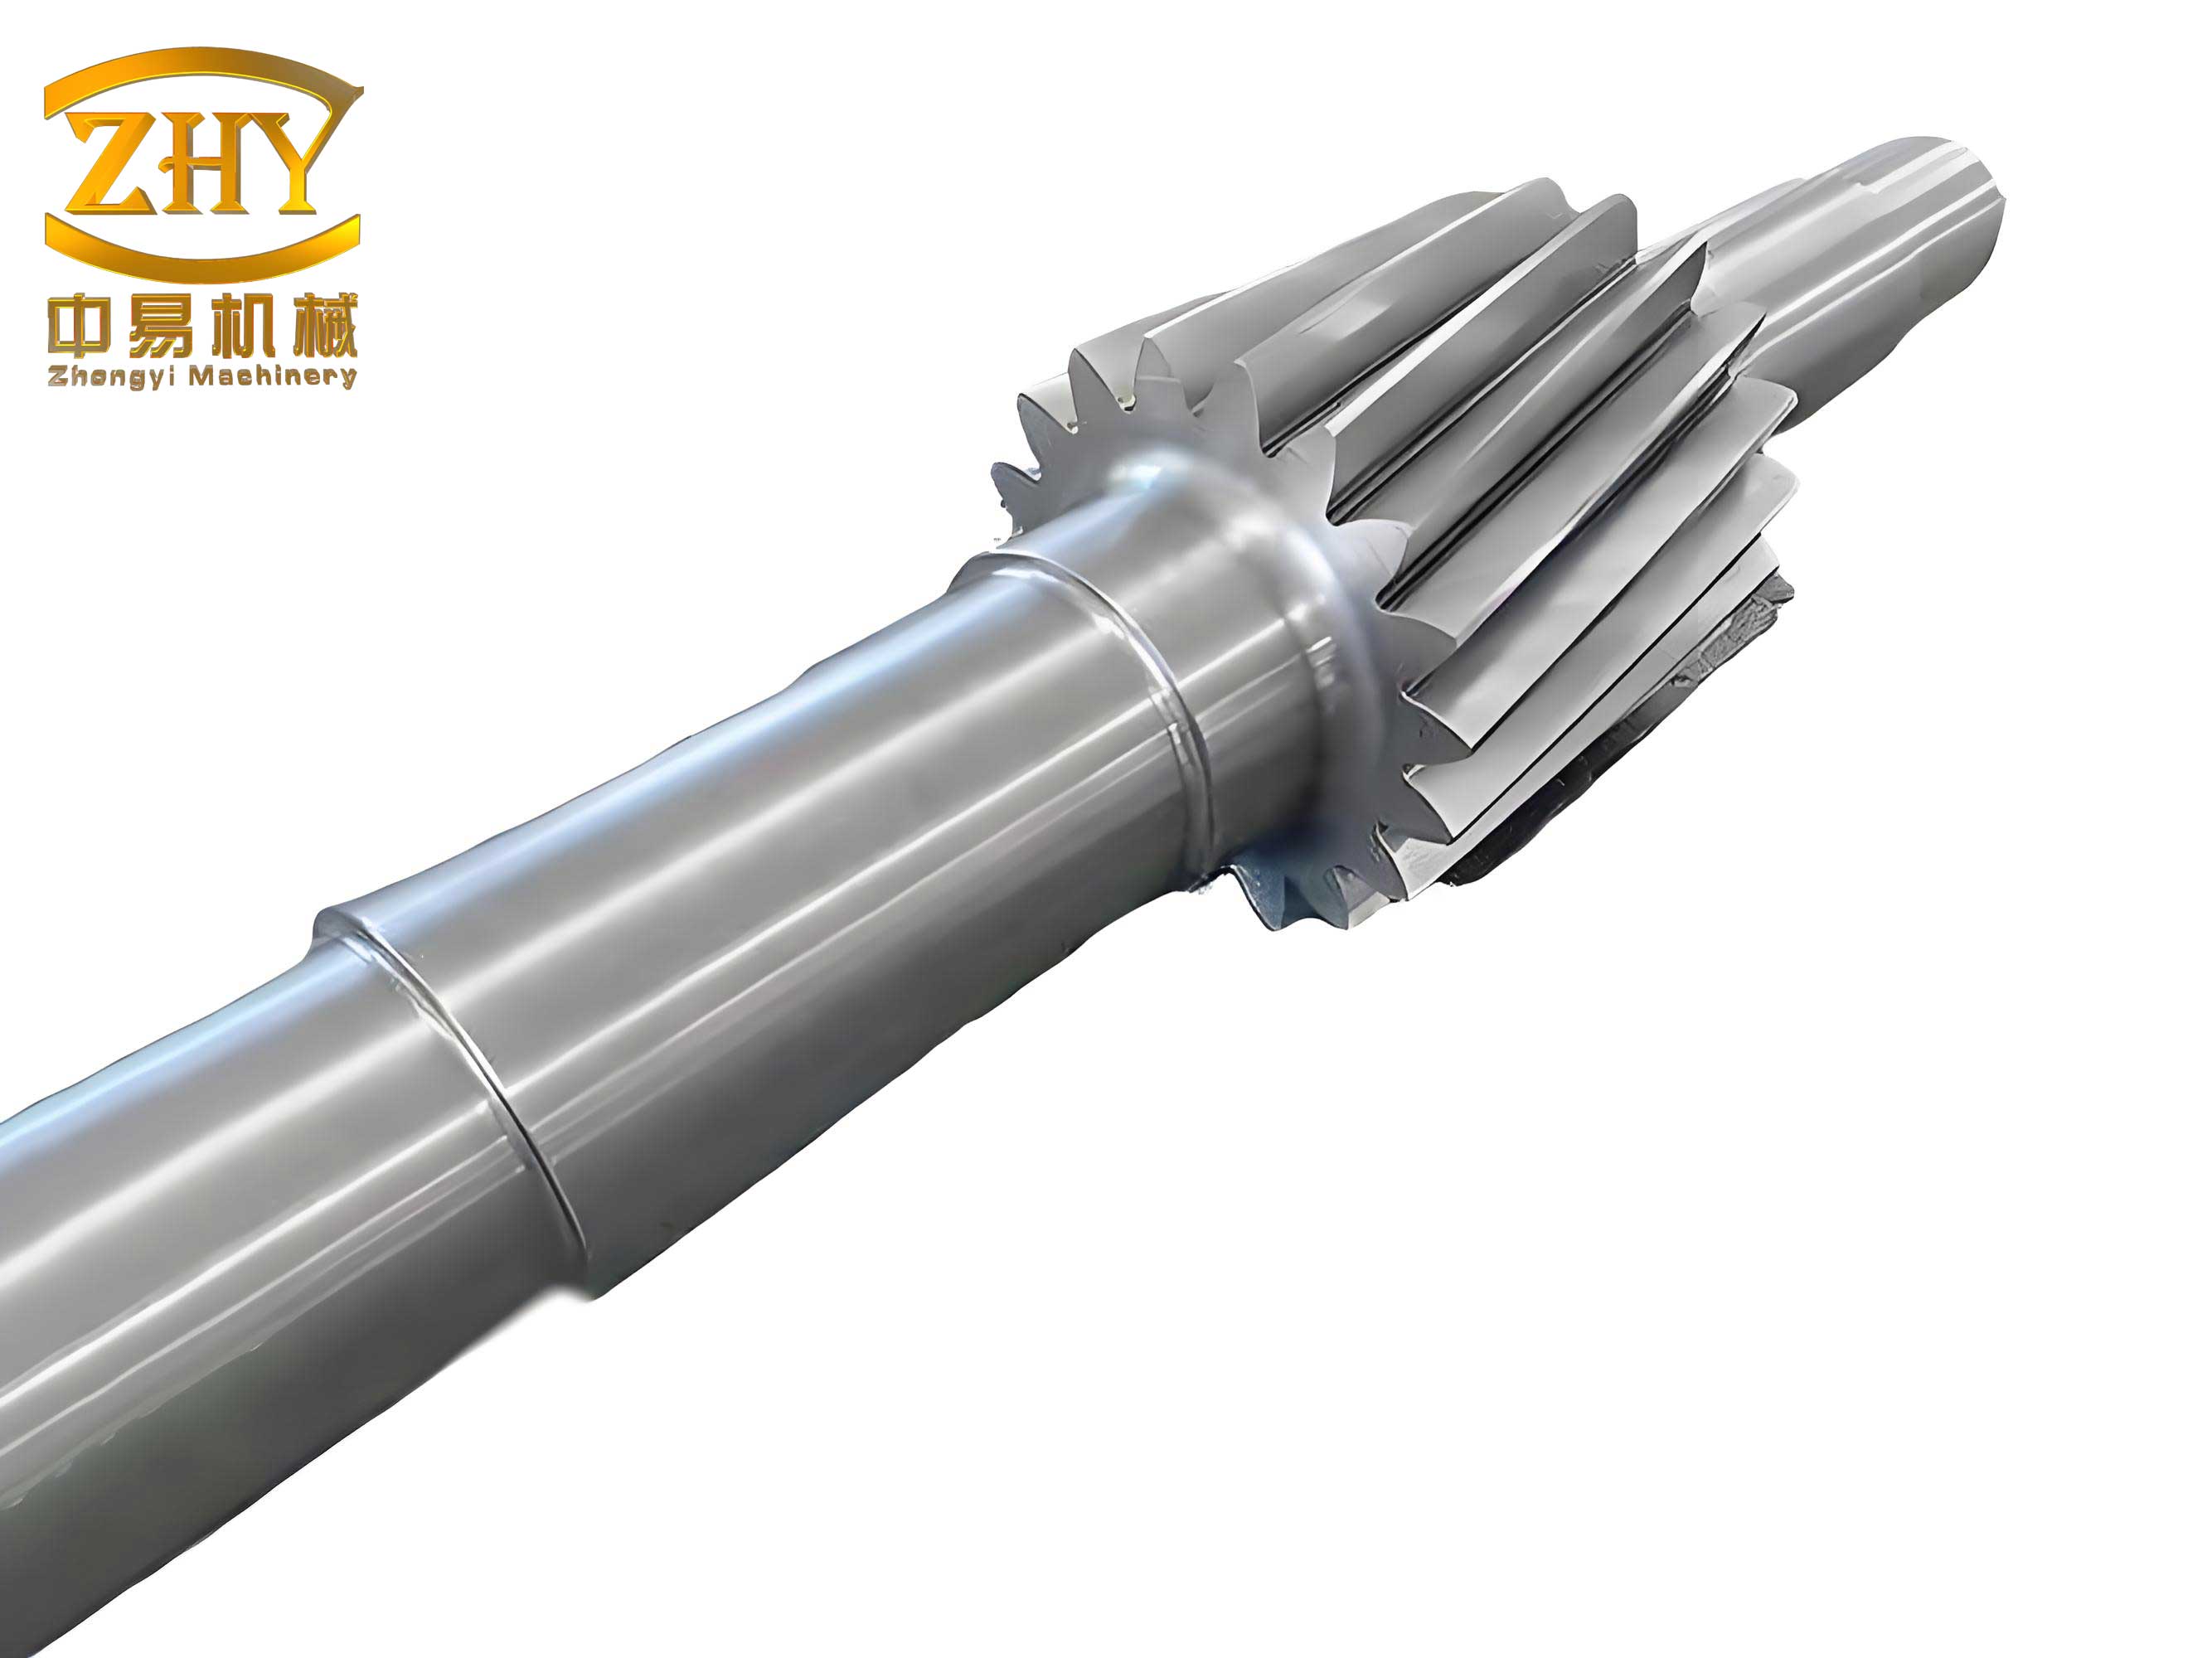
The gear shaft in question was part of a batch of twelve. Following the final tempering operation, the components were stored. Approximately two days later, a distinct longitudinal crack, roughly 1.5 mm wide, was observed on the smooth section of one specific gear shaft, located near the geared segment. The crack exhibited alarming characteristics: it propagated audibly, with occasional sharp cracking sounds, and grew steadily over the following days. Within four days, it had traversed the entire length of the gear shaft, from one end face to the other, and its depth exceeded the central axis. The crack path was primarily axial but showed deviations, becoming stepped when crossing a shaft diameter change, indicating complex stress interactions during propagation.
Macroscopic Examination and Fractography
The failed gear shaft was sectioned along its longitudinal axis for detailed examination. The fracture surface revealed classic brittle fracture features. Macroscopically, radial ridges were observed converging to a singular origin point located approximately 220 mm from the gear end and about 12 mm beneath the surface of the shaft body. At this origin, a distinct, grayish-white, elongated strip was visible, aligned with the shaft’s axis. This strip, measuring approximately 5.50 mm in length and 0.40 mm in width, was unequivocally identified as the crack initiation site, as all surrounding fracture ridges emanated from it. The fracture morphology varied from a relatively smooth region near the surface to a rougher zone around the mid-radius, finally transitioning to a smoother appearance again near the core, suggesting changes in microstructure and stress state through the cross-section of the gear shaft.
Comprehensive Material and Property Verification
To rule out generalized material or heat treatment deficiencies, a battery of tests was conducted on samples extracted from the crack initiation region of the affected gear shaft.
Chemical Composition and Cleanliness
The chemical composition of the gear shaft material was verified and found to be fully compliant with the specification for 18CrNiMo7-6 steel, as shown in Table 1. Furthermore, gas content analysis (Table 2) and standard metallographic assessment of non-metallic inclusions (Table 3) also met all required standards. Macro-etching tests revealed no evidence of gross segregation or pipe.
| Element | C | Si | Mn | P | S | Cr | Mo | Ni | Al | Fe |
|---|---|---|---|---|---|---|---|---|---|---|
| Measured | 0.20 | 0.26 | 0.78 | 0.012 | 0.015 | 1.73 | 0.30 | 1.46 | 0.03 | Bal. |
| Specification | 0.15-0.21 | ≤0.40 | 0.50-0.90 | ≤0.025 | ≤0.025 | 1.50-1.80 | 0.28-0.35 | 1.40-1.70 | ≤0.05 | Bal. |
| Gas | Oxygen (O2) | Nitrogen (N2) | Hydrogen (H2) |
|---|---|---|---|
| Measured | 12 | 100 | 2 |
| Specification | ≤25 | 50-150 | ≤2.5 |
| Type | A (Thick) | A (Thin) | B (Thick) | B (Thin) | C (Thick) | C (Thin) | D (Thick) | D (Thin) |
|---|---|---|---|---|---|---|---|---|
| Measured | 0 | 0.5 | 0 | 0.5 | 0 | 0 | 0 | 1.0 |
Heat Treatment Quality Assessment
The integrity of the carburizing and hardening process on the gear shaft was evaluated. Microstructural examination of the case revealed a fine, acicular martensite with an acceptable level of retained austenite (≈12%). The core microstructure consisted of tempered martensite. No anomalous phases, such as excessive non-martensitic products or grain boundary networks, were observed. The surface hardness and case depth were measured at various locations, including near the crack origin and on the gear teeth, confirming the heat treatment was performed correctly and uniformly (Table 4).
| Location on Gear Shaft | Surface Hardness (HRC) | Case Depth (550 HV1), mm |
|---|---|---|
| Near Crack Origin | 59.7 | 1.85 |
| Gear Tooth Tip | 61.2 | 2.55 |
| Gear Tooth Pitch | 60.3 | 2.16 |
| Gear Tooth Root | 59.9 | 1.75 |
| Specification | 58 – 62 | 1.52 – 2.80 |
Mechanical Properties
Tensile and impact specimens were taken from the region near the crack origin at the mid-radius position of the gear shaft body. The results, summarized in Table 5, demonstrate that the base material’s strength, ductility, and toughness were all within the specified limits, ruling out a general degradation of mechanical properties as the cause of failure for this gear shaft.
| Property | Ultimate Tensile Strength (MPa) | Elongation (%) | Reduction of Area (%) | Charpy Impact Energy (J) |
|---|---|---|---|---|
| Measured Value | 1230 | 15.1 | 63.7 | 122 |
| Specification | ≥1080 | ≥11 | ≥35 | ≥25 |
Microscopic Analysis of the Crack Origin
The investigation then focused intensely on the strip-like feature at the crack origin. Scanning Electron Microscopy (SEM) examination revealed that this strip was not a metallic feature but an agglomeration of numerous discrete particles. Energy Dispersive Spectroscopy (EDS) analysis was pivotal. Area mapping across the strip and the surrounding matrix showed a significant enrichment in Aluminum (Al) and Oxygen (O) within the strip. Point analysis on individual particles confirmed they were primarily composed of Al and O, identifying the strip as a large, exogenous aluminum oxide (Al2O3) slag inclusion.
The fracture morphology around this inclusion was highly revealing. Immediately adjacent to the oxide cluster, the fracture mode was predominantly intergranular (IG). The grain facets exhibited subtle, fine tear ridges, a morphology often associated with hydrogen-assisted cracking. As the distance from the origin increased, the fracture mode transitioned from quasi-cleavage to a ductile dimple morphology in the core region. The carburized case, however, maintained an intergranular fracture character, consistent with its high hardness and susceptibility to environmentally assisted cracking.
Discussion: Mechanism of Failure in the Gear Shaft
The convergence of evidence points to a specific failure mechanism known as hydrogen-induced delayed cracking. The sequence of events leading to the fracture of this gear shaft can be reconstructed as follows:
1. The Critical Role of the Oxide Inclusion
The large aluminum oxide slag inclusion, situated approximately 12 mm beneath the surface, acted as a potent stress concentrator and a hydrogen trap. Its size and morphology created a severe local discontinuity in the steel matrix of the gear shaft. After quenching, the region surrounding this defect experiences a triaxial tensile stress state, significantly elevating the local stress intensity. The stress intensity factor (\( K \)) at the tip of such a flaw can be conceptually represented, even for an embedded irregularity, by relations considering an effective crack size (\( a \)):
$$ K \approx \sigma \sqrt{\pi a} \cdot Y $$
where \( \sigma \) is the local residual stress and \( Y \) is a geometric factor. The presence of the inclusion dramatically reduces the critical stress or critical flaw size required for crack initiation in the gear shaft.
2. Residual Stress Profile in the Carburized Gear Shaft
The carburizing and quenching process induces a characteristic residual stress profile. The surface region, transformed to high-carbon martensite, is in a state of compressive residual stress, which is beneficial for fatigue resistance. However, beneath this compressive layer, in the transition zone where the carbon gradient and transformation sequences differ, a peak tensile residual stress develops. This tensile stress maximum typically occurs at a depth corresponding to the transition from case to core properties. The crack origin in this gear shaft was located precisely within this subsurface region of maximum residual tensile stress, providing the macroscopic driving force for crack opening.
3. Hydrogen Embrittlement and Delayed Cracking
The delayed nature of the crack’s appearance—occurring days after the final tempering—is a hallmark of hydrogen-assisted failure. Hydrogen atoms (\( H \)) can be introduced during steelmaking or subsequent processing (like acid cleaning or plating, though not directly indicated here, could be from the atmosphere during heating). These diffusible hydrogen atoms migrate under the influence of stress gradients, accumulating at regions of high triaxial tension, such as the interface of the hard oxide inclusion and the steel matrix in the gear shaft.
The hydrogen accumulation lowers the cohesive strength of the metal lattice, particularly along prior austenite grain boundaries. The pressure build-up from hydrogen recombination (\( 2H \rightarrow H_2 \)) within micro-voids adds to the local stress. The combined effect can be described by models where the threshold stress intensity for crack propagation (\( K_{th} \)) is reduced in the presence of hydrogen:
$$ K_{th}(H) = K_{th}(0) – \alpha \cdot C_H $$
where \( K_{th}(0) \) is the threshold in hydrogen-free conditions, \( C_H \) is the local hydrogen concentration, and \( \alpha \) is a material constant. When the local condition, defined by the residual stress (defining \( K \)) and the trapped hydrogen concentration (\( C_H \)), satisfies \( K \geq K_{th}(H) \), crack initiation occurs. The intergranular fracture with micro-tear ridges observed at the origin is the classic microscopic signature of this process. Once a micro-crack initiates at the inclusion, it propagates under the sustained residual stress field, leading to the observed macroscopic failure of the gear shaft.
This mechanism explains why only one gear shaft in the batch failed: the catastrophic flaw was a rare, localized material defect—the large oxide inclusion—acting in concert with the ever-present factors of heat-treatment residual stress and trace amounts of hydrogen.
Conclusion and Recommendations
The longitudinal cracking of the wind turbine gear shaft was determined to be a hydrogen-induced delayed fracture, with the primary root cause being the presence of an abnormally large exogenous aluminum oxide (Al2O3) slag inclusion in the subsurface region of high residual tensile stress. This inclusion served as both a potent stress concentrator and a hydrogen trap. Under the combined action of quenching residual stresses and locally trapped hydrogen, intergranular cracking initiated at the inclusion-matrix interface and propagated, resulting in complete fracture of the gear shaft.
To prevent recurrence of such failures in critical components like gear shafts, the following measures are recommended:
- Enhanced Raw Material Inspection: Standard microscopic inclusion ratings may not detect isolated, macroscopic slag clusters. Implementing rigorous ultrasonic testing (UT) of forged or rolled blanks for gear shafts is essential to identify and reject material containing large, non-metallic inclusions before costly machining and heat treatment.
- Control of Hydrogen Sources: Scrutinize all processes (e.g., cleaning, phosphating) prior to heat treatment that could introduce hydrogen into the steel of the gear shaft. Ensure furnaces are maintained to avoid water vapor contamination.
- Optimized Heat Treatment Practice: While tempering was performed, ensuring the absolute minimum delay between quenching and tempering for high-strength gear shafts is critical. This allows hydrogen to diffuse out and reduces the residual stress level before significant hydrogen segregation can occur at critical sites.
This case underscores that the reliability of high-performance components like wind turbine gear shafts depends not only on proper heat treatment and design but fundamentally on the intrinsic cleanliness and homogeneity of the base material. A single, severe material defect can negate all other quality controls, leading to sudden and catastrophic failure.