
In the pursuit of quieter automotive transmissions, controlling gear meshing noise has become a paramount objective. As an engineer deeply involved in gear manufacturing, I have focused on the critical process of gear shaving and its potential to significantly influence acoustic performance. The primary challenge lies in the inherent dynamics of gear pairing. During operation, the contact between teeth is not constant; it alternates between single and double tooth contact due to the contact ratio (ε), which typically lies between 1 and 2. This alternating pattern, combined with variable tooth stiffness and manufacturing imperfections, creates cyclical impacts and vibrations that manifest as objectionable noise.
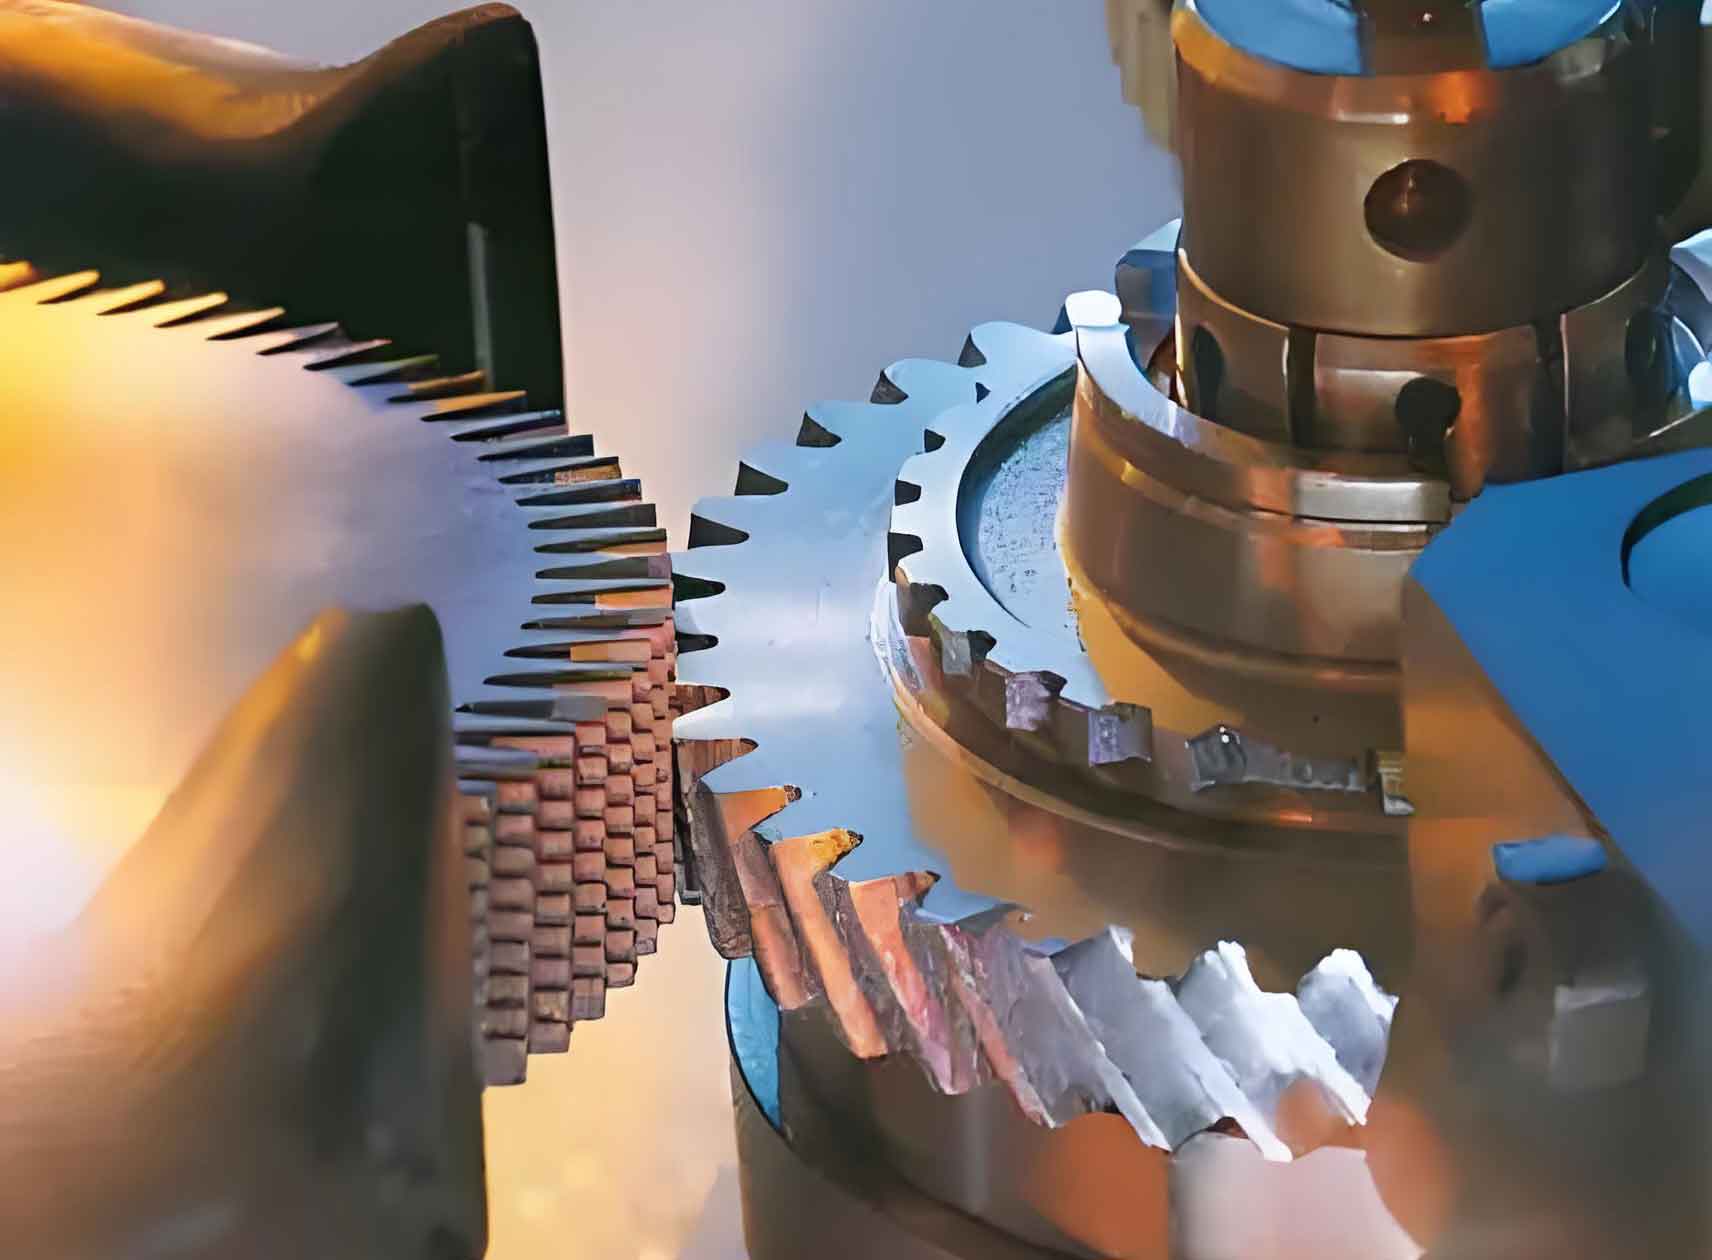
The conventional gear shaving process, while effective for finishing, often introduces a specific form error known as “mid-relief” or “shaving concavity.” This is a direct consequence of the variable cutting forces during the gear shaving cycle. In the single-pair contact zone near the pitch line, the cutting force per tooth is higher, removing more material and creating a slight depression on the gear flank. This deviation from the ideal involute profile exacerbates meshing impacts. Therefore, the solution is not merely to shave, but to strategically modify the process. By employing a form-ground gear shaving cutter, we can pre-correct the gear tooth profile. This proactive correction, or “working flank modification,” aims to achieve a designed tooth form that compensates for deflection under load and minimizes entry/exit impacts, ultimately yielding a quieter gearset.
Foundational Theory of Contact and Modification
The design of a modified tooth profile, often referred to as a “tip-and-root relief” or “crowned” profile, is essential. An ideal modified profile consists of distinct zones: a tip relief zone ($l_{a}$), a root relief zone ($l_{f}$), a central theoretical involute zone ($l_{i}$), and chamfers. The relief amounts, typically in the range of 0.015-0.02 mm, prevent edge contacts. The goal of gear shaving with a form-ground cutter is to impart this optimized geometry onto the workpiece gear.
To achieve this via gear shaving, we must first mathematically locate the problematic areas on the gear flank induced by the standard process. The core of the calculation involves determining the boundaries of the single-pair contact region during the meshing of the shaving cutter and the work gear.
Mathematical Modeling for Cutter Form Design
The following analysis outlines the step-by-step procedure for calculating the necessary corrections on the gear shaving cutter. We define key parameters for the work gear (subscript ‘1’ or ‘g’) and the shaving cutter (subscript ‘0’ or ‘c’).
1. Basic Gear and Mesh Parameters
Given standard gear data (module $m_n$, number of teeth $z$, helix angle $\beta$, pressure angle $\alpha_n$, etc.), we calculate derived geometry.
| Parameter | Symbol | Formula/Description |
|---|---|---|
| Normal Module | $m_n$ | Given (e.g., 3.5 mm) |
| Transverse Module | $m_t$ | $m_t = m_n / \cos\beta$ |
| Transverse Pressure Angle | $\alpha_t$ | $\alpha_t = \arctan(\tan\alpha_n / \cos\beta)$ |
| Base Circle Diameter (Gear) | $d_{b1}$ | $d_{b1} = d_1 \cdot \cos\alpha_t$ where $d_1 = m_t \cdot z_1$ |
| Base Circle Diameter (Cutter) | $d_{b0}$ | $d_{b0} = d_0 \cdot \cos\alpha_{t0}$ |
| Base Helix Angle | $\beta_b$ | $\sin\beta_b = \sin\beta \cdot \cos\alpha_n$ |
| Center Distance (Cutter-Gear) | $a$ | Given or calculated from sum of pitch radii. |
| Working Transverse Pressure Angle | $\alpha_{wt}$ | $\cos\alpha_{wt} = (d_{b1} + d_{b0}) / (2a)$ |
2. Determining the Single-Pair Contact Zone
The length of the path of contact $L$ for the shaving cutter-gear pair is:
$$L = \frac{1}{2}\left( \sqrt{d_{a1}^2 – d_{b1}^2} + \sqrt{d_{a0}^2 – d_{b0}^2} \right) – a \cdot \sin\alpha_{wt}$$
where $d_a$ denotes the tip diameter.
The transverse base pitch is $p_{bt} = \pi m_t \cos\alpha_t$. The theoretical contact ratio is $\varepsilon = L / p_{bt}$. Since $\varepsilon < 2$, there is a single-pair contact region of length $L_{sp}$ within the total path:
$$L_{sp} = L – p_{bt}$$
This region is symmetrically located about the pitch point. The boundaries of this region on the work gear flank are defined by their radii of curvature, $\rho_1$ and $\rho_2$:
$$\rho_1 = \frac{L_{sp}}{2} \cdot \cos\beta_b$$
$$\rho_2 = \rho_1 + p_{bt} \cdot \cos\alpha_t \cdot \cos\beta_b = \frac{L + p_{bt}}{2} \cdot \cos\beta_b$$
These curvature radii are measured from the gear’s base circle tangent point.
3. Mapping the Zone onto the Shaving Cutter
The corresponding points on the shaving cutter flank that generate the single-pair contact zone on the gear are found via the constant length of the line of action. The radii of curvature on the cutter, $\rho_{1c}$ and $\rho_{2c}$, are:
$$\rho_{1c} = (L – \rho_1 / \cos\beta_b) \cdot \cos\beta_{b0}$$
$$\rho_{2c} = (L – \rho_2 / \cos\beta_b) \cdot \cos\beta_{b0}$$
These can be converted to actual diameters on the shaving cutter where modification must begin and end:
$$D_{1c} = 2 \cdot \sqrt{\rho_{1c}^2 + (d_{b0}/2)^2}$$
$$D_{2c} = 2 \cdot \sqrt{\rho_{2c}^2 + (d_{b0}/2)^2}$$
Furthermore, for grinding the cutter on a machine like the Y7125, we need the corresponding roll angles or the projection onto the cutter’s transverse plane. The transverse pressure angle at a point with diameter $D_{c}$ on the cutter is:
$$\alpha_{tc} = \arccos(d_{b0} / D_{c})$$
The related roll angle $\theta_c$ (for indexing) is:
$$\theta_c = \frac{z_0}{\pi} \cdot \left( \tan\alpha_{tc} – \tan\alpha_{t0} + \text{inv}\,\alpha_{t0} – \text{inv}\,\alpha_{tc} \right)$$
4. Calculating the Grinding Template Profile
The final step is to translate the required modification on the cutter flank into a profile for the grinding machine template. The grinding is performed at a specific machine setting angle $\alpha_m$, which is the transverse pressure angle at the cutter’s pitch line during the grinding setup, often equal to $\alpha_{t0c}’$, the working transverse pressure angle between the imaginary grinding rack and the cutter.
The linear displacement $x$ on the template corresponding to a change in radius of curvature $\Delta \rho_c$ on the cutter is:
$$x = \Delta \rho_c \cdot \tan\alpha_m$$
Therefore, the length on the template representing the single-pair contact zone ($\rho_{1c}$ to $\rho_{2c}$) is:
$$l_{sp\text{ template}} = (\rho_{1c} – \rho_{2c}) \cdot \tan\alpha_m$$
The total active profile length on the template, from the start of modification near the tip to the end near the root, is:
$$l_{total\text{ template}} = (\rho_{c\text{ max}} – \rho_{c\text{ min}}) \cdot \tan\alpha_m$$
where $\rho_{c\text{ max}}$ and $\rho_{c\text{ min}}$ are the maximum and minimum radii of curvature on the cutter flank to be modified.
A practical grinding template is not a simple straight line but a profiled curve. A common and effective design combines three sections, summarized in the table below:
| Template Section | Purpose | Profile Shape | Effect on Cutter/Gear |
|---|---|---|---|
| Tip Region | To generate tip relief on the finished gear. | Gradual drop-off from the nominal involute line. | Prevents gear tip contact, reducing entry impact. |
| Central Region (Pitch Zone) | To counteract the shaving concavity. | Protrusion or “bump” relative to the nominal line, centered on the single-pair contact zone. | Adds material to the cutter in the zone where it normally cuts too deep, resulting in a straighter gear flank. |
| Root Region | To generate root relief on the finished gear. | Gradual drop-off from the nominal involute line. | Prevents gear root contact, reducing exit impact. |
Comprehensive Calculation Example
To solidify the theory, let’s walk through a summarized calculation for a specific work gear. The following table lists key input parameters and intermediate results, following the mathematical sequence described.
| Step | Parameter | Symbol | Value / Calculation | Result |
|---|---|---|---|---|
| 1 | Work Gear Data | $m_n, z_1, \beta_1, \alpha_n$ | $3.5, 42, 28^\circ 11’52”, 20^\circ$ | – |
| 2 | Shaving Cutter Data | $z_0, \beta_0$ | $61, 16^\circ 11’52″$ | – |
| 3 | Transverse Pressure Angle (Gear) | $\alpha_{t1}$ | $\arctan(\tan20^\circ / \cos28.19778^\circ)$ | $22.43976^\circ$ |
| 4 | Base Helix Angle (Gear) | $\beta_{b1}$ | $\arcsin(\sin28.19778^\circ \cdot \cos20^\circ)$ | $26.36068^\circ$ |
| 5 | Path of Contact Length | $L$ | Per formula using tip diameters | $80.07323$ mm |
| 6 | Single-Pair Contact Zone on Gear | $\rho_1, \rho_2$ | $\rho_1 = \frac{L-p_{bt}}{2}\cos\beta_b$, $\rho_2=\rho_1+p_{bt}\cos\alpha_t\cos\beta_b$ | $28.64490$ mm, $30.71649$ mm |
| 7 | Corresponding Zone on Cutter | $\rho_{1c}, \rho_{2c}$ | $(L – \rho_{1,2}/\cos\beta_{b1})\cos\beta_{b0}$ | $47.00100$ mm, $44.76985$ mm |
| 8 | Cutter Diameters at Zone Boundaries | $D_{1c}, D_{2c}$ | $2\sqrt{\rho_{c}^2 + (d_{b0}/2)^2}$ | $228.1554$ mm, $220.3504$ mm |
| 9 | Grinding Setting Angle | $\alpha_m$ | $\arccos(d_{b0} / D_{pitch,c})$ | $19^\circ 10’15″$ |
| 10 | Template Length for SPC Zone | $l_{sp}$ | $(\rho_{1c} – \rho_{2c}) \cdot \tan\alpha_m$ | $0.7757$ mm |
| 11 | Total Template Modification Length | $l_{total}$ | $(\rho_{c\text{ max}} – \rho_{c\text{ min}}) \cdot \tan\alpha_m$ | $6.2576$ mm |
These calculated values directly instruct the manufacture of the grinding template. The protrusion height for the central “bump” is determined based on the desired compensation for the shaving concavity, typically derived from experience or measured data from unmodified gear shaving trials.
Benefits and Implementation of Form-Ground Shaving
The strategic application of form-ground gear shaving cutters delivers multiple benefits that directly address noise and quality concerns.
- Targeted Noise Reduction: By precisely controlling the contact pattern and minimizing edge contacts and transmission error, gear meshing noise can be reduced by several decibels.
- Compensation for Process Defects: It directly counteracts the mid-relief phenomenon inherent to standard gear shaving, leading to a straighter, more optimal flank geometry.
- Improved Load Distribution: The designed tip and root relief allow for slight misalignments and deflections under load without concentrating stress at the edges, improving gear life.
- Process Flexibility: The modification profile on the cutter can be customized for specific gear applications, load conditions, and noise targets, making gear shaving a highly adaptable finishing process.
In conclusion, moving from standard to precision form-ground gear shaving represents a significant technological upgrade in gear finishing. It transforms gear shaving from a mere stock-removal operation into a controlled, corrective process for active noise and performance optimization. The mathematical framework for designing the modified cutter, centered on analyzing the shaving mesh to locate the single-pair contact zone, provides a rigorous engineering basis for this improvement. Successful implementation requires close collaboration between design, manufacturing engineering, and metrology to translate calculated template profiles into verified, quieter gears. This approach underscores the fact that in modern gear manufacturing, the finish machining process, particularly gear shaving, is not just about achieving a smooth surface but about sculpting a precise mechanical interface for optimal acoustic and dynamic performance.