
I treat the precision forging of straight bevel gears as a coupled problem of tooth-cavity design, material-flow control, and die-life management. In vehicle drivelines, machine tools, marine transmissions, and industrial reducers, straight bevel gears are used where motion must be transferred between intersecting shafts. Their teeth are the functional core of the part, and the forging quality of those teeth determines noise, contact fatigue, bending strength, and dimensional consistency. Conventional gear cutting removes material, interrupts the grain flow, and can leave the tooth root less favorable for high bending loads. Precision forging of straight bevel gears, by contrast, can produce a near-net tooth form with continuous grain flow and reduced material waste. However, a single final forging step is rarely sufficient for straight bevel gears with demanding tooth geometry. The tooth cavity is deep, the corner regions at the tooth tip are difficult to fill, and the material must flow simultaneously in radial, axial, and tangential directions. Therefore, I use a two-step precision forging route: pre-forging followed by final forging. The pre-forging shape, especially the pre-forging tooth profile, controls how the material enters the final tooth cavity. A well-designed pre-forging tooth for straight bevel gears can improve fill, reduce folding and cracking, lower forming load, and extend die life. This is the reason I focus on a trapezoidal nonstandard pre-forging tooth and validate it with DEFORM-3D numerical simulation.
| Aspect | Gear cutting for straight bevel gears | Precision forging for straight bevel gears | Manufacturing consequence |
|---|---|---|---|
| Material yield | Low to moderate; chips are removed | High; near-net tooth form | Less waste and lower input mass |
| Grain flow | Interrupted at tooth surfaces | Continuous and favorable around tooth roots | Higher bending fatigue resistance |
| Tooth accuracy | High after finishing | Requires controlled pre-forging and final forging | Pre-forging design is critical |
| Tooling cost | Moderate for cutting tools | High for forging dies | Simpler pre-forging teeth reduce cost |
| Production rate | Moderate | High for established forging lines | Suited to mass production |
| Tooth-corner filling | Not a material-flow issue | Major issue in final forging | Pre-forging must create shunt space |
| Folding risk | Low | Possible if preform is poorly designed | Nonstandard pre-forging teeth help |
| Die life | Depends on cutting conditions | Depends on load, temperature, and flow | Balanced pre-forging reduces load |
I structure the process route for straight bevel gears so that each step prepares the material for the next without introducing avoidable defects. The central divided flow method is the basis of my approach. In this method, a punch with a central boss creates a divided-flow zone at the end face of the pre-forging billet. This zone acts as a temporary reservoir and as a flow guide. During pre-forging, the boss forces material outward toward the tooth cavity while the divided-flow zone controls the backpressure. During final forging, the remaining cavity from the pre-forging stage allows material to continue filling the tooth form rather than becoming trapped or folded. For straight bevel gears, this is especially useful because the tooth height changes along the cone, and the small end and large end do not fill at the same instant. The process route I use is summarized in the following table.
| Step | Operation | Purpose for straight bevel gears | Key control variables |
|---|---|---|---|
| 1 | Precision blanking | Establish accurate billet mass and volume | Mass tolerance, cut quality, end-face squareness |
| 2 | Turning or grinding of outer surface | Remove surface defects and scale | Diameter, surface roughness, defect depth |
| 3 | Controlled or low-oxidation heating | Bring billet to forging temperature with minimal decarburization | Temperature, time, atmosphere |
| 4 | Pre-forging | Create divided-flow zone and trapezoidal tooth preform | Boss geometry, tooth height, draft, fillet radius |
| 5 | Final forging | Fill the standard involute tooth cavity | Flash control, die temperature, press speed |
| 6 | Cold trimming | Remove flash and define outer contour | Trim clearance, tool alignment |
| 7 | Heat treatment | Develop required core and surface properties | Austenitizing, quench, tempering |
| 8 | Subsequent machining | Finish bores, faces, and any functional surfaces | Datum selection, stock allowance |
I describe the central divided flow method mathematically through volume conservation and flow resistance. If I denote the final tooth cavity volume by \(V_f\), the pre-forging volume by \(V_p\), the flash volume by \(V_{fl}\), the divided-flow reservoir volume by \(V_s\), and unavoidable loss by \(V_l\), then the design must satisfy
$$V_f + V_{fl} + V_s + V_l = V_p + V_{ad},$$
where \(V_{ad}\) is any additional volume intentionally added to the preform. In practice, I do not want \(V_s\) to be so large that final forging becomes a simple upsetting operation with excessive flash. I also do not want \(V_s\) to be so small that the tooth tips and root corners starve for material. For straight bevel gears, the optimal divided-flow volume is a function of cone angle, tooth height, face width, and friction. I express the local fill condition as
$$\eta_f = \frac{V_{filled}}{V_{cavity}},$$
where \(\eta_f\) is the fill ratio of a local tooth region. A value of \(\eta_f = 1\) means complete filling. In my design target, the tooth tip corner and root fillet of straight bevel gears should both reach \(\eta_f \ge 0.98\) before the press load rises excessively. The divided-flow method helps because it changes the effective flow resistance:
$$R_{eff} = R_{tooth} + R_{flash} + R_{shunt},$$
where \(R_{tooth}\) is the resistance of the tooth cavity, \(R_{flash}\) is the resistance of the flash gap, and \(R_{shunt}\) is the resistance of the shunt or divided-flow zone. A well-designed pre-forging tooth reduces \(R_{tooth}\) by replacing part of the final tooth volume with a simpler intermediate shape, while the shunt volume controls \(R_{shunt}\) so that material can still move into difficult corners.
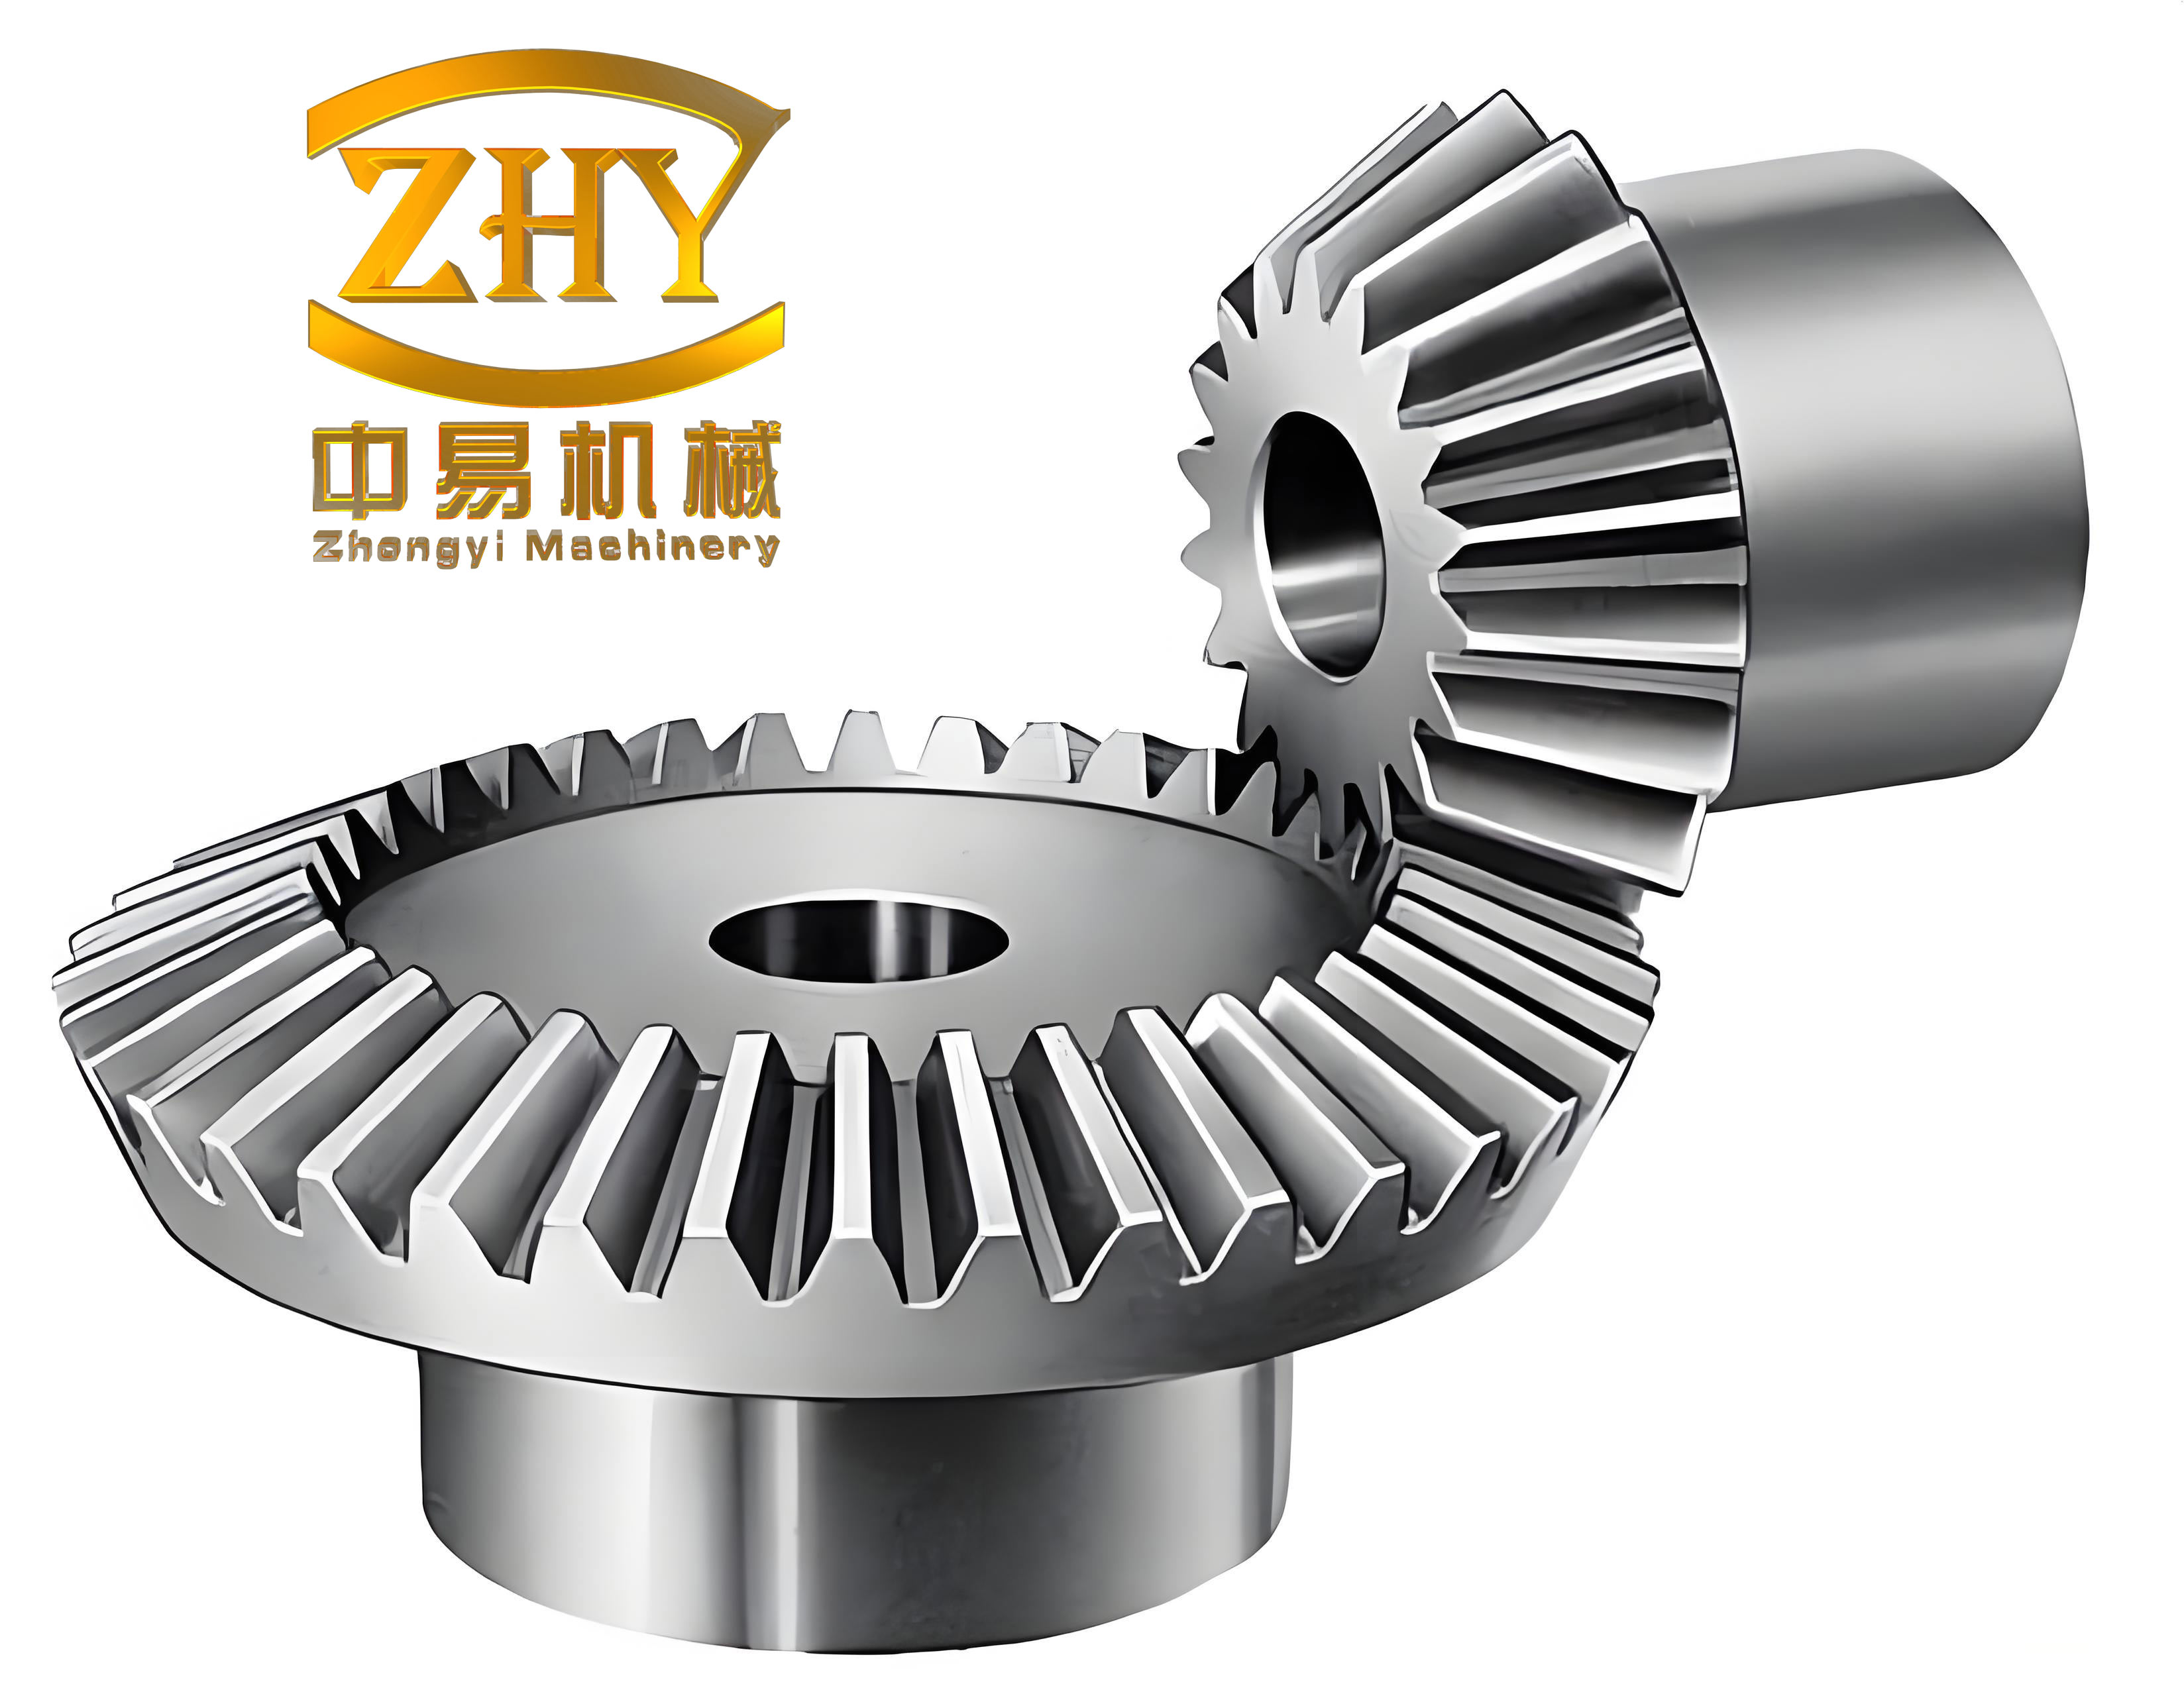
The representative geometry of the straight bevel gears I study has several characteristic dimensions that influence pre-forging design. The outer diameter, inner diameters, face width, cone angles, and tooth height all change the volume distribution along the tooth. I use these geometric features to determine where the pre-forging tooth must be lower, where it must be wider, and where the divided-flow boss should be placed. The image below shows a representative straight bevel gear form that I use as the geometric reference for the flow analysis.
When I compare pre-forging tooth concepts for straight bevel gears, I consider four families: standard involute teeth, standard involute teeth with uniform offset, nonstandard teeth with increased mid-face finishing allowance, and trapezoidal nonstandard teeth. The standard involute pre-forging tooth is attractive because it is close to the final tooth shape. The final forging deformation is therefore small, and the tooth surfaces do not have to move far. However, the pre-forging die cavity is almost as complex as the final die cavity. More importantly, if the pre-forging tooth height is larger than the final tooth height, final forging does not upset the entire face width at once. The small end and large end deform at different times, which can produce folding on the tooth surface and can push too much material toward the flash land. That behavior is especially undesirable for straight bevel gears because the large end is often the last region to fill, and a lack of material there produces an incomplete tooth.
A uniform offset standard tooth is another option. I can shift the tooth flank outward by a finishing allowance and shift the root inward to preserve volume. This reduces the final machining or finishing stock, but the final forging simulation often shows folding near the tooth root. The fold appears because the root region is overconstrained while the flank is still moving. If I reduce the finishing allowance, the fold becomes less severe, but the pre-forging tooth becomes closer to the final tooth, which increases the risk of incomplete filling in the tip corners. A nonstandard tooth with a larger mid-face allowance can avoid some folding because the middle of the tooth face provides a local reservoir. The final forging flow then proceeds from the mid-face toward the tip and root. This is an improvement, but the die cavity is still complex and relatively expensive to manufacture for straight bevel gears.
I therefore propose a trapezoidal nonstandard pre-forging tooth. The first version I considered is a full-height trapezoidal tooth. It is geometrically simple, but the pre-forging die slot becomes narrow and deep. During pre-forging, metal must flow into a deep trapezoidal slot, and the slot itself can cause incomplete filling or excessive load. A full-height trapezoidal tooth also removes too little of the final tooth volume, so final forging still has to move a large amount of material in the radial direction. For straight bevel gears, this is inefficient because the tooth height varies along the face width.
I then adopt a non-full-height trapezoidal tooth. Its height is slightly greater than one-half of the final tooth height. This choice creates a favorable compromise. The pre-forging cavity is shallow enough to fill easily, but the pre-forging tooth still provides a controlled volume of material near the final tooth position. The trapezoidal flanks are simple to machine and simple to model. The top of the trapezoid is not the final tooth tip. Instead, it leaves a definite gap between the pre-forging tooth and the final tooth cavity. That gap becomes a shunt space during final forging. Because the divided-flow boss also creates a central reservoir, the final forging of straight bevel gears has two complementary shunt mechanisms: one at the center of the billet end face and one along the tooth flanks and tooth tips.
| Pre-forging tooth concept for straight bevel gears | Geometric character | Advantages | Problems | My assessment |
|---|---|---|---|---|
| Standard involute | Same involute family as final tooth | Small final deformation; close to final shape | Complex die; possible folding; nonuniform end filling | Useful as a reference, not preferred |
| Uniformly offset standard involute | Flank shifted outward, root shifted inward | Controls finishing allowance | Root folding; load increases with allowance | Needs careful allowance reduction |
| Nonstandard with mid-face allowance | Larger allowance near the middle of the face | Reduces folding; improves local flow | Still complex; die cost remains high | Better than standard, but not simplest |
| Full-height trapezoid | Simple straight flanks, full tooth height | Simple geometry; easy to define | Narrow and deep slot; difficult pre-forging fill | Not suitable for straight bevel gears |
| Non-full-height trapezoid | Simple flanks, height slightly above half final height | Easy pre-forging fill; creates final shunt space | Requires height and angle control | My selected design |
I define the height of the trapezoidal pre-forging tooth as
$$h_p = \alpha h_f,$$
where \(h_f\) is the final tooth height of the straight bevel gears and \(\alpha\) is a height factor. My design uses
$$0.5 \lt \alpha \lt 0.65,$$
with a preferred value near \(0.55\) to \(0.60\). This means the pre-forging tooth is slightly taller than half of the final tooth. The exact value depends on the cone angle and the face width. For a larger cone angle, the tooth height changes more rapidly from the small end to the large end, so I may choose a slightly smaller \(\alpha\) at the small end and a slightly larger \(\alpha\) at the large end. I express this variation as
$$h_p(x) = \alpha(x) h_f(x),$$
where \(x\) is the position along the cone from the small end to the large end. The trapezoidal flank angle is also adjusted relative to the final involute flank:
$$\theta_p = \theta_f – \Delta\theta,$$
where \(\theta_p\) is the pre-forging flank angle, \(\theta_f\) is the final flank angle, and \(\Delta\theta\) is a small angular reduction. This angular reduction opens the pre-forging slot and makes it easier for metal to enter. The top land width \(w_p\) is chosen so that the pre-forging tooth is not knife-edged:
$$w_p \ge w_{min},$$
where \(w_{min}\) is the minimum top land width that avoids excessive die stress and filling difficulty. The root fillet radius \(r_p\) is kept larger than the final root radius \(r_f\):
$$r_p \gt r_f,$$
because a larger pre-forging fillet improves metal flow and reduces stress concentration in the pre-forging die. The final forging then refines the root region without requiring the pre-forging die to form a sharp corner.
| Pre-forging tooth parameter | Symbol | Design rule | Reason for straight bevel gears |
|---|---|---|---|
| Tooth height | \(h_p\) | \(h_p = \alpha h_f\), \(0.5 \lt \alpha \lt 0.65\) | Leaves final shunt space and avoids deep pre-forging cavity |
| Height variation along face | \(\alpha(x)\) | Smaller at small end, larger at large end if needed | Compensates for changing tooth height |
| Flank angle | \(\theta_p\) | \(\theta_p = \theta_f – \Delta\theta\) | Opens the slot for easier pre-forging fill |
| Top land width | \(w_p\) | \(w_p \ge w_{min}\) | Prevents knife edge and die cracking |
| Root fillet radius | \(r_p\) | \(r_p \gt r_f\) | Improves flow and die strength |
| Draft angle | \(\gamma\) | Positive, typically \(1^\circ\) to \(3^\circ\) | Allows clean ejection from the pre-forging die |
| Corner radius | \(r_c\) | Sufficiently large to avoid stress concentration | Reduces local die wear and filling defects |
| Divided-flow boss diameter | \(d_b\) | Set relative to billet and tooth root diameter | Controls central shunt volume and radial flow |
| Divided-flow boss height | \(h_b\) | Set to create the desired \(V_s\) | Prevents starvation in final forging |
For the numerical simulation of straight bevel gears, I use DEFORM-3D as the finite-element platform. I build the pre-forging die with trapezoidal tooth slots and the final forging die with standard involute tooth slots. I import the models into the simulation system and define the billet as a deformable body. The die surfaces are treated as rigid or near-rigid, which is appropriate because the elastic deformation of the die is small compared with the plastic flow of the billet. I use automatic remeshing to compensate for element distortion. The mesh is initially about 80,000 elements. During the simulation, the local mesh is refined in the tooth regions where large gradients of strain, strain rate, and temperature occur. The volume loss caused by repeated remeshing is compensated automatically so that the predicted fill remains physically meaningful.
The thermal boundary conditions are important for straight bevel gears because the tooth regions have thin sections and high surface-to-volume ratios. I set the initial die temperature to 200\(^\circ\)C and the initial billet temperature to 800\(^\circ\)C. The friction coefficient between the billet and the dies is 0.25, which represents a well-lubricated forging condition but still includes the effect of sliding along the tooth flanks. The upper die moves at 50 mm/s. The heat transfer coefficient between the billet and air is 0.02 N/(s mm\(^\circ\)C), and the heat transfer coefficient between the billet and the dies is 5 N/(s mm\(^\circ\)C). These values allow the simulation to capture the temperature drop near the die surfaces while still allowing the interior of the billet to remain hot enough for flow into the tooth cavities.
| Simulation parameter | Value | Unit | Role in straight bevel gear forging |
|---|---|---|---|
| Mesh element count | 80,000 | elements | Provides resolution in tooth cavities |
| Remeshing | Automatic with volume compensation | — | Controls distortion and volume loss |
| Die initial temperature | 200 | \(^\circ\)C | Represents preheated forging dies |
| Billet initial temperature | 800 | \(^\circ\)C | Hot forging range for the gear material |
| Friction coefficient | 0.25 | — | Models lubricated die-billet contact |
| Upper die velocity | 50 | mm/s | Controls strain rate and press speed |
| Billet-air heat transfer coefficient | 0.02 | N/(s mm\(^\circ\)C) | Accounts for air cooling |
| Billet-die heat transfer coefficient | 5 | N/(s mm\(^\circ\)C) | Accounts for heat loss to dies |
| Material model | Thermo-viscoplastic | — | Captures temperature and rate sensitivity |
I use the following constitutive relation to describe the flow stress of the billet material during the forging of straight bevel gears:
$$\sigma = K \bar{\varepsilon}^n \dot{\bar{\varepsilon}}^m \exp\left(\frac{\beta}{T}\right),$$
where \(\sigma\) is the flow stress, \(\bar{\varepsilon}\) is the effective strain, \(\dot{\bar{\varepsilon}}\) is the effective strain rate, \(T\) is the absolute temperature, and \(K\), \(n\), \(m\), and \(\beta\) are material constants. The effective strain is calculated from the principal strain components as
$$\bar{\varepsilon} = \sqrt{\frac{2}{3}\left(\varepsilon_1^2 + \varepsilon_2^2 + \varepsilon_3^2\right)},$$
and the effective strain rate is
$$\dot{\bar{\varepsilon}} = \sqrt{\frac{2}{3}\left(\dot{\varepsilon}_1^2 + \dot{\varepsilon}_2^2 + \dot{\varepsilon}_3^2\right)}.$$
In the tooth cavity of straight bevel gears, the strain path is not uniform. The small end experiences different radial and tangential compression than the large end. Therefore, I monitor the effective strain distribution rather than a single nominal strain value. The local velocity field is also important. I use the effective velocity
$$v_{eff} = \sqrt{v_r^2 + v_z^2 + v_\theta^2},$$
where \(v_r\), \(v_z\), and \(v_\theta\) are the radial, axial, and tangential velocity components. High \(v_{eff}\) in a narrow region indicates that material is being forced through a small gap. If that gap is not intentionally designed, it can become a folding site. The trapezoidal pre-forging tooth creates a controlled gap between the pre-forging tooth and the final tooth cavity, so the high-velocity region is distributed rather than concentrated at one sharp corner.
I also evaluate the interfacial friction using a shear friction model:
$$\tau_f = m k = m \frac{\sigma_y}{\sqrt{3}},$$
where \(\tau_f\) is the friction shear stress, \(m\) is the friction factor, \(k\) is the shear yield strength, and \(\sigma_y\) is the yield strength. In the simulations, the friction coefficient of 0.25 is used in the Coulomb-like sense for the contact model, while the shear friction relation helps me interpret the local resistance along the tooth flank. The heat transfer at the billet-die interface is
$$q = h \left(T_b – T_d\right),$$
where \(q\) is the heat flux, \(h\) is the interface heat transfer coefficient, \(T_b\) is the billet surface temperature, and \(T_d\) is the die surface temperature. The internal heat conduction is governed by
$$\rho c_p \frac{\partial T}{\partial t} = \nabla \cdot \left(k \nabla T\right) + \dot{q},$$
where \(\rho\) is density, \(c_p\) is specific heat, \(k\) is thermal conductivity, and \(\dot{q}\) is the internal heat generation rate due to plastic deformation. For straight bevel gears, the plastic heat generation is concentrated in the tooth regions, especially near the root and tip corners. This local heating can temporarily reduce flow stress, which helps filling, but it can also accelerate die wear if the contact pressure is high.
The pre-forging stage with the trapezoidal tooth proceeds in several recognizable stages. In the first stage, the central boss of the upper punch contacts the billet end face. The boss does not yet fill the tooth slot. Instead, it creates the divided-flow zone and begins to force material radially outward. In the second stage, the billet contacts the small-end tooth top and then the large-end tooth top. The contact is not simultaneous, which is why the trapezoidal tooth height must vary along the face width. In the third stage, the billet fills the shallow trapezoidal slots and begins to form the conical body. In the fourth stage, the trapezoidal slots are completely filled, and the flash land begins to control the pressure. I summarize these stages in the table below.
| Pre-forging stage for straight bevel gears | Contact condition | Dominant deformation | Material-flow behavior | Design implication |
|---|---|---|---|---|
| Initial boss contact | Punch boss touches billet center | Local upsetting and radial displacement | Material begins to move outward from the center | Boss diameter and height set the shunt volume |
| Partial tooth-top contact | Billet touches small-end tooth tops first | Local compression near the small end | Flow splits toward the tooth flanks and the large end | Small-end preform height must not be excessive |
| Full tooth-top contact | Billet contacts the entire tooth-top region | General upsetting and radial spreading | Material enters the trapezoidal slots | Trapezoidal flank angle controls fill resistance |
| Trapezoidal slot filling | Metal reaches the slot roots and flanks | Combined compression and shear | Slots fill from the bottom toward the top land | Root fillet radius must be large enough |
| Final pre-forging fill | Slots are nearly full; flash land activates | Pressure-driven flow into remaining corners | Material reaches the top land and flash region | Pre-forging load remains moderate |
After pre-forging, the workpiece has a central divided-flow depression, a conical body, and trapezoidal teeth that are slightly taller than half of the final tooth height. During final forging, the standard involute die closes on this preform. The final forging is not a uniform upsetting process. It is a sequence of local filling events. The central depression allows the material to move inward and outward without creating a dead zone. The gap between the trapezoidal pre-forging tooth and the final involute tooth cavity acts as a distributed shunt. Metal flows from the trapezoidal top region toward the final tooth tip, and from the trapezoidal flank region toward the final tooth flank. Because the pre-forging tooth is lower than the final tooth, the final die first contacts the pre-forging tooth top. This contact creates a local pressure increase that drives material into the final tooth tip corner. At the same time, the trapezoidal flank gap allows material to feed the central part of the tooth flank. This dual action is the main reason the trapezoidal nonstandard pre-forging tooth is effective for straight bevel gears.
I evaluate final forging by the fill ratio, velocity field, effective strain, and forming load. The fill ratio of the tooth tip corner is defined as
$$\eta_{tip} = \frac{V_{tip,filled}}{V_{tip,cavity}},$$
and the fill ratio of the root region is
$$\eta_{root} = \frac{V_{root,filled}}{V_{root,cavity}}.$$
My simulation target is to achieve \(\eta_{tip} \ge 0.98\) and \(\eta_{root} \ge 0.98\) before the load reaches the press limit. The forming load is estimated by integrating the normal and shear stresses over the die-billet contact area:
$$F = \int_A \sigma_n \, dA + \int_A \tau \, dA,$$
where \(\sigma_n\) is the normal contact stress and \(\tau\) is the shear contact stress. The load reduction achieved by the trapezoidal pre-forging tooth relative to a standard involute pre-forging tooth can be expressed as
$$\Delta F = \frac{F_{std} – F_{trap}}{F_{std}} \times 100\%,$$
where \(F_{std}\) is the maximum load with the standard pre-forging tooth and \(F_{trap}\) is the maximum load with the trapezoidal pre-forging tooth. In my simulations, the trapezoidal design reduces the peak load because the pre-forging stage requires less pressure to fill a shallow trapezoidal slot than a deep involute slot. The final forging load is also better distributed because the material does not have to travel as far in a single step.
| Final forging feature for straight bevel gears | Observed behavior with trapezoidal pre-forging tooth | Mechanism | Quality consequence |
|---|---|---|---|
| Tooth tip corner | Complete filling without a sharp pressure spike | Pre-forging tooth top provides a local reservoir and shunt gap | Reduced risk of incomplete tip |
| Tooth flank | Smooth and symmetric flow from mid-face toward edges | Trapezoidal flank gap distributes material | Lower folding risk |
| Tooth root | Progressive filling with larger pre-forging fillet | Large pre-forging fillet reduces local resistance | Better root contour and die life |
| Small end | Fills earlier and then acts as a flow guide | Lower pre-forging height at small end | Prevents small-end overloading |
| Large end | Fills later but receives material from the shunt gap | Height variation along the face width | Improves large-end completeness |
| Central region | Divided-flow depression helps radial and axial flow | Boss-created reservoir | Reduces dead zone and backpressure |
| Flash formation | Controlled and progressive | Preform volume distribution | Lower material waste and load |
| Tooth symmetry | Symmetric left and right flanks | Balanced trapezoidal geometry | Better final gear quality |
The velocity-field results confirm the benefit of the trapezoidal nonstandard pre-forging tooth for straight bevel gears. In the pre-forging stage, the velocity vectors show that material first moves radially outward from the central boss, then turns into the trapezoidal slots, and finally moves upward into the top land region. The velocity magnitude is highest near the boss and near the slot entrance, but it is not concentrated in a single narrow band. In the final forging stage, the velocity field changes. The material in the trapezoidal tooth region moves toward the final tooth tip and flank. The central divided-flow region continues to feed material toward the tooth roots. The large-end region receives additional material from the shunt gap that was created by the lower pre-forging tooth height. Because the pre-forging tooth is not full height, the final forging does not have to compress a solid tooth-shaped block. Instead, it deforms a preform that already has a favorable volume distribution.
I also examine the effective strain distribution. In a poorly designed preform for straight bevel gears, the strain can localize near the root or near the mid-face, producing a fold. In the trapezoidal design, the effective strain is more uniformly distributed. The maximum effective strain occurs near the tooth tip and the root corner, which are the regions that require the most deformation to reach the final involute shape. However, the maximum is not accompanied by a sharp velocity discontinuity. The strain gradient is moderate because the pre-forging tooth provides a gradual transition from the trapezoidal shape to the involute shape. The strain rate is also controlled by the die velocity of 50 mm/s. A lower die velocity would reduce the strain rate and the flow stress, but it would also reduce productivity. The chosen velocity is a compromise that keeps the forging load within a reasonable range while still filling the tooth cavity.
The temperature field shows that the billet surface cools near the die contact regions, especially at the tooth tips and the flash land. The interior of the billet remains hotter and therefore more deformable. The trapezoidal pre-forging tooth reduces the contact area in the early stage, which slows the heat loss from the tooth flanks. In the final forging stage, the contact area increases rapidly as the final tooth cavity fills. The heat transfer coefficient of 5 N/(s mm\(^\circ\)C) is high enough to produce a measurable surface temperature drop, but the simulation still predicts complete filling because the flow stress remains acceptable. If the die temperature were lower or the transfer coefficient were higher, the tooth tip corner would be the first region to suffer from incomplete filling. This is another reason the pre-forging shunt space is valuable: it allows the final filling to occur with less total deformation and less exposure to cold die surfaces.
I summarize the volume balance for the trapezoidal pre-forging design with the following relation:
$$V_{pre} = V_{trap} + V_{cone} + V_{boss} + V_{flash,pre},$$
where \(V_{trap}\) is the volume of the trapezoidal teeth, \(V_{cone}\) is the volume of the conical body, \(V_{boss}\) is the volume displaced by the divided-flow boss, and \(V_{flash,pre}\) is the pre-forging flash volume. The final forging volume balance is
$$V_{final} = V_{pre} – V_{flash,pre} + V_{shunt} – V_{flash,final} – V_{loss},$$
where \(V_{shunt}\) is the additional cavity volume between the pre-forging tooth and the final tooth, and \(V_{flash,final}\) is the final flash volume. For a successful design, \(V_{shunt}\) must be positive but not excessive. I express the optimal shunt volume as a fraction of the final tooth volume:
$$V_{shunt} = \lambda V_{tooth},$$
where \(\lambda\) is a shunt fraction. In my simulations, a value of \(\lambda\) between 0.08 and 0.18 gives good filling without excessive flash. If \(\lambda\) is too small, the tooth tip corner starves. If \(\lambda\) is too large, the final forging becomes a low-pressure upsetting process that produces excessive flash and poor dimensional control. The exact value depends on the cone angle and the tooth height distribution of the straight bevel gears.
| Volume component | Symbol | Design role in straight bevel gears | Typical target |
|---|---|---|---|
| Final tooth volume | \(V_{tooth}\) | Defines the required material in the tooth region | Fixed by gear geometry |
| Trapezoidal pre-forging tooth volume | \(V_{trap}\) | Provides part of the final tooth volume in a simple shape | About 45% to 60% of \(V_{tooth}\) |
| Shunt volume | \(V_{shunt}\) | Feeds tooth tip and flank during final forging | \(0.08 V_{tooth}\) to \(0.18 V_{tooth}\) |
| Central boss volume | \(V_{boss}\) | Creates divided-flow zone and radial flow | Depends on billet diameter |
| Pre-forging flash | \(V_{flash,pre}\) | Controls pre-forging pressure | Minimized but sufficient |
| Final flash | \(V_{flash,final}\) | Controls final cavity pressure | Small and uniform |
| Loss | \(V_{loss}\) | Accounts for scale, flash trimming, and simulation compensation | Kept below a few percent |
The die design for the trapezoidal pre-forging tooth is simpler than the die design for a standard involute pre-forging tooth. The trapezoidal flank is a straight line in the axial cross-section, so the electrode or milling path is easier to generate. The top land is a simple surface, and the root fillet can be made larger. This simplicity reduces the manufacturing cost of the pre-forging die. For straight bevel gears, the pre-forging die is not the final die, so it does not need to produce the exact involute surface. It only needs to produce a preform that allows the final die to fill correctly. Therefore, I can accept a simpler pre-forging tooth as long as the final forging quality is maintained. The trapezoidal design achieves this balance.
I also consider the effect of the divided-flow boss on the final forging of straight bevel gears. The boss creates a central depression in the preform. During final forging, this depression collapses and feeds material toward the tooth roots and flanks. If the boss is too small, the central reservoir is insufficient, and the tooth roots may not fill. If the boss is too large, the final forging may produce a deep central defect or excessive flash. I therefore define the boss volume as a function of the tooth volume:
$$V_{boss} = \mu V_{tooth},$$
where \(\mu\) is the boss volume fraction. I have found that \(\mu\) between 0.05 and 0.12 is a reasonable starting range for straight bevel gears. The boss diameter \(d_b\) and height \(h_b\) satisfy
$$V_{boss} = \frac{\pi}{4} d_b^2 h_b$$
for a simple cylindrical boss. If the boss has a draft angle or a rounded corner, the volume is adjusted accordingly. The boss should be centered on the billet axis and should not extend into the tooth region. Its purpose is to create a controlled flow path, not to replace the tooth preform. The trapezoidal tooth and the boss together create a two-level shunt system. The boss controls the central flow, while the trapezoidal tooth gap controls the local tooth flow. This combination is what makes the central divided flow method effective for straight bevel gears.
I compare the trapezoidal design with the standard involute design using the following fill and load indicators:
$$\eta_{std} = \frac{V_{filled,std}}{V_{cavity}}, \qquad \eta_{trap} = \frac{V_{filled,trap}}{V_{cavity}},$$
and
$$F_{std} = \max\left(F(t)\right)_{std}, \qquad F_{trap} = \max\left(F(t)\right)_{trap}.$$
The improvement in fill is
$$\Delta \eta = \eta_{trap} – \eta_{std},$$
and the load reduction is
$$\Delta F = \frac{F_{std} – F_{trap}}{F_{std}} \times 100\%.$$
In my numerical experiments, \(\Delta \eta\) is positive in the tooth tip and root regions, and \(\Delta F\) is positive because the trapezoidal pre-forging tooth requires less pressure to fill the pre-forging cavity. The final forging also benefits because the material has less distance to travel. The exact values depend on the specific straight bevel gear geometry, but the trend is consistent: a simpler pre-forging tooth with a carefully chosen height and shunt volume can improve both filling and load.
| Indicator | Standard involute pre-forging tooth | Trapezoidal nonstandard pre-forging tooth | Interpretation for straight bevel gears |
|---|---|---|---|
| Pre-forging die complexity | High | Low | Trapezoid is easier to manufacture |
| Pre-forging fill resistance | High in deep tooth slots | Lower in shallow slots | Trapezoid fills more easily |
| Final tooth tip fill | May be incomplete at large end | Improved by shunt gap | Better tip corner filling |
| Folding tendency | Higher | Lower | More uniform flow |
| Maximum forming load | Higher | Lower to moderate | Reduced press requirement |
| Die life | Shorter if load is high | Longer due to lower load and simpler geometry | Better production economy |
| Final involute accuracy | Good if filling is complete | Good after final forging | Final die controls the involute |
| Application to straight bevel gears | Possible but sensitive | Preferred in my design | Balances quality and cost |
I further analyze the final forging load history. The load curve typically has three phases. In the first phase, the final die contacts the trapezoidal tooth tops. The load rises slowly because the contact area is small and the material can still flow into the shunt gap. In the second phase, the tooth flanks and root regions begin to fill. The load rises more rapidly because the contact area increases and the flash land begins to restrict flow. In the third phase, the tooth tips and corners complete filling. The load reaches its maximum near the end of the stroke. With the trapezoidal pre-forging tooth, the third phase is shorter and less intense than with a standard pre-forging tooth because the shunt gap has already supplied material to the critical regions. This reduces the risk of die overload and improves die life.
I express the load history as a function of stroke \(s\):
$$F(s) = F_0 + c_1 s + c_2 s^2 + c_3 \exp\left(c_4 s\right),$$
where \(F_0\) is the initial contact load and \(c_1\), \(c_2\), \(c_3\), and \(c_4\) are fitting coefficients. The exponential term represents the rapid load increase near the end of the stroke when the flash land and tooth corners are filled. A well-designed pre-forging tooth reduces \(c_3\) and \(c_4\) because the final cavity is not starved. In my simulation, the trapezoidal design produces a smoother load curve with a less abrupt final rise. This is favorable for press selection and die stress control.
The strain distribution also affects the final tooth quality. I define the strain homogeneity index as
$$H = 1 – \frac{\bar{\varepsilon}_{max} – \bar{\varepsilon}_{min}}{\bar{\varepsilon}_{avg}},$$
where \(\bar{\varepsilon}_{max}\), \(\bar{\varepsilon}_{min}\), and \(\bar{\varepsilon}_{avg}\) are the maximum, minimum, and average effective strains in the tooth region. A value of \(H\) close to 1 indicates a homogeneous strain distribution. A low value indicates strain localization. In my simulations, the trapezoidal pre-forging tooth increases \(H\) compared with a standard involute pre-forging tooth. The reason is that the trapezoidal shape distributes the deformation over a larger volume and avoids a sharp transition at the root. For straight bevel gears, a more homogeneous strain distribution is beneficial because it reduces residual stress and improves dimensional stability after heat treatment.
The temperature history is equally important. The local temperature at the tooth surface can drop significantly during final forging because the die is cooler than the billet. I define the dimensionless temperature drop as
$$\Theta = \frac{T_b – T_d}{T_b – T_0},$$
where \(T_0\) is the initial die temperature. A larger \(\Theta\) means a greater relative cooling effect. In the tooth tip corner, \(\Theta\) can become large if the contact time is long and the flow distance is short. The trapezoidal pre-forging tooth reduces the contact time in the critical corner because the corner fills earlier. Therefore, the temperature drop is less severe, and the local flow stress remains lower. This further improves filling.
From a die-manufacturing perspective, the trapezoidal tooth is attractive because it can be produced by simple milling or grinding operations. The straight flanks do not require a special involute profile. The top land and root fillet can be formed with standard tools. This reduces the lead time and cost of the pre-forging die. Since the pre-forging die is not the final die, its surface finish does not need to match the final gear tooth surface. It only needs to be smooth enough to allow material flow and clean ejection. The final die, which contains the standard involute cavity, is the die that determines the final tooth accuracy. By simplifying the pre-forging die, I can allocate more manufacturing precision to the final die.
I also consider the effect of the trapezoidal pre-forging tooth on flash. Flash is necessary to build pressure in the final forging cavity, but excessive flash wastes material and increases trimming cost. The trapezoidal pre-forging tooth provides a better volume distribution, so the final flash can be thinner and more uniform. The flash ratio is defined as
$$R_{flash} = \frac{V_{flash,final}}{V_{final}} \times 100\%.$$
In my design, I aim for a small but positive flash ratio. If \(R_{flash}\) is too small, the cavity pressure may be insufficient to fill the tooth tip. If \(R_{flash}\) is too large, material waste and trimming load increase. The trapezoidal pre-forging tooth helps control \(R_{flash}\) because the preform volume is closer to the final tooth volume distribution, even though the shape is simpler.
| Response variable | Symbol | Definition | Target for straight bevel gears |
|---|---|---|---|
| Tooth tip fill ratio | \(\eta_{tip}\) | \(V_{tip,filled}/V_{tip,cavity}\) | \(\ge 0.98\) |
| Root fill ratio | \(\eta_{root}\) | \(V_{root,filled}/V_{root,cavity}\) | \(\ge 0.98\) |
| Shunt fraction | \(\lambda\) | \(V_{shunt}/V_{tooth}\) | 0.08 to 0.18 |
| Boss volume fraction | \(\mu\) | \(V_{boss}/V_{tooth}\) | 0.05 to 0.12 |
| Height factor | \(\alpha\) | \(h_p/h_f\) | 0.55 to 0.60 |
| Flash ratio | \(R_{flash}\) | \(V_{flash,final}/V_{final}\) | Small but positive |
| Strain homogeneity | \(H\) | 1 minus normalized strain range | As high as possible |
| Load reduction | \(\Delta F\) | \((F_{std}-F_{trap})/F_{std}\) | Positive |
The numerical simulation of straight bevel gears with the trapezoidal pre-forging tooth shows complete final filling. The final forging has a smooth tooth surface, a symmetric tooth profile, and well-defined tooth tips. The root region is filled without a visible fold. The large end and small end both reach the final die surface. The central divided-flow depression is eliminated by the final forging, and the flash is uniform. These results support the feasibility of the trapezoidal nonstandard pre-forging tooth. They also show that the pre-forging design does not need to replicate the final involute tooth. A simpler intermediate shape can be more effective if it creates the right volume distribution and flow paths.
I summarize the design logic in equation form. The final tooth volume is partitioned as
$$V_{tooth} = V_{trap} + V_{shunt} + V_{final,local},$$
where \(V_{final,local}\) is the volume that is formed directly by the final die from the preform. The pre-forging tooth height is
$$h_p = \alpha h_f, \qquad 0.5 \lt \alpha \lt 0.65,$$
and the flank angle is
$$\theta_p = \theta_f – \Delta\theta, \qquad \Delta\theta \gt 0.$$
The divided-flow volume is
$$V_s = V_{boss} + V_{trap,gap},$$
where \(V_{trap,gap}\) is the volume of the gap between the trapezoidal pre-forging tooth and the final tooth cavity. The total volume balance is
$$V_p = V_f + V_{fl} + V_s + V_l.$$
These equations provide a compact framework for designing pre-forging teeth for straight bevel gears. They can be used to check whether a proposed preform has enough material in the right places and whether the shunt volume is sufficient for final filling.
| Design equation | Expression | Purpose |
|---|---|---|
| Pre-forging tooth height | \(h_p = \alpha h_f\) | Sets the vertical gap for final filling |
| Height factor range | \(0.5 \lt \alpha \lt 0.65\) | Balances easy pre-forging and sufficient volume |
| Flank angle | \(\theta_p = \theta_f – \Delta\theta\) | Opens the pre-forging slot |
| Shunt volume | \(V_s = V_{boss} + V_{trap,gap}\) | Feeds tooth tip and flank during final forging |
| Volume balance | \(V_p = V_f + V_{fl} + V_s + V_l\) | Ensures no starvation or excess flash |
| Fill ratio | \(\eta_f = V_{filled}/V_{cavity}\) | Quantifies local filling |
| Load reduction | \(\Delta F = (F_{std}-F_{trap})/F_{std}\) | Measures improvement over standard preform |
| Strain homogeneity | \(H = 1 – (\bar{\varepsilon}_{max}-\bar{\varepsilon}_{min})/\bar{\varepsilon}_{avg}\) | Measures uniformity of deformation |
| Flash ratio | \(R_{flash} = V_{flash,final}/V_{final}\) | Controls material waste and cavity pressure |
From my results, I draw several conclusions for the precision forging of straight bevel gears. First, the pre-forging tooth shape is not a minor detail. It controls the final material flow, the filling of the tooth tip and root, and the maximum forming load. Second, a nonstandard pre-forging tooth can be superior to a standard involute pre-forging tooth because it can provide a better volume distribution and a more controlled shunt path. Third, a trapezoidal nonstandard tooth with a height slightly greater than half of the final tooth height is feasible for straight bevel gears. It is easy to manufacture, it fills well during pre-forging, and it provides the necessary shunt volume for final forging. Fourth, the central divided flow method works together with the trapezoidal tooth. The central boss creates a reservoir, and the trapezoidal tooth creates a distributed gap. The combination improves filling and reduces the risk of folding.
I also conclude that the pre-forging design should remain as simple as possible while still satisfying the final forging requirements. Since the pre-forging step is not the final step, it does not need to reproduce the exact involute tooth surface. A simplified tooth shape reduces die cost and manufacturing time. The final die, which contains the standard involute cavity, controls the final tooth accuracy. Therefore, the design strategy is to use a simple pre-forging tooth to create the correct volume distribution and flow paths, and then use the final forging die to produce the precise straight bevel gear tooth form.
| Conclusion element | Finding for straight bevel gears | Practical consequence |
|---|---|---|
| Pre-forging tooth importance | Controls fill, load, and defect formation | Must be designed with volume and flow in mind |
| Standard involute preform | Close to final shape but not always optimal | Can cause folding and incomplete filling |
| Nonstandard preform | Can improve flow and reduce defects | More robust than a simple offset |
| Trapezoidal tooth | Simple, fillable, and effective | Feasible for production |
| Non-full-height feature | Creates final shunt space | Improves tip and root filling |
| Central divided flow | Adds a central reservoir | Reduces dead zones and backpressure |
| DEFORM-3D validation | Predicts complete filling and symmetric profile | Supports the proposed design |
| Die cost | Simpler pre-forging die lowers cost | Better overall process economy |
For future work, I would extend the current model of straight bevel gears by including die elasticity, wear prediction, and a full thermal-mechanical coupling with temperature-dependent material properties. I would also study how the trapezoidal tooth height factor \(\alpha\) and the shunt fraction \(\lambda\) change with different cone angles and face widths. A design map could be constructed with \(\alpha\) on one axis and \(\lambda\) on the other, showing regions of incomplete filling, folding, excessive flash, and optimal filling. Such a map would make the pre-forging design of straight bevel gears more systematic and less dependent on trial and error. I would also compare the trapezoidal pre-forging tooth with other simple nonstandard shapes, such as rounded trapezoids and stepped trapezoids, to determine whether additional flow control can further reduce load or improve tooth quality.
In summary, my work shows that the pre-forging tooth design for straight bevel gears can be simplified without sacrificing final forging quality. The trapezoidal nonstandard tooth, combined with the central divided flow method, provides a practical route to complete tooth filling, reduced folding risk, lower forming load, and lower die manufacturing cost. The numerical simulation confirms that the final involute tooth cavity can be filled completely from a trapezoidal preform. The design equations and tables presented here give a framework for selecting the pre-forging tooth height, flank angle, boss volume, and shunt volume. For straight bevel gears produced by precision forging, this framework supports a two-step process that is both technically feasible and economically attractive.