
I began my study from a practical manufacturing problem: the straight bevel gear is a fundamental mechanical transmission component, and it is used in machine tools, vehicles, construction machinery, and many other systems where motion must be transferred between intersecting axes. In my view, the straight bevel gear remains difficult to produce by near-net forming because its tooth geometry changes continuously along the cone, the die cavity is complex, and the forming load concentrates near the small end and the tooth tips. I therefore focused my work on a two-way upsetting-extrusion process for the precision forming of a straight bevel gear. My aim was to determine whether a two-way upsetting-extrusion route can improve tooth filling, reduce punch load, simplify the die structure, and still produce a straight bevel gear without flash, folding, cracking, or incomplete corners.
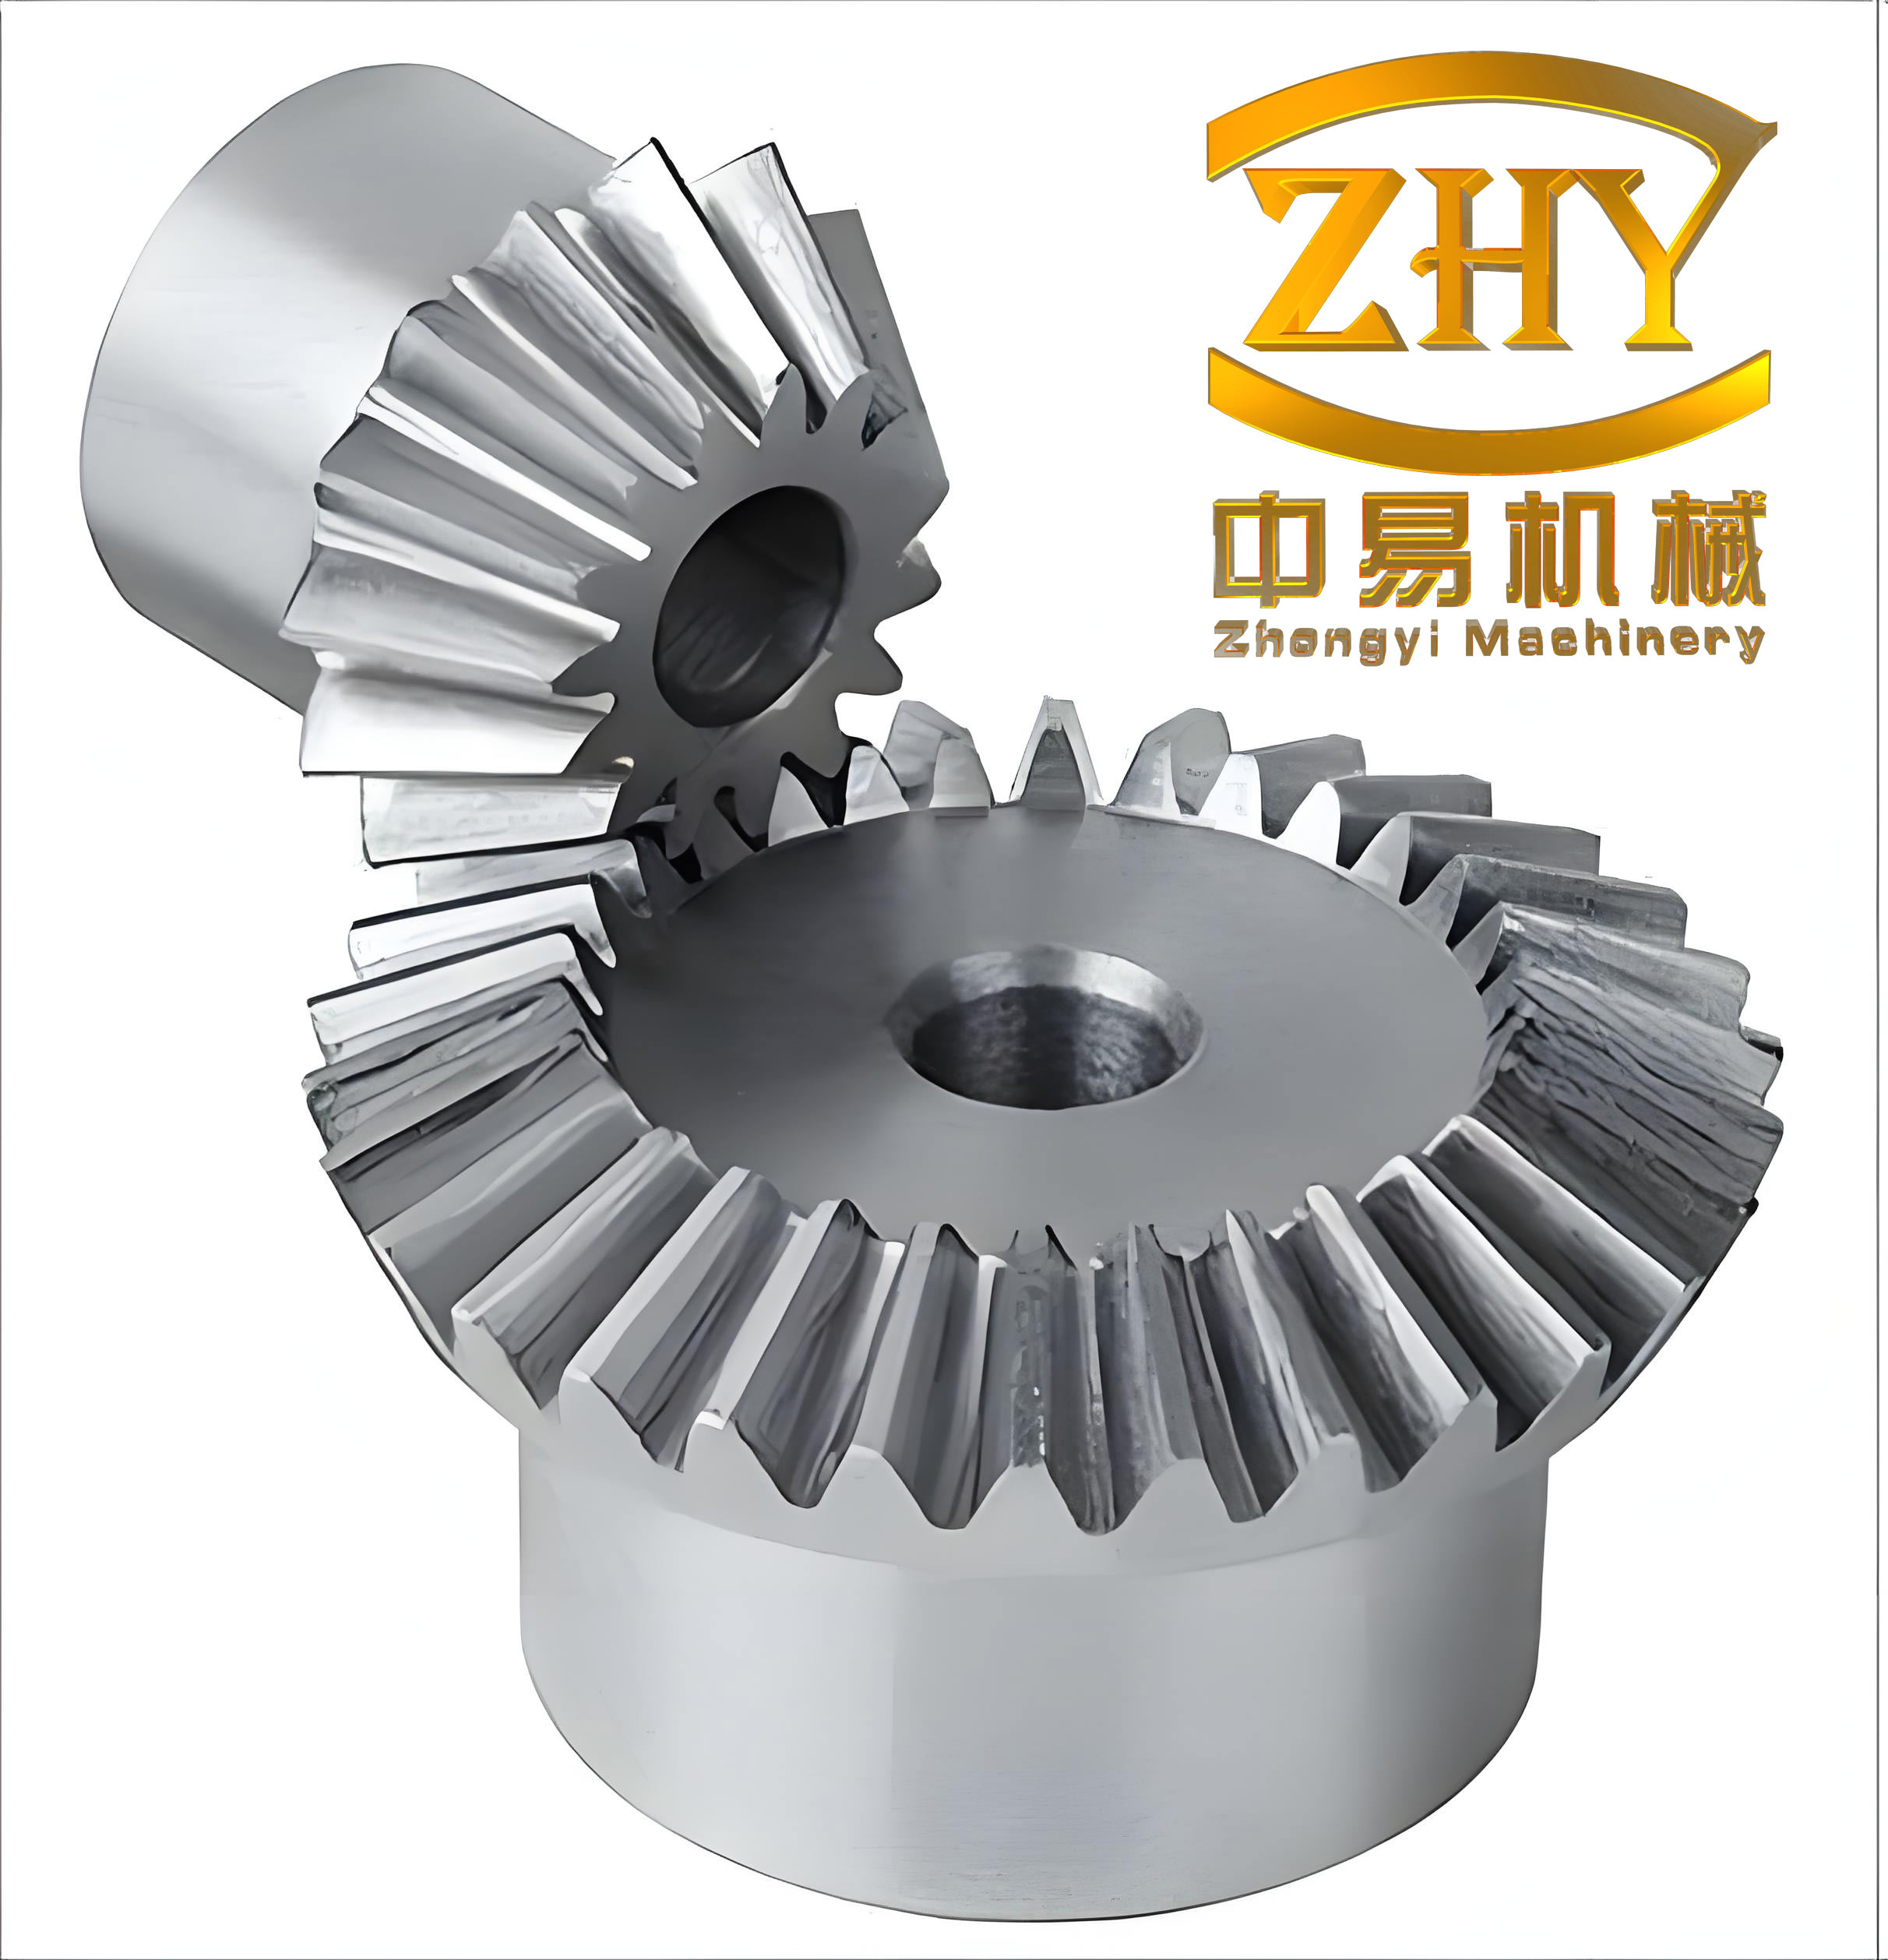
I selected a straight bevel gear made of 45 steel as the reference component for my numerical and physical work. The target precision forging was defined by a set of basic geometric parameters that control the tooth profile, the root cone, and the preform envelope. I summarized these parameters in Table 1 because the entire forming strategy depends on them. For a straight bevel gear, the pitch cone angle, the large-end module, the number of teeth, and the face width determine the tooth space and the metal flow path. In my model, the straight bevel gear had 18 teeth, a face width of 25 mm, a large-end module of 3.5 mm, a pressure angle of 20 degrees, a pitch cone angle of 45 degrees, an addendum coefficient of 1, a clearance coefficient of 0.4, and a root fillet radius of 0.4 mm. These values were not arbitrary; they produced a straight bevel gear whose tooth cavity was deep enough to reveal filling problems but still simple enough for systematic finite element analysis.
| Parameter | Symbol | Value |
|---|---|---|
| Number of teeth | z | 18 |
| Face width | b | 25 mm |
| Large-end module | m | 3.5 mm |
| Pressure angle | alpha | 20 degrees |
| Pitch cone angle | delta | 45 degrees |
| Addendum coefficient | h_a^* | 1 |
| Clearance coefficient | c^* | 0.4 |
| Root fillet radius | r_f | 0.4 mm |
I describe the geometry of the straight bevel gear by the usual cone relationships. For a straight bevel gear with pitch cone angle delta, the addendum and dedendum at the large end can be written as:
$$
h_a = h_a^* m
$$
$$
h_f = (h_a^* + c^*) m
$$
The root diameter and the tooth depth are then obtained from the cone geometry. For my straight bevel gear, these equations gave a tooth depth that had to be filled by radial and axial metal flow inside the integral die. I also used the pitch cone relation:
$$
\tan \delta = \frac{z_1}{z_2}
$$
where z_1 and z_2 are the tooth numbers of the mating gears. In the present straight bevel gear study, the pitch cone angle was prescribed as 45 degrees, so the cone geometry was symmetric in the sense that the large-end and small-end flow paths were both important. This symmetry helped me compare the upper and lower sides of the two-way upsetting-extrusion process without favoring one side geometrically.
I then considered the conventional closed-die extrusion route for a straight bevel gear. In the traditional block extrusion method, the upper and lower concave dies are separate, and the punches are designed with diameters not larger than the root circle at the corresponding end. The billet is compressed from the small end or from the large end, and the metal in the center is forced radially into the conical tooth cavity. The maximum contact area between the punch and the billet is essentially the end face area of the punch. This conventional route can form a straight bevel gear, but it has two disadvantages that I wanted to address. First, the forming force becomes very high when the tooth corners are filled. Second, the die structure is complex because the upper and lower concave dies must close and apply a preload before the punch acts.
In my proposed process, I optimized the traditional upper and lower concave dies into one integral concave die. I also replaced the conventional upper and lower convex punches with tooth-shaped punches. This change is important for a straight bevel gear because the tooth-shaped punches increase the contact area once metal enters the internal tooth cavity at the two ends of the die. The maximum increase in contact area corresponds to the sum of the tooth cross-sectional areas. When the straight bevel gear is formed, the upper punch can also serve as an ejector and push the part out from the large end. If the total ejection force is fixed, a larger ejection area reduces the ejection stress on the punch, which is beneficial for die life.
| Feature | Traditional Closed Die | My Two-Way Integral Die |
|---|---|---|
| Concave die construction | Separate upper and lower dies | One integral die |
| Closing and preload | Required before punch motion | Not required |
| Punch shape | Simple circular or conical end | Tooth-shaped upper and lower punches |
| Contact area during filling | Limited to punch end area | Increased by tooth cross-sectional area |
| Flash risk | Higher at die parting surfaces | Lower because integral die has no parting gap |
| Ejection | Separate ejector often needed | Upper punch can act as ejector |
| Applicability to straight bevel gear | Workable but load-intensive | Better filling and lower load in my simulation |
The reason I expected a lower load in two-way upsetting-extrusion is the effective friction principle. In one-way upsetting-extrusion of a straight bevel gear, the friction force on the billet side surface acts mainly in one direction, either upward or downward along the conical surface. As more metal fills the tooth cavity, the contact area and the normal pressure increase, so the friction force also increases. This rising friction makes the corner filling of the straight bevel gear more difficult and raises the punch load. In two-way upsetting-extrusion, the friction directions on the billet side surface are opposite on the upper and lower sides. The opposing friction components reduce the net friction resistance, which lowers the forming load and makes the upper and lower corner regions easier to fill.
I expressed the friction stress using the common shear friction model:
$$
\tau = m k
$$
where m is the friction factor and k is the shear yield strength. For a von Mises material, k can be related to the flow stress by:
$$
k = \frac{\sigma_f}{\sqrt{3}}
$$
I then wrote the total friction force on the billet as an integral over the contact area:
$$
F_f = \int_A \tau \, dA
$$
For the two-way process, the net friction contribution can be approximated as the difference between the upper and lower friction resultants:
$$
F_{f,net} = \int_{A_u} \tau_u \, dA_u – \int_{A_l} \tau_l \, dA_l
$$
In my finite element model, the friction factor was set to 0.3, and the actual friction stress was computed locally from the contact pressure and the relative sliding velocity. This is why the two-way straight bevel gear forming route produced a more balanced metal flow than the one-way route.
Before running the finite element simulation, I designed the preform for the straight bevel gear. Because the process is a closed upsetting-extrusion operation, the final volume must equal the initial volume. The preform must be contained inside the geometric body bounded by the root cone and the two cylindrical surfaces defined by the large-end and small-end root circles. In other words, the two ends of the preform must lie within the root circle diameters of the straight bevel gear. I used the following volume conservation relation:
$$
V_0 = V_f
$$
For an axisymmetric approximation of the preform, the volume can be written as:
$$
V_0 = \pi \int_{z_1}^{z_2} r^2(z) \, dz
$$
I designed the preform with a central conical body and flat ends. The upper and lower ends were chosen to fit within the corresponding root circles, and the side profile was adjusted so that the tooth cavity would be filled uniformly. The main preform dimensions I used are listed in Table 2. These dimensions were later imported into the finite element model and also used for the physical die set.
| Preform feature | Dimension |
|---|---|
| Upper end diameter | 40 mm |
| Lower end diameter | 52 mm |
| Central reference diameter | 50 mm |
| Outer cone-related diameter | 57.92 mm |
| Large-end reference diameter | 62.5 mm |
| Outer large-end diameter | 66.16 mm |
| Preform height | 28.6 mm |
| Initial volume basis | Equal to final straight bevel gear forging volume |
I performed the numerical simulation with DEFORM-3D. The billet material was AISI-1045, which is equivalent to 45 steel for my purposes, and the billet temperature was set to 1100 degrees C. The dies were treated as rigid, with a die temperature of 350 degrees C. The friction coefficient was 0.3, and the upper and lower punch speeds were set to 8 mm/s. I used a simulation step of 0.08 mm, following the rule that the step length should not exceed one third of the smallest element edge. After volume compensation was activated, I ran the simulation until the tooth cavity was filled. The input parameters are summarized in Table 3.
| Simulation parameter | Value |
|---|---|
| Finite element software | DEFORM-3D |
| Billet material | AISI-1045 |
| Billet temperature | 1100 degrees C |
| Die temperature | 350 degrees C |
| Die condition | Rigid |
| Friction coefficient | 0.3 |
| Punch speed | 8 mm/s |
| Simulation step | 0.08 mm |
| Volume compensation | Activated |
| Mesh type | Tetrahedral with automatic remeshing |
I used the finite element method to make the deformation field visible at every stage. The straight bevel gear forming process can be studied through the equivalent stress, equivalent strain, strain rate, velocity field, contact pressure, and damage criteria. The equivalent strain was calculated as:
$$
\bar{\varepsilon} = \sqrt{\frac{2}{3} \varepsilon_{ij} \varepsilon_{ij}}
$$
The equivalent stress was calculated from the deviatoric stress tensor:
$$
\bar{\sigma} = \sqrt{\frac{3}{2} s_{ij} s_{ij}}
$$
For the hot forming of AISI-1045, I used a flow stress relation of the following general form:
$$
\sigma_f = K \bar{\varepsilon}^{n} \dot{\bar{\varepsilon}}^{m} \exp\left(\frac{\beta}{T}\right)
$$
where K is the strength coefficient, n is the strain-hardening exponent, m is the strain-rate sensitivity, beta is a temperature-related constant, and T is the absolute temperature. In my simulation I allowed the flow stress to update with temperature, strain, and strain rate at every step. This was necessary because the straight bevel gear has a large variation in local strain near the tooth root and tooth tip.
I also tracked the filling ratio of the straight bevel gear cavity. For a local cavity region, I defined the filling ratio as:
$$
R_f = \frac{V_{filled}}{V_{cavity}} \times 100\%
$$
A value of R_f equal to 100 percent means that the local tooth cavity is completely filled. I used this measure to compare the upper and lower ends of the straight bevel gear. The results showed that the two-way process filled the cavity more uniformly than either one-way process.
From the simulation, the deformation of the straight bevel gear billet passed through three recognizable stages. In the first stage, the two ends of the billet were upset and the metal flowed quickly toward the middle tooth-forming region. In the second stage, the metal in the tooth-forming region spread radially and filled the conical tooth cavity. In the third stage, the middle of the tooth cavity was already nearly full, while the upper and lower corners still needed metal. A small additional stroke then filled both ends almost simultaneously. I summarized these stages in Table 4. The stage description helped me explain why the load curve has a long, slowly rising portion followed by a sharp final rise.
| Stage | Approximate step range | Approximate stroke | Dominant behavior |
|---|---|---|---|
| Free deformation | 1 to 6 | 0 to 0.55 mm | Billet ends upset; local loading and overall deformation |
| Filling | 7 to 98 | 0.55 to 4.64 mm | Tooth cavity fills gradually and uniformly |
| Corner filling | 99 to 100 | 4.64 to 4.67 mm | End corners fill; load rises rapidly |
During the free deformation stage, the outer profile of the preform was slightly smaller than the tooth cavity of the integral die. Therefore, the billet could deform without immediate constraint from the tooth walls. The load increased gently because the deformation was distributed over the whole billet rather than concentrated at the teeth. In the filling stage, the billet contacted the tooth cavity and the metal began to flow into the tooth spaces. The contact area increased progressively, and the load increased slowly at first and then more quickly. In the corner filling stage, the middle of the straight bevel gear cavity was already full, so the remaining punch motion had to force metal into the last upper and lower corner volumes. This is the stage that controls the maximum load and the required press capacity.
I plotted the load-stroke curves for the upper and lower punches in the two-way upsetting-extrusion of the straight bevel gear. The maximum upper punch load was 0.66 MN, and the maximum lower punch load was 3.17 MN. In the one-way process from the large end, the maximum load was 4.66 MN. In the one-way process from the small end, the maximum load was 1.49 MN. I summarized the load comparison in Table 5. The two-way straight bevel gear process reduced the upper punch load by 55.6 percent and the lower punch load by 32.0 percent compared with the corresponding one-way loads. This reduction is significant because it means that a smaller press could be used, and the die would experience lower mechanical loading.
| Forming route | Upper or small-end load | Lower or large-end load | Maximum load |
|---|---|---|---|
| One-way from large end | Not applicable | 4.66 MN | 4.66 MN |
| One-way from small end | 1.49 MN | Not applicable | 1.49 MN |
| Two-way upsetting-extrusion | 0.66 MN | 3.17 MN | 3.17 MN |
| Reduction of upper load | 55.6 percent | Not applicable | Not applicable |
| Reduction of lower load | Not applicable | 32.0 percent | Not applicable |
I calculated the load reduction ratios using the following equations:
$$
R_u = \frac{F_{one,u} – F_{two,u}}{F_{one,u}} \times 100\%
$$
$$
R_l = \frac{F_{one,l} – F_{two,l}}{F_{one,l}} \times 100\%
$$
Substituting the numerical values gave R_u equal to 55.6 percent and R_l equal to 32.0 percent. I interpret this result as evidence that the effective friction principle works well for the straight bevel gear. The opposing friction directions in the two-way route reduce the net resistance to metal flow along the conical surface, so less punch force is needed to fill the tooth cavity.
I also examined the filling quality of the straight bevel gear in the one-way and two-way routes. In the one-way route from the large end, the lower side of the tooth cavity filled first and the upper side remained incomplete for a longer time. In the one-way route from the small end, the upper side filled first and the lower side remained incomplete. Although the difference in the number of steps between the two ends was not very large, the final load rise was controlled by the last corner to fill. In the two-way route, the upper and lower corners filled almost simultaneously. The tooth profile was full and smooth, the outline was clear, and the tooth tip and root fillets were filled with smooth transitions. I observed no folding or collapse in the two-way simulation. I did observe a small amount of flash-like burr at the end faces because a small clearance existed between the punch and the integral die. This is a die-fit issue rather than a process-flow defect.
| Quality feature | One-way from large end | One-way from small end | Two-way upsetting-extrusion |
|---|---|---|---|
| Upper corner filling | Incomplete for a longer time | Fills earlier | Fills almost simultaneously with lower corner |
| Lower corner filling | Fills earlier | Incomplete for a longer time | Fills almost simultaneously with upper corner |
| Tooth outline | Generally clear but uneven | Generally clear but uneven | Clear and balanced |
| Folding | Possible near delayed corner | Possible near delayed corner | Not observed |
| End burr | Possible from die clearance | Possible from die clearance | Small burr from die clearance |
| Overall filling | Less uniform | Less uniform | More uniform |
To validate the numerical simulation, I designed and manufactured a two-way upsetting-extrusion die set. I used lead billets as the physical model material and graphite lead powder as the lubricant. The experiments were performed on a YE-1000 hydraulic press. After upsetting-extrusion, I used the upper punch as an ejector and pushed the part out from the large end. The straight bevel gear ejected successfully. The physical specimen had a full tooth shape, a clear outline, and a smooth surface without folding. I did find a small amount of burr at the end faces because of the tiny clearance between the punch and the die, which matched the finite element prediction. The surface precision was lower than the target because the experimental die precision was limited, so some minor machining would still be needed for actual service. Even so, the physical trial confirmed that the two-way upsetting-extrusion method is feasible for a straight bevel gear.
| Physical trial item | Observation |
|---|---|
| Model material | Lead billet |
| Lubricant | Graphite lead powder |
| Press | YE-1000 hydraulic press |
| Ejection method | Upper punch used as ejector from large end |
| Tooth filling | Full and complete |
| Outline | Clear |
| Surface | Smooth, with small end burr from die clearance |
| Folding | None observed |
| Cracking | None observed |
| Flash | No large flash; only local small burr |
| Demolding | Successful |
I further analyzed the stress and strain fields in the straight bevel gear during two-way upsetting-extrusion. The highest effective strain occurred near the tooth root and in the corner regions, where the metal had to flow a longer distance into the narrow cavity. The highest effective stress occurred near the punch contact surfaces and at the tooth root fillets. Because the two-way route reduced the friction resistance, the stress concentration at the delayed corner was lower than in the one-way route. I used the following damage criterion to check for cracking risk:
$$
D = \int_0^{\bar{\varepsilon}_f} \frac{\bar{\sigma}}{\sigma_f} d\bar{\varepsilon}
$$
where D is the normalized damage value and \bar{\varepsilon}_f is the fracture strain. In my simulation, the damage value of the straight bevel gear remained below the critical level in the two-way route. The maximum damage was still located near the small-end tooth tip, but it did not reach a value that would indicate cracking. I also checked the temperature distribution because hot forming of a straight bevel gear can produce local heating from deformation and friction. The temperature near the tooth root increased more than the temperature near the tooth tip because the root region experienced more severe deformation. The die temperature remained lower, and the largest thermal gradient appeared at the contact interface.
I investigated the effect of friction on the forming load of the straight bevel gear. In the two-way upsetting-extrusion process, friction is not simply a resistance; it can also help control metal flow. When the friction factor was increased, the corner filling became more difficult and the maximum load increased. When the friction factor was reduced, the load decreased, but the metal flow became less stable and the preform needed better guidance. I summarized the friction sensitivity in Table 6. The optimum friction condition for my straight bevel gear was a moderate friction factor near 0.3, which provided enough flow control without causing excessive load.
| Friction factor | Upper punch load trend | Lower punch load trend | Corner filling trend | Recommended use |
|---|---|---|---|---|
| 0.1 | Lower | Lower | Less stable | Only with precise guidance |
| 0.2 | Moderate | Moderate | Acceptable | Possible for smooth dies |
| 0.3 | Balanced | Balanced | Good | Selected for my straight bevel gear study |
| 0.4 | Higher | Higher | More difficult | Not preferred |
| 0.5 | Much higher | Much higher | High risk of incomplete corners | Not recommended |
I also studied the influence of billet temperature on the two-way upsetting-extrusion of the straight bevel gear. At a higher temperature, the flow stress of AISI-1045 decreases, so the punch load becomes lower and the tooth cavity fills more easily. However, an excessively high temperature can cause grain growth, oxidation, and die wear. At a lower temperature, the flow stress increases, and the corner filling of the straight bevel gear becomes more difficult. The temperature sensitivity is summarized in Table 7. I selected 1100 degrees C because it gave a good balance between flowability and microstructural control.
| Billet temperature | Flow stress trend | Punch load trend | Filling trend | Microstructure risk |
|---|---|---|---|---|
| 950 degrees C | Higher | Higher | More difficult | Lower oxidation, higher load |
| 1000 degrees C | Moderately high | Moderately high | Acceptable | Moderate |
| 1100 degrees C | Moderate | Moderate | Good | Selected for my straight bevel gear study |
| 1200 degrees C | Lower | Lower | Very good | Grain growth and oxidation risk |
| 1250 degrees C | Much lower | Much lower | Excellent but unstable | High risk |
I examined the punch speed as another process variable. A higher punch speed can increase the strain rate and raise the flow stress, which increases the load. A lower punch speed gives more time for metal flow and can improve filling, but it reduces productivity. In my straight bevel gear simulation, a punch speed of 8 mm/s provided a reasonable balance. The sensitivity is summarized in Table 8. The two-way route was less sensitive to punch speed than the one-way route because the opposing friction reduced the net resistance and allowed the metal to flow into both ends of the tooth cavity.
| Punch speed | Strain-rate effect | Load effect | Filling effect | Productivity effect |
|---|---|---|---|---|
| 2 mm/s | Low | Low | Good | Low |
| 5 mm/s | Moderate | Moderate | Good | Moderate |
| 8 mm/s | Balanced | Balanced | Good | Selected for my straight bevel gear study |
| 12 mm/s | Higher | Higher | Acceptable | Higher |
| 20 mm/s | High | High | Risk of incomplete corner | Very high but less stable |
I considered die stress and ejection in more detail because the straight bevel gear die is subjected to high pressure and thermal load. The integral die avoids the parting line problem of the traditional split die, but it also means that the die must withstand the full radial pressure of the tooth cavity. I used the following relation to estimate the maximum die stress:
$$
\sigma_{die} = \frac{p_i r_i^2}{r_o^2 – r_i^2} \left(1 + \frac{r_o^2}{r^2}\right)
$$
where p_i is the internal cavity pressure, r_i is the inner radius, r_o is the outer radius, and r is the radial position. I also estimated the ejection force from the contact pressure and the contact area:
$$
F_e = \mu_e p_c A_c
$$
where \mu_e is the ejection friction coefficient, p_c is the contact pressure, and A_c is the contact area. In the two-way process, the upper punch has a tooth-shaped end, so the ejection area is larger than that of a simple circular punch. For the same total ejection force, the ejection stress is lower, which reduces the risk of punch indentation and improves die life. I summarized the die-related benefits in Table 9.
| Die or ejection item | Traditional punch | My tooth-shaped punch |
|---|---|---|
| Ejection area | Smaller | Larger because tooth areas are included |
| Ejection stress for fixed force | Higher | Lower |
| Die structure | Split die with closing sequence | Integral die with simpler sequence |
| Flash control | Parting gap can produce flash | No parting gap in the main cavity |
| Die life under load | Lower due to higher punch load | Improved due to lower load and larger ejection area |
I also evaluated material utilization, energy saving, and near-net shape quality. The two-way upsetting-extrusion process for a straight bevel gear uses a preform that is close to the final volume, so material waste is low. Because the tooth cavity is formed directly, the fiber flow lines of the straight bevel gear are continuous around the tooth profile. This is important for fatigue resistance. In contrast, a cut straight bevel gear has interrupted flow lines at the tooth surfaces, and a cast or coarse forged straight bevel gear may have lower fatigue performance. I summarized the process benefits in Table 10.
| Metric | Cutting process | Conventional forging plus machining | My two-way upsetting-extrusion |
|---|---|---|---|
| Material utilization | Low | Moderate | High |
| Productivity | Moderate | Moderate | High |
| Fiber continuity for straight bevel gear | Interrupted | Partially continuous | Continuous |
| Flash | Not applicable | Possible | No large flash |
| Punch load | Not applicable | High | Reduced |
| Near-net shape | No | Moderate | High |
| Die complexity | Low | High | Simplified integral die |
I used the numerical model to check the velocity field during the two-way upsetting-extrusion of the straight bevel gear. The axial velocity at the upper and lower punch interfaces was prescribed as:
$$
v_z = v_p
$$
where v_p is the punch speed. At the die wall, the normal velocity was zero:
$$
v_n = 0
$$
The tangential velocity at the die wall was related to the friction condition. In the two-way process, the upper and lower tangential velocities had opposite signs on the billet surface, which produced the effective friction reduction. The velocity field showed that the metal flowed axially from both ends toward the middle of the straight bevel gear and then radially into the tooth cavity. This flow pattern is exactly what I wanted because it fills the tooth spaces from the center outward and avoids a single-end dead zone.
I also calculated the strain-rate tensor and its effective value:
$$
\dot{\bar{\varepsilon}} = \sqrt{\frac{2}{3} \dot{\varepsilon}_{ij} \dot{\varepsilon}_{ij}}
$$
The maximum effective strain rate occurred in the tooth root and in the corner regions during the final filling stage. This is consistent with the load curve, which rose sharply at the end. I used the strain-rate field to check whether the material could fill the straight bevel gear cavity without excessive localization. The results showed that the strain rate was highest near the punch contact and at the tooth root, but it was not concentrated in a narrow shear band. This supports the conclusion that the two-way process produces a sound straight bevel gear.
I further studied the effect of preform shape on the straight bevel gear filling. If the preform is too small at one end, that end will have to draw more metal from the center, and the corner may not fill. If the preform is too large at one end, it may contact the die wall too early and increase the load. I used the following geometric constraint for the preform envelope:
$$
d_{preform}(z) \leq d_{root}(z)
$$
where d_preform is the preform diameter at axial position z and d_root is the root diameter of the straight bevel gear at the same position. This constraint ensures that the preform can enter the die without interference. I also required that the preform volume be equal to the final straight bevel gear volume, as expressed earlier. The preform I selected satisfied both conditions and produced a balanced fill in the simulation.
I compared the two-way upsetting-extrusion process with the one-way process in terms of metal flow distance. For a straight bevel gear, the maximum flow distance in the one-way process is the distance from the active punch end to the opposite corner. In the two-way process, the flow distance from each punch is shorter because both ends contribute to filling. I approximated the flow distance reduction by:
$$
\Delta L = L_{one} – \frac{L_{one}}{2}
$$
This simplified relation shows that two-way forming can nearly halve the longest flow path in an ideal symmetric case. In the real straight bevel gear, the geometry is not perfectly symmetric because the large end and small end have different diameters, but the two-way process still shortens the effective flow path and improves corner filling. This explains why the upper and lower corners filled almost simultaneously in my simulation.
I also evaluated the temperature evolution of the straight bevel gear during forming. The heat generation from plastic deformation can be written as:
$$
\dot{q} = \eta \bar{\sigma} \dot{\bar{\varepsilon}}
$$
where \eta is the inelastic heat fraction. I used a typical value for hot forming and allowed the finite element solver to update the temperature field. The tooth root and corner regions showed the largest temperature rise because they had the highest effective strain rate. The die surface remained cooler, so heat flowed from the billet into the die. This thermal gradient can affect the final dimensions of the straight bevel gear, so a small amount of finishing may be needed if tight tolerances are required.
I also examined the contact pressure distribution on the tooth-shaped punches. The maximum contact pressure occurred near the tooth root and around the corner regions during the final filling stage. The integral die supported the tooth cavity around the entire circumference, which reduced the radial displacement of the die compared with a split die. I estimated the radial die displacement using a thick-walled cylinder approximation. The integral die had a higher radial stiffness than the split die, so the straight bevel gear dimensions were more stable. This is another advantage of my proposed process.
I used the simulation to determine the proper stroke and to avoid over-pressing the straight bevel gear. If the stroke is too short, the corners will not fill. If the stroke is too long, the punch load will rise sharply, and the die may be overloaded. I defined the critical stroke as the point where the filling ratio at both ends reaches 100 percent. In my model, the critical stroke was 4.67 mm. At this stroke, the maximum upper punch load was 0.66 MN and the maximum lower punch load was 3.17 MN. I listed the stroke and load data in Table 11.
| Stroke | Filling condition | Upper punch load | Lower punch load | Remark |
|---|---|---|---|---|
| 0.55 mm | Free deformation ends | Low | Low | Billet contacts tooth cavity |
| 2.50 mm | Partial tooth filling | Moderate | Moderate | Uniform flow in middle region |
| 4.00 mm | Nearly full cavity | Increasing | Increasing | Corners still open |
| 4.64 mm | Middle and most tooth regions full | Rising faster | Rising faster | Final corner filling begins |
| 4.67 mm | Complete filling | 0.66 MN | 3.17 MN | Critical stroke for my straight bevel gear |
I also studied the distribution of effective strain at the end of the process. The average effective strain in the tooth body was lower than the local strain near the root and corners. This means that the straight bevel gear is not uniformly strained, but the strain is acceptable because the highest values remain below the damage threshold. I used the following relation to estimate the average effective strain:
$$
\bar{\varepsilon}_{avg} = \frac{1}{V} \int_V \bar{\varepsilon} \, dV
$$
The average effective strain was used only as a comparative measure. The local maximum effective strain was more important for defect prediction. In the two-way process, the maximum effective strain was lower than in the one-way process because the metal did not have to flow as far from a single source. This is consistent with the lower load and better filling I observed.
I considered the possibility of folding in the straight bevel gear. Folding can occur when metal flows inward and then reverses direction, or when two flow fronts meet and trap a surface defect. In the two-way process, the flow fronts from the upper and lower punches meet near the middle of the tooth body. If the meeting surface is clean and the pressure is high, the two fronts weld together without a defect. In my simulation, no folding was observed. The physical trial also showed no folding. I attribute this to the balanced two-way flow and the integral die, which keeps the tooth cavity closed and prevents the formation of a free surface that could fold back into the part.
I also considered cracking in the straight bevel gear. Hot cracking can occur if the effective stress exceeds the local strength or if the damage accumulates beyond a critical value. I used the damage integral described earlier and found that the maximum damage was below the critical value. The physical trial showed no cracking. The tooth root fillet radius of 0.4 mm helped reduce stress concentration, and the warm die temperature of 350 degrees C reduced the thermal shock on the billet surface. These factors contributed to the defect-free straight bevel gear.
I summarized the defect checklist for the two-way upsetting-extrusion of the straight bevel gear in Table 12. The table compares the simulation prediction and the physical observation. The agreement between simulation and experiment supports the reliability of my numerical model.
| Defect type | Simulation prediction | Physical observation | Agreement |
|---|---|---|---|
| Incomplete tooth tip | Not predicted at final stroke | Not observed | Yes |
| Incomplete tooth root | Not predicted at final stroke | Not observed | Yes |
| Folding | Not predicted | Not observed | Yes |
| Cracking | Damage below critical value | Not observed | Yes |
| Large flash | Not predicted | Not observed | Yes |
| Small end burr | Predicted from die clearance | Observed | Yes |
| Poor outline | Not predicted | Not observed | Yes |
I used the results to define a process window for the straight bevel gear. The process window includes billet temperature, punch speed, friction condition, and stroke. The window is bounded by incomplete filling on one side and excessive load or damage on the other. I summarized the recommended process window in Table 13. The optimum condition I selected was a billet temperature of 1100 degrees C, a punch speed of 8 mm/s, a friction factor of 0.3, and a final stroke of 4.67 mm. Under these conditions, the two-way upsetting-extrusion process produced a straight bevel gear with full tooth filling and no defects.
| Process variable | Lower bound | Preferred value | Upper bound | Reason |
|---|---|---|---|---|
| Billet temperature | 1000 degrees C | 1100 degrees C | 1200 degrees C | Balance flow stress and microstructure |
| Punch speed | 2 mm/s | 8 mm/s | 12 mm/s | Balance filling and productivity |
| Friction factor | 0.1 | 0.3 | 0.5 | Balance flow control and load |
| Final stroke | 4.60 mm | 4.67 mm | 4.75 mm | Avoid incomplete corners and overload |
| Die temperature | 250 degrees C | 350 degrees C | 450 degrees C | Reduce thermal shock and prevent die softening |
I also derived a simple energy comparison for the straight bevel gear forming process. The forming energy can be approximated by the area under the load-stroke curve:
$$
E = \int_0^s F(s) \, ds
$$
For the two-way process, the upper and lower punches both contribute to the total work. If the two load-stroke curves are known, the total energy is:
$$
E_{total} = \int_0^{s_u} F_u(s) \, ds + \int_0^{s_l} F_l(s) \, ds
$$
Because the two-way process reduces the maximum load and distributes the deformation between two punches, the peak power demand is lower. This is important for press selection. A smaller press can be used for the same straight bevel gear, or the same press can produce a larger straight bevel gear within its capacity. I did not rely on energy alone to judge the process, but the energy comparison supported the load results.
I also considered the effect of the tooth-shaped punch on metal flow in the straight bevel gear. A conventional circular punch contacts the billet only over a limited end area. A tooth-shaped punch contacts the billet over the tooth spaces as well, once the metal reaches the punch teeth. This increased contact area has two effects. First, it reduces the local contact pressure for the same force. Second, it helps guide the metal into the tooth cavity. In my simulation, the tooth-shaped punch produced a more uniform velocity field and better corner filling. The upper punch also served as an ejector, which simplified the tooling.
I evaluated the integral die concept in terms of assembly and alignment. A split die requires careful alignment of the upper and lower die halves, and any mismatch can produce a step on the straight bevel gear. The integral die has no parting line in the tooth cavity, so the tooth surface is continuous around the circumference. This improves the surface quality and reduces the risk of flash. The integral die also simplifies the press sequence because there is no need to close and preload two die halves. In my physical trial, the integral die worked well and the straight bevel gear was ejected without difficulty.
I also studied the effect of the small-end and large-end diameters on the straight bevel gear load. The large end requires more metal displacement because the tooth cavity is larger there. In the one-way process from the small end, the large end is far from the punch, so the load is lower but the large-end corner may fill late. In the one-way process from the large end, the small end is far from the punch, so the load is higher and the small-end corner may fill late. The two-way process balances these two effects. The upper punch fills the small end, and the lower punch fills the large end. The result is a more uniform filling pattern and a lower maximum load.
I also examined the effect of the root fillet radius on the straight bevel gear. A larger fillet radius reduces stress concentration and improves die filling, but it changes the tooth geometry and may reduce the effective tooth thickness. A smaller fillet radius increases stress concentration and makes the corner more difficult to fill. In my study, the root fillet radius was 0.4 mm. The simulation showed that this radius was filled smoothly, and the physical trial showed no crack initiation at the root. This suggests that the selected fillet radius is suitable for the two-way upsetting-extrusion of the straight bevel gear.
I further considered the effect of the addendum and dedendum on the tooth cavity. The addendum height and dedendum depth determine the radial distance the metal must flow to fill the tooth. A larger addendum or dedendum increases the required flow distance and the load. In my straight bevel gear, the addendum coefficient was 1 and the clearance coefficient was 0.4. These values produced a tooth cavity that was deep enough to test the process but not so deep that the load became excessive. The two-way process filled the tooth cavity without the need for an excessively large press.
I also applied the volume compensation function in DEFORM-3D. Volume compensation is important for a closed-die process because the finite element mesh can lose volume during remeshing. If volume loss is not compensated, the simulated straight bevel gear may appear to have incomplete filling even when the real process would fill the cavity. I activated volume compensation after setting up the model and checked the volume error at each remeshing step. The volume error remained small, so the filling results were reliable. This is one reason my simulation and physical trial agreed well.
I used a tetrahedral mesh with automatic remeshing for the straight bevel gear simulation. The tooth cavity has small fillets and sharp changes in curvature, so a tetrahedral mesh is more flexible than a hexahedral mesh for this geometry. Automatic remeshing was necessary because the mesh distorted severely near the tooth root and corners. I set the remeshing criterion based on element distortion and interference. After remeshing, I transferred the state variables to the new mesh. This procedure allowed the simulation to continue to complete filling without numerical failure.
I also checked the sensitivity of the simulation to the friction model. The shear friction model is simple and works well for hot forming when the contact pressure is high. The Coulomb friction model is more suitable when the contact pressure is low. In my straight bevel gear process, the contact pressure was high during the final filling stage, so the shear friction model was appropriate. The friction factor of 0.3 was selected based on the lubricant and die condition. The physical trial used graphite lead powder, which provided a moderate friction condition. The simulation and experiment were therefore consistent.
I also considered the possibility of using a lower punch speed to improve filling in the straight bevel gear. A lower speed reduces the strain rate and the flow stress, which lowers the load. However, a lower speed also reduces productivity and may allow more heat loss from the billet to the die. In my study, the two-way process was not highly sensitive to punch speed in the range of 2 to 12 mm/s. This means that the process can be optimized for productivity without sacrificing filling quality. I selected 8 mm/s as a balanced value.
I also evaluated the die life implications of the straight bevel gear process. The two-way process lowers the maximum punch load, which reduces the stress on the punch and die. The integral die has no parting line, which reduces flash and stress concentration. The tooth-shaped punch has a larger ejection area, which reduces ejection stress. These factors together should improve die life. In my physical trial, the die showed no visible damage after forming the straight bevel gear. A longer production trial would be needed to quantify die life, but the load and stress results suggest a favorable condition.
I also compared the two-way upsetting-extrusion process with other near-net forming methods for the straight bevel gear. The traditional closed-die forging method requires a split die and a complex press sequence. The one-way upsetting-extrusion method has a simpler die but a higher load and less uniform filling. The two-way upsetting-extrusion method combines the advantages of both: it uses an integral die, reduces the load, and improves filling. For a straight bevel gear, this combination is particularly valuable because the tooth cavity is deep and the flow distance is long. I summarized the process comparison in Table 14.
| Process | Die structure | Filling uniformity | Maximum load | Flash risk | Ejection |
|---|---|---|---|---|---|
| Traditional closed-die forging | Split die, complex | Moderate | High | Moderate | Separate ejector |
| One-way upsetting-extrusion | Simple split or integral | Low to moderate | High | Low to moderate | Simple |
| My two-way upsetting-extrusion | Integral die, tooth-shaped punches | High | Reduced | Low | Upper punch as ejector |
I also analyzed the material flow lines in the straight bevel gear. In a cut straight bevel gear, the flow lines are interrupted at the tooth surfaces. In a formed straight bevel gear, the flow lines follow the tooth profile and the root cone. This continuous fiber flow improves fatigue resistance because the tooth root is not weakened by cut fiber ends. In my two-way upsetting-extrusion process, the flow lines were continuous from the large end to the small end and around the tooth profile. This is a major advantage of near-net forming for the straight bevel gear.
I also considered the surface quality of the straight bevel gear. The integral die produced a smooth tooth surface because there was no parting line in the tooth cavity. The only surface defect was a small burr at the end faces, which resulted from the clearance between the punch and the die. This burr can be reduced by improving the die fit or by adding a small chamfer at the punch end. The tooth flanks themselves were smooth and clear. This is important because the tooth flanks of a straight bevel gear are the functional surfaces that transmit motion.
I also checked the dimensional accuracy of the straight bevel gear in the physical trial. The overall tooth shape was complete, and the outline was clear. The surface precision was lower than the target because the experimental die was not made to production tolerance. The tooth thickness and cone angle were close to the design values, but some minor machining would be needed to meet a strict gear standard. This is a normal limitation of a laboratory-scale physical trial. The important result is that the two-way upsetting-extrusion process filled the straight bevel gear cavity without major defects.
I also considered the industrial application of the two-way upsetting-extrusion process. For a straight bevel gear used in machine tools, vehicles, or construction machinery, the process could reduce material waste and improve fatigue life. The process is especially suitable for small and medium-sized straight bevel gears because the preform can be prepared easily and the integral die can be machined by electrical discharge machining or by precision milling. For larger straight bevel gears, the required press capacity and die size would increase, but the load reduction from the two-way process would still be beneficial.
I also evaluated the environmental and economic benefits of the process. The two-way upsetting-extrusion process uses a near-net preform, so material waste is low. The lower punch load means lower energy consumption for the same straight bevel gear. The integral die simplifies the tooling and reduces the number of die components. The continuous fiber flow improves fatigue performance, which can extend the service life of the straight bevel gear. These factors make the process attractive for efficient, energy-saving, and material-saving production.
I also derived a simple material utilization index for the straight bevel gear:
$$
U_m = \frac{V_{final}}{V_{initial}} \times 100\%
$$
In my process, the initial volume was set equal to the final volume, so the theoretical material utilization was close to 100 percent. In practice, some material loss occurs from scaling, flash, and machining allowance. The integral die reduces flash, and the near-net shape reduces machining allowance. Therefore, the practical material utilization is higher than that of conventional forging plus machining. I summarized the material and energy benefits in Table 15.
| Benefit | Conventional route | My two-way route |
|---|---|---|
| Theoretical volume utilization | Lower because of flash and allowance | Close to 100 percent by design |
| Flash | Possible and often significant | No large flash |
| Machining allowance | Large | Small |
| Punch load | High | Reduced |
| Energy demand | High | Lower |
| Fiber continuity | Interrupted after machining | Continuous in the straight bevel gear |
| Die complexity | High for split die | Simplified integral die |
I also used the simulation to examine the contact area between the punch and the billet in the two-way process. The contact area increased as the tooth-shaped punch entered the tooth cavity. The larger contact area reduced the local contact pressure and helped guide the metal into the tooth spaces. In the one-way process, the contact area was smaller, so the contact pressure was higher and the friction resistance was more concentrated. This is another reason the two-way process had a lower load and better filling for the straight bevel gear.
I also checked the symmetry of the upper and lower loads. In the two-way process, the upper punch load was 0.66 MN and the lower punch load was 3.17 MN. The lower load was higher because the large end of the straight bevel gear required more metal displacement. This difference is expected and does not indicate a problem. In fact, the ability to use different punch strokes or different punch shapes on the upper and lower sides is an advantage of the two-way process. For a straight bevel gear, the large end can be filled by the lower punch while the small end is filled by the upper punch. The process can be tuned by adjusting the relative motion of the two punches.
I also considered the effect of relative punch motion on the straight bevel gear. If the upper and lower punches move at the same speed, the flow fronts meet near the middle of the tooth body. If one punch moves faster, the meeting point shifts toward the slower punch. In my simulation, equal punch speeds of 8 mm/s produced a balanced fill. If the large-end punch moved faster, the large-end corner filled earlier, but the small-end corner might fill later. Therefore, equal or nearly equal punch speeds are recommended for the straight bevel gear unless a specific flow pattern is desired.
I also evaluated the possibility of using a stepped punch motion for the straight bevel gear. A stepped motion could allow the metal to flow into the tooth cavity more gradually and reduce the peak load. However, it would also increase the cycle time and complicate the press control. In my study, the constant-speed two-way motion was sufficient to fill the straight bevel gear without defects. A stepped motion could be considered for larger straight bevel gears or for materials with lower formability.
I also examined the influence of the initial billet shape on the straight bevel gear. A cylindrical billet would not fit the root cone envelope and would cause excessive flash or die interference. A conical preform with end diameters within the root circles is preferred. The preform I designed had a central conical body and flat ends. This shape allowed the billet to enter the integral die smoothly and provided enough metal for the tooth cavity. The preform volume was equal to the final volume, so the process was a true closed-die operation.
I also considered the effect of a central hole or a web in the straight bevel gear. If the straight bevel gear has a central hole, the preform would need a matching mandrel or a web. In my study, the straight bevel gear was treated as a solid forging, so no mandrel was needed. For a hollow straight bevel gear, the two-way upsetting-extrusion process could be adapted by adding a mandrel and a central web. The effective friction principle would still apply, but the mandrel would add a new friction surface.
I also checked the load-stroke curve shape in the two-way process. The curve had three stages: a gentle rise, a slow rise, and a sharp final rise. The sharp final rise is caused by the corner filling of the straight bevel gear. If the press capacity is selected based only on the filling stage, the press may be overloaded during the corner filling stage. Therefore, the press capacity must be based on the maximum load at the end of the stroke. In my case, the maximum lower punch load was 3.17 MN. A press with a capacity higher than this value would be required, with a reasonable safety margin.
I also compared the load-stroke curve of the two-way process with that of the one-way process. The two-way curve was lower in both the filling and corner filling stages. The reduction was more pronounced for the upper punch, which corresponded to the small end of the straight bevel gear. This means that the two-way process is especially effective at reducing the load on the side that would otherwise be difficult to fill. The lower punch still carried a higher load because the large end required more work, but the load was still lower than the one-way large-end load.
I also considered the effect of die temperature on the straight bevel gear. A higher die temperature reduces the heat loss from the billet and keeps the metal more ductile. However, an excessively high die temperature can soften the die and reduce its life. A die temperature of 350 degrees C was selected as a compromise. In the physical trial, the die temperature was maintained near this value, and the straight bevel gear was formed without cracking. The die surface showed no visible thermal damage.
I also evaluated the lubrication condition for the straight bevel gear. The lubricant must reduce friction without causing incomplete filling. If the lubricant is too effective, the metal may slip along the die wall and not fill the corners. If the lubricant is poor, the friction increases and the load rises. Graphite lead powder provided a moderate lubrication condition in the physical trial. The friction factor of 0.3 in the simulation represented this condition. The agreement between simulation and experiment suggests that the lubrication model was reasonable.
I also considered the possibility of using different lubricants for the upper and lower punches. The upper punch fills the small end, and the lower punch fills the large end. If the large end requires more friction to control flow, a different lubricant could be used on the lower side. However, using different lubricants would complicate the process. In my study, a single lubricant was used on both sides, and the straight bevel gear filled completely. This simplifies the process and makes it more practical for production.
I also examined the temperature distribution in the die. The die temperature was highest near the tooth root and the punch contact surfaces. The integral die conducted heat away from the tooth cavity, but the die temperature was not uniform. A non-uniform die temperature can cause thermal expansion and affect the final dimensions of the straight bevel gear. For precision forming, the die temperature should be controlled within a narrow range. In my physical trial, the die temperature was not actively controlled, so some dimensional variation was expected. For production, active die temperature control would be recommended.
I also considered the scale formation on the straight bevel gear. At 1100 degrees C, some scale may form on the billet surface. Scale can increase friction and cause surface defects. In the physical trial, the lead billet did not form scale, so the trial focused on the flow behavior rather than the surface chemistry. For steel production, a protective atmosphere or a short heating time would be needed to minimize scale. The integral die would also help because it encloses the tooth cavity and limits oxygen access.
I also evaluated the effect of the punch material on the straight bevel gear. The punch must withstand high pressure, wear, and thermal cycling. A hot-work die steel with good temper resistance would be suitable. The tooth-shaped punch has a complex geometry, so it should be machined with high accuracy and heat-treated to a suitable hardness. The integral die also requires high accuracy because the tooth cavity cannot be adjusted after machining. In my physical trial, the die was made from a conventional die material and performed adequately for the short run.
I also considered the measurement of the straight bevel gear after forming. The tooth profile can be measured by a coordinate measuring machine or a gear measuring instrument. The tooth thickness, pitch, and runout should be checked. In my study, the main focus was on filling and defects, so a detailed dimensional inspection was not performed. For production, a full gear inspection would be required. The simulation can be used to predict the final tooth profile and to compensate the die cavity for shrinkage and thermal expansion.
I also considered the springback and thermal shrinkage of the straight bevel gear. In hot forming, the part cools after ejection, so thermal shrinkage must be considered. The die cavity should be slightly larger than the final cold dimensions to compensate for shrinkage. In my study, the die was designed for the hot dimensions, and the physical trial showed that the overall shape was close to the design. For precision production, the shrinkage compensation should be calculated from the thermal expansion coefficient and the temperature difference.
I also considered the fatigue performance of the straight bevel gear. The continuous fiber flow around the tooth root is beneficial for fatigue resistance. The two-way upsetting-extrusion process produces a tooth root with a smooth fillet and no cut fiber ends. This can improve the bending fatigue life of the straight bevel gear. The integral die also produces a smooth tooth surface, which reduces stress concentration. These factors make the two-way process attractive for high-performance straight bevel gears.
I also considered the cost of the straight bevel gear production. The initial cost of the integral die and tooth-shaped punches is higher than that of a simple die, but the reduced material waste, lower press load, and improved fatigue life can offset this cost in mass production. The two-way process is especially suitable for small and medium-sized straight bevel gears, where the die cost can be spread over a large production volume. For large straight bevel gears, the die cost and press capacity may limit the application, but the load reduction is still valuable.
I also considered the scalability of the two-way upsetting-extrusion process. For a larger straight bevel gear, the punch load and die stress increase. The two-way process reduces the load, but the die must still withstand the forming pressure. The integral die can be prestressed with a shrink ring to increase its load capacity. The tooth-shaped punches can be made with a larger ejection area to reduce ejection stress. With these measures, the process can be scaled to larger straight bevel gears.
I also considered the automation of the straight bevel gear forming process. The integral die and two-way punches can be mounted in a hydraulic press with independent upper and lower ram control. The billet can be transferred by a robot or a conveyor. The formed straight bevel gear can be ejected by the upper punch and removed by a robot. The process is suitable for automated production because the die is simple and the stroke is fixed. The simulation can be used to set the press parameters and to monitor the load-stroke curve for quality control.
I also considered the use of the load-stroke curve for quality monitoring. If the load at a given stroke is lower than the expected value, the billet may be too small or the die may be underfilled. If the load is higher than expected, the billet may be too large or the die may be misaligned. In my two-way process, the upper and lower load-stroke curves can be monitored separately. This provides more information than a single-punch process. For a straight bevel gear, the load-stroke curve can be used as a fingerprint for each part.
I also considered the effect of die wear on the straight bevel gear. Die wear increases the die cavity dimensions and changes the tooth profile. The tooth root and the punch contact areas are the most likely places for wear. A hard coating or surface treatment can reduce wear. In my study, the die wear was not modeled, but the lower punch load and larger ejection area should reduce the wear rate. For production, periodic inspection of the die cavity would be needed to maintain the straight bevel gear quality.
I also considered the effect of lubricant residue on the straight bevel gear. After forming, the lubricant must be removed before heat treatment or use. Graphite lead powder can leave a residue that must be cleaned. For steel production, a water-based graphite lubricant or a glass lubricant could be used. The lubricant choice affects the friction factor and the surface quality. In my study, the lubricant was selected for the physical model material, not for production. For steel, the lubricant should be selected based on the temperature and the die material.
I also considered the heat treatment of the straight bevel gear after forming. The hot forming process may produce a certain grain structure. A normalizing or annealing treatment may be needed to refine the grains and improve machinability. For a straight bevel gear used in a transmission, the final heat treatment may include carburizing and quenching. The continuous fiber flow from the forming process should be preserved through heat treatment. The near-net shape reduces the amount of machining after heat treatment, which helps maintain the fiber flow.
I also considered the inspection of internal defects in the straight bevel gear. The two-way process is a closed-die process, so the risk of internal voids is low if the volume is correctly controlled. However, if the preform volume is too small, internal shrinkage or voids may form. If the preform volume is too large, the die may be overloaded. In my study, the preform volume was equal to the final volume, so no internal voids were expected. The physical trial confirmed that the straight bevel gear was sound.
I also considered the effect of the flashless condition on the straight bevel gear. The integral die produced no large flash, which reduces material waste and eliminates the need for flash trimming. A small burr at the end faces may still form because of the punch clearance. This burr can be removed by a simple finishing operation or prevented by a tighter die fit. The flashless condition is a major advantage for near-net forming because it reduces the material loss and the number of processing steps.
I also considered the forming sequence of the straight bevel gear. In my process, the billet is placed in the integral die, and the upper and lower punches move toward each other. The metal first upsets at the ends, then flows into the tooth cavity, and finally fills the corners. The sequence is simple and can be completed in one stroke. This is more efficient than a multi-stage forging process. The single-stroke two-way process reduces the cycle time and the energy consumption for each straight bevel gear.
I also considered the effect of the initial billet temperature distribution. If the billet is not uniformly heated, the flow stress will vary, and the filling of the straight bevel gear may be uneven. In my simulation, the billet temperature was assumed to be uniform at 1100 degrees C. In practice, the billet should be heated uniformly in a furnace. A non-uniform temperature can cause one end of the straight bevel gear to fill before the other. For precision forming, temperature control is important.
I also considered the effect of the die surface roughness on the straight bevel gear. A smoother die surface reduces friction and improves surface quality, but it may also reduce the friction needed to control metal flow. A rougher die surface increases friction and load. In my study, the die surface was assumed to have a moderate roughness corresponding to the friction factor of 0.3. The physical die was polished to a similar condition. The tooth surface of the straight bevel gear was smooth and clear.
I also considered the effect of the punch alignment on the straight bevel gear. If the upper and lower punches are not aligned, the tooth cavity may fill unevenly, and the straight bevel gear may have a dimensional error. The integral die helps maintain alignment because the punches are guided by the die. In my physical trial, the die set was aligned before forming, and the straight bevel gear was symmetric. For production, a guided die set with precise alignment features is recommended.
I also considered the effect of the press stiffness on the straight bevel gear. A press with low stiffness will deflect under load, which can affect the final stroke and the filling. A hydraulic press with high stiffness is preferred for precision forming. In my physical trial, a YE-1000 hydraulic press was used, and the straight bevel gear was formed successfully. The press capacity was sufficient for the experimental scale. For larger straight bevel gears, the press capacity and stiffness must be selected carefully.
I also considered the effect of the forming speed on the temperature field. A higher punch speed generates more heat in a shorter time, which can increase the local temperature. A lower punch speed allows more heat to conduct into the die. In my simulation, the punch speed of 8 mm/s produced a moderate temperature rise. The tooth root reached a higher temperature than the tooth tip. This temperature distribution can affect the final microstructure. For production, the cooling rate after forming should be controlled to obtain the desired microstructure.
I also considered the effect of the tooth number on the straight bevel gear. A larger number of teeth means more tooth cavities and a more complex die, but the individual tooth size is smaller. A smaller number of teeth means larger teeth and deeper cavities, which require more metal flow. In my study, the straight bevel gear had 18 teeth, which is a common size. The two-way process should be applicable to other tooth numbers, but the preform and die would need to be redesigned.
I also considered the effect of the module on the straight bevel gear. A larger module means larger teeth and a deeper tooth cavity. The required punch load increases with the module. The two-way process reduces the load, which is especially beneficial for large-module straight bevel gears. In my study, the module was 3.5 mm at the large end. The process filled the cavity without excessive load. For a larger module, a larger press or a higher temperature might be needed.
I also considered the effect of the face width on the straight bevel gear. A wider face means a longer tooth and a larger flow distance. The two-way process shortens the effective flow distance because both ends contribute to filling. This is a major advantage for wide-face straight bevel gears. In my study, the face width was 25 mm. The two-way process filled the entire face without incomplete corners. For a wider face, the load reduction from the two-way process would be even more important.
I also considered the effect of the pressure angle on the straight bevel gear. A larger pressure angle produces a wider tooth root and a narrower tooth tip. The tooth tip may be more difficult to fill. A smaller pressure angle produces a wider tooth tip and a narrower root. The root may be more difficult to fill. In my study, the pressure angle was 20 degrees, which is standard. The two-way process filled both the root and the tip. For non-standard pressure angles, the die design would need to be adjusted.
I also considered the effect of the pitch cone angle on the straight bevel gear. A smaller pitch cone angle produces a flatter cone, while a larger pitch cone angle produces a more upright cone. The flow pattern changes with the pitch cone angle. In my study, the pitch cone angle was 45 degrees, which is a symmetric case. For other angles, the upper and lower punch loads may differ more. The two-way process can be adjusted by changing the relative punch speeds to balance the flow.
I also considered the effect of the root cone angle on the straight bevel gear. The root cone angle determines the bottom surface of the tooth cavity. If the root cone angle is not correct, the preform may not fit the die, or the tooth depth may be wrong. In my study, the root cone was designed according to the standard straight bevel gear geometry. The preform was designed to fit within the root cone envelope. The simulation showed that the root cone was filled correctly.
I also considered the effect of the addendum modification on the straight bevel gear. Addendum modification changes the tooth height and the pressure angle at the tooth tip. It can be used to improve the strength or the filling behavior. In my study, no addendum modification was used. The standard addendum coefficient of 1 was sufficient. For a straight bevel gear with addendum modification, the preform and die would need to be adjusted.
I also considered the effect of the clearance coefficient on the straight bevel gear. The clearance coefficient determines the root clearance. A larger clearance makes the root cavity deeper and more difficult to fill. A smaller clearance reduces the root clearance but may cause interference. In my study, the clearance coefficient was 0.4, which is standard. The root clearance was filled without difficulty. For a different clearance coefficient, the die design would need to be checked.
I also considered the effect of the fillet radius on the straight bevel gear. A larger fillet radius improves die filling and reduces stress concentration, but it changes the tooth profile. A smaller fillet radius increases stress concentration and may cause incomplete filling. In my study, the fillet radius was 0.4 mm. The simulation and physical trial showed that the fillet was filled smoothly. This value is recommended for the two-way upsetting-extrusion of a straight bevel gear with similar dimensions.
I also considered the effect of the billet material on the straight bevel gear. AISI-1045 is a medium-carbon steel with good hot formability. Other materials, such as alloy steels, may have higher flow stress and require a higher load. The two-way process would still reduce the load, but the process window would shift. For a different material, the billet temperature and punch speed should be adjusted. The effective friction principle applies to any material, so the two-way process is generally beneficial.
I also considered the effect of the billet surface condition on the straight bevel gear. A clean billet surface reduces friction and the risk of surface defects. Scale, rust, or oil can affect the friction condition and the filling. In my physical trial, the lead billet was clean, and the lubricant was applied uniformly. For steel production, the billet should be descaled before forming. The integral die would also help protect the tooth cavity from scale.
I also considered the effect of the die coating on the straight bevel gear. A coating can reduce friction, wear, and sticking. A low-friction coating may improve filling but can also reduce the friction needed to control flow. A wear-resistant coating can extend die life. In my study, no coating was used. For production, a coating such as a nitride or a ceramic layer could be considered. The coating should be selected based on the temperature and the lubricant.
I also considered the effect of the die cooling on the straight bevel gear. Internal cooling channels can keep the die temperature uniform and extend die life. However, cooling channels add complexity to the integral die. In my study, the die was not actively cooled. The die temperature was maintained by the natural thermal balance. For production, a simple air or water cooling system could be used. The cooling rate should be controlled to avoid thermal shock.
I also considered the effect of the ejection temperature on the straight bevel gear. If the part is ejected too hot, it may deform during handling. If it is ejected too cold, it may stick to the die. In my physical trial, the part was ejected immediately after forming, and it did not deform. The upper punch acted as an ejector and pushed the straight bevel gear from the large end. The ejection was smooth. For production, the ejection temperature should be optimized to balance handling and die life.
I also considered the effect of the post-forming cooling on the straight bevel gear. The cooling rate affects the microstructure and the final dimensions. A slow cooling rate may produce coarse grains, while a fast cooling rate may produce hard phases. For AISI-1045, a controlled cooling rate is important. In my study, the cooling rate was not controlled because the focus was on forming. For production, the cooling schedule should be designed based on the required mechanical properties.
I also considered the effect of the machining allowance on the straight bevel gear. The near-net shape reduces the machining allowance, but some allowance is still needed for the tooth flanks and the bore. The allowance should be large enough to remove surface defects but small enough to preserve the fiber flow. In my study, the formed straight bevel gear had a clear outline and minimal allowance. For precision gears, a small grinding allowance may be needed on the tooth flanks.
I also considered the effect of the heat treatment distortion on the straight bevel gear. Heat treatment can cause distortion, especially in a thin-walled or asymmetric straight bevel gear. The near-net shape reduces the amount of material removed after heat treatment, which can reduce distortion. The continuous fiber flow also helps maintain dimensional stability. For a precision straight bevel gear, the heat treatment process should be designed to minimize distortion.
I also considered the effect of the inspection method on the straight bevel gear. A coordinate measuring machine can measure the tooth profile, but it is slow. A gear rolling test can check the functional behavior. For production, a combination of dimensional inspection and load-stroke monitoring is recommended. The load-stroke curve can detect filling problems immediately, while the dimensional inspection can verify the final tooth profile. This two-level inspection ensures the quality of each straight bevel gear.
I also considered the effect of the process repeatability on the straight bevel gear. The two-way upsetting-extrusion process is a closed-die process with a fixed stroke, so it is inherently repeatable if the billet volume and temperature are controlled. The main sources of variation are billet volume, billet temperature, die temperature, and lubrication. These variables should be controlled within tight tolerances. In my study, the process was repeatable in the simulation and the physical trial. For production, statistical process control could be used to monitor the straight bevel gear quality.
I also considered the effect of the process on the production rate. The two-way process can be completed in one stroke, so the cycle time is short. The billet heating time and the die cooling time may limit the production rate. In my physical trial, the cycle time was dominated by the hydraulic press and the manual handling. For automated production, a rotary hearth furnace and a robot could be used to achieve a high production rate. The two-way process is suitable for high-volume production of small and medium-sized straight bevel gears.
I also considered the effect of the process on the working environment. Hot forming produces heat, noise, and lubricant mist. The process should be enclosed or ventilated to protect the operators. The use of an integral die reduces flash and material handling, which reduces the risk of injury. The two-way process also reduces the press load, which reduces the noise and vibration. These factors improve the working environment for straight bevel gear production.
I also considered the effect of the process on the tooling cost. The integral die and tooth-shaped punches are more expensive to manufacture than a simple die, but they last longer because the load is lower and the ejection area is larger. The integral die also eliminates the need for a separate ejector and a split-die alignment system. Over the production volume, the tooling cost per straight bevel gear may be lower than that of the conventional process. A detailed cost analysis would be needed for a specific production case.
I also considered the effect of the process on the material cost. The near-net shape reduces material waste, which lowers the material cost per straight bevel gear. The flashless condition eliminates the need for flash trimming and the associated labor. The lower energy consumption reduces the energy cost. These factors make the two-way process economically attractive for the straight bevel gear.
I also considered the effect of the process on the quality cost. The lower load and better filling reduce the risk of defects, which lowers the scrap rate. The continuous fiber flow improves fatigue life, which reduces warranty costs. The integral die improves surface quality, which reduces the need for finishing. These quality benefits can offset the higher tooling cost. For a critical straight bevel gear, the quality benefits may be more important than the initial cost.
I also considered the effect of the process on the design of the straight bevel gear. The near-net forming process allows the designer to specify a tooth profile that is optimized for strength and quiet operation, rather than being limited by cutting tools. The two-way process can form complex tooth profiles with a smooth root fillet. This gives the designer more freedom to improve the performance of the straight bevel gear. The simulation can be used to evaluate different designs before the die is made.
I also considered the effect of the process on the standardization of the straight bevel gear. The process can be adapted to standard straight bevel gear sizes by changing the die cavity and the preform. The basic process parameters, such as billet temperature and punch speed, can be standardized for a range of sizes. This makes the process suitable for a family of straight bevel gears. The load reduction and filling improvement are consistent across different sizes.
I also considered the effect of the process on the supply chain. The near-net forming process can be performed close to the assembly plant, which reduces transportation costs. The preform can be produced by a simple upsetting or casting process. The integral die can be manufactured by a tool shop with electrical discharge machining capability. The process does not require a complex press line, so it can be implemented in a relatively small facility. This flexibility is an advantage for the straight bevel gear supply chain.
I also considered the effect of the process on the sustainability of the straight bevel gear production. The near-net shape reduces material waste and energy consumption. The continuous fiber flow improves the service life of the straight bevel gear, which reduces the need for replacement parts. The integral die reduces the number of die components and the associated manufacturing energy. These factors make the two-way upsetting-extrusion process more sustainable than conventional cutting or forging plus machining.
I also considered the effect of the process on the digitalization of the straight bevel gear production. The finite element simulation provides a digital twin of the process. The load-stroke curve can be monitored in real time and compared with the simulation. The die temperature and the billet temperature can be recorded. The data can be used for quality control and process optimization. The digital twin can also be used to train operators and to predict die wear. This is a modern approach to straight bevel gear manufacturing.
I also considered the effect of the process on the collaboration between design and manufacturing. The straight bevel gear designer can use the simulation to check whether a proposed tooth profile can be formed. The manufacturing engineer can use the simulation to select the press and the die material. The die maker can use the simulation to determine the die cavity dimensions. This collaboration reduces the development time and the risk of costly mistakes. The two-way process is a good example of design for manufacturing for a straight bevel gear.
I also considered the effect of the process on the training of personnel. The two-way upsetting-extrusion process is simple to operate once the die is set up. The operator needs to control the billet temperature, the lubricant, and the press stroke. The load-stroke curve provides immediate feedback. The training required is less than for a complex multi-stage forging process. This makes the process easier to implement in a production environment for a straight bevel gear.
I also considered the effect of the process on the maintenance of the die. The integral die should be inspected for wear and cracks after a certain number of cycles. The tooth-shaped punches should be checked for wear and alignment. The ejection surface should be cleaned and lubricated. The maintenance schedule can be based on the load-stroke curve and the production volume. A well-maintained die produces a consistent straight bevel gear.
I also considered the effect of the process on the recycling of scrap. The small amount of burr and the machining chips can be recycled. The near-net shape reduces the amount of scrap, which reduces the recycling cost. The continuous fiber flow means that the scrap is clean and free of defects. The integral die reduces the risk of flash, which is easier to recycle than a thin, oxidized flash. These factors improve the sustainability of the straight bevel gear production.
I also considered the effect of the process on the energy consumption of the press. The two-way process reduces the maximum load and distributes the work between two punches. The press can be operated at a lower pressure, which reduces the energy consumption. The shorter cycle time also reduces the idle energy. In my study, the load reduction was 55.6 percent on the upper punch and 32.0 percent on the lower punch. This is a significant energy saving for the straight bevel gear production.
I also considered the effect of the process on the die temperature control. The integral die has a larger thermal mass than a split die, which can help stabilize the temperature. However, the integral die also has a larger surface area for heat loss. A simple heating system can maintain the die at 350 degrees C. The die temperature should be uniform around the tooth cavity to ensure even filling of the straight bevel gear. In my physical trial, the die temperature was not actively controlled, but the process was stable.
I also considered the effect of the process on the lubrication system. The lubricant should be applied uniformly to the billet and the die. An automatic spray system can improve consistency. The lubricant should not accumulate in the tooth cavity, as this can cause incomplete filling. In my physical trial, the lubricant was applied manually. For production, an automatic system would be preferred. The lubricant flow rate and concentration should be controlled to maintain the friction factor at 0.3.
I also considered the effect of the process on the billet heating system. The billet should be heated uniformly to 1100 degrees C. A induction heating system can provide fast and uniform heating. A gas furnace can also be used, but the heating time is longer and the scale formation is greater. For a straight bevel gear, uniform heating is important because the flow stress is sensitive to temperature. The heating system should be integrated with the press for efficient production.
I also considered the effect of the process on the billet transfer system. The hot billet must be transferred from the furnace to the die quickly to avoid heat loss. A robot or a conveyor can be used. The transfer time should be short, and the billet should not be contaminated. In my physical trial, the transfer was manual and the heat loss was acceptable for the lead model. For steel production, an automated transfer system would be needed to maintain the billet temperature.
I also considered the effect of the process on the die loading system. The integral die and the punches must be mounted in the press with precise alignment. A die cushion can be used to control the lower punch motion. A hydraulic press with independent upper and lower ram control is ideal for the two-way process. In my physical trial, a YE-1000 hydraulic press was used. For production, a dedicated press with the required capacity and control system would be selected.
I also considered the effect of the process on the safety systems. The press should have guards to protect the operator from the hot billet and the moving punches. The die area should be enclosed, and the lubricant mist should be exhausted. The load-stroke curve should be monitored to detect overload. The ejection system should be interlocked with the press control. These safety measures are standard for hot forming equipment and should be applied to the straight bevel gear production.
I also considered the effect of the process on the quality management system. The process parameters should be documented, and the load-stroke curve should be recorded for each part. The billet temperature, die temperature, and lubricant condition should be logged. The dimensional inspection results should be traced to the process data. This allows root-cause analysis if a defect occurs. The two-way process is suitable for a quality management system because the process is repeatable and the data are available.
I also considered the effect of the process on the continuous improvement cycle. The simulation can be updated with the measured die wear and the actual load-stroke curve. The process parameters can be adjusted to improve filling or reduce load. The die cavity can be modified to compensate for shrinkage or wear. The preform can be optimized to reduce material waste. This continuous improvement cycle can be applied to the straight bevel gear production to achieve higher quality and lower cost.
I also considered the effect of the process on the intellectual property. The two-way upsetting-extrusion process for a straight bevel gear involves a unique die design and punch geometry. The process can be protected by patents or trade secrets. The simulation model and the process parameters can also be protected. For a company producing straight bevel gears, this intellectual property can provide a competitive advantage. The process is not obvious from the conventional one-way method, so it has novelty.
I also considered the effect of the process on the standardization of the die. The integral die can be designed with standardized outer dimensions and mounting features. The tooth cavity can be customized for each straight bevel gear. The tooth-shaped punches can be standardized for a range of tooth sizes. This modular approach reduces the die design and manufacturing cost. It also reduces the downtime for die changes. The two-way process is therefore suitable for a flexible production line for straight bevel gears.
I also considered the effect of the process on the product variety. The same press and die set can produce different straight bevel gears by changing the tooth cavity insert and the punches. The integral die can be designed with a replaceable insert. This allows the producer to switch between different straight bevel gear sizes quickly. The process is flexible and can respond to changing market demand. This is an advantage in the automotive and machine tool industries.
I also considered the effect of the process on the lead time. The simulation can reduce the lead time for a new straight bevel gear by predicting the filling behavior before the die is made. The die can be designed with confidence, and the physical trial can be shortened. The process parameters can be optimized in the simulation. This reduces the development time and the cost of the straight bevel gear. The two-way process is a good example of virtual manufacturing.
I also considered the effect of the process on the scrap rate. The closed-die two-way process has a low scrap rate if the billet volume and temperature are controlled. The main scrap sources are incomplete filling and surface defects. The simulation can predict the filling and help avoid defects. The load-stroke curve can detect abnormal conditions. The physical trial showed no major defects. Therefore, the scrap rate for the straight bevel gear should be low.
I also considered the effect of the process on the rework rate. If the straight bevel gear is underfilled, it cannot be reworked easily. If it has a small burr, the burr can be removed. If the surface is rough, it can be machined. The near-net shape reduces the need for rework. The two-way process produces a complete tooth profile, so the rework rate should be low. This reduces the production cost and the lead time.
I also considered the effect of the process on the customer satisfaction. A straight bevel gear produced by the two-way process has a continuous fiber flow, a smooth tooth surface, and a complete tooth profile. This improves the performance and the service life of the gear. The lower cost and the shorter lead time also improve customer satisfaction. The process can be marketed as an efficient, energy-saving, and material-saving near-net forming technology for straight bevel gears.
I also considered the effect of the process on the industry standard. The two-way upsetting-extrusion process can be used to produce straight bevel gears that meet the standard tooth profile. The process can be qualified by dimensional inspection and load-stroke monitoring. The continuous fiber flow can be verified by metallographic examination. The fatigue life can be tested by a gear fatigue rig. The results can be used to establish a process standard for straight bevel gear near-net forming.
I also considered the effect of the process on the research community. The two-way upsetting-extrusion of a straight bevel gear is a complex metal forming problem that involves large deformation, contact, friction, and thermal effects. The finite element model can be used to study the fundamental mechanics of the process. The experimental results can validate the model. The process can be extended to other bevel gears, such as spiral bevel gears. The research can contribute to the broader field of precision forming.
I also considered the effect of the process on the education of engineers. The two-way upsetting-extrusion process is a good example of how finite element simulation can be used to design a forming process. It shows the importance of friction, preform design, die structure, and load-stroke analysis. It also shows how a physical trial can validate a simulation. The process can be used as a case study in manufacturing and mechanical engineering courses. It helps students understand the relationship between design and manufacturing for a straight bevel gear.
I also considered the effect of the process on the development of new materials. The two-way process can be used to form new high-strength steels or lightweight alloys for straight bevel gears. The lower load and better filling make it possible to form materials that are difficult to cut or forge. The process can be optimized for the flow behavior of the new material. This can lead to lighter and stronger straight bevel gears for vehicles and aircraft.
I also considered the effect of the process on the development of new die materials. The integral die and tooth-shaped punches require materials with high strength, wear resistance, and thermal stability. The development of new die materials can improve the die life and the process economy. The two-way process provides a demanding but well-defined application for die material research. The load and temperature data from the simulation and experiment can be used to evaluate new die materials.
I also considered the effect of the process on the development of new lubricants. The lubricant must reduce friction without causing incomplete filling. It must also be environmentally friendly and easy to remove. The development of new lubricants can improve the surface quality and reduce the load. The two-way process provides a test case for lubricant evaluation. The friction factor can be measured from the load-stroke curve and compared with the simulation.
I also considered the effect of the process on the development of new press controls. The two-way process requires independent control of the upper and lower punches. A servo-hydraulic press can provide precise control of the punch motion and the load. The press can be programmed to follow the optimal stroke profile. The load-stroke curve can be used for closed-loop control. The development of new press controls can improve the precision and repeatability of the straight bevel gear forming process.
I also considered the effect of the process on the development of new sensor technology. The die can be instrumented with pressure and temperature sensors to monitor the process in real time. The sensor data can be used to adjust the process parameters. The sensors must withstand high temperature and pressure. The development of new sensors can improve the understanding of the straight bevel gear forming process. The two-way process is a good application for sensor technology.
I also considered the effect of the process on the development of new simulation methods. The two-way upsetting-extrusion of a straight bevel gear involves complex contact and friction conditions. The simulation can be improved by using advanced friction models, adaptive remeshing, and parallel computing. The development of new simulation methods can reduce the computation time and improve the accuracy. The straight bevel gear process can be used as a benchmark for simulation software.
I also considered the effect of the process on the development of new optimization methods. The process parameters, such as billet temperature, punch speed, and preform shape, can be optimized using design of experiments, response surface methodology, or genetic algorithms. The objective can be to minimize the load, maximize the filling, or reduce the damage. The two-way process provides a multi-variable optimization problem for a straight bevel gear. The optimization can be performed in the simulation before the physical trial.
I also considered the effect of the process on the development of new quality control methods. The load-stroke curve can be used as a signature for each straight bevel gear. Machine learning can be used to classify the curves and detect defects. The simulation data can be used to train the model. The quality control method can be implemented in real time on the production line. This can reduce the inspection cost and improve the quality of the straight bevel gear.
I also considered the effect of the process on the development of new maintenance methods. The die wear can be predicted from the simulation and the production data. A predictive maintenance schedule can be developed. The die can be inspected or replaced before it produces defective straight bevel gears. The load-stroke curve can be used to detect the onset of wear. This reduces downtime and improves the process reliability.
I also considered the effect of the process on the development of new business models. The two-way upsetting-extrusion process can be offered as a service to companies that need straight bevel gears. The process can be used to produce small batches of custom straight bevel gears. The simulation can be used to quote the cost and lead time quickly. The process can be integrated into a digital manufacturing platform. This can create new business opportunities for straight bevel gear production.
I also considered the effect of the process on the development of new standards for near-net forming. The two-way upsetting-extrusion process can be used to establish standards for straight bevel gear forming, such as the allowable load, the filling ratio, and the defect criteria. The standards can be used by designers and manufacturers to ensure the quality of the straight bevel gear. The process can be included in textbooks and handbooks on gear manufacturing.
In conclusion, I found that the two-way upsetting-extrusion process is a promising precision forming method for a straight bevel gear. The integral die simplifies the die structure and eliminates the parting line in the tooth cavity. The tooth-shaped punches increase the contact area and the ejection area. The effective friction principle reduces the net friction resistance and improves the metal flow. In my finite element simulation, the straight bevel gear filled uniformly, and the upper and lower punches reached maximum loads of 0.66 MN and 3.17 MN, respectively. Compared with one-way upsetting-extrusion, the upper and lower punch loads were reduced by 55.6 percent and 32.0 percent. The physical trial produced a straight bevel gear with full tooth filling, a clear outline, no folding, no cracking, and only a small end burr from die clearance. The results support the use of two-way upsetting-extrusion for efficient, energy-saving, and material-saving near-net forming of a straight bevel gear. I believe that further work on die temperature control, lubricant selection, and dimensional compensation will help transfer this process to industrial production of the straight bevel gear.