
In modern mechanical transmissions, spiral bevel gears play a critical role due to their ability to transmit power smoothly and efficiently between intersecting shafts. The demand for high-performance spiral bevel gears with enhanced durability, precision, and load capacity has driven the development of hard tooth surface machining techniques. From my perspective as a researcher in gear technology, I find that the transition to hard tooth surfaces—typically achieved through carburizing, quenching, or nitriding to reach hardness levels above 58 HRC—presents both opportunities and challenges. This article delves into the significance, current status, and future directions of hard tooth surface machining for spiral bevel gears, emphasizing key technological advancements and practical considerations. I will explore various finishing methods, international and domestic landscapes, heat treatment deformation control, and the impact of CNC technology, all while incorporating tables and formulas to summarize complex concepts. The overarching goal is to provide a comprehensive overview that underscores the importance of spiral bevel gears in industrial applications and the evolving strategies to optimize their manufacturing.
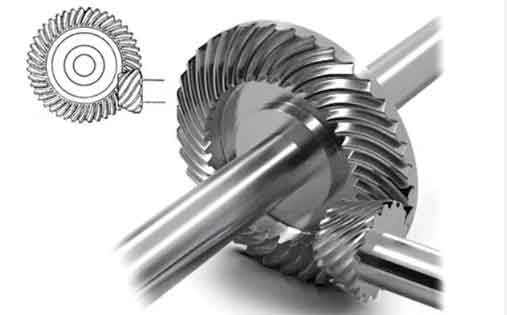
The significance of hard tooth surface machining for spiral bevel gears cannot be overstated, as it directly influences gear performance, lifespan, and noise reduction. Currently, three primary methods are employed for finishing hard tooth surfaces of spiral bevel gears: lapping, grinding, and skiving (also known as hard milling or刮削). Lapping is a traditional process characterized by high productivity; however, its ability to correct errors beyond reducing surface roughness at contact areas is very limited. Grinding, on the other hand, offers high error elimination capabilities but requires specialized grinding machines, which are scarce and expensive domestically, making it unsuitable for gears that do not demand ultra-high transmission quality. Skiving, developed in the mid-20th century, involves using hard alloy cutters to remove a thin layer of metal from quenched surfaces with hardness up to 60-62 HRC, effectively correcting heat treatment deformation errors. This method has gained widespread adoption due to its high productivity and relatively moderate cost increase. Internationally, companies like Klingelnberg in Germany and Gleason in the USA have pioneered skiving technology, but its implementation in regions like China faces hurdles such as high investment costs and compatibility with existing machinery. For small to medium-batch production, where controlling heat treatment deformation is challenging, skiving presents a viable solution, provided that cost-effectiveness can be enhanced. In this context, developing localized hard tooth surface machining methods for spiral bevel gears tailored to domestic conditions becomes imperative.
To better understand the trade-offs between these methods, I have compiled a comparison table that highlights their key attributes. This analysis underscores why skiving is increasingly favored for spiral bevel gears in many industrial settings.
| Method | Advantages | Disadvantages | Typical Surface Roughness | Suitability for Spiral Bevel Gears |
|---|---|---|---|---|
| Lapping | High productivity, low cost | Limited error correction, only improves roughness | 0.4–0.8 μm | Low-precision applications |
| Grinding | High precision, excellent error elimination | High cost, specialized equipment needed, limited to small sizes | 0.1–0.4 μm | High-precision, small to medium gears |
| Skiving | Good error correction, high productivity, suitable for large gears | High initial investment, requires advanced tooling | 0.2–0.6 μm | Medium to large spiral bevel gears, batch production |
The current status and development of hard tooth surface machining for spiral bevel gears reflect a global push towards higher efficiency and precision. In developed industrial nations, the journey began with Klingelnberg’s development of the “Palloid” method in the 1970s, which uses mechanically clamped hard alloy inserts in cutter heads to finish spiral bevel gears with hardness up to 62 HRC, achieving accuracy grades up to DIN 5 and surface roughness of 0.4–0.8 μm. This method enables machining of spiral bevel gears with diameters up to 2000 mm, modules up to 30 mm, and power transmission capacities exceeding 10,000 kW, addressing needs in heavy machinery where grinding is impractical. Gleason followed with its skiving technology, utilizing brazed hard alloy cutters on cutter heads mounted on machines like the Phoenix series, capable of finishing spiral bevel gears with hardness up to 60 HRC, accuracy grades of AGMA 10-12, and similar roughness levels. Japan’s Sumitomo Electric has also contributed by employing cubic boron nitride (CBN) inserts for skiving, achieving high precision for spiral bevel gears with modules up to 12 mm. These advancements highlight the critical role of cutter design and tool materials—such as hard alloys and CBN—in enabling effective skiving of spiral bevel gears. In contrast, the domestic scene in China shows a gap, with reliance on imported technologies and challenges in adapting them to local machine tools. Some factories have introduced Klingelnberg or Gleason systems, but issues like quality consistency and high costs persist, underscoring the need for indigenous innovation. The productivity gains from skiving spiral bevel gears are substantial, often 5–10 times higher than grinding and 3–5 times higher than lapping, making it a key focus for future development.
A deeper look into the technical parameters of international skiving methods for spiral bevel gears reveals the importance of optimized tool geometry and machining conditions. I have summarized these in a table to illustrate the capabilities and limitations.
| Company | Tool Material | Gear Hardness (HRC) | Max Gear Diameter (mm) | Max Module (mm) | Achievable Accuracy Grade | Surface Roughness (μm) |
|---|---|---|---|---|---|---|
| Klingelnberg | Mechanically clamped hard alloy | Up to 62 | 2000 | 30 | DIN 5 | 0.4–0.8 |
| Gleason | Brazed hard alloy | Up to 60 | 1500 | 25 | AGMA 10-12 | 0.2–0.6 |
| Sumitomo | CBN inserts | Up to 60 | 1000 | 12 | JIS 0-1 | 0.1–0.4 |
The control of heat treatment deformation is intrinsically linked to hard tooth surface machining for spiral bevel gears, as increasing surface hardness often exacerbates distortion during quenching. From my analysis, this poses a fundamental contradiction: higher hardness improves wear resistance and load capacity but introduces errors that must be corrected post-heat treatment. For spiral bevel gears subjected to carburizing and quenching, deformation arises from factors like non-uniform cooling, residual stresses, and material heterogeneity. Research has focused on minimizing deformation through improved steel metallurgy, optimized渗碳 processes, controlled cooling techniques, and better fixturing. However, complete elimination is nearly impossible, making post-heat treatment machining essential. Skiving of spiral bevel gears offers a strategic solution by removing a thin, controlled layer—typically 0.05–0.2 mm—to correct distortions while maintaining hardness. The relationship between deformation and machining allowances can be modeled using formulas that account for material properties and gear geometry. For instance, the expected deformation ΔD for a spiral bevel gear after quenching can be approximated by:
$$ \Delta D = k \cdot \frac{\sigma_y \cdot V}{E} $$
where k is a material constant, σ_y is the yield strength, V is the volume, and E is the Young’s modulus. By integrating such models, manufacturers can pre-calculate machining allowances for spiral bevel gears, optimizing the skiving process to achieve target tolerances. This synergy between deformation control and hard tooth surface machining is crucial for producing high-quality spiral bevel gears with extended service life and reduced noise.
The advent of CNC gear cutting machines has profoundly impacted hard tooth surface machining for spiral bevel gears, offering enhanced flexibility, precision, and rigidity. Traditional mechanical machines for spiral bevel gears rely on complex linkages to generate tool-workpiece motions, but CNC systems replace these with digitally controlled axes, enabling more accurate and adaptable manufacturing. For example, Gleason’s Phoenix series uses a 6-axis CNC to produce any锥齿轮 geometry, eliminating components like the cradle, eccentric mechanism, and cutter tilt, thereby increasing system stiffness and reducing error sources. Similarly, Klingelnberg’s CNC series features multiple axes for high-efficiency machining. These advancements are particularly beneficial for skiving spiral bevel gears, as the intermittent cutting actions demand robust machine structures and precise motion control. The kinematic equations for CNC machining of spiral bevel gears can be derived from the gear tooth geometry. Consider a spiral bevel gear with pitch cone angle γ, spiral angle β, and module m. The cutter path relative to the workpiece can be described by:
$$ \mathbf{R}(t) = \mathbf{T}(\theta(t)) \cdot \mathbf{C}(\phi(t)) + \mathbf{O} $$
where \(\mathbf{R}(t)\) is the position vector, \(\mathbf{T}\) is the transformation matrix for workpiece rotation θ, \(\mathbf{C}\) is the cutter motion function for rotation φ, and \(\mathbf{O}\) is the offset vector. By programming these motions in CNC, manufacturers can achieve optimal tool engagement for skiving hard tooth surfaces on spiral bevel gears, improving surface integrity and tool life. Moreover, CNC machines facilitate the implementation of adaptive strategies, such as varying feed rates based on real-time feedback, which is essential for handling the high cutting forces involved in skiving spiral bevel gears with hardness above 58 HRC.
To illustrate the advantages of CNC machines for hard tooth surface machining of spiral bevel gears, I have prepared a table comparing traditional and CNC-based approaches.
| Aspect | Traditional Mechanical Machines | CNC Machines |
|---|---|---|
| Motion Generation | Mechanical linkages (cradle, eccentrics) | Digital servo axes |
| Flexibility | Limited to specific gear types | High, adaptable to various spiral bevel gear designs |
| Precision | Subject to wear and backlash | High positioning accuracy (e.g., ±0.001 mm) |
| Rigidity | Lower due to multiple joints | Higher, with reduced mechanical interfaces |
| Setup Time | Long, manual adjustments | Short, programmable parameters |
| Suitability for Skiving | Limited, often requires modifications | Excellent, with optimized kinematics for hard tooth surfaces |
Looking ahead, the development of hard tooth surface machining for spiral bevel gears will likely focus on several key areas. First, tool technology must advance to include more durable materials like advanced ceramics or diamond-coated inserts, which can withstand the abrasive nature of skiving high-hardness spiral bevel gears. Second, process optimization through simulation and AI-driven analytics will enable better prediction of heat treatment deformation and machining outcomes for spiral bevel gears, reducing trial-and-error. For instance, finite element analysis (FEA) models can simulate quenching distortion, allowing pre-compensation in soft machining stages. The distortion compensation ΔC can be expressed as:
$$ \Delta C = f(H, T, t) $$
where H is hardness, T is temperature, and t is time. Integrating such models with CNC systems will streamline the production of spiral bevel gears. Third, hybrid processes that combine skiving with subsequent superfinishing may emerge to achieve ultra-low roughness on spiral bevel gears, further enhancing efficiency and noise performance. Additionally, the rise of digital twins and IoT in manufacturing will facilitate real-time monitoring of skiving processes for spiral bevel gears, ensuring consistency and quality. Domestically, efforts should prioritize cost reduction via localized tooling and machine retrofits, making skiving accessible for small to medium-batch producers of spiral bevel gears. Collaborative research between academia and industry can accelerate innovation, as seen in ongoing studies on tooth contact analysis and load distribution for spiral bevel gears.
In conclusion, hard tooth surface machining for spiral bevel gears is a dynamic field that balances technological innovation with practical economic considerations. From my viewpoint, the significance of spiral bevel gears in transmitting power efficiently necessitates continuous improvement in finishing methods, with skiving standing out as a promising approach despite its challenges. The current status shows a divide between advanced international capabilities and domestic hurdles, but the integration of CNC technology and better deformation control offers a path forward. By leveraging tables and formulas to summarize key aspects—such as method comparisons, technical parameters, and kinematic equations—I have aimed to provide a detailed exposition that underscores the centrality of spiral bevel gears in modern engineering. Future progress will depend on holistic strategies that encompass tool design, process simulation, and adaptive manufacturing, ultimately enabling the widespread adoption of high-quality hard tooth surface spiral bevel gears across industries. As research continues, the synergy between these elements will drive the evolution of spiral bevel gear machining, ensuring they meet the ever-growing demands for performance and reliability.
To further elaborate on the technical nuances, let’s consider the geometric design of spiral bevel gears, which influences their machinability and performance. The tooth profile of a spiral bevel gear can be described using mathematical equations that account for the spiral angle and curvature. For a standard spiral bevel gear, the tooth surface equation in a coordinate system attached to the gear might be given by:
$$ \mathbf{S}(u, v) = \begin{bmatrix} (R_m + u \cos \beta) \cos \theta \\ (R_m + u \cos \beta) \sin \theta \\ u \sin \beta \end{bmatrix} $$
where \(R_m\) is the mean cone distance, \(\beta\) is the spiral angle, \(\theta\) is the angular position, and u and v are parameters. This geometry complicates machining, especially for hard tooth surfaces, as it requires precise cutter alignment and motion control. During skiving of spiral bevel gears, the cutter must follow this surface while maintaining optimal cutting conditions to avoid tool wear and ensure surface quality. The cutting force \(F_c\) can be modeled as:
$$ F_c = K_c \cdot a_p \cdot f_z \cdot \sin(\psi) $$
where \(K_c\) is the specific cutting force, \(a_p\) is the depth of cut, \(f_z\) is the feed per tooth, and \(\psi\) is the engagement angle. For spiral bevel gears with high hardness, \(K_c\) increases, necessitating robust tooling and machine stability. These formulas highlight the interplay between gear design and machining parameters, emphasizing why specialized approaches are needed for spiral bevel gears.
Another critical aspect is the economic analysis of hard tooth surface machining for spiral bevel gears. I have developed a table to compare the cost components across different methods, which can guide decision-making for manufacturers focused on spiral bevel gears.
| Cost Component | Lapping | Grinding | Skiving |
|---|---|---|---|
| Equipment Investment | Low ($50,000–$100,000) | High ($500,000–$2M) | Medium ($200,000–$800,000) |
| Tooling Cost | Low ($1,000–$5,000) | High ($10,000–$50,000) | Medium ($5,000–$20,000) |
| Operational Cost | Low ($10–$50/hour) | High ($100–$300/hour) | Medium ($50–$150/hour) |
| Production Time | Short (0.5–2 hours) | Long (2–10 hours) | Moderate (1–4 hours) |
| Total Cost per Gear | $100–$500 | $1,000–$5,000 | $300–$1,500 |
| Suitability for Spiral Bevel Gears | Low-volume, low-precision | High-precision, small batches | Medium to high-volume, various sizes |
This economic perspective reinforces why skiving is often preferred for spiral bevel gears in many scenarios, as it balances cost and performance. Moreover, the lifecycle benefits of hard tooth surface spiral bevel gears—such as increased service life and reduced downtime—can justify higher initial investments. For instance, a spiral bevel gear with skived hard surfaces might last 50% longer than a lapped one, leading to significant savings over time. To quantify this, the total cost of ownership (TCO) can be calculated as:
$$ TCO = C_i + \sum_{t=1}^{n} \frac{C_o}{(1+r)^t} $$
where \(C_i\) is the initial cost, \(C_o\) is the annual operating cost, r is the discount rate, and n is the lifespan in years. For spiral bevel gears, skiving often yields a lower TCO due to reduced maintenance and replacement needs.
In summary, the journey of hard tooth surface machining for spiral bevel gears is one of continuous innovation and adaptation. From the early days of lapping to the modern era of CNC-driven skiving, each advancement has brought us closer to producing spiral bevel gears that meet the rigorous demands of industries like automotive, aerospace, and heavy machinery. As I reflect on the current landscape, I am optimistic about the future, especially with emerging technologies like additive manufacturing for tooling and digital process chains. By staying focused on the unique challenges of spiral bevel gears—such as their complex geometry and sensitivity to heat treatment—we can develop more efficient and cost-effective solutions. Ultimately, the goal is to ensure that spiral bevel gears remain a cornerstone of mechanical transmissions, delivering reliable power transmission in an increasingly automated world.