
In mechanical engineering, bevel gears play a pivotal role as transmission components, enabling the conversion of motion between intersecting shafts. Compared to coaxial gears, bevel gears are specifically designed to alter the direction of power transmission. During service, bevel gears are often subjected to high stresses, leading to failures such as tooth root fracture. To enhance the strength and longevity of these critical components, heat treatment processes like quenching are extensively employed. Quenching involves heating a metal part to a specific temperature, holding it, and then rapidly cooling it to modify its microstructure and achieve desired mechanical properties. This process induces beneficial residual stresses that can improve fatigue resistance. However, the interplay of thermal and phase transformation stresses during quenching can also lead to undesirable outcomes like distortion and cracking, which compromise the performance and reliability of bevel gears. Traditional experimental methods for studying quenching, such as metallographic analysis, are often time-consuming, costly, and difficult to control due to numerous influencing factors. Therefore, computational simulations using finite element analysis (FEA) have become an indispensable tool. This article employs Ansys finite element software to simulate the quenching process of a bevel gear, investigating the evolution of temperature fields and stress fields under different cooling conditions. By correlating simulation results with experimental principles, this analysis aims to provide valuable insights for optimizing the heat treatment of bevel gears in industrial applications.
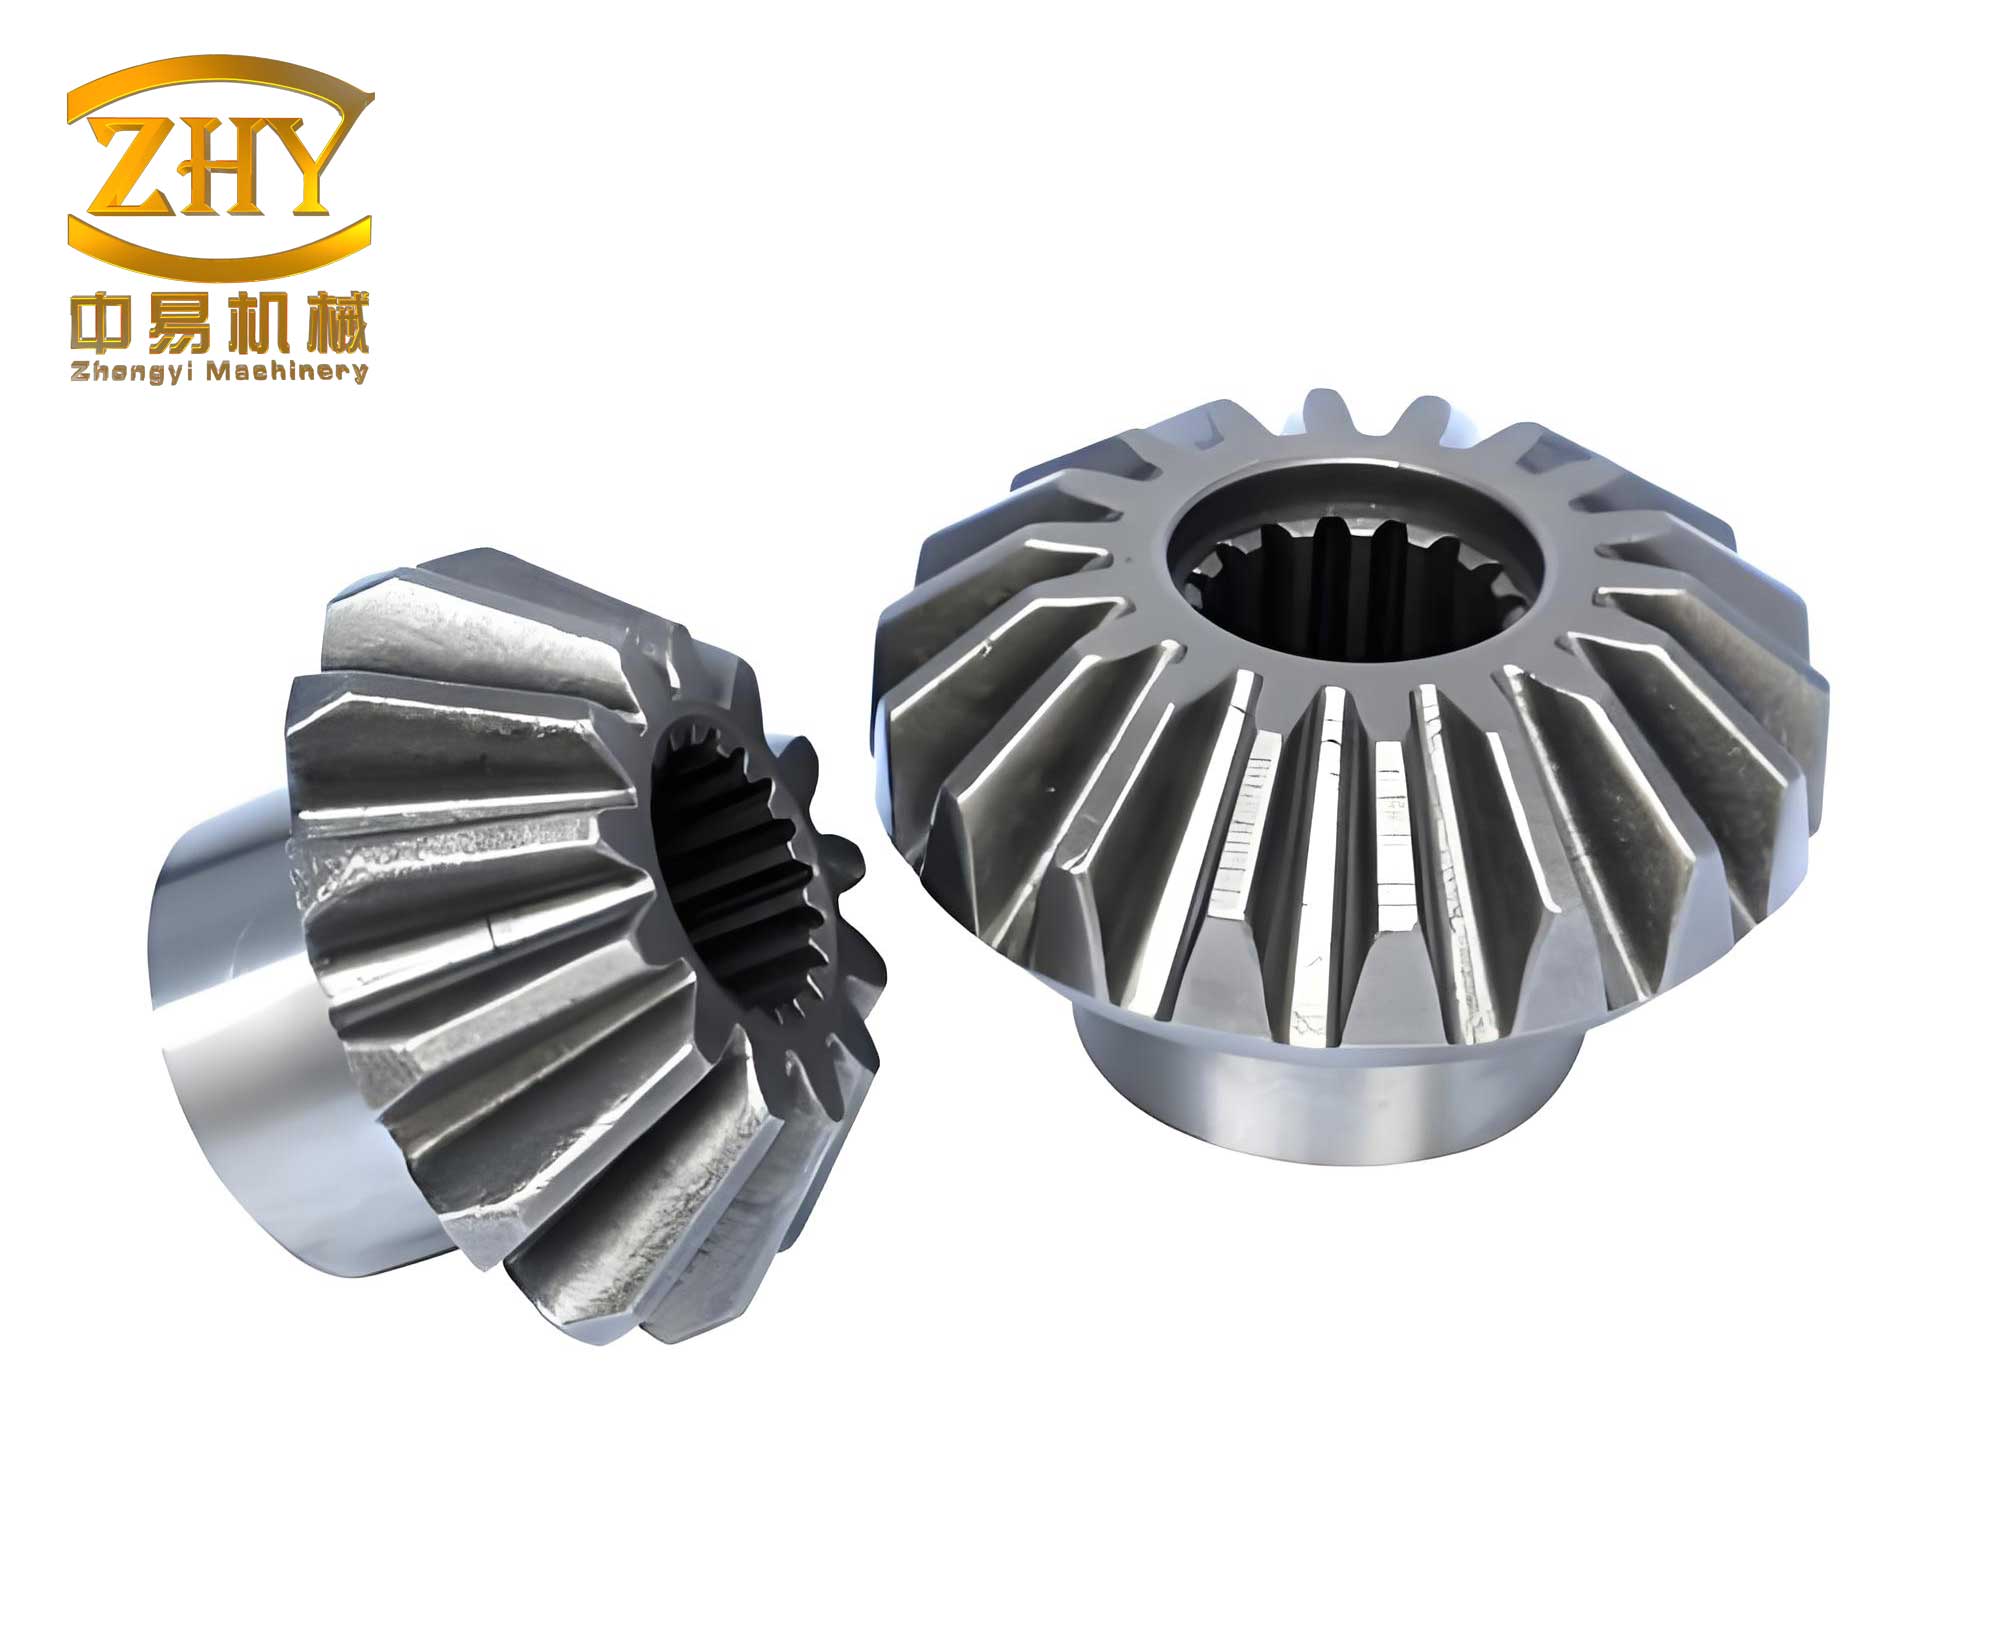
The quenching of a bevel gear is a complex, transient, non-linear thermo-mechanical process. It primarily involves heat transfer between the hot gear and the quenching medium, accompanied by microstructural phase transformations (e.g., austenite to martensite or bainite). The fundamental governing equation for heat conduction during this process is Fourier’s law, expressed in three dimensions for a material with internal heat generation (like phase transformation latent heat). The general heat conduction equation forms the basis for the thermal analysis of the bevel gear during quenching.
$$ \frac{\partial}{\partial x} \left( k \frac{\partial T}{\partial x} \right) + \frac{\partial}{\partial y} \left( k \frac{\partial T}{\partial y} \right) + \frac{\partial}{\partial z} \left( k \frac{\partial T}{\partial z} \right) + q = \rho c \frac{\partial T}{\partial t} $$
Here, \( T \) represents temperature (in °C or K), \( k \) is the temperature-dependent thermal conductivity (in W·m⁻¹·°C⁻¹), \( q \) is the internal heat generation rate per unit volume (in W·m⁻³), which accounts for the latent heat released during phase transformations, \( \rho \) is the density (in kg·m⁻³), \( c \) is the specific heat capacity (in J·kg⁻¹·°C⁻¹), and \( t \) is time (in seconds). For the bevel gear quenching simulation, the boundary condition at the gear surface is typically a convective heat transfer condition, defined as the third kind (Robin condition). This is crucial for accurately modeling the interaction between the bevel gear and the quenching medium.
$$ -k \left. \frac{\partial T}{\partial n} \right|_s = h (T_w – T_c) $$
In this equation, \( h \) is the heat transfer coefficient (in W·m⁻²·°C⁻¹), which is a highly non-linear function of surface temperature and the quenching medium’s properties. \( T_w \) is the temperature of the bevel gear’s surface, and \( T_c \) is the temperature of the quenching medium (oil, water, or air). The initial condition for the simulation is the uniform austenitizing temperature of the bevel gear:
$$ T|_{t=0} = T_0 $$
The mechanical response of the bevel gear during quenching is driven by thermal strains and transformation-induced strains. The total strain \( \epsilon_{total} \) can be decomposed into elastic \( \epsilon_{el} \), plastic \( \epsilon_{pl} \), thermal \( \epsilon_{th} \), and phase transformation \( \epsilon_{tr} \) components. The thermal strain is calculated as:
$$ \epsilon_{th} = \alpha (T – T_{ref}) $$
where \( \alpha \) is the coefficient of thermal expansion (in °C⁻¹) and \( T_{ref} \) is a reference temperature (often the initial temperature). The von Mises stress \( \sigma_{vm} \), a key indicator of yielding and potential failure in the bevel gear, is derived from the stress tensor components:
$$ \sigma_{vm} = \sqrt{ \frac{1}{2} \left[ (\sigma_{11} – \sigma_{22})^2 + (\sigma_{22} – \sigma_{33})^2 + (\sigma_{33} – \sigma_{11})^2 + 6(\sigma_{12}^2 + \sigma_{23}^2 + \sigma_{31}^2) \right] } $$
These equations form the mathematical foundation for the coupled thermo-mechanical finite element analysis of the bevel gear quenching process.
To perform the simulation, a three-dimensional model of a bevel gear is essential. Given the complexity of bevel gear geometry, dedicated CAD software like Pro/ENGINEER (Pro/E) or SolidWorks is typically used for modeling. The model is then imported into Ansys for preprocessing. To reduce computational cost while maintaining accuracy, symmetry can be exploited. For a single bevel gear tooth, symmetric boundary conditions can be applied on the cut faces, allowing the analysis of one tooth segment as representative of the entire bevel gear behavior. The finite element mesh is generated using suitable elements. For a coupled thermal-stress analysis, Ansys provides coupled-field elements like SOLID226 or SOLID227. Alternatively, an indirect sequential coupling approach can be used, where the thermal analysis results (temperature history) are imported as a load into a separate structural analysis. However, for a more integrated solution, direct coupling with a single element type that computes temperature and displacement degrees of freedom simultaneously is often preferred for processes like bevel gear quenching where thermal and mechanical phenomena are strongly interdependent.
The material chosen for this bevel gear simulation is a low-alloy steel, such as 20CrMoH, commonly used for carburized gears. Its temperature-dependent properties are critical inputs. Below is a summary table of key material properties at room temperature, though for accurate simulation, these should be defined as functions of temperature.
| Property | Symbol | Value | Units |
|---|---|---|---|
| Density | \( \rho \) | 7840 | kg·m⁻³ |
| Thermal Conductivity | \( k \) | 44 | W·m⁻¹·°C⁻¹ |
| Specific Heat Capacity | \( c \) | 460 | J·kg⁻¹·°C⁻¹ |
| Elastic Modulus | \( E \) | 210 × 10⁹ | Pa |
| Poisson’s Ratio | \( \nu \) | 0.278 | – |
| Coefficient of Thermal Expansion | \( \alpha \) | 1.27 × 10⁻⁵ | °C⁻¹ |
The most critical parameter for quenching simulation is the heat transfer coefficient (HTC) \( h \), which defines the cooling intensity at the bevel gear surface. It is a complex function of surface temperature, medium type, agitation, and part geometry. For simplicity, empirical data or values from literature are often used. The HTC profiles for oil and water quenching, relevant for bevel gear processing, are presented below.
| Surface Temperature (°C) | Heat Transfer Coefficient (W·m⁻²·°C⁻¹) |
|---|---|
| 50 | 224.5 |
| 100 | 250.4 |
| 200 | 270.6 |
| 300 | 459.5 |
| 400 | 1757.4 |
| 500 | 4358.6 |
| 600 | 3872.6 |
| 700 | 2189.9 |
| 860 | 947.0 |
| Surface Temperature (°C) | Heat Transfer Coefficient (W·m⁻²·°C⁻¹) |
|---|---|
| 50 | 1000 |
| 100 | 3800 |
| 200 | 6000 |
| 300 | 13500 |
| 400 | 12500 |
| 500 | 7000 |
| 600 | 4200 |
| 755 | 1000 |
| 860 | 500 |
The initial temperature \( T_0 \) for the bevel gear is set to 860°C, representing a typical austenitizing temperature. The quenching medium temperature \( T_c \) is 50°C. For stress analysis, a comparison is made between conventional continuous quenching and a stepped (interrupted) quenching process. In stepped quenching, the bevel gear is first quenched in oil until it reaches an intermediate temperature (e.g., 300°C), and then it is cooled in air. The HTC for air cooling is significantly lower, typically around 50 W·m⁻²·°C⁻¹.
The temperature field evolution within the bevel gear during quenching reveals the cooling kinetics. Monitoring points are selected at critical locations on a single tooth: Point A at the tooth core (center of the gear blank section within the tooth), Point B on the fillet region or root area between teeth (a high-stress concentration zone), and Point C at the tooth tip. The cooling curves for these points under oil and water quenching are analyzed. The temperature distribution across the bevel gear at various time steps can be visualized through contour plots. The governing equation solved numerically by Ansys for each node is a discretized form of the Fourier equation combined with the boundary condition.
$$ [C]\{\dot{T}\} + [K]\{T\} = \{Q\} $$
Here, \( [C] \) is the heat capacity matrix, \( [K] \) is the thermal conductivity matrix, \( \{T\} \) is the vector of nodal temperatures, \( \{\dot{T}\} \) is its time derivative, and \( \{Q\} \) is the nodal heat flux vector accounting for boundary conditions like convection. The results show that for the bevel gear, water quenching achieves a much faster cooling rate than oil quenching. The tooth tip (Point C) cools the fastest due to its higher surface area-to-volume ratio and direct exposure to the medium. In water, the entire bevel gear reaches near ambient temperature in approximately 150 seconds, whereas oil quenching requires about 600 seconds. The temperature gradients within the bevel gear are more severe in water quenching, especially during the initial stages. This rapid cooling can lead to higher thermal stresses. The temperature difference \( \Delta T \) between the surface and core of the bevel gear is a key driver of thermal stress, calculated at any point as:
$$ \Delta T = T_{surface} – T_{core} $$
This gradient is significantly larger during the first few seconds of water quenching compared to oil quenching for the bevel gear.
The stress field development in the bevel gear is a consequence of non-uniform cooling and phase transformation. The total stress \( \sigma \) is related to the elastic strain by Hooke’s law, modified for thermal effects:
$$ \{\sigma\} = [D] (\{\epsilon_{total}\} – \{\epsilon_{th}\} – \{\epsilon_{tr}\}) $$
where \( [D] \) is the elasticity matrix. The von Mises stress is monitored at the same points A, B, and C. For conventional oil quenching of the bevel gear, the maximum von Mises stress typically occurs at Point B, the root fillet region, which is a critical area for fatigue failure. Point C (tooth tip) exhibits the most rapid change in stress. The stress history shows that different points on the bevel gear experience varying stress magnitudes at the same time, leading to complex internal stresses that can cause distortion. In stepped quenching, the bevel gear is initially cooled in oil to 300°C and then air-cooled. This process alters the stress evolution. The cooling rate in the air stage is much slower, allowing for more temperature homogenization and stress relaxation. Consequently, the stress differences between Points A and B are reduced after the initial oil quench phase. While the final stress state might be similar, the path to get there is more controlled. The thermal strain rate, which influences stress generation, is lower during air cooling.
$$ \dot{\epsilon}_{th} = \alpha \dot{T} $$
By reducing \( \dot{T} \) in the martensitic transformation range (below ~300°C for many steels), stepped quenching mitigates the risk of quench cracking in the bevel gear. The distortion, particularly at the tooth tip (Point C), is also more gradual in stepped quenching compared to the abrupt dimensional changes in conventional quenching.
A comprehensive comparison of the two quenching methods for bevel gear treatment can be summarized in the following table, which highlights key parameters affecting quality.
| Parameter | Conventional Oil Quenching | Stepped Quenching (Oil + Air) | Water Quenching |
|---|---|---|---|
| Total Cooling Time to 50°C | ~600 s | ~2200 s | ~150 s |
| Max Cooling Rate (at tooth tip) | Moderate | Low (in air stage) | Very High |
| Max von Mises Stress Location | Tooth Root (Point B) | Tooth Root (Point B) | Tooth Root (Point B) |
| Stress Uniformity During Cooling | Low (High gradient between points) | Higher (Reduced gradient after oil stage) | Very Low (Severe gradients) |
| Risk of Distortion | Moderate | Lower | High |
| Risk of Quench Cracking | Moderate | Lower | Very High |
| Suitability for Complex Bevel Gears | Good | Excellent (for sensitive geometries) | Poor (risk of cracking) |
To further quantify the thermal history, the cooling rate \( CR \) at a specific point is crucial for predicting microstructure. It can be approximated from the simulation data:
$$ CR = -\frac{dT}{dt} $$
For instance, at the tooth tip of the bevel gear during the first second of water quenching, \( CR \) can exceed 200 °C/s, while in oil it might be around 80 °C/s. The integral of the stress over time, related to the strain energy density \( U \), also provides insight into potential damage accumulation in the bevel gear:
$$ U = \int_{0}^{t} \sigma : d\epsilon $$
In practice, the goal for heat treating a bevel gear is to achieve a hardened case with a tough core while minimizing residual stresses that promote distortion. The finite element analysis allows for optimizing process parameters such as quenching medium temperature, agitation speed, and the transition temperature in stepped quenching. For example, varying the intermediate temperature in stepped quenching for the bevel gear from 250°C to 350°C can be simulated to find the optimum that balances microstructure formation and stress minimization.
Another important aspect is the effect of bevel gear geometry on quenching. Parameters like module, pressure angle, and spiral angle influence heat dissipation and stress concentration. A finer mesh in the fillet region of the bevel gear is often necessary to accurately capture the high stress gradients. The symmetry assumption used for a single tooth is valid for uniform quenching conditions around the entire bevel gear circumference. However, if the quenching process involves non-uniform immersion or spray cooling, a full 360-degree model of the bevel gear might be required.
Material property dependence on temperature and phase is also critical. For instance, during the martensitic transformation in the bevel gear, there is a volumetric expansion. This can be modeled as a transformation strain proportional to the volume fraction of martensite \( f_m \):
$$ \epsilon_{tr} = \beta f_m $$
where \( \beta \) is the transformation expansion coefficient. The evolution of \( f_m \) is often described by the Koistinen-Marburger equation for diffusionless transformation:
$$ f_m = 1 – \exp[-\phi(M_s – T)] $$
for \( T < M_s \) (martensite start temperature), where \( \phi \) is a material constant. Incorporating such kinetics into the finite element model of the bevel gear quenching simulation enhances the accuracy of stress prediction, as the transformation plasticity effects are significant.
Validation of the finite element model for bevel gear quenching is essential. This can be done by comparing simulated cooling curves with experimental data from thermocouples embedded in a prototype bevel gear during quenching. Similarly, residual stress measurements using techniques like X-ray diffraction or hole-drilling on a quenched bevel gear can be compared with simulation results. Good agreement confirms the model’s reliability for predicting the behavior of production bevel gears under different quenching schedules.
In conclusion, finite element analysis using Ansys provides a powerful virtual platform for investigating the quenching process of bevel gears. By solving the coupled thermal and mechanical equations, it reveals detailed insights into temperature distribution, cooling rates, stress evolution, and distortion tendencies. The simulation clearly demonstrates that oil quenching offers a gentler cooling profile for the bevel gear compared to water quenching, reducing thermal shock and the risk of cracking. However, stepped quenching emerges as a superior strategy for critical bevel gear applications, as it promotes more uniform stress development and controlled distortion by employing a slow air-cooling stage after the initial quench. The tooth root region of the bevel gear is identified as the zone of highest tensile stress, necessitating careful process design to prevent fatigue failure. The use of tables and mathematical equations, as shown throughout this analysis, helps systematically summarize the complex interactions. This computational approach enables engineers to optimize quenching parameters for bevel gears without the cost and time of extensive physical trials, ultimately leading to more reliable and durable gear components in power transmission systems. Future work could involve integrating more detailed phase transformation kinetics, simulating carburizing prior to quenching for case-hardened bevel gears, and exploring the effects of alloying elements on the quenchability of bevel gear steels.