
In modern mechanical transmission systems, particularly within the demanding environment of aerospace propulsion, bevel gears serve as critical components for redirecting power flow. Their reliable operation is paramount to the overall stability and safety of the system. However, during service, bevel gears are subjected to a complex interplay of cyclic loading, sliding friction, manufacturing tolerances, and operational stresses. This often leads to various forms of surface degradation, such as wear, pitting, spalling, and scuffing. Traditional maintenance philosophies, often erring on the side of extreme caution, result in the premature scrapping of bevel gears that retain significant residual functional life and embodied value. This practice not only inflates operational costs but also contributes to unnecessary resource consumption and waste. Consequently, the development and implementation of a robust remanufacturing strategy for bevel gears present a compelling solution, aligning technical feasibility with significant economic and environmental benefits.
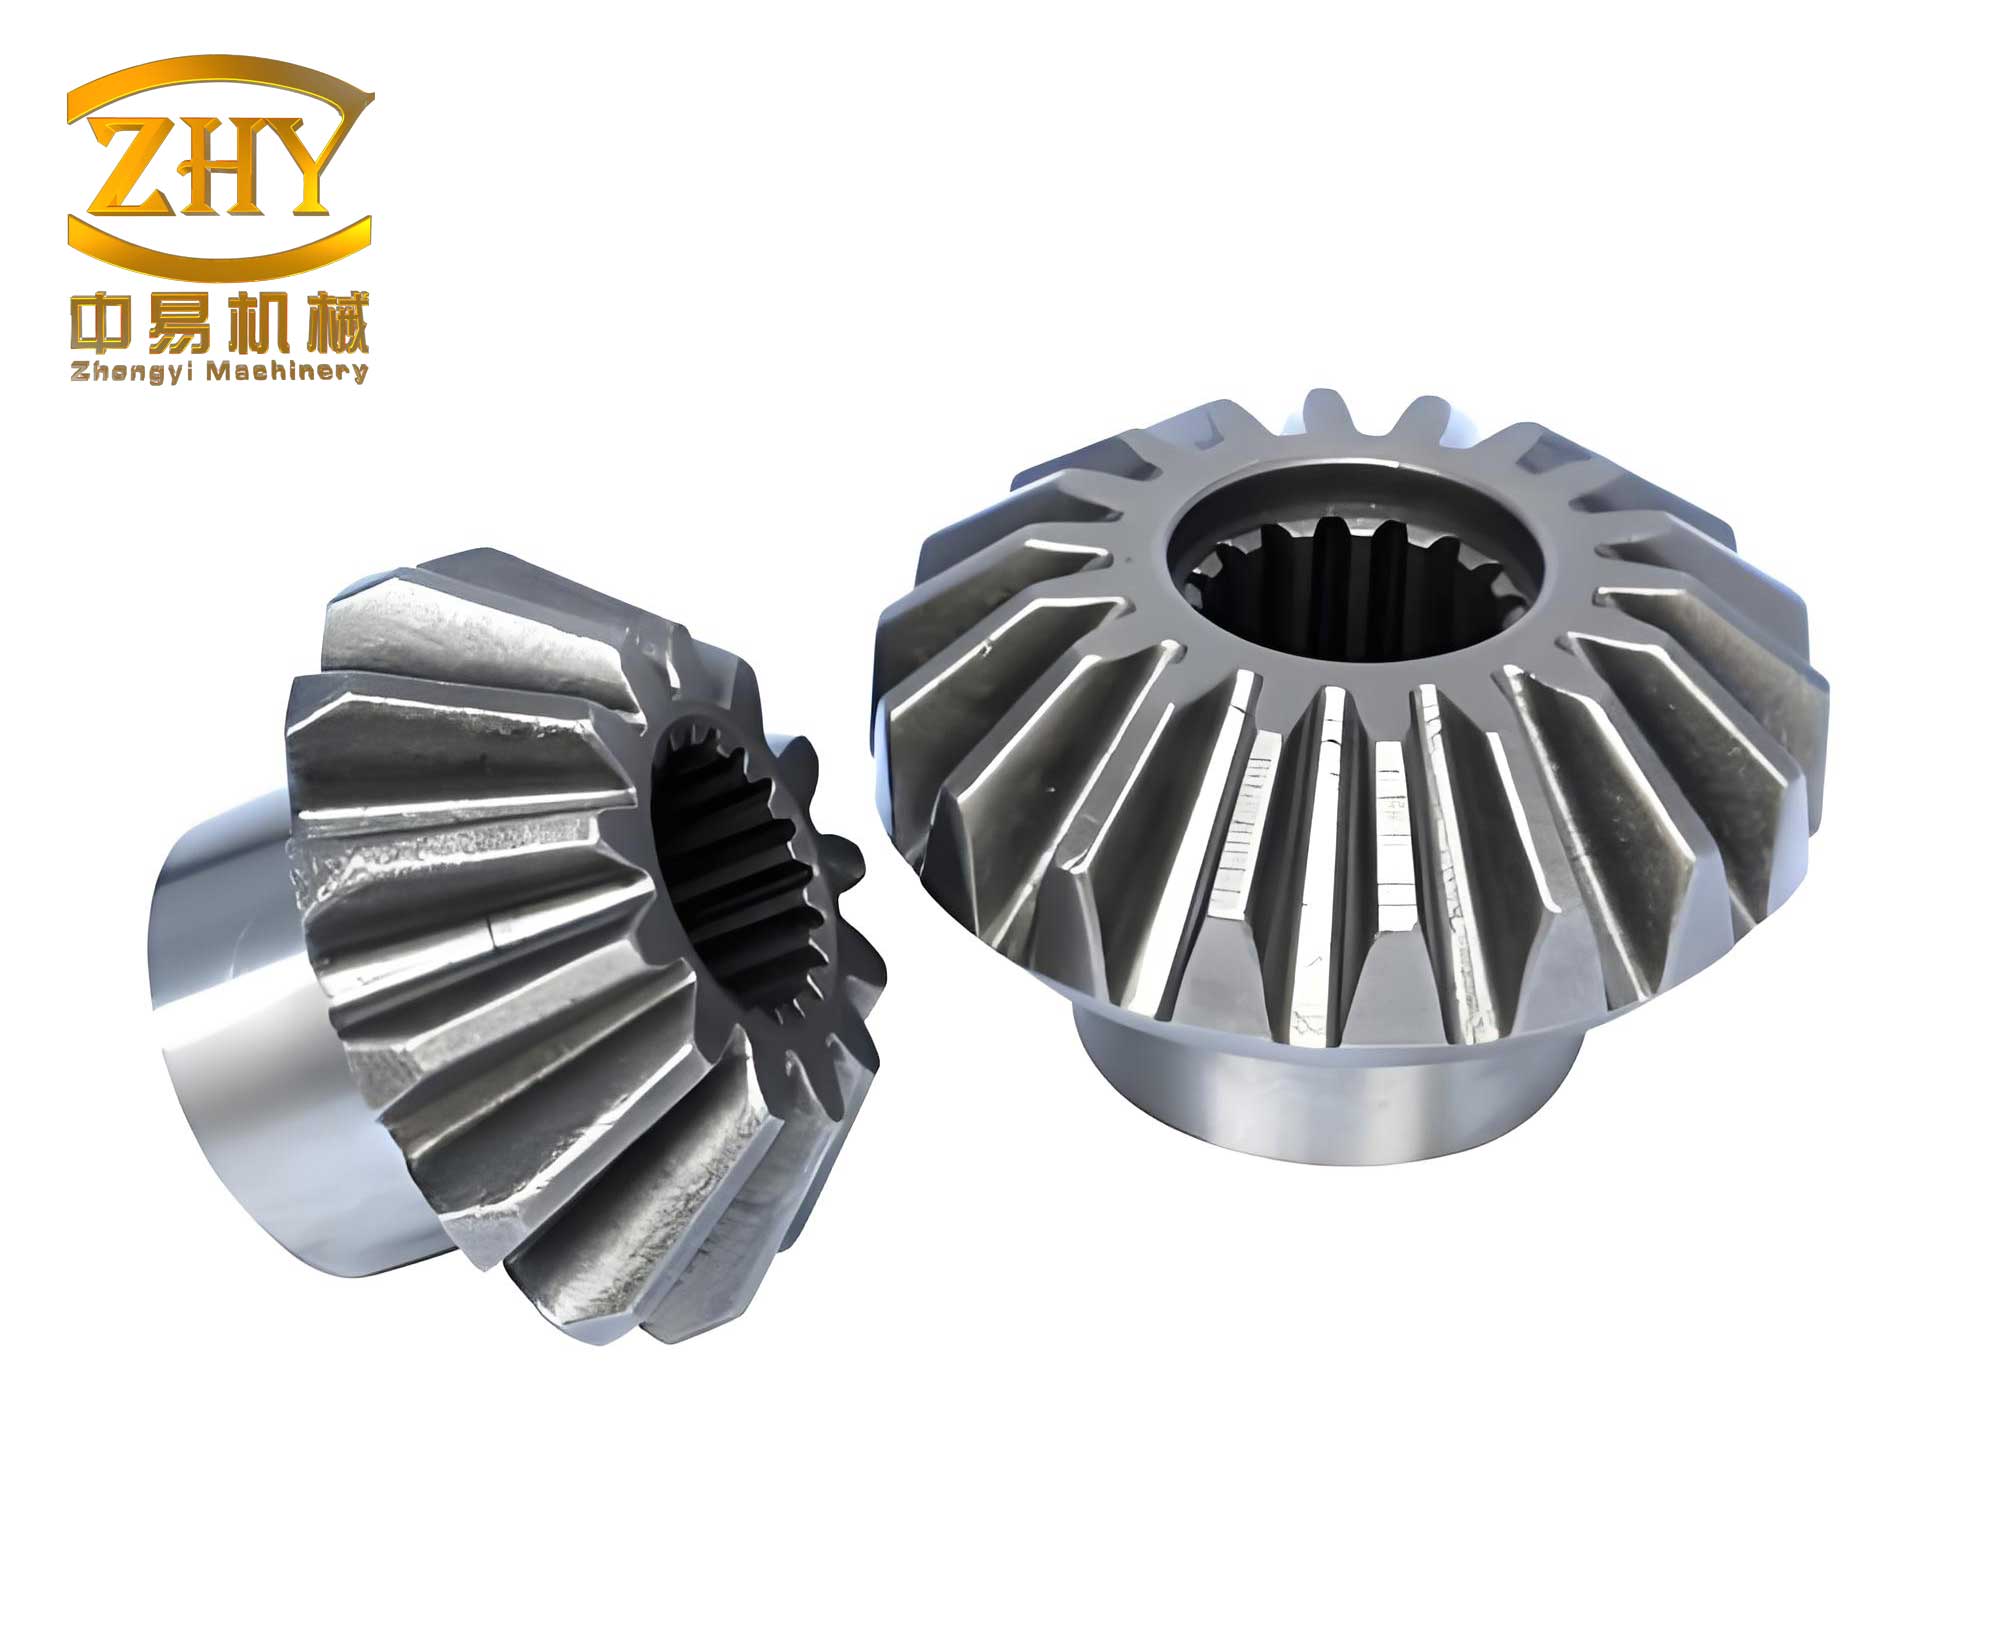
Bevel gear remanufacturing, in this context, is defined as the series of industrial processes applied to a used bevel gear that has been removed from service primarily due to surface degradation. The core objective is to restore, and potentially enhance, the gear’s performance characteristics to meet or exceed original specifications without fundamentally altering its base material or geometry. This is achieved while ensuring the final product complies with contemporary environmental and performance standards. The central philosophy is to preserve the high embedded value—encompassing material, energy, and labor—of the original component, which often constitutes up to 85% of the new part’s total cost, while addressing the root cause of failure to extend its service life.
Failure Modes and Feasibility Assessment for Bevel Gear Remanufacturing
A thorough understanding of failure mechanisms is the cornerstone of developing an effective remanufacturing protocol. The primary failure modes observed in bevel gears are surface-initiated.
Scuffing (Abrasive Wear & Adhesion): This occurs when the lubricant film between mating tooth surfaces breaks down under high pressure and sliding velocity. The resulting metal-to-metal contact leads to localized welding and subsequent tearing of surface material, causing scoring and material transfer.
Pitting and Spalling (Contact Fatigue): These are fatigue-driven failures. Repeated Hertzian contact stresses exceeding the material’s endurance limit initiate micro-cracks below the surface. These cracks propagate, eventually leading to the release of small pits or larger spalls. Contributing factors include improper heat treatment, material defects, overload, and misalignment.
Progressive Wear: Gradual loss of material from the tooth flank due to the presence of abrasives in the lubricant or marginal lubrication conditions, leading to altered tooth profile and increased backlash.
The feasibility of remanufacturing a bevel gear hinges on several critical factors beyond just the observable damage:
- Technical Viability: The core process of profile modification (or tooth flank correction) is a well-established technique in gear manufacturing and repair. Its application to restore the functional geometry of a used bevel gear is technically sound.
- Life-Cycle Considerations: Aerospace bevel gears are typically designed for a fatigue life (e.g., stress cycles > 10^7) that far exceeds the engine’s overhaul interval. A gear removed for surface damage often retains sufficient subsurface material integrity to fulfill another full service interval post-remanufacturing.
- Geometric and Metallurgical Constraints: The amount of material removed during profile modification is minimal (typically in the range of 0.02-0.08 mm). This ensures the case-hardened layer depth (e.g., 0.7-1.1 mm) remains within functional limits. Furthermore, post-remanufacturing surface enhancement processes like shot peening can reintroduce beneficial compressive residual stresses, improving fatigue resistance.
- Economic and Temporal Justification: The cost of remanufacturing is a fraction of a new bevel gear. The lead time for remanufacturing is also significantly shorter than procuring a new part, reducing aircraft downtime.
Based on these factors, a formal acceptance criterion must be established to determine which bevel gears are suitable candidates for remanufacturing. The following table outlines a proposed quantitative standard.
| Failure Mode | Remanufacturing Acceptance Criterion | Rejection Condition |
|---|---|---|
| Wear | Sum of wear on both flanks ≤ 10% of module. | Exceeds allowable wear limit. |
| Scuffing | Area ≤ 20% of working flank area AND depth ≤ 10% of module. | Exceeds either area or depth limit. |
| Pitting | Area ≤ 50% of working flank area; For area >20%, max pit size ≤ 20% of module AND max pit depth ≤ 10% of module. | Exceeds area, size, or depth limits. |
| Other | N/A | Severe burns, case crushing, base metal exposure, or any detectable cracks. |
The Core Technology: Profile Modification Theory and Parameters
Profile modification is the pivotal technical intervention in bevel gear remanufacturing. Its purpose is to deliberately alter the ideal involute or octoidal tooth profile by removing a small, controlled amount of material from specific areas of the flank. This corrective measure addresses the primary sources of vibration and dynamic load in gear meshing: meshing-in and meshing-out冲击.
Under load, teeth deflect elastically. This deflection, combined with inherent manufacturing errors (like base pitch deviation), causes a phenomenon known as “tip interference.” During meshing-in, the tip of the driven gear can interfere with the root of the driver gear. During meshing-out, the tip of the driver gear interferes with the root of the driven gear. This interference causes a sudden transfer of load between tooth pairs, generating noise, vibration, and high dynamic stresses that accelerate surface failures like scuffing.
By gently relieving the tooth tip and root regions (the areas where interference occurs), profile modification allows for a smoother transition of load between consecutive tooth pairs. The modified profile ensures continuous, controlled contact, mitigating冲击 and reducing dynamic excitations.
The modification is defined by three key parameters: the modification curve, the modification length (L), and the maximum modification amount (Cmax). A common form for the modification curve is given by:
$$ \Delta = C_{max} \left( \frac{x}{L} \right)^n $$
where $\Delta$ is the relief amount at a distance $x$ from the start of the modification along the path of contact, and $n$ defines the shape of the curve (parabolic, linear, etc.).
The maximum modification amount is typically calculated to compensate for the combined elastic deflection of the mating teeth and the anticipated manufacturing errors:
$$ C_{max} = \delta \pm \Delta f_b $$
where $\delta$ is the composite elastic deflection and $\Delta f_b$ is the base pitch error.
For spiral bevel gears, modification is often applied as a function of the gear’s rotation, leading to a “rotated” or “eased” profile from the toe to the heel. The parameters vary across the face width. Standards such as ISO provide guidelines for modification amounts relative to module. For a bevel gear with a module of 4 mm, typical parameters derived from practice and standards are summarized below:
| Parameter | Toe (Small End) | Heel (Large End) |
|---|---|---|
| Rotation Angle (α) | 1.3° – 1.8° | 0.2° – 0.6° |
| Modification Amount (Cα) | 0.015 – 0.020 mm | 0.015 – 0.022 mm |
| Modification Length (ΔLα) | 0.88 – 2.23 mm | 2.52 – 3.20 mm |
The Remanufacturing Process Flow for Bevel Gears
A systematic and controlled process is essential to ensure the quality and reliability of a remanufactured bevel gear. The following sequence outlines the key steps, contrasting with the more extensive new manufacturing cycle.
- Initial Cleaning & Disassembly: The gear is thoroughly cleaned to remove contaminants and lubricant residues, providing a clean surface for inspection.
- Non-Destructive Inspection (NDI): A critical step. Magnetic particle inspection or fluorescent penetrant inspection is mandatory to identify any subsurface cracks or material defects. Gears with cracks are immediately rejected.
- Visual Assessment & Pre-Machining: The gear is assessed against the acceptance criteria. Minor surface imperfections like burrs or light scoring may be carefully removed via precision polishing with stones or fine abrasives, ensuring minimal material removal (< 0.05 mm).
- Core Remanufacturing – Profile Modification Grinding: This is the central operation. Using a CNC bevel gear grinder (e.g., a Gleason machine), the tooth flanks are precision ground according to the predetermined modification parameters. The goal is to generate a smooth, continuous new profile that eliminates damaged material and establishes the optimized geometry.
- Surface Enhancement – Shot Peening: After grinding, the gear undergoes shot peening. This process bombards the tooth surfaces with small, spherical media, inducing a layer of compressive residual stress in the subsurface material. This significantly improves resistance to contact fatigue and bending fatigue, often recovering or exceeding the original gear’s fatigue strength.
- Post-Processing Cleaning: The gear is cleaned again to remove any grinding debris or peening media residue.
Verification, Testing, and Quality Assurance
Rigorous verification is what distinguishes professional remanufacturing from simple repair. Every remanufactured bevel gear must undergo a battery of tests to validate its conformance to original equipment manufacturer (OEM) specifications.
- Geometric Inspection: The modified tooth profile is measured using a coordinate measuring machine (CMM) or a dedicated gear inspection system. The profile deviation across numerous measured points should fall within a tight tolerance band (e.g., ±10 µm).
- Final NDI: A second NDI is performed post-grinding to ensure no defects were introduced during the remanufacturing process.
- Dimensional Checks: Chordal tooth thickness is measured to confirm it is within allowable wear limits. Surface roughness of the flanks is verified to ensure proper lubricant film formation.
- Metallurgical Verification:
- Case Depth: A sample or the actual gear (if permissible) is sectioned to measure the effective case depth. It must remain above the specified minimum (e.g., >0.7 mm).
- Hardness: Surface hardness (e.g., ≥ 60 HRC) and core hardness are tested to ensure the heat treatment properties are intact.
- Microstructure: The metallurgical structure of the case and core is examined to confirm the absence of overtempering or undesirable phases.
- Assembly & Functional Testing:
- Backlash Check: The remanufactured gear is paired with its mate and installed in a test fixture or the actual housing. The gear mesh backlash is measured and adjusted to specification.
- Gear Pattern Check: Using precision marking compound (bluing), the contact pattern on the tooth flanks is inspected under light load. The pattern must be centrally located and cover an adequate percentage of the flank area (e.g., >65%), indicating proper alignment and tooth contact.
- Dynamic Test Run: The final validation is a controlled test run under simulated or actual operating conditions. Vibration and acoustic emissions are monitored. A post-test inspection of the contact pattern (now a polished “wear-in” pattern) provides definitive proof of correct meshing under load.
Application Case Study and Economic Impact Analysis
The practical application of this remanufacturing methodology demonstrates its efficacy. In a representative case, an aero-engine was experiencing high vibration levels. Spectral analysis of vibration signals pointed to a fault in the bevel gear stage, with pronounced sidebands and abnormal harmonic amplitudes suggesting localized damage and misalignment. Upon disassembly, the bevel gear set exhibited pitting and scuffing on the pitch line. The gears were evaluated and found to be within the remanufacturing acceptance criteria.
Following the outlined process flow—cleaning, crack inspection, profile modification grinding, shot peening, and comprehensive verification—the bevel gears were successfully restored. Post-remanufacturing inspection showed a case depth of 0.93 mm, surface hardness of 62.6 HRC, and a precise tooth profile. After assembly, backlash and contact patterns met all specifications. The engine test run was smooth, with vibration and noise levels significantly reduced and within acceptable limits. Subsequent field deployment of the remanufactured bevel gears has accumulated substantial service hours (e.g., 650-870 hours) without incident, confirming their reliability.
The economic and environmental advantages are substantial and quantifiable. The dominant cost in a new bevel gear is not the raw material (∼15%) but the “value-added” processes: forging, machining, heat treatment, and finishing (∼85%). Remanufacturing preserves this embedded value.
| Metric | New Bevel Gear | Remanufactured Bevel Gear | Saving / Benefit |
|---|---|---|---|
| Unit Cost | 100% (Baseline) | ~11.3% | ~88.7% cost reduction |
| Energy Consumption | 100% | ~14% | ~86% energy saving |
| Material Consumption | 100% | ~22% | ~78% material saving |
| Lead Time | Long (procurement) | Short (in-house process) | Reduced asset downtime |
| Environmental Impact | High (mining, smelting, processing) | Very Low | Reduced CO2, waste, and resource depletion |
From a broader perspective, implementing a bevel gear remanufacturing program transforms a linear consumption model (produce-use-dispose) into a circular one (produce-use-remanufacture-reuse). It ensures the continuity of supply for legacy engine platforms, reduces dependency on new part supply chains, and contributes directly to sustainable engineering practices by drastically lowering the carbon footprint and material intensity associated with component life-cycle.
Conclusion
Bevel gear remanufacturing, centered on the precise science of profile modification and supported by rigorous process control and validation, is a mature, reliable, and highly advantageous engineering practice. It is technically feasible, restoring the dynamic performance and load-bearing capacity of damaged gears. The established acceptance criteria allow for the salvage of a significant majority (often over 60%) of gears that would otherwise be scrapped. The process flow, from initial inspection through grinding, enhancement, and final testing, ensures that the remanufactured product meets or exceeds original performance specifications.
The economic argument is unequivocal, with cost savings exceeding 85% per unit. The environmental benefits, reflected in energy savings of ~86% and material savings of ~78%, make it a cornerstone of green manufacturing and life-cycle engineering strategies. For industries operating high-value capital assets like aircraft, the adoption of bevel gear remanufacturing is not merely a cost-saving tactic but a strategic imperative that enhances operational readiness, promotes sustainability, and preserves critical technical expertise in component lifecycle management.