
In the realm of power transmission systems, the gear shaft stands as a critical component, whose reliability and precision directly influence the overall performance, efficiency, and service life of the machinery. To achieve the necessary surface hardness, wear resistance, and high core toughness, carburizing followed by quenching remains the dominant heat treatment process for high-performance gear shafts. However, this thermochemical process, involving prolonged heating, carbon diffusion, and rapid cooling, inevitably introduces complex distortion. This distortion manifests as changes in dimensions and geometry, such as shrinkage, warpage, and profile errors, which can severely compromise the meshing accuracy, load distribution, and noise characteristics of the final assembly. For large-scale gear shafts characterized by significant cross-sectional variations and substantial face width, the challenge of distortion control is magnified. The differential cooling rates between the bulky central regions and the ends or thinner sections lead to pronounced thermal and transformational stresses, often resulting in unacceptable, hard-to-predict deformations like a “saddle-shaped” profile across the tooth face width. Traditionally, reliance has been placed on empirical process adjustments and allocating excessive machining allowances during final finishing (e.g., grinding) to compensate for this distortion. These approaches are not only costly and wasteful but also introduce secondary problems such as non-uniform case depth and hardness on the finished tooth flank, ultimately undermining the component’s designed performance.
The advent of sophisticated numerical simulation techniques, particularly Finite Element Analysis (FEA), has revolutionized the approach to this longstanding challenge. By creating a coupled thermo-metallurgical-mechanical model, it is now possible to virtually simulate the entire carburizing, quenching, and tempering sequence. This digital twin approach allows for a detailed investigation of the transient temperature fields, phase transformations, stress evolution, and resulting distortion throughout the process. Consequently, it enables engineers to diagnose the root causes of distortion in existing processes and proactively design optimized heat treatment strategies—such as modified heating cycles, alternative quenching media, and specialized fixtures—to achieve precise control over the final geometry of the gear shaft. This study employs a systematic FEA-based methodology to analyze and subsequently control the distortion of a large alloy steel gear shaft, transitioning from a problematic conventional oil quench to a precisely controlled salt bath quenching process.
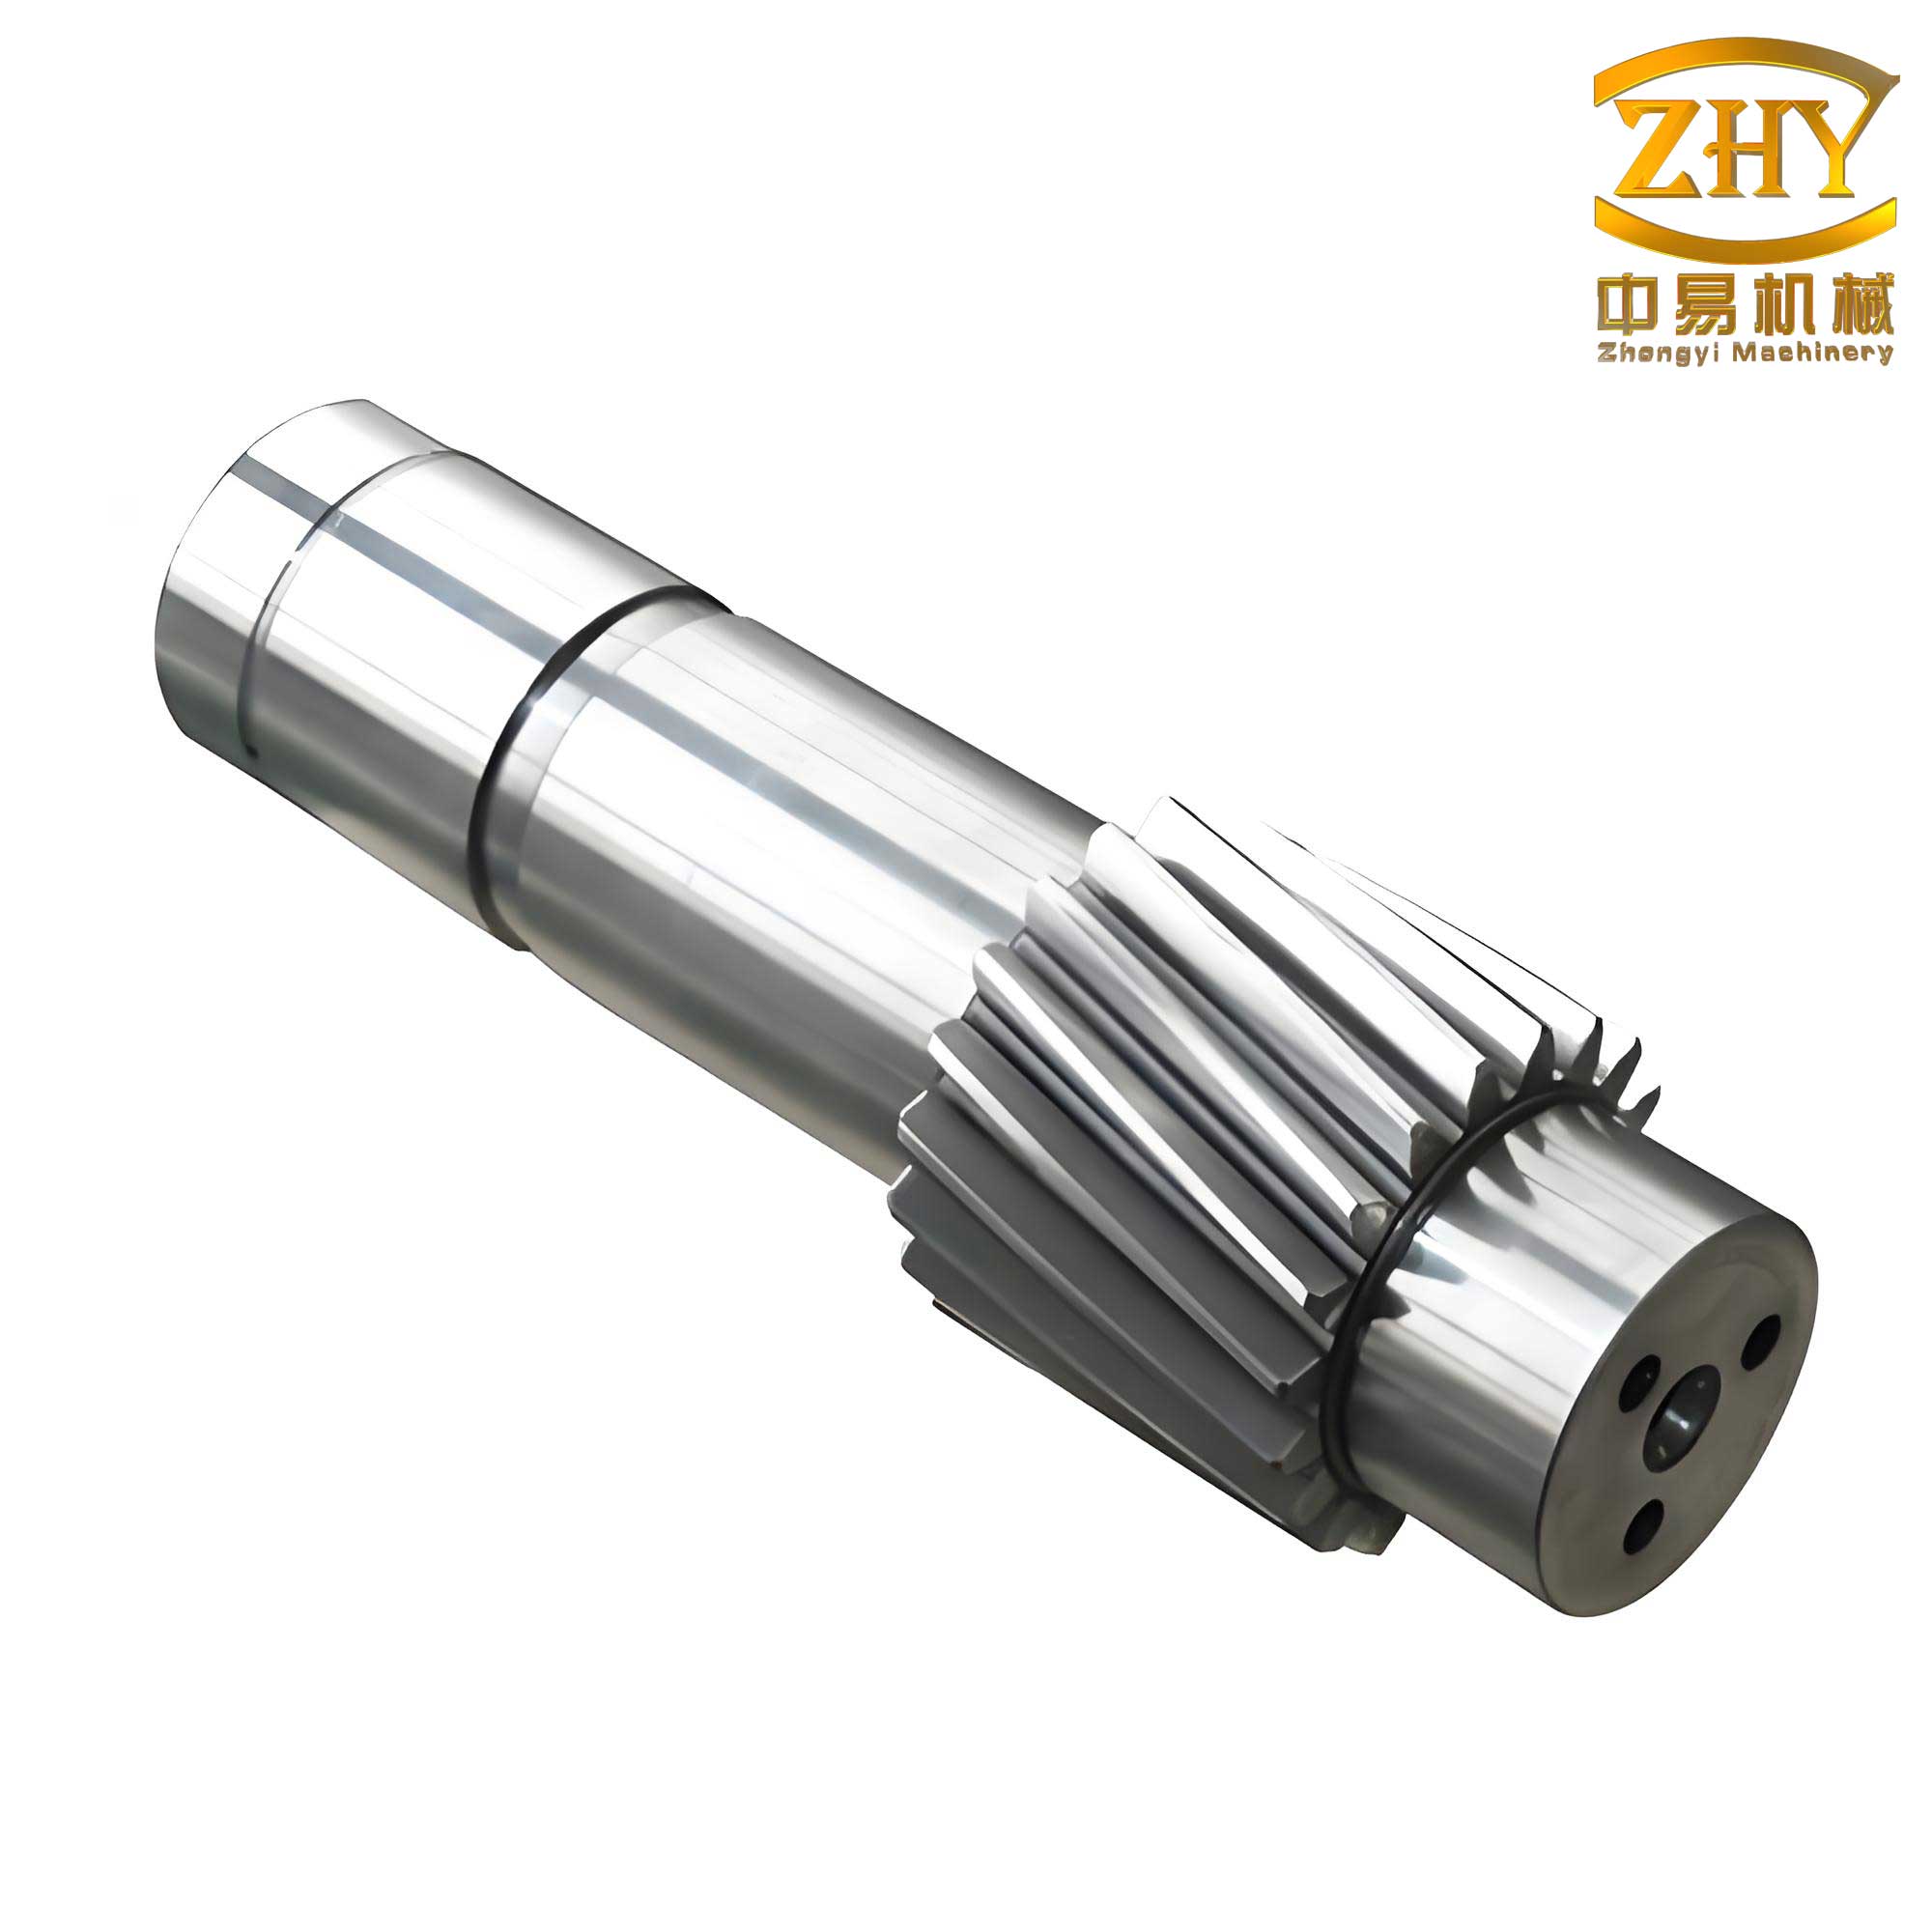
1. Gear Shaft Model Specifications and Finite Element Setup
The subject of this investigation is a large gear shaft manufactured from the low-alloy carburizing steel 17CrNiMo6. The chemical composition of this material, crucial for defining its transformation kinetics and hardenability in the simulation, is provided in Table 1.
| C | Si | Mn | Cr | Mo | Ni | Fe |
|---|---|---|---|---|---|---|
| 0.17 | 0.27 | 0.65 | 1.61 | 0.29 | 1.57 | Bal. |
The key geometrical parameters of the gear shaft are as follows: module M = 22 mm, number of teeth Z = 23, tip diameter ≈ 550 mm, and a substantial face width of B = 400 mm. The shaft is assumed to be suspended vertically from one end during the heat treatment process. The technical requirements for the case-hardened gear shaft specify an effective case depth (ECD) of 5.0 – 5.5 mm, measured perpendicular to the tooth flank at a hardness threshold corresponding to 550 HV. The distortion limits are stringent: the maximum concave distortion (sinking) at the center of the tooth face width should not exceed 1.5 mm, and the overall warpage (the difference in radial shrinkage between the center and the ends) must be less than 1.5 mm.
To ensure computational efficiency while maintaining accuracy, a symmetry-based simplification was employed. Due to the geometric symmetry of the gear shaft, a single-tooth sector representing half of the face width (200 mm) was modeled. The mesh was generated using tetrahedral elements, with a high degree of refinement in the tooth region where steep thermal and carbon gradients are expected. The final model consisted of approximately 60,000 elements. Appropriate boundary conditions were applied: symmetric constraints on the mid-face-width cross-section and the two radial faces of the tooth sector, and a fixed constraint at the shaft end to simulate the hanging condition.
The core of the simulation involves solving coupled governing equations. The temperature field $T(\mathbf{x}, t)$ is governed by the transient heat conduction equation with a heat source term accounting for the latent heat of phase transformations:
$$\rho c_p \frac{\partial T}{\partial t} = \nabla \cdot (k \nabla T) + \dot{Q}_{latent}$$
where $\rho$ is density, $c_p$ is specific heat, $k$ is thermal conductivity, and $\dot{Q}_{latent}$ is the latent heat generation rate.
The carbon diffusion during carburizing is modeled using Fick’s second law:
$$\frac{\partial C}{\partial t} = \nabla \cdot (D(C, T) \nabla C)$$
where $C$ is the carbon concentration and $D$ is the carbon diffusion coefficient, which is strongly dependent on both carbon content and temperature.
The phase transformation kinetics, particularly for the diffusion-controlled formation of pearlite and the diffusionless martensitic transformation, are modeled using time-temperature-transformation (TTT) data and the Koistinen-Marburger relationship:
$$V_m = 1 – \exp[-\alpha(M_s – T)]$$
where $V_m$ is the volume fraction of martensite, $M_s$ is the martensite start temperature (a function of carbon content), $T$ is the temperature, and $\alpha$ is a material constant.
The total strain rate $\dot{\boldsymbol{\epsilon}}_{total}$ is decomposed into elastic, plastic, thermal, and transformational components:
$$\dot{\boldsymbol{\epsilon}}_{total} = \dot{\boldsymbol{\epsilon}}_{el} + \dot{\boldsymbol{\epsilon}}_{pl} + \dot{\boldsymbol{\epsilon}}_{th} + \dot{\boldsymbol{\epsilon}}_{tr}$$
The transformational strain $\dot{\boldsymbol{\epsilon}}_{tr}$ is critical and is related to the volumetric change associated with the austenite-to-martensite transformation. The stress field $\boldsymbol{\sigma}$ is then solved using the incremental theory of plasticity, obeying the yield criterion and flow rule.
2. Analysis of Initial Process: Conventional Carburizing and Oil Quenching
The initial, conventional process was simulated to establish a baseline. The carburizing cycle consisted of a strong carburizing stage at 920°C with an atmosphere carbon potential of 1.2% C for 40 hours, followed by a diffusion stage at the same temperature but with a reduced carbon potential of 0.8% C for 20 hours. This was followed by a slow furnace cool. The FEA results for the carbon profile are shown in Figure 2. The simulation predicted a surface carbon content of approximately 0.79% at the tooth tip. The carbon gradient from the mid-face-width position into the core confirmed that the effective case depth (to 0.35% C) was about 5.2 mm, well within the specified 5.0–5.5 mm range. This validated the carburizing model and confirmed that the initial carburizing schedule was functionally adequate for achieving the required case depth on the gear shaft.
The subsequent quenching process employed a conventional fast quenching oil at 60°C. The cooling curve and corresponding heat transfer coefficient (HTC) for the oil were critical inputs. The oil quench was simulated for a duration of 1 hour. The metallurgical output revealed a critical issue: due to the high hardenability of the 17CrNiMo6 steel and the significant mass of the gear shaft, the entire tooth section transformed to a high fraction of martensite (exceeding 90% at the surface). While this achieves high hardness, the associated volumetric expansion from austenite to martensite is substantial and a primary driver of distortion.
The distortion results from the oil quench process were alarming. The radial shrinkage of the tooth tip diameter was not uniform across the face width. A pronounced “saddle” or “hourglass” distortion pattern was observed. The maximum shrinkage, occurring at the center of the face width, was calculated to be 2.2 mm. In contrast, the shrinkage near the free ends of the tooth was only about 0.8 mm. This resulted in a concave distortion at the center of 1.4 mm ( (2.2-0.8)/2 ) and a warpage of 1.4 mm, both values perilously close to and exceeding the specified limit of 1.5 mm. The post-quench distortion state of the gear shaft was therefore deemed unacceptable.
A detailed analysis of the stress field provided the root cause. Figure 5 shows the stress distribution along the tooth tip line from the center to the end after oil quenching. A significant gradient in both magnitude and sign was evident. The central region (from the midpoint to about 150mm along the face width) was under high compressive stress, peaking at approximately -116 MPa. From 150mm to the end, the stress transitioned to tensile, reaching about +29 MPa at the very end. This stark contrast is a direct consequence of the differential cooling. The massive center of the gear shaft cools more slowly than the ends. However, when the martensite transformation finally occurs in the center, it is constrained by the already-transformed and cooler ends, generating high compressive stresses in the center and reactive tensile stresses at the ends. This non-uniform stress state is the mechanical origin of the saddle-shaped distortion. It is noteworthy that the distortion state of the gear shaft after carburizing and before the final quench was minimal (max ~0.45 mm and without the saddle pattern), confirming that the majority of the problematic distortion occurred during the quenching phase.
3. Design and Analysis of the Optimized Process: Controlled Heating and Salt Bath Quenching
Based on the FEA diagnosis, the optimization strategy focused on two key aspects: 1) Reducing thermal gradients during heating to minimize thermal stress before quenching, and 2) Modifying the quenching medium and method to reduce both thermal shock and transformational stresses.
3.1 Optimized Heating Cycle: To mitigate heating-induced stresses, a stepped heating approach was implemented. Instead of direct heating to the austenitizing temperature, the gear shaft is first heated to 560°C and held for 3 hours to equalize temperature. It is then slowly heated further to the final austenitizing temperature, which was also lowered from 850°C (typical for direct oil quenching) to 820°C. This lower temperature reduces the thermal energy that must be extracted and minimizes the temperature difference between surface and core at the start of quenching, thereby reducing thermal stress.
3.2 Salt Bath Quenching Process: The most significant change was the substitution of oil quenching with a salt bath (nitrate-nitrite) martempering process. The cooling characteristics of the salt bath are fundamentally different from oil. Figure 7 compares the heat transfer coefficients. The salt bath (a typical mixture of 55% KNO3 + 45% NaNO2 with ~0.7% water) exhibits a much higher maximum HTC (~22 kW/m²·K) occurring at a higher temperature (around 560°C), whereas the fast oil has a lower maximum HTC (~5.6 kW/m²·K) at a lower temperature (~450°C). This means the salt bath extracts heat very rapidly in the high-temperature austenite region, helping to avoid the formation of soft transformation products. However, its cooling rate in the low-temperature martensite transformation range is significantly milder than oil. In the martempering process, the gear shaft is quenched into the salt bath held at a temperature just above the Ms point (e.g., 180°C), held until the temperature equalizes throughout the cross-section, and then air-cooled. This allows the lower-carbon core to transform to martensite first, followed by the higher-carbon case transforming during the slower air cool, thereby reducing the transformational stresses that cause distortion.
The optimized quenching sequence was simulated as: Quench into 180°C salt bath for 2 hours (simulating temperature equalization), followed by air cooling to room temperature. This was followed by a low-temperature tempering at 180°C for 12 hours to relieve stresses and stabilize the microstructure.
4. Results of the Optimized Process and Comparative Assessment
The FEA results for the optimized process demonstrated a remarkable improvement in the distortion behavior of the gear shaft. The saddle-shaped distortion was drastically reduced. The maximum radial shrinkage at the tooth center was reduced from 2.2 mm to 1.41 mm. The shrinkage at the ends was also reduced to about 0.5 mm. This translates to a concave distortion at the center of approximately 0.91 mm ( (1.41-0.5)/2 ) and a warpage of 0.91 mm. Both values are now well within the 1.5 mm specification limit. A direct quantitative comparison is presented in Table 2.
| Process | Max Shrinkage (Center) | Shrinkage (End) | Calculated Concave | Calculated Warpage | Within Spec? |
|---|---|---|---|---|---|
| Conventional Oil Quench | 2.20 mm | 0.80 mm | 1.40 mm | 1.40 mm | No |
| Optimized Salt Bath Quench | 1.41 mm | 0.50 mm | 0.91 mm | 0.91 mm | Yes |
The stress distribution after the salt bath process was also significantly more favorable. While a stress gradient still existed, the magnitude of both compressive and tensile stresses was greatly diminished, and the transition was more gradual. This directly correlates with the reduced distortion. The successful outcome of the simulation was validated in production. The implemented salt bath martempering process consistently produced gear shaft components meeting the distortion specifications. This allowed for a rational reduction of the final grinding allowance from a previously over-sized margin to a precisely determined 1.5 mm. This reduction minimizes the amount of the hardened case removed during finishing, ensuring more uniform case depth and hardness on the final tooth flank, while also reducing grinding time, wheel wear, and overall manufacturing cost.
5. Conclusion
This comprehensive study underscores the powerful synergy between advanced computational modeling and practical heat treatment engineering for solving complex industrial problems. The application of coupled Finite Element Analysis provided an in-depth, causal understanding of the severe saddle-shaped distortion encountered in a large 17CrNiMo6 gear shaft during conventional carburizing and oil quenching. The simulation identified the core issue: the large face width led to drastic differences in cooling rates and martensite transformation timing between the central region and the ends, generating a steep and non-uniform residual stress profile that manifested as unacceptable geometric distortion.
Guided by this virtual diagnosis, a targeted process optimization was designed and simulated. The solution involved a dual-strategy approach: (1) implementing a controlled, stepped heating cycle to minimize pre-quench thermal stresses, and (2) fundamentally changing the quenching mechanism from oil to a nitrate salt bath martempering process. The salt bath’s characteristic cooling curve—rapid cooling above the martensite start temperature and slow cooling through the transformation range—proved to be exceptionally effective in homogenizing cooling and mitigating the detrimental transformational stresses.
The FEA results of the optimized process predicted a dramatic improvement, reducing the central concave distortion from 1.40 mm to 0.91 mm and the warpage from 1.40 mm to 0.91 mm, both within the strict 1.5 mm tolerance. Subsequent industrial implementation confirmed the model’s accuracy, leading to a reliable and repeatable production process. Beyond meeting the distortion specification, this optimization yielded significant secondary benefits: it enabled a precise and minimized grinding allowance, which in turn ensures superior consistency in the final case depth and hardness of the gear shaft tooth flanks and reduces overall finishing costs. This methodology establishes a robust framework for the distortion-by-design of complex, safety-critical carburized components.