
In my extensive experience with power transmission components, the sudden and unpredictable failure of large-scale gear shafts presents a particularly challenging and costly problem for manufacturers. The case I will discuss involves a series of longitudinal cracks discovered in multiple gear shafts post-assembly, load testing, and even after delivery. These failures, occurring after the components had ostensibly passed rigorous power loading tests up to 1660 kW, created significant technical and logistical difficulties. My investigation focused on a detailed forensic analysis of three such failed gear shafts to uncover the underlying metallurgical and processing causes. The gear shafts in question were manufactured from a steel grade equivalent to 18CrNiMo7-6, processed from bar stock, machined, and subjected to carburizing, quenching, and low-temperature tempering at 170°C.
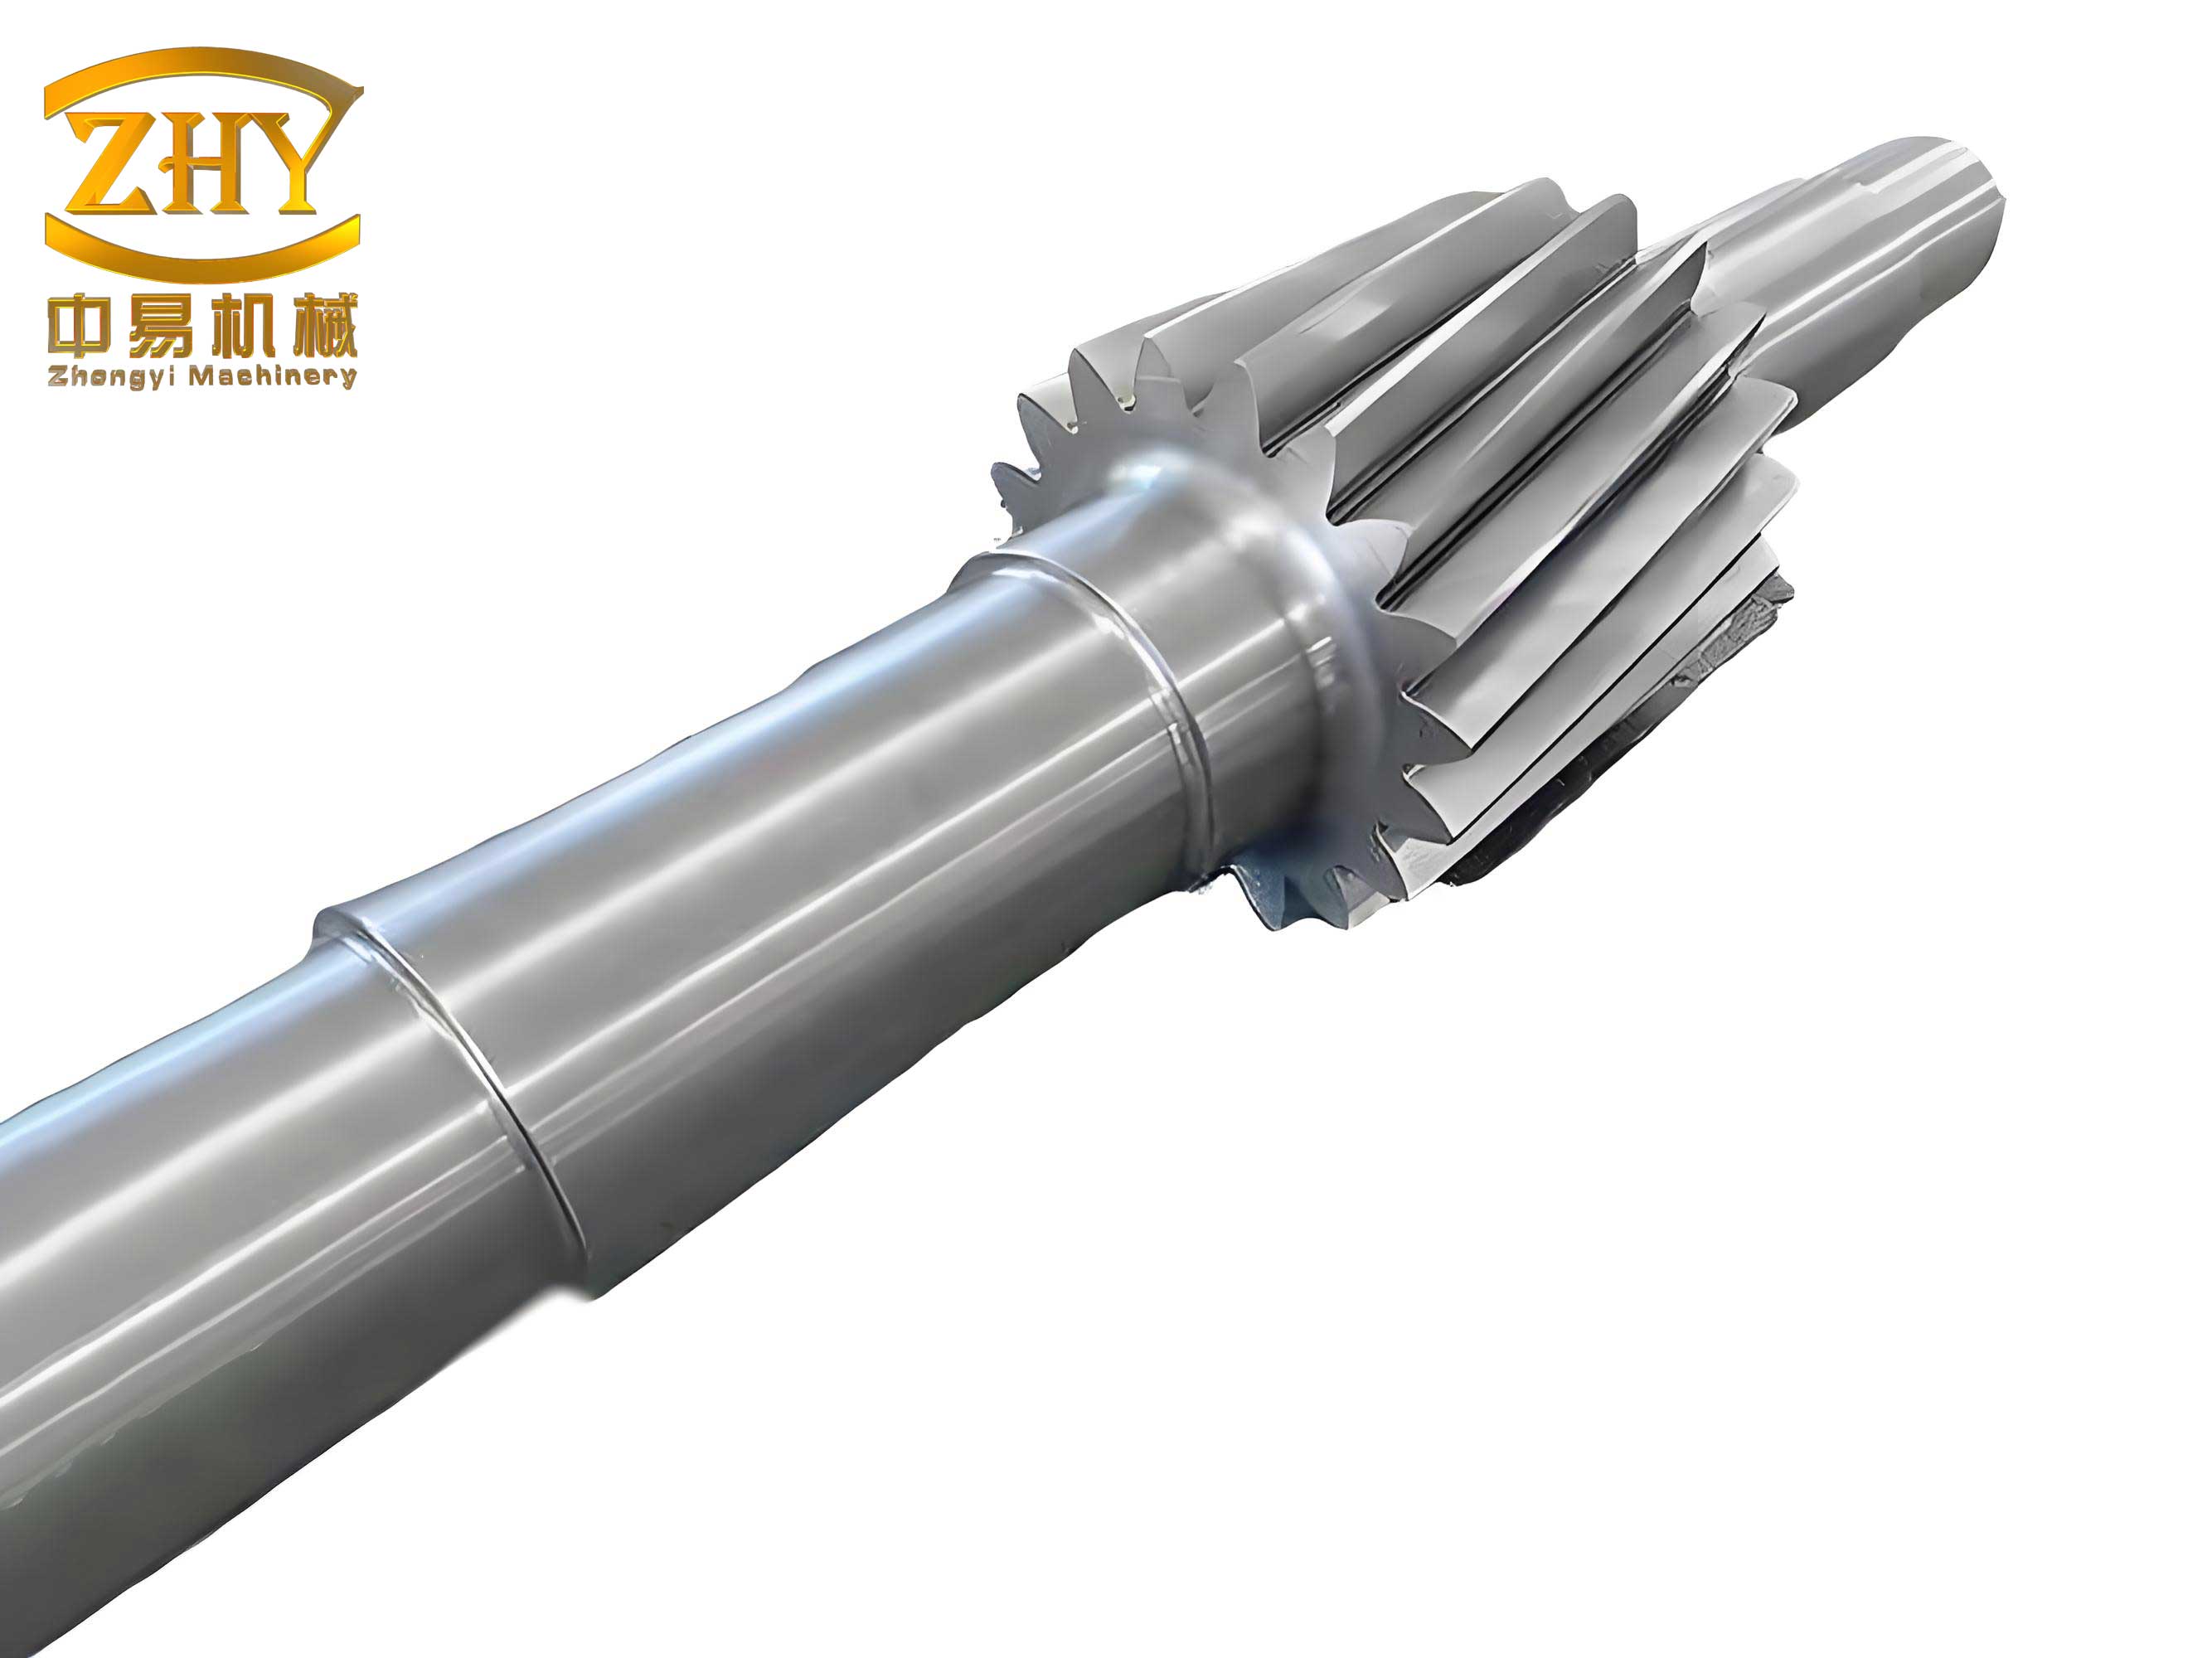
My methodology was comprehensive, involving a systematic examination of fracture surfaces, chemical composition, macro- and micro-structure, hardness depth profiles, and residual stress states. The primary goal was to identify the sequence of failure and pinpoint the root cause to prevent future occurrences in these critical gear shaft components.
Analytical Methodology and Detailed Findings
The investigation began with a macroscopic examination, followed by progressively higher-magnification techniques to build a complete picture of the failure mechanism affecting the gear shaft integrity.
1. Chemical Composition Verification
The first step was to verify that the base material met specification requirements. Spectroscopic analysis was performed on samples extracted from the failed gear shaft bodies. The results, compared against the standard for 18CrNiMo7-6 steel, are summarized in Table 1. Notably, the hydrogen content was found to be very low (< 0.7 ppm), effectively ruling out classical hydrogen embrittlement as a primary cause.
| Element | Analyzed Value | 18CrNiMo7-6 Specification | Conformance |
|---|---|---|---|
| C | 0.15 | 0.15 – 0.20 | Yes |
| Si | 0.23 | ≤ 0.40 | Yes |
| Mn | 0.53 | 0.50 – 0.90 | Yes |
| Cr | 1.69 | 1.50 – 1.80 | Yes |
| Ni | 1.52 | 1.40 – 1.70 | Yes |
| Mo | 0.26 | 0.25 – 0.35 | Yes |
| Al | 0.048 | 0.02 – 0.05 | Yes |
| H (ppm) | 0.7 | ≤ 2.0 | Yes |
2. Fractography and Crack Initiation Site Analysis
All failed gear shaft components exhibited similar macroscopic crack morphology: a longitudinal crack running parallel to the axis, propagating through the helical gear teeth and often spanning the entire length of the shaft. The cracks were straight, unbranched, and exhibited significant opening displacement, characteristics reminiscent of quench cracking. Upon opening the cracks, fractographic analysis revealed a critical and consistent feature: the fracture originated not at the surface, but at subsurface locations. The crack initiation sites were consistently associated with large, non-metallic inclusions located several millimeters beneath the surface, within the coarse-diameter section of the gear shaft. The relevant data for the three analyzed shafts is consolidated in Table 2.
| Gear Shaft Sample | Initiation Site Location | Depth from Surface (mm) | Inclusion Length (μm) | Inclusion Width (μm) |
|---|---|---|---|---|
| 1 | Gear Tooth Region | 2.2 | 1200 | 55 |
| 2 | Relief Groove Region | 12.0 | 3000 | 250 |
| 3 | Relief Groove Region | 13.0 | 4300 | 430 |
Scanning Electron Microscopy (SEM) and Energy Dispersive X-ray Spectroscopy (EDS) confirmed these inclusions were primarily aluminum oxides (Al2O3). A clear correlation was observed: the deeper the initiation site, the larger the critical inclusion size required to trigger a crack. The microscopic fracture mode was predominantly intergranular in the carburized case region and near the inclusion interface, transitioning to transgranular quasicleavage in the non-carburized core. No evidence of classical fatigue striations was found, indicating a non-cyclic failure mode.
3. Microstructural Evaluation
Macro-etching revealed a relatively uniform structure with only slight ingot segregation. However, detailed microstructural examination uncovered a significant issue: severe banding. After a special 860°C anneal to highlight segregation, the structure showed extensive, continuous bands of ferrite, rated as a severe Level 4 per relevant standards. The core microstructure consisted of tempered lath martensite with a prior austenite grain size of 8.0, which is acceptable. The carburized layer showed acicular martensite. While random non-metallic inclusions (B-type and D-type) were observed in longitudinal sections, none as large as those found at the crack origins were seen in the sampled planes, highlighting the statistical nature of this defect.
4. Hardness and Case Depth Profile
Micro-hardness traverses were performed from the tooth root surface towards the core. The effective case depth (550 HV) was approximately 1.4 mm, with a total hardened layer influencing properties extending to about 2.5 mm. The core hardness averaged 430 HV0.5 but exhibited significant scatter (350-450 HV0.5), directly attributable to the severe microstructural banding. The hardness profile can be modeled by an exponential decay function, where the hardness $H(d)$ at depth $d$ from the surface is approximated by:
$$ H(d) = H_{core} + (H_{surface} – H_{core}) \cdot e^{-k d} $$
where $H_{surface}$ is the surface hardness (~700 HV), $H_{core}$ is the core hardness (~430 HV), and $k$ is a constant defining the decay rate related to carburizing parameters.
5. Residual Stress Analysis
X-ray diffraction measurements on the cross-section after cracking showed a complex residual stress state, but it was largely relaxed due to the crack itself. To estimate the original, pre-crack stress, I performed a simple elastic back-calculation based on the measured crack opening displacement (COD). Modeling the gear shaft as a thick-walled cylinder under a uniform tangential stress, the COD at the surface relates to the original stress. For a through-thickness longitudinal crack, the relationship between the original residual hoop stress $\sigma_{\theta}$ and the measured crack opening $u$ can be simplified as:
$$ u \approx \frac{\sigma_{\theta} \cdot \pi \cdot a}{E} $$
where $a$ is the effective crack length (radius of the shaft) and $E$ is Young’s modulus. Using this approach, the original macroscopic residual tensile stress in the hoop direction near the subsurface region was estimated to be approximately 500 MPa. This high tensile stress exists in the transition zone between the carburized case (in compression) and the core due to differential volume expansion during martensitic transformation.
Synthesis and Discussion: The Mechanism of Delayed Cracking
Integrating all findings, the failure mechanism for these gear shaft components is classified as delayed quench cracking driven by热处理残余应力. The timeline and physics of the failure can be described as follows:
- Stress State Creation: During the quenching process after carburizing, the high-carbon case transforms to martensite first, expanding in volume. The lower-carbon core transforms later, imposing a tensile hoop stress on the already hardened and contracted case. The peak of this tensile residual stress field is located in the subsurface transition zone, precisely where the carbon gradient levels off to the core level. The estimated 500 MPa stress is a significant portion of the material’s yield strength.
- Stress Concentration at Defects: The subsurface region of peak tensile stress contained large, brittle alumina inclusions. These inclusions act as potent stress raisers. The stress concentration factor $K_t$ for an elliptical flaw oriented perpendicular to the stress direction is given by:
$$ K_t = 1 + 2\sqrt{\frac{a}{\rho}} $$
where $a$ is the flaw’s major semi-axis (length/2) and $\rho$ is the radius of curvature at its tip. For the observed inclusions with sharp edges ($\rho \rightarrow 0$), $K_t$ becomes very large, locally amplifying the 500 MPa stress to levels exceeding the cohesive strength of the matrix-inclusion interface or the surrounding embrittled microstructure. - Crack Initiation and Subcritical Growth (Delayed Period): Cracks initiate at these inclusions but do not cause instantaneous failure. The surrounding tempered martensite, especially given the high core hardness and severe banding, exhibits high susceptibility to delayed fracture under sustained tensile stress. The banded structure, with its alternating hard and soft zones, creates micro-plasticity constraints and localized stress incompatibilities that further promote crack initiation and slow, stable growth. This accounts for the “delay” where the gear shaft passes load tests but fails later during storage or transit. The load test itself may have contributed minor cyclic loads that assisted in breaching the final barriers to crack initiation from the inclusion.
- Final Fast Fracture: Once the initiated crack reaches a critical size, defined by the fracture toughness $K_{IC}$ of the material and the applied stress $\sigma$, it propagates catastrophically. The critical flaw size $a_c$ is approximated by:
$$ a_c \propto \left( \frac{K_{IC}}{\sigma} \right)^2 $$
The combination of high residual stress and the initial inclusion size likely brought the component very close to this critical state, leading to final rapid crack propagation through the core, resulting in the observed longitudinal split.
The correlation in Table 2 is key: in the region of maximum stress (~2-3 mm depth), even a relatively small inclusion (~55 µm wide) can initiate a crack. Deeper, where the residual stress is lower, a much larger inclusion is required to create the necessary local stress intensity to trigger failure. This explains why the origins were found at different depths.
Conclusions and Engineering Recommendations
My investigation conclusively determines that the failure of these large gear shaft components was caused by delayed cracking initiated at subsurface non-metallic inclusions under the influence of high热处理残余应力. The problem was exacerbated by severe microstructural banding and a relatively high core hardness, which increased the material’s susceptibility to this failure mode.
To prevent recurrence in future gear shaft production, a multi-faceted approach is essential:
| Root Cause | Impact | Recommended Mitigation Strategy |
|---|---|---|
| Subsurface Macro-Inclusions (Al2O3) | Acts as stress concentrator and direct crack initiator in the high-stress zone. |
|
| Severe Microstructural Banding | Reduces transverse ductility and toughness, promotes uneven stress distribution and crack path guidance. |
|
| High Residual Stress & Core Hardness | Provides the driving force for crack propagation; high hardness lowers fracture toughness. |
|
In summary, securing the reliability of these high-value gear shaft components requires a shift in quality control focus from solely final inspection to proactive control of material internal quality and optimized heat treatment parameters. The solution lies not in any single action, but in the synergistic implementation of cleaner steel practices, strict microstructural control, and a heat treatment process designed to minimize both hardness and the resultant detrimental stress state in the final gear shaft.