
As a mechanical engineer specializing in high-precision transmission components, I have extensively analyzed the challenges associated with machining central holes in hollow gear shafts for new energy vehicle transmissions. The gear shaft is a critical component, and its accuracy directly impacts the performance, efficiency, and noise levels of the transmission system. In this article, I will delve into the factors influencing the machining of 60° conical central holes on hollow gear shafts, and present optimized工艺 approaches that enhance precision, reduce coaxiality errors, and provide a reliable定位基准 for subsequent grinding operations. The gear shaft, particularly in hollow configurations, demands meticulous attention to detail due to its sensitivity to thermal and mechanical deformations.
The hollow gear shaft, such as those used in the 1T15E new energy transmission, operates at input speeds exceeding 9000 r/min, necessitating gear accuracy levels of 4 to 6 grades. To achieve this, the central holes at both ends of the gear shaft serve as the primary定位基准 for精加工 processes like gear grinding and external cylindrical grinding. Any imperfections in these central holes—such as deviations in depth, cone angle, roundness, surface roughness, or coaxiality—can propagate errors, leading to misalignment, increased radial runout, and compromised transmission quality. This analysis focuses on optimizing the entire process chain, from initial turning to post-heat treatment grinding, ensuring that the gear shaft meets stringent automotive standards.
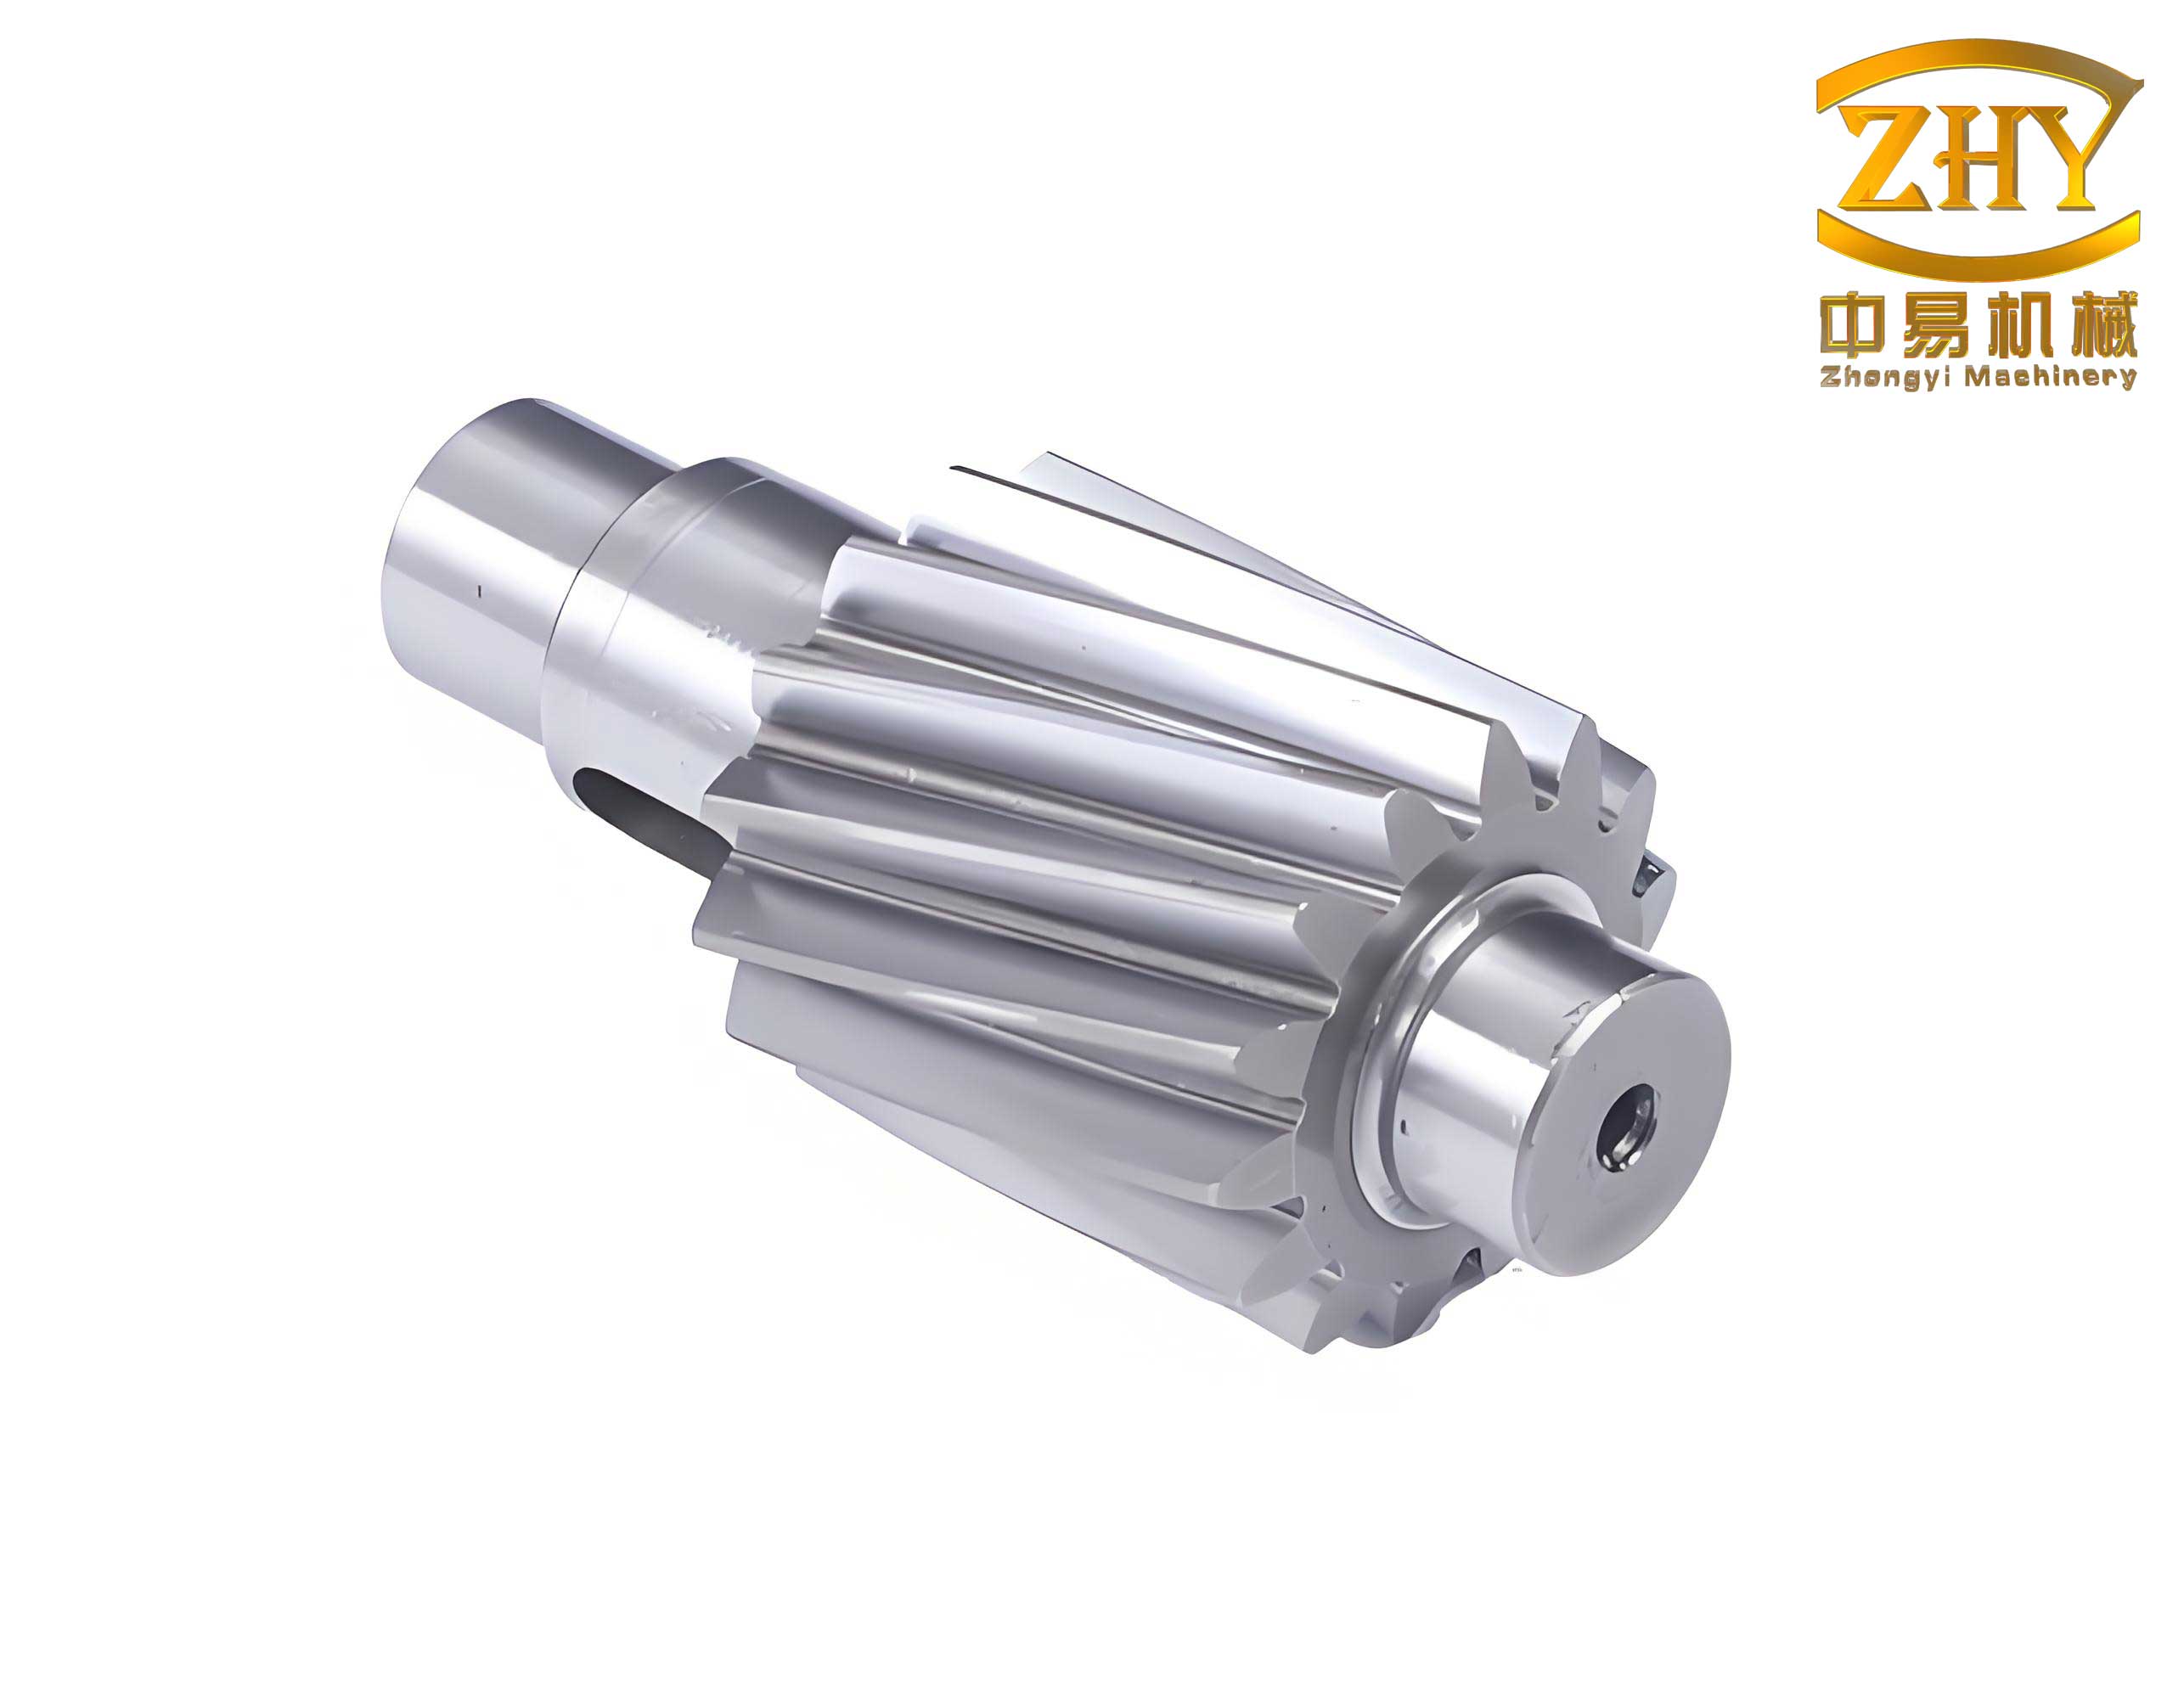
In the manufacturing of hollow gear shafts, the initial machining of central holes is typically performed on CNC lathes. However, several factors contribute to errors: selection of定位基准, clamping methods, tool wear, and thermal effects. For instance, when machining the first central hole, the gear shaft is often clamped using a three-jaw self-centering chuck based on the rough-turned outer cylindrical surface, which may have inherent runout. When machining the second central hole after flipping the gear shaft, the already finished outer surface provides a better基准, but inconsistencies can arise due to clamping forces and alignment issues. This leads to coaxiality errors between the two central holes, expressed as radial runout and roundness deviations. To quantify this, the coaxiality error (ΔC) can be modeled as a function of radial runout (ΔR) and roundness error (ΔO): $$ \Delta C = \sqrt{(\Delta R)^2 + (\Delta O)^2} $$ where ΔR is the maximum radial displacement from the ideal axis, and ΔO is the variation in radius measured around the circumference. For a gear shaft, minimizing ΔC is crucial for ensuring that subsequent grinding operations produce concentric features.
To address these issues, I have optimized the CNC turning process for central holes on the hollow gear shaft. First, the定位基准 selection is refined: the rough-turned outer cylindrical section is used only for initial粗加工, after which a精加工 step is performed on one end, including its central hole, using the same setup to ensure concentricity. Then, for the opposite end, the gear shaft is re-clamped using the finished outer surface as the基准, reducing runout to below 0.02 mm. Additionally, the CNC program is adjusted to compensate for tool deflection and thermal expansion during cutting. The cutting trajectory for the 60° cone is modified to achieve a more accurate angle, and the夹具 is calibrated to have end and radial runouts under 0.01 mm. Before clamping, compressed air is used to clean both the chuck jaws and the gear shaft’s定位 surfaces to prevent debris-induced misalignment. This reduces angular errors in the central hole cone, which ideally should be $$ \theta = 60^\circ \pm 0.5^\circ $$ but often deviates due to process variability.
After CNC turning, the gear shaft undergoes heat treatment, such as carburizing and quenching, which introduces significant deformations. The hollow structure, with thin and uneven wall thickness, causes the central hole to expand and lose roundness. Based on empirical data, the cone angle typically increases by 20′ to 40′, and roundness degrades by up to 20 μm. To compensate, I have implemented a pre-变形 adjustment in the CNC turning phase: the cone angle is intentionally machined slightly smaller, for example, at $$ \theta_{\text{pre}} = 60^\circ – 0.5^\circ $$ to account for post-heat treatment expansion. This proactive measure reduces the material removal required during subsequent grinding, preserving the integrity of the gear shaft. The thermal deformation can be approximated using a linear expansion model: $$ \Delta \theta = \alpha \cdot \Delta T \cdot L $$ where α is the coefficient of thermal expansion for the gear shaft material (e.g., alloy steel), ΔT is the temperature change during quenching, and L is the effective length of the conical section. By characterizing this for specific gear shaft geometries, we can fine-tune the pre-compensation.
The design of the central hole itself is also optimized. Instead of a standard A-type center, a B-type central hole with a 120° protective cone is adopted for the hollow gear shaft. This design offers multiple benefits: it protects the 60° working surface from damage during handling, reduces the effective contact area susceptible to thermal distortion, and facilitates easier grinding post-heat treatment. The effective contact length (h) of the 60° cone is critical; it can be calculated based on the gear shaft’s diameter and load requirements: $$ h = \frac{D}{2 \cdot \tan(30^\circ)} $$ where D is the nominal diameter at the central hole. By minimizing h, we localize wear and improve accuracy during定位. This optimization is particularly important for high-speed gear shafts where dynamic balance is paramount.
Following heat treatment, the central hole must be reground to restore precision. I have implemented a post-heat treatment grinding process using a dedicated center hole grinder. In this setup, the gear shaft is positioned with its lower central hole on a tailstock center, while the upper end is supported by a节圆夹具 that clamps onto the gear teeth’s pitch circle. This ensures that the grinding基准 aligns with the functional axis of the gear shaft, reducing cumulative errors. The grinding wheel rotates at high speed (approximately 30 m/s) and oscillates along the 30° half-angle of the cone. The material removal rate is controlled precisely, with feed rates kept between 0.005 and 0.010 mm/s to avoid overheating and ensure surface integrity. The grinding depth per pass is limited to 0.05 mm, which minimizes residual stresses on the gear shaft. The roundness improvement can be described by a wear model: $$ \Delta O_{\text{final}} = \Delta O_{\text{initial}} \cdot e^{-k \cdot t} $$ where k is a grinding efficiency constant, and t is the grinding time. This exponential decay highlights the effectiveness of fine grinding for achieving roundness under 3 μm.
To illustrate the impact of these optimizations, I have compiled data from multiple production runs of the hollow gear shaft. The tables below summarize key measurements before and after process improvements.
| Gear Shaft End | Roundness at Small End (μm) | Roundness at Large End (μm) | Cone Angle | Surface Roughness Ra (μm) | Outer Roundness at Hole Location (μm) |
|---|---|---|---|---|---|
| Internal Spline End | 5.44 | 6.66 | 62°16′48″ | ≤3.2 | 5.22 |
| Opposite End | 12.80 | 14.29 | 59°57′54″ | ≤3.2 | 9.07 |
| Gear Shaft End | Roundness at Small End (μm) | Roundness at Large End (μm) | Cone Angle | Surface Roughness Ra (μm) | Outer Roundness at Hole Location (μm) |
|---|---|---|---|---|---|
| Internal Spline End | 11.48 | 12.42 | 62°54′49″ | ≤3.2 | 14.68 |
| Opposite End | 14.80 | 20.29 | 60°18′55″ | ≤3.2 | 11.07 |
| Gear Shaft Sample | Roundness at Small End (μm) | Roundness at Large End (μm) | Cone Angle | Surface Roughness Ra (μm) | Radial Runout After External Grinding (μm) |
|---|---|---|---|---|---|
| Sample 1 (Internal Spline End) | 5.29 | 5.40 | 59°45′3″ | ≤0.4 | 1.41 |
| Sample 1 (Opposite End) | 2.50 | 3.04 | 59°46′46″ | ≤0.4 | 1.49 |
| Sample 2 (Internal Spline End) | 2.65 | 6.67 | 59°51′32″ | ≤0.4 | 2.60 |
| Sample 2 (Opposite End) | 1.97 | 2.07 | 59°43′45″ | ≤0.4 | 3.33 |
| Sample 3 (Optimized Internal Spline End) | 1.67 | 2.15 | 60°03′22″ | ≤0.4 | 2.03 |
| Sample 3 (Optimized Opposite End) | 2.87 | 1.96 | 59°59′06″ | ≤0.4 | 2.62 |
The data clearly demonstrates that post-heat treatment grinding significantly enhances central hole accuracy. For instance, roundness is reduced to below 3 μm, cone angle is controlled within $$ \theta = 60^\circ \pm 4′ $$, and surface roughness improves to Ra ≤ 0.4 μm. This directly translates to better performance during external grinding of the gear shaft, where radial runout is consistently kept under 3 μm. The relationship between central hole quality and final gear accuracy can be expressed using a transfer function: $$ \Delta G = k_1 \cdot \Delta C + k_2 \cdot \Delta R_s $$ where ΔG is the gear tooth error, ΔC is the central hole coaxiality error, ΔR_s is the surface roughness of the central hole, and k1, k2 are influence coefficients specific to the gear shaft geometry and grinding process. By minimizing ΔC and ΔR_s, we achieve higher gear accuracy grades.
Another critical aspect is the grinding tooling. The wheel arbor used for center hole grinding must have high precision to ensure concentricity between the grinding wheel and the spindle. I design the arbor with a maximum outer cylindrical section as the primary基准, machining all critical features in one setup to minimize runout. The runout between the arbor’s mounting thread and the wheel-attachment surface is controlled to within 0.015 mm. This precision is vital for maintaining the integrity of the gear shaft during grinding. Additionally, the selection of grinding wheels is optimized: for surface roughness Ra ≤ 0.4 μm, a chromium oxide wheel with grit size F100 is used, while for Ra ≤ 0.8 μm, a white aluminum oxide wheel with grit size F60 suffices. The material removal rate (MRR) during grinding can be calculated as: $$ \text{MRR} = v_f \cdot A \cdot \rho $$ where v_f is the feed rate, A is the contact area, and ρ is the material density. For the hollow gear shaft, maintaining a low MRR prevents heat buildup and distortion.
In practice, the clamping method for the gear shaft during center hole grinding is further optimized using a custom pitch circle夹具. This夹具 consists of three jaws evenly distributed on a diaphragm chuck, which grips the gear teeth’s pitch circle without damaging the functional surfaces. This approach ensures that the grinding基准 is aligned with the gear’s operational axis, reducing errors that could arise from using the outer diameter alone. The clamping force is calibrated to avoid elastic deformation of the hollow gear shaft, which could otherwise introduce temporary distortions. The alignment accuracy can be verified using a test bar between centers, confirming coaxiality within 0.02 mm before grinding commences. This meticulous setup is essential for producing a gear shaft that meets the demands of high-speed transmissions.
Beyond the mechanical processes, I also consider the metallurgical aspects of the gear shaft. The material selection and heat treatment parameters are tuned to minimize residual stresses that could affect central hole stability. For example, using low-distortion carburizing steels and controlled quenching media reduces the tendency for cone angle enlargement. The phase transformations during heat treatment can be modeled using the Koistinen-Marburger equation for martensite formation: $$ f_m = 1 – \exp[-k_m (M_s – T)] $$ where f_m is the martensite fraction, k_m is a constant, M_s is the martensite start temperature, and T is the temperature. By controlling the cooling rate, we can influence the final dimensions of the gear shaft, including its central holes.
To achieve a comprehensive optimization, I have integrated these strategies into a holistic process flow for the hollow gear shaft. The revised工艺路线 includes: material cutting → forging → normalizing → rough turning →精加工 I (one end and central hole) →精加工 II (opposite end and central hole) → spline broaching → gear hobbing → chamfering → cleaning → heat treatment → post-heat treatment center hole grinding → external cylindrical grinding → hard turning of internal bores → gear grinding → cleaning → final inspection. Each step is monitored using statistical process control (SPC) to ensure consistency. For instance, the central hole cone angle is measured with a coordinate measuring machine (CMM) and plotted on control charts to detect any drifts.
The benefits of these optimizations extend beyond accuracy. They also enhance the durability and reliability of the gear shaft in service. A well-machined central hole ensures even load distribution during operation, reducing wear and fatigue on bearing surfaces. This is particularly important for electric vehicle transmissions, where efficiency and longevity are paramount. The vibration characteristics of the gear shaft can be analyzed using finite element analysis (FEA), where the central hole quality influences modal frequencies. The fundamental frequency f can be estimated as: $$ f = \frac{1}{2\pi} \sqrt{\frac{k}{m}} $$ where k is the stiffness influenced by the central hole’s roundness, and m is the mass of the gear shaft. Improved roundness increases k, leading to higher natural frequencies and reduced resonance risks.
In conclusion, through systematic analysis and optimization of the machining process for central holes in hollow gear shafts, I have demonstrated significant improvements in precision and performance. Key measures include refining CNC turning基准, compensating for heat treatment deformations, optimizing central hole design, and implementing post-heat treatment grinding with specialized tooling. These steps collectively reduce coaxiality errors, enhance roundness, and provide a robust定位基准 for final grinding operations. The gear shaft, as a core component, thereby achieves the high standards required for modern new energy transmissions. Future work may involve incorporating in-process monitoring and adaptive control to further push the limits of gear shaft manufacturing. This holistic approach ensures that every gear shaft produced meets the stringent demands of efficiency, noise reduction, and longevity in automotive applications.