
In modern industrial applications, gear shafts serve as critical components in power transmission systems, particularly in heavy machinery such as wind turbines, mining equipment, and marine propulsion. The performance and reliability of these gear shafts are heavily dependent on their surface hardness and wear resistance, which are typically enhanced through carburizing and quenching heat treatments. However, the complex thermal and phase transformation processes involved often lead to significant distortion, especially in large gear shafts with substantial cross-sectional variations and extended tooth widths. This distortion can compromise dimensional accuracy, increase manufacturing costs through excessive machining allowances, and lead to non-uniform carburized layers, ultimately affecting the service life of the components. In this study, I employ finite element analysis (FEA) to investigate the distortion mechanisms in large carburized gear shafts and propose optimized process controls to mitigate these issues.
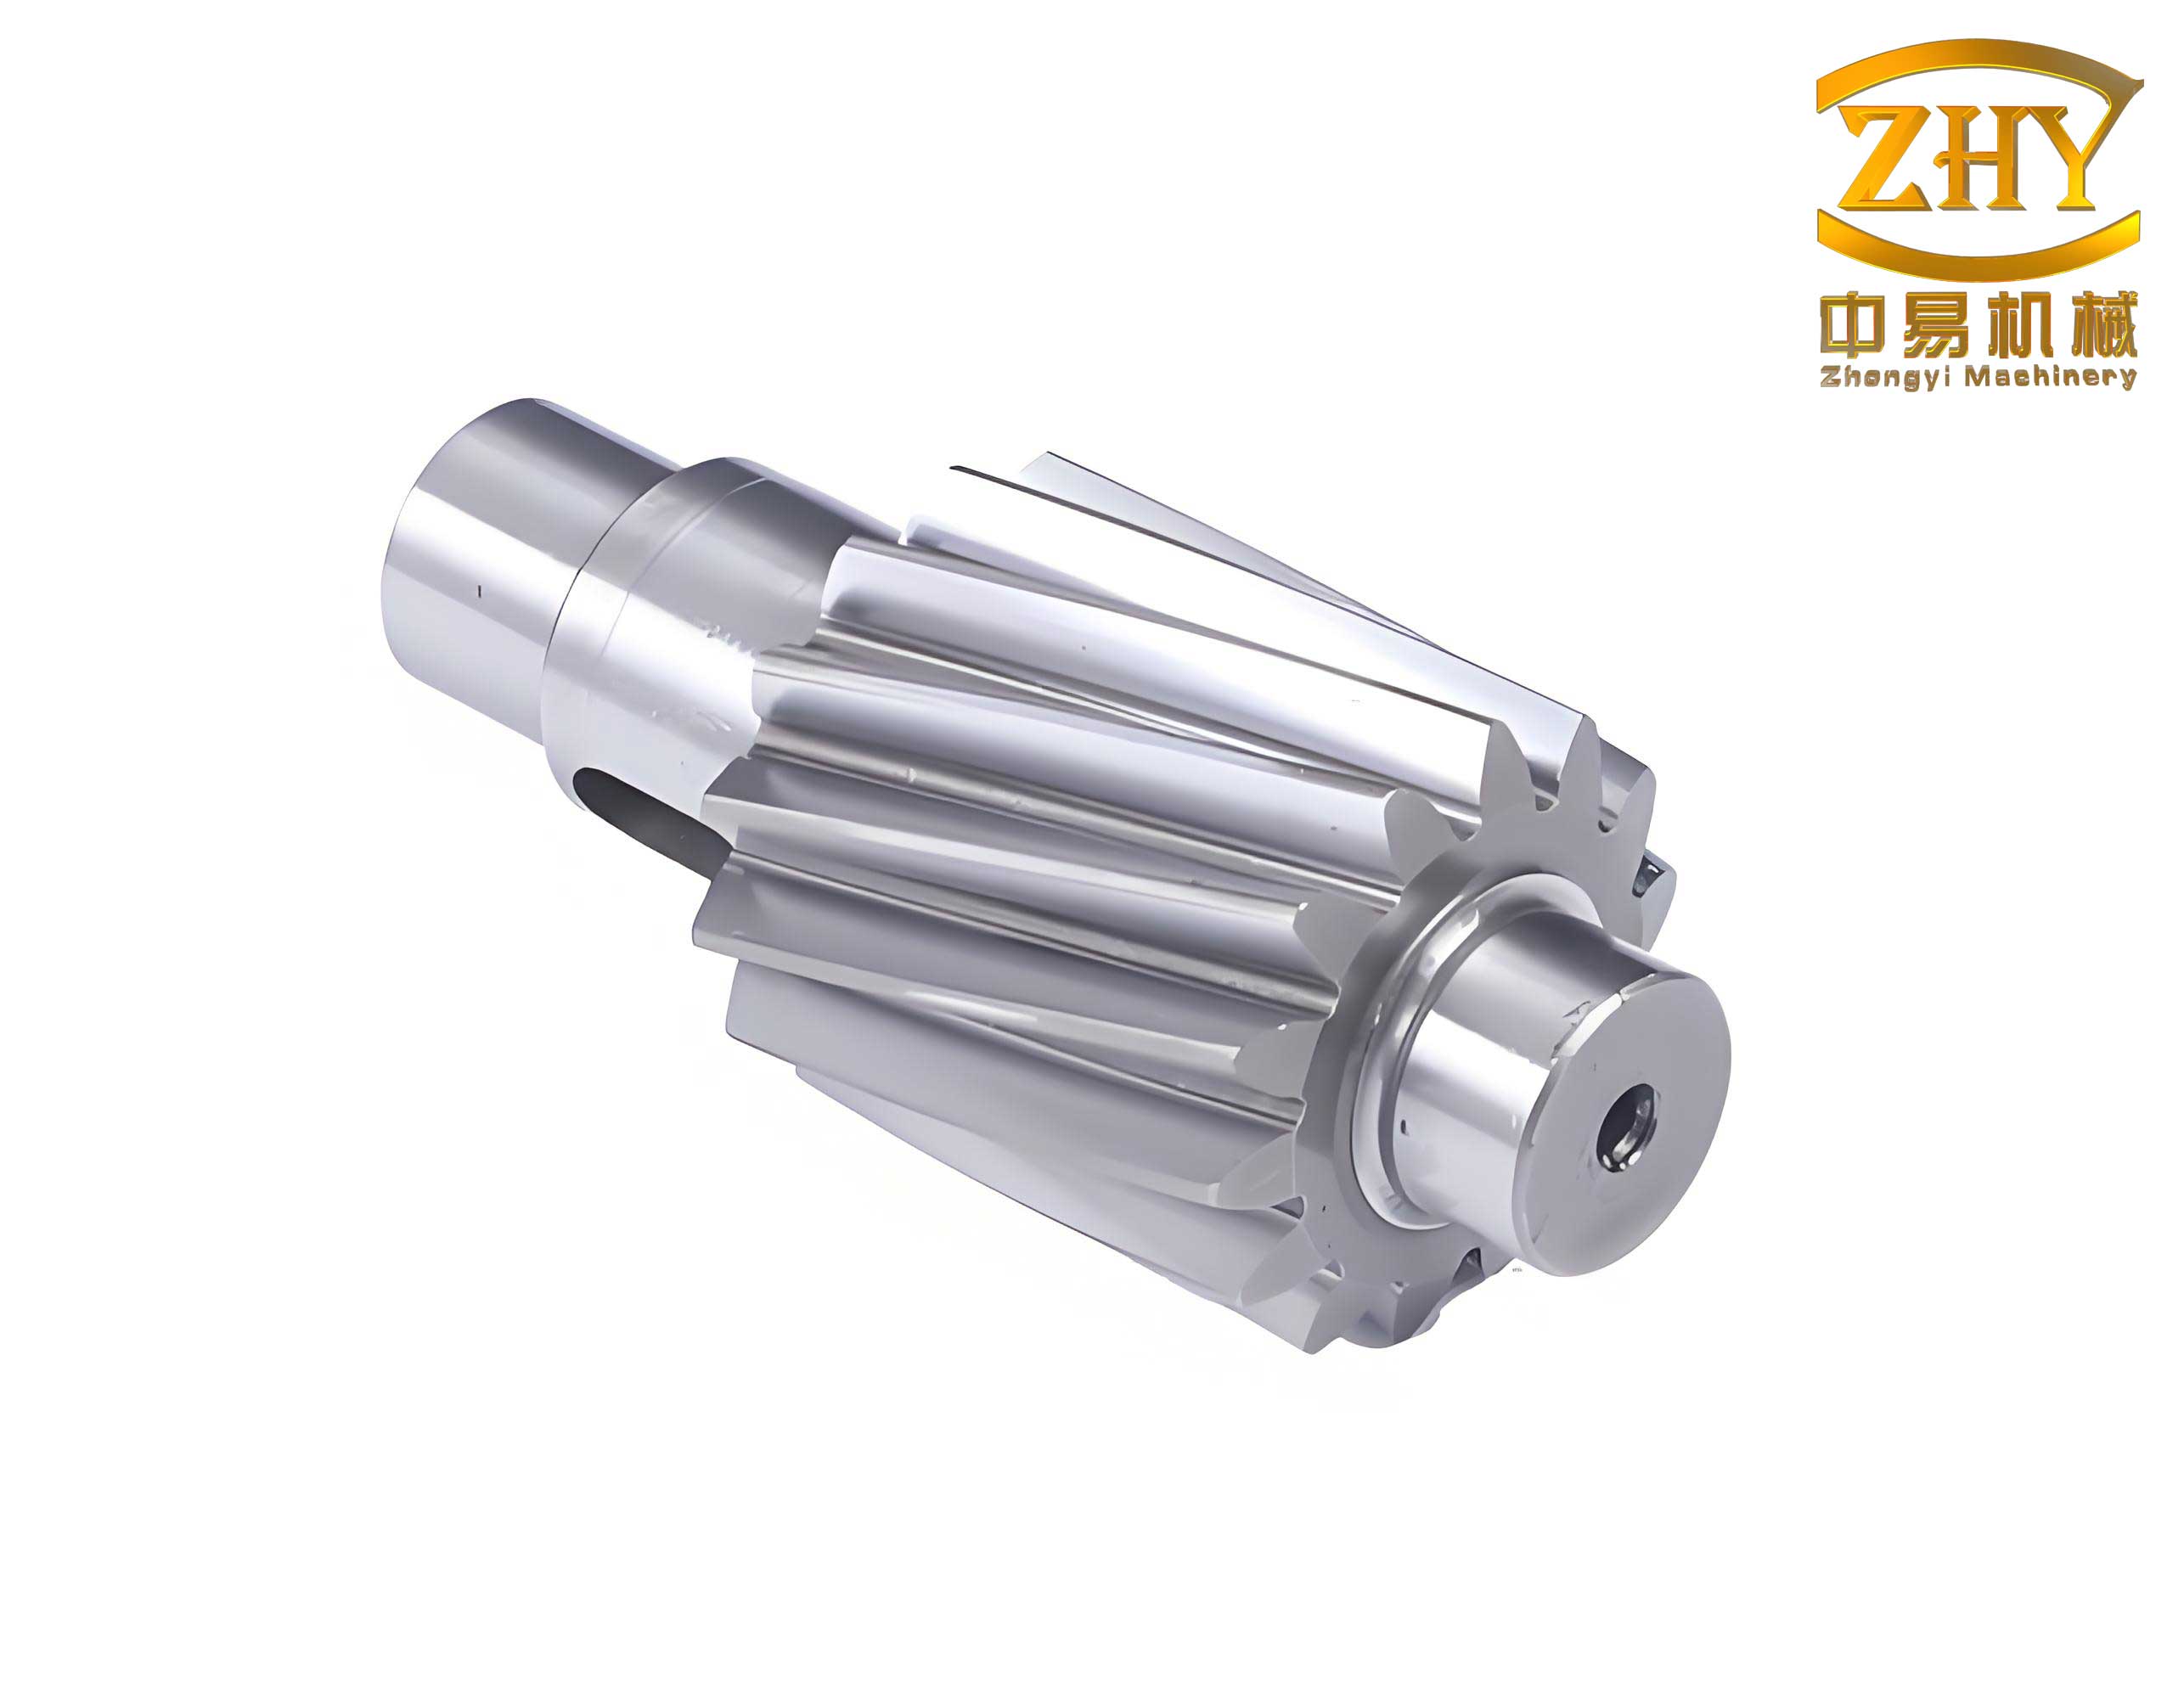
The material under consideration is a low-alloy steel, specifically 17CrNiMo6, which is widely used for high-strength gear shafts due to its excellent hardenability and toughness. The chemical composition of this steel is summarized in Table 1, highlighting key alloying elements that influence phase transformations during heat treatment. The gear shaft geometry, as modeled in this analysis, features a module of 22 mm, 23 teeth, a tip diameter of 550 mm, and a tooth width of 400 mm. Such dimensions are representative of large-scale gear shafts where distortion control becomes paramount. To efficiently simulate the heat treatment process, I utilize a symmetric half-tooth model with appropriate boundary conditions, meshed with approximately 60,000 tetrahedral elements using DEFORM software, a robust platform for coupled thermal, metallurgical, and mechanical analyses.
| Element | C | Si | Mn | Cr | Mo | Ni |
|---|---|---|---|---|---|---|
| Content (%) | 0.17 | 0.27 | 0.65 | 1.61 | 0.29 | 1.57 |
The carburizing process for these gear shafts involves exposing them to a carbon-rich atmosphere at elevated temperatures to diffuse carbon into the surface layer, thereby increasing hardness. The standard practice includes a strong carburizing phase at 920°C with a carbon potential of 1.2% for 40 hours, followed by a diffusion phase at a reduced carbon potential of 0.8% for 20 hours, and subsequent furnace cooling. The carbon concentration profile resulting from this process can be described by Fick’s second law of diffusion, which governs the transient carbon distribution. The equation is given by:
$$\frac{\partial C}{\partial t} = D \nabla^2 C$$
where \(C\) is the carbon concentration, \(t\) is time, and \(D\) is the diffusion coefficient, which is temperature-dependent and follows an Arrhenius relationship: \(D = D_0 \exp\left(-\frac{Q}{RT}\right)\), with \(D_0\) as the pre-exponential factor, \(Q\) the activation energy, \(R\) the gas constant, and \(T\) the absolute temperature. For the gear shafts, simulation results indicate a surface carbon content of up to 0.79%, with an effective case depth of 5.2 mm measured at the 0.35% carbon threshold, meeting the technical requirement of 5.0–5.5 mm. This confirms the adequacy of the carburizing parameters, but the subsequent quenching step introduces significant challenges.
Traditionally, oil quenching is employed for gear shafts due to its moderate cooling rate, which aims to achieve a martensitic transformation while minimizing cracking risk. In this analysis, I simulate oil quenching using a fast quenching oil at 60°C, with a quenching duration of 1 hour. The cooling behavior is characterized by the heat transfer coefficient, which varies with temperature and influences thermal stresses. For oil, the heat transfer coefficient \(h\) can be modeled as a function of temperature \(T\), often derived from experimental cooling curves. The net heat flux \(q\) at the surface is given by:
$$q = h(T) (T_{\text{surface}} – T_{\text{quenchant}})$$
where \(T_{\text{surface}}\) is the gear shaft surface temperature and \(T_{\text{quenchant}}\) is the quenchant temperature. The results from the oil quenching simulation reveal a severe distortion pattern in the gear shafts, characterized by a saddle-shaped deformation along the tooth width. Specifically, the outer diameter contracts non-uniformly, with a maximum contraction of 2.2 mm at the tooth center and only 0.8 mm at the ends, leading to a saddle distortion magnitude of 1.4 mm (calculated as the difference between center and end contractions). This exceeds the allowable distortion limit of 1.5 mm for both concavity and warpage, necessitating process optimization.
To understand the root causes of this distortion in gear shafts, I analyze the thermal and phase transformation stresses. During quenching, the gear shafts experience rapid cooling, leading to differential cooling rates between the tooth center and ends due to the large width. The center cools slower initially but undergoes martensitic transformation later, while the ends cool faster and transform earlier. This sequential transformation generates significant thermal and transformation stresses. The martensitic transformation is accompanied by a volume expansion, described by the volumetric strain \(\epsilon_v\), which is proportional to the martensite fraction \(f_m\):
$$\epsilon_v = \beta f_m$$
where \(\beta\) is the transformation dilatation coefficient, typically around 0.01–0.02 for steel. The stress distribution post-quenching, as shown in the simulation, indicates compressive stresses up to 116 MPa at the tooth center and tensile stresses up to 29 MPa at the ends. This stress gradient drives the saddle distortion. Moreover, the martensite content reaches 92% at the surface, exacerbating volume changes. It is evident that for large gear shafts, conventional oil quenching is insufficient due to the high thermal gradients and uncontrolled phase transformation timing.
Building on these insights, I propose an improved heat treatment strategy for gear shafts that combines modified heating and quenching techniques. The heating process is revised to a two-stage approach: first, the gear shafts are heated to 560°C and held for 3 hours to reduce thermal gradients; then, they are gradually heated to the quenching temperature of 820°C over 9 hours. This slow heating minimizes thermal stresses before quenching. More critically, the quenching medium is changed from oil to a salt bath, specifically a mixture of 55% KNO3 and 45% NaNO2 with 0.7% water content. Salt bath quenching offers a unique cooling characteristic: high heat extraction at elevated temperatures (around 560°C) and slower cooling at lower temperatures, which reduces both thermal and transformation stresses. The heat transfer coefficient for the salt bath, derived from experimental data, is significantly higher than that of oil, as summarized in Table 2.
| Quenching Medium | Maximum Heat Transfer Coefficient (W/mm²·°C) | Temperature at Maximum (°C) |
|---|---|---|
| Fast Quenching Oil (60°C) | 5.6 | 450 |
| Salt Bath (180°C) | 22.0 | 560 |
The salt bath quenching process involves immersing the gear shafts in a 180°C salt bath for 2 hours, followed by air cooling. This allows the low-carbon core to undergo martensitic transformation first, while the high-carburized surface transforms more slowly in air, thereby reducing transformation stresses. Subsequently, a tempering treatment at 180°C for 12 hours is applied to convert martensite to tempered martensite, stabilize retained austenite, and relieve residual stresses. The effectiveness of this optimized process is evaluated through FEA simulation, and the results demonstrate a remarkable reduction in distortion. The maximum concavity at the tooth center is reduced to 1.41 mm, and the warpage along the width is minimized to 0.9 mm, both within the specified limits. A comparative summary of distortion outcomes is provided in Table 3.
| Process | Maximum Concavity at Tooth Center (mm) | Warpage Along Tooth Width (mm) | Stress Range (MPa) |
|---|---|---|---|
| Oil Quenching | 2.20 | 1.40 | -116 to +29 |
| Salt Bath Quenching | 1.41 | 0.90 | -85 to +15 |
The underlying mechanics of distortion control in gear shafts can be further elucidated through analytical models. The total distortion \(\delta\) in a gear shaft during quenching is a superposition of thermal distortion \(\delta_t\) and transformation distortion \(\delta_{tr}\):
$$\delta = \delta_t + \delta_{tr}$$
Thermal distortion arises from non-uniform cooling and is governed by the thermal strain \(\epsilon_t = \alpha \Delta T\), where \(\alpha\) is the coefficient of thermal expansion and \(\Delta T\) is the temperature gradient. For gear shafts with large widths, the temperature gradient along the tooth width \(\Delta T_w\) can be approximated using the heat conduction equation in cylindrical coordinates, considering the gear shaft as a hollow cylinder. The transformation distortion is linked to the martensite start temperature \(M_s\), which is carbon-dependent and given by:
$$M_s = M_s^0 – k C_c$$
where \(M_s^0\) is the martensite start temperature for pure iron, \(k\) is a constant, and \(C_c\) is the carbon content. In carburized gear shafts, the surface has higher carbon, lowering \(M_s\) and delaying transformation relative to the core. The salt bath process mitigates this by providing a more uniform cooling profile, reducing \(\Delta T_w\) and synchronizing transformation timing. Additionally, the stress evolution during quenching can be modeled using the von Mises yield criterion and plasticity theory, but for brevity, the FEA approach captures these complexities directly.
To generalize the findings for various gear shafts, I explore the influence of key parameters such as tooth width, module, and material grade. For instance, increasing tooth width amplifies distortion due to larger thermal gradients, as shown by a parametric study where distortion scales approximately linearly with width \(W\) for widths over 300 mm. The relationship can be expressed as:
$$\delta \propto W \cdot \Delta T_{\text{max}}$$
where \(\Delta T_{\text{max}}\) is the maximum temperature difference during quenching. Similarly, higher alloy content in gear shafts, such as increased nickel or chromium, affects hardenability and \(M_s\), altering distortion patterns. Therefore, process optimization must be tailored to specific gear shaft geometries and materials. The use of finite element analysis enables such customization by simulating diverse scenarios without costly physical trials.
In practice, the implementation of salt bath quenching for gear shafts requires careful control of bath composition and temperature. The salt mixture’s properties, including thermal conductivity and viscosity, impact heat transfer rates. Regular monitoring and maintenance are essential to prevent degradation. Furthermore, environmental and safety considerations, such as salt disposal and fume extraction, must be addressed. Despite these challenges, the benefits for large gear shafts are substantial: reduced machining allowances (down to 1.5 mm), improved carburized layer uniformity, and lower production costs. This aligns with industry trends toward sustainable manufacturing and high-precision components.
Looking ahead, advanced modeling techniques can further enhance distortion control in gear shafts. Incorporating machine learning algorithms with FEA could predict distortion based on historical data, enabling real-time process adjustments. Additionally, multi-scale modeling that accounts for microstructural evolution, such as carbide precipitation and grain growth, would provide deeper insights. For gear shafts used in extreme environments, like aerospace or deep-sea applications, these refinements are critical. Continued research into novel quenching media, such as polymer solutions or high-pressure gas quenching, may offer alternatives for gear shafts with complex geometries.
In conclusion, through finite element analysis, I have demonstrated that distortion in large carburized gear shafts is primarily driven by uneven cooling and sequential martensitic transformation during conventional oil quenching. By adopting a two-stage heating process and switching to salt bath quenching, distortion can be effectively controlled within technical specifications. The optimized process reduces concavity to 1.41 mm and warpage to 0.9 mm, ensuring dimensional accuracy and uniform carburizing for gear shafts. This approach not only mitigates manufacturing defects but also extends the service life of gear shafts in demanding applications. The integration of simulation tools into heat treatment design represents a paradigm shift toward data-driven optimization, paving the way for more reliable and efficient gear shaft production.
To summarize the key equations and relationships discussed in this analysis of gear shafts, I present a consolidated list:
- Carbon diffusion: $$\frac{\partial C}{\partial t} = D \nabla^2 C$$
- Diffusion coefficient: $$D = D_0 \exp\left(-\frac{Q}{RT}\right)$$
- Heat flux during quenching: $$q = h(T) (T_{\text{surface}} – T_{\text{quenchant}})$$
- Volumetric strain from martensite: $$\epsilon_v = \beta f_m$$
- Martensite start temperature: $$M_s = M_s^0 – k C_c$$
- Distortion scaling: $$\delta \propto W \cdot \Delta T_{\text{max}}$$
These formulations, combined with empirical data from tables, provide a comprehensive framework for analyzing and controlling distortion in gear shafts. As industries continue to demand larger and more precise gear shafts, such methodologies will be indispensable for achieving quality and performance goals.