
The drive pinion gear shaft is a critical component within the automotive rear axle differential assembly, playing a pivotal role in power transmission. The fracture of such a gear shaft represents the most severe form of gear failure, leading directly to a complete loss of drivetrain function. This analysis details the investigation into a specific case where an SUV’s drive pinion gear shaft fractured at the spline section during vehicle operation after approximately 50,000 kilometers. The objective is to determine the root cause of the failure through systematic examination.
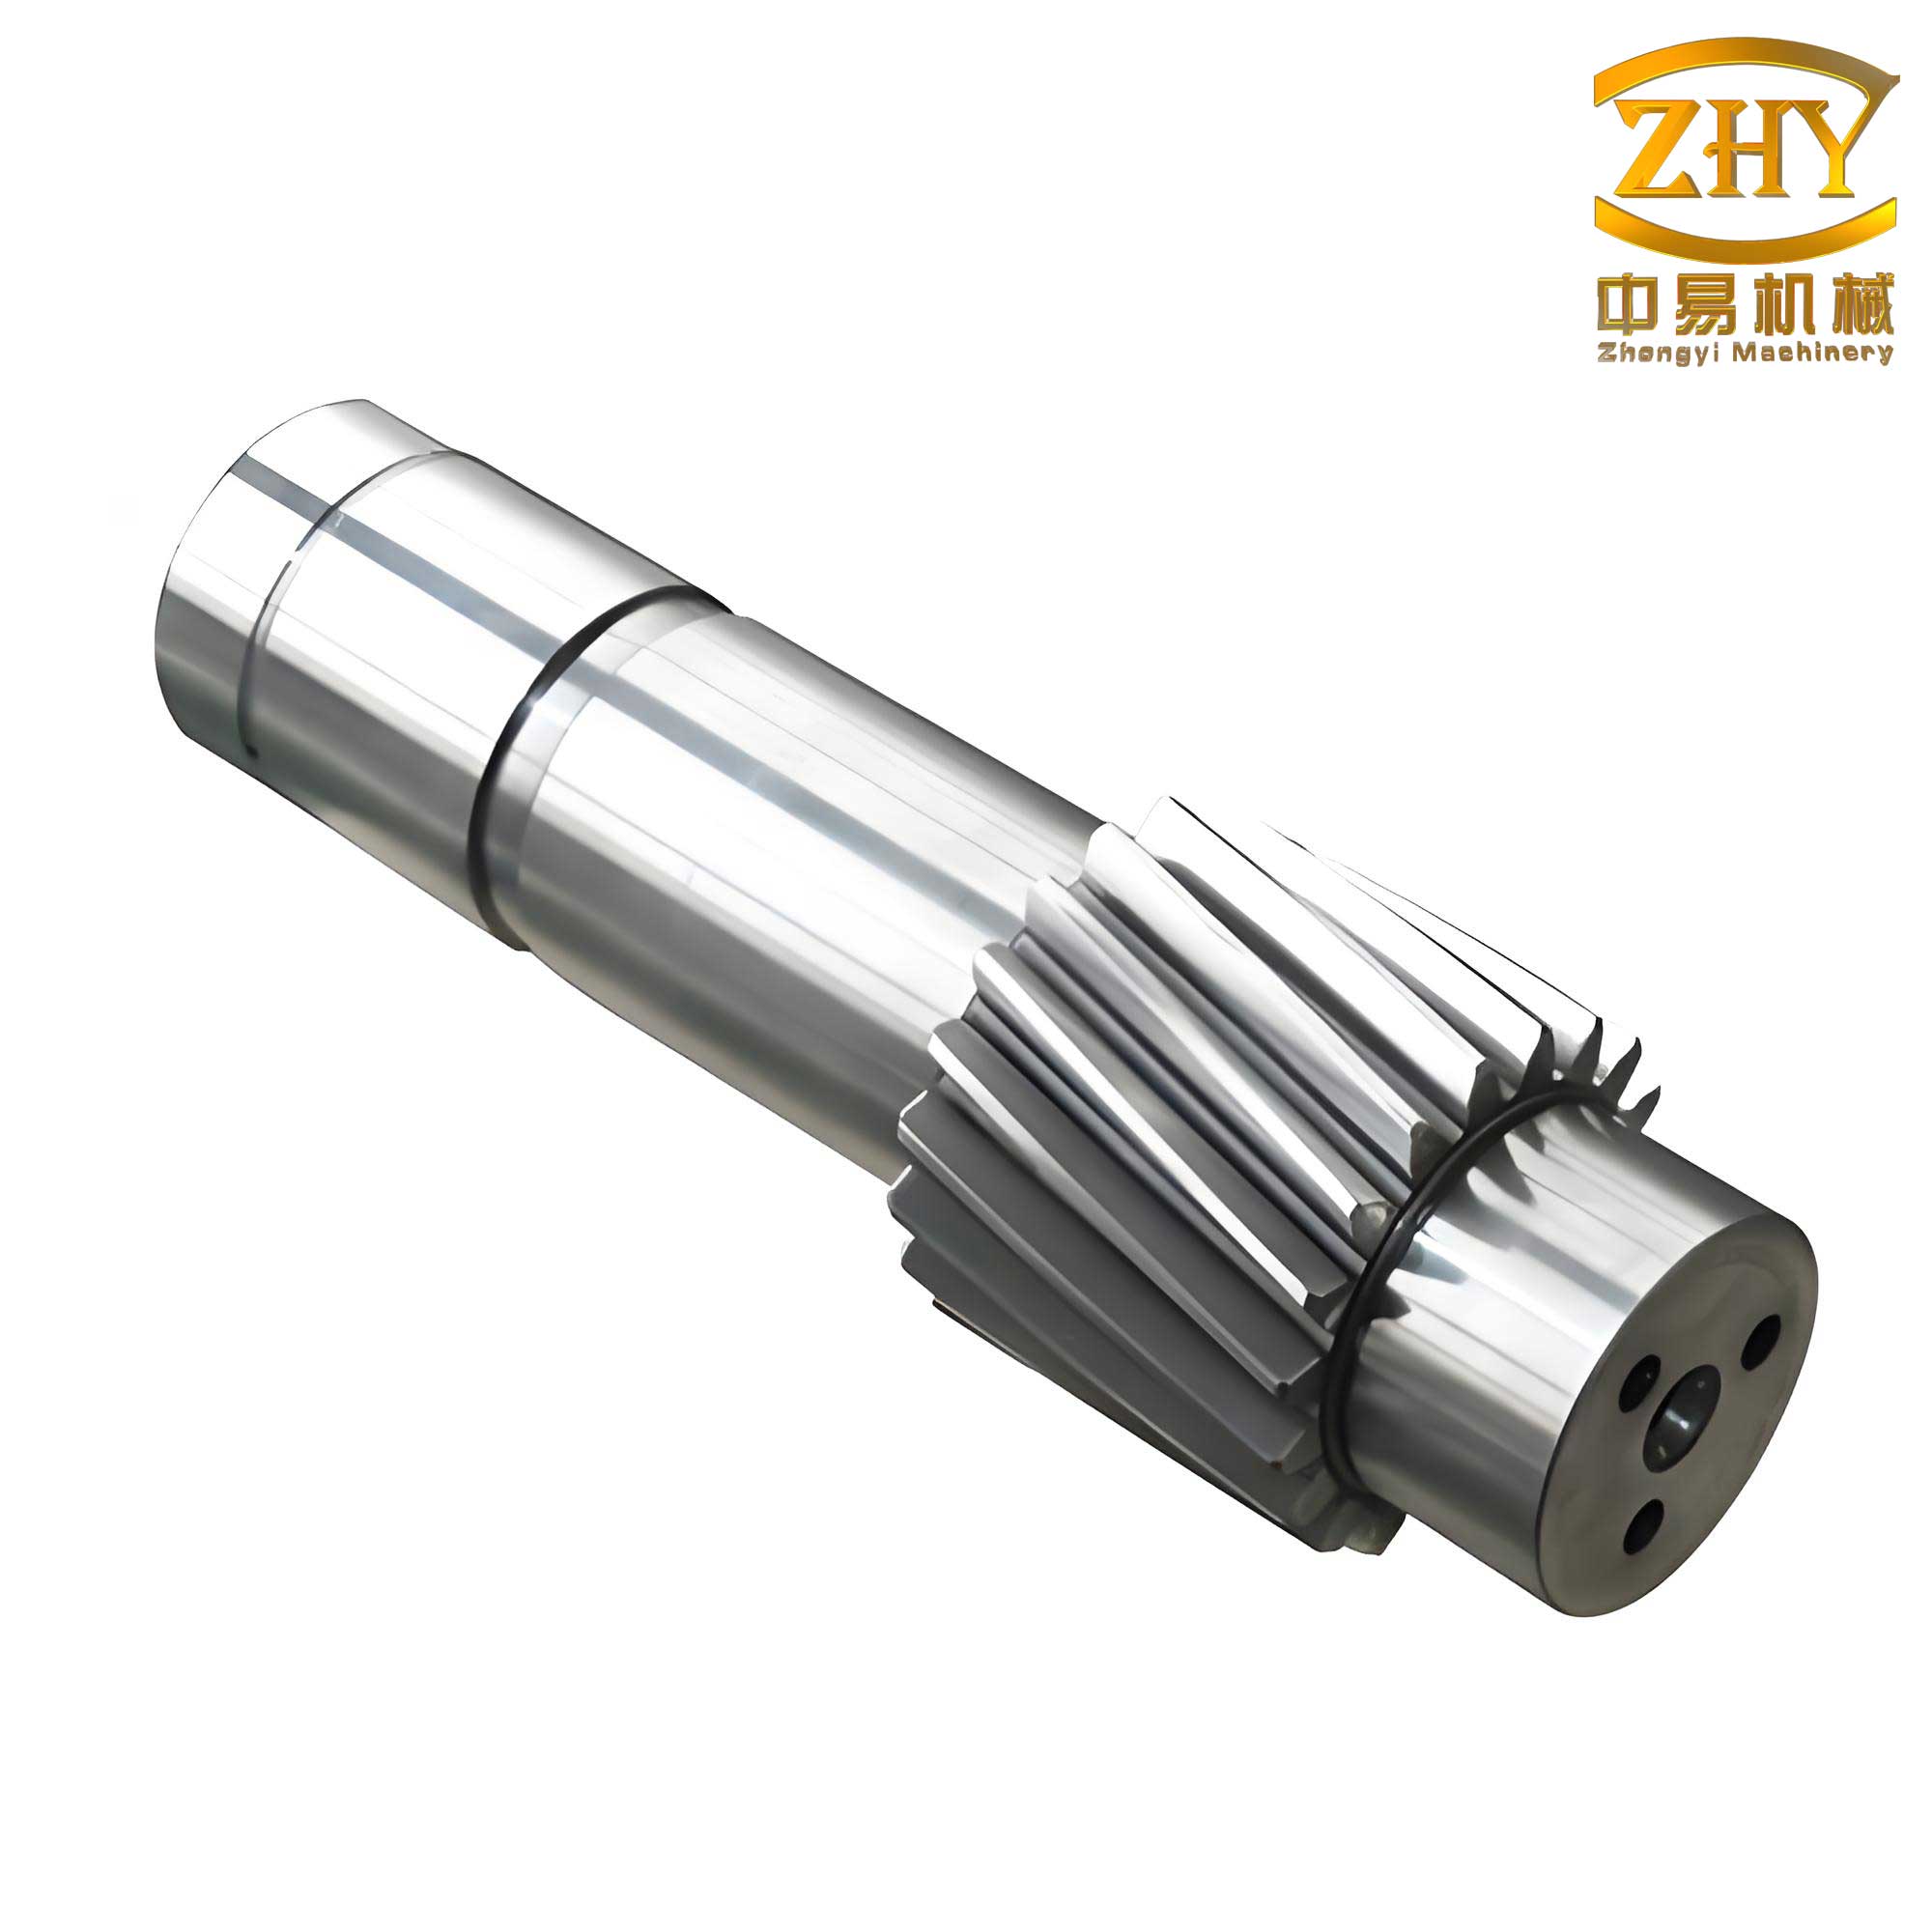
The failed component was manufactured from 20CrMnTiH alloy steel, a common choice for such high-stress applications due to its good hardenability and carburizing response. The typical manufacturing route involved: forging, normalizing, machining, spline rolling, gear cutting, carburizing and quenching, low-temperature tempering, shot peening, and finally, thread annealing.
1. Macroscopic Examination of the Fracture
The fracture occurred at the transition radius between the splined section and the smooth shaft of the gear shaft. The fracture surface was relatively flat and oriented perpendicular to the shaft’s axis, showing no significant macroscopic plastic deformation or abnormal mechanical damage. Initial observation indicated that the fracture originated at the carburized surface layer within the spline root fillet region. The presence of multiple radial ridges suggested the possibility of several crack initiation sites.
2. Chemical Composition Analysis
A sample from the failed gear shaft was subjected to spectroscopic chemical analysis. The results are compared with the standard specification for 20CrMnTiH steel in the table below.
| Element | Standard (GB/T 5216-2004) (wt.%) | Measured Value (wt.%) | Assessment |
|---|---|---|---|
| C | 0.17 – 0.23 | 0.21 | Conforms |
| Si | 0.17 – 0.37 | 0.24 | Conforms |
| Mn | 0.80 – 1.15 | 1.02 | Conforms |
| P | ≤ 0.035 | 0.012 | Conforms |
| S | ≤ 0.035 | 0.030 | Conforms |
| Cr | 1.00 – 1.35 | 1.21 | Conforms |
| Ti | 0.04 – 0.10 | 0.060 | Conforms |
| Ni | ≤ 0.30 | 0.035 | Conforms |
| Cu | ≤ 0.30 | 0.10 | Conforms |
The chemical composition of the gear shaft material is fully compliant with the required standard, eliminating material chemistry as a contributory factor in the failure.
3. Hardness and Case Depth Measurement
Surface hardness, core hardness, and the effective case depth were measured. The results are summarized in the following tables.
| Property | Specification | Measured Value | Assessment |
|---|---|---|---|
| Surface Hardness (HRC) | 58 – 64 | 63.9 (Avg.) | Conforms |
| Core Hardness (HRC) | 32 – 45 | 32.7 (Avg.) | Conforms |
| Distance from Surface (mm) | Micro-hardness (HV0.2) |
|---|---|
| 0.15 | 817 |
| 0.25 | 798 |
| 0.35 | 814 |
| 0.45 | 795 |
| 0.55 | 791 |
| 0.65 | 807 |
| 0.75 | 773 |
| 0.85 | 655 |
| 0.95 | 652 |
| 1.05 | 584 |
| 1.15 | 549 |
The effective case depth, defined as the depth where hardness falls to 550 HV, was calculated from the micro-hardness profile.
$$ \text{Effective Case Depth (CHD)} \approx 1.05 \text{ mm} $$
Both the surface/core hardness values and the calculated case depth of ~1.05 mm were within the specified range (0.9-1.3 mm), indicating that the carburizing and quenching heat treatment processes achieved the intended hardening characteristics for these gear shafts.
4. Macroetching and Surface Inspection
A transverse section was subjected to macroetching. The etched surface revealed a sound internal structure with no indications of gross defects such as pipe, segregation, or internal voids. The surface finish in the fracture region appeared normal, without evidence of grinding burns, notches, or other stress-concentrating anomalies. The radius at the spline-to-shaft transition was measured and found to be within the specified drawing tolerance.
5. Non-Metallic Inclusion Assessment
A longitudinal sample taken near the fracture was examined for non-metallic inclusions according to standard chart methods. The rating results are presented below.
| Inclusion Type | Series | Specification (Max. Level) | Measured Level | Assessment |
|---|---|---|---|---|
| A (Sulfides) | Thin | 3.0 | 2.5 | Conforms |
| Thick | 2.5 | 1.0 | Conforms | |
| B (Aluminates) | Thin | 3.0 | 0 | Conforms |
| Thick | 2.5 | 0.5 | Conforms | |
| C (Silicates) | Thin | 2.0 | 0.5 | Conforms |
| Thick | 2.0 | 0 | Conforms | |
| D (Oxides) | Thin | 2.0 | 1.0 | Conforms |
| Thick | 2.0 | 0.5 | Conforms |
The inclusion content was within acceptable limits for high-quality gear steel, indicating good steelmaking and rolling practices. This factor was not considered detrimental to the performance of these gear shafts.
6. Metallographic (Microstructural) Examination
Samples were sectioned, mounted, polished, and etched for microscopic evaluation at various locations on the gear shafts.
Core Microstructure: The core region exhibited a mixture of upper bainite, tempered martensite, and a small amount of ferrite. The presence of tempered martensite is desirable for achieving good core strength and toughness in carburized components like these gear shafts.
Case Microstructure: The bulk of the carburized case, away from the immediate surface, consisted of fine tempered martensite with a small amount of retained austenite, rated as a normal 4-level structure. This is the intended high-strength microstructure.
Critical Surface Anomaly: A significant finding was observed at the extreme surface of the spline root. An un-etched sample showed a continuous grey network along prior austenite grain boundaries. After etching, this layer appeared dark and was unresolvable at optical magnifications. Measurement confirmed this layer, indicative of non-martensitic transformation products, had a depth of approximately 0.03 mm. This exceeds the commonly specified limit of ≤ 0.02 mm for critical gear applications. Furthermore, multiple cracks were identified initiating from the surface within the spline tooth run-out areas, directly associated with this darkened surface layer.
To elucidate the nature of this “dark layer,” high-magnification Scanning Electron Microscopy (SEM) was employed on a polished but un-etched sample. The SEM analysis revealed that this layer was not the desired high-carbon martensite. Instead, it consisted of non-martensitic transformation products, specifically fine pearlite/upper bainite (troostite) structures. The formation of this layer is typically attributed to intergranular oxidation (IGO) during carburizing, which depletes alloying elements like Chromium and Manganese near the surface, thereby lowering the local hardenability. The relationship between hardenability ($DI$) and critical cooling rate can be expressed as:
$$ DI \propto \frac{1}{V_c} $$
where $DI$ is the ideal critical diameter and $V_c$ is the critical cooling rate. Surface alloy depletion reduces $DI$, increasing $V_c$ and making the surface layer more prone to forming softer, non-martensitic phases during quenching. The depth of this affected zone, $d_{IGO}$, is a critical parameter for gear shafts’ fatigue performance.
7. Fractography via Scanning Electron Microscopy (SEM)
The fracture surface was examined in the SEM to determine the failure mode and initiation characteristics.
Initiation Zone: The primary fracture origin was confirmed at the surface of the spline root fillet. The microfractographic features at this origin were predominantly intergranular fracture, characterized by a faceted, “rock candy” appearance. This is a classic signature of brittle fracture along prior austenite grain boundaries, consistent with the presence of the weakened, non-martensitic surface layer and/or grain boundary oxidation.
Propagation Zones: The crack propagated both clockwise and counter-clockwise from the initiation site. The fracture morphology in these propagation regions was a mixture of intergranular and cleavage fracture, both being brittle mechanisms. During propagation, secondary cracks were observed initiating at the roots of other spline teeth, indicating multiple stress concentration points were active.
Final Fracture Zone: The central region of the shaft, representing the final overload fracture, exhibited a predominantly cleavage fracture morphology with secondary cracking. A small area near the lower edge showed microvoid coalescence (dimples), indicative of limited ductile tearing at the very end of the failure process.
The transition in fracture mode from intergranular at the surface to cleavage in the core and finally to minor ductile tearing can be related to the stress state and microstructure. The stress intensity factor $K$ governs crack growth:
$$ K = Y \sigma \sqrt{\pi a} $$
where $Y$ is a geometric factor, $\sigma$ is the applied stress, and $a$ is the crack length. The brittle surface layer provided an easy path for crack initiation (low fracture toughness, $K_{Ic}$) at low $K$ values. As the crack grew into the tougher core martensite, the required $K$ increased, leading to cleavage. The presence of the non-martensitic layer effectively reduced the effective fatigue strength $S_f’$ of the component according to a degradation factor:
$$ S_f’ = S_f \cdot k_{surf} $$
where $k_{surf} < 1$ represents the surface condition factor detrimentally affected by the non-martensitic layer and microcracks.
8. Synthesis and Root Cause Analysis
The integration of all analytical findings leads to a conclusive failure mechanism for these gear shafts. The failure was a result of high-cycle fatigue, initiating at stress concentration points on the spline.
The key sequence of events is summarized as follows:
- Material and General Heat Treatment: The base material (20CrMnTiH), its cleanliness, core microstructure, bulk case hardness, and case depth were all conforming. The primary carburizing and quenching cycle was nominally correct.
- Critical Surface Condition: A critical anomaly was identified: an excessive depth (~0.03 mm) of non-martensitic transformation products (troostite/upper bainite) at the extreme surface of the spline root. This layer is softer, has lower fatigue strength, and often contains micro-notches from grain boundary oxidation.
- Crack Initiation: During service, the spline of the gear shaft transmits high torque under complex loading (torsion, bending, shock). The spline root is a natural stress concentrator. The brittle, weak surface layer, combined with this stress concentration, provided ideal sites for the initiation of multiple microcracks. The intergranular nature of the fracture origin confirms the weakness of the grain boundaries in this surface zone.
- Crack Propagation and Final Fracture: Once initiated, these cracks propagated through the high-strength case via a mix of intergranular and cleavage modes. Propagation was facilitated by the cyclic service loads. As the crack(s) grew, reducing the load-bearing cross-section, the stress intensity increased until catastrophic fast fracture occurred through the core of the gear shaft.
Therefore, the root cause of the fracture of these gear shafts is attributed to the presence of an excessively deep layer of non-martensitic microstructure at the surface of the spline root fillet. This microstructural defect significantly compromised the bending fatigue resistance of the component, leading to premature crack initiation under normal service loads. The primary cause of this defective layer is likely related to the atmosphere control during carburizing or an insufficient quenching rate/cooling capacity specifically at the spline geometry, allowing for partial transformation to softer phases.
9. Conclusion and Corrective Actions
The fracture of the drive pinion gear shaft was a fatigue failure originating from the spline root. The fundamental cause was a subsurface microstructural defect in the form of an out-of-specification non-martensitic layer (troostite), resulting from surface oxidation and/or inadequate quenching at that location. This defect acted as a potent fatigue initiator, drastically reducing the component’s service life.
To prevent recurrence in the production of such critical gear shafts, the following measures are recommended:
- Enhanced Process Control for Spline Areas: Special attention must be paid to the thermal profile and quenching conditions for components with splines. The geometry of splines can disrupt uniform fluid flow during oil quenching, leading to localized slow cooling. Process validation (e.g., using instrumented parts or simulation) should ensure adequate and uniform cooling rates across the entire spline section, including the root fillets.
- Atmosphere and Carbon Potential Control: Tighten controls on the carburizing atmosphere to minimize intergranular oxidation. This includes maintaining proper dew point, using oxygen probes accurately, and ensuring furnace integrity to prevent air ingress.
- Stricter Microspecification and Inspection: Enforce a strict limit for the non-martensitic layer depth, particularly at high-stress locations like spline roots and gear tooth fillets. For heavily loaded gear shafts, a maximum depth of 0.02 mm is a common stringent requirement. Implement regular metallographic audits on production gear shafts, specifically sectioning through spline areas to monitor this critical parameter.
- Post-Quench Inspection: Consider non-destructive testing methods capable of detecting surface irregularities or changes in magnetic properties that might be associated with soft surface layers on finished gear shafts.
By addressing the heat treatment process parameters that lead to the formation of surface non-martensitic phases, the fatigue performance and reliability of these essential automotive gear shafts can be significantly improved, preventing similar field failures.