
In modern manufacturing, the pursuit of efficiency and precision drives continuous innovation in metal forming processes. Cold forging, as a net-shape manufacturing technique, offers significant advantages in producing high-quality components with excellent surface finish and dimensional accuracy. Among various applications, the production of spur and pinion gears through cold forging has garnered attention due to the potential for material savings and reduced machining steps. However, the high forging pressures required in cold forging pose challenges for equipment and tooling, making it crucial to explore methods for reducing these forces. In this article, I delve into the impact of apical shunt cavity structures on the cold forging process for spur and pinion gears, leveraging simulation studies to compare different die designs and optimize performance.
The spur and pinion gear, a fundamental component in mechanical transmission systems, typically features straight teeth aligned parallel to the axis of rotation. Its geometry is defined by parameters such as module, number of teeth, pressure angle, and pitch diameter. For instance, a standard spur and pinion gear might have a module of 3 mm, 20 teeth, a pressure angle of 25°, and a pitch diameter of 60 mm, as considered in this analysis. The cold forging of such gears involves deforming a metal billet at room temperature using dies that replicate the gear’s tooth profile. This process not only enhances material utilization but also aligns with green manufacturing principles by minimizing waste.
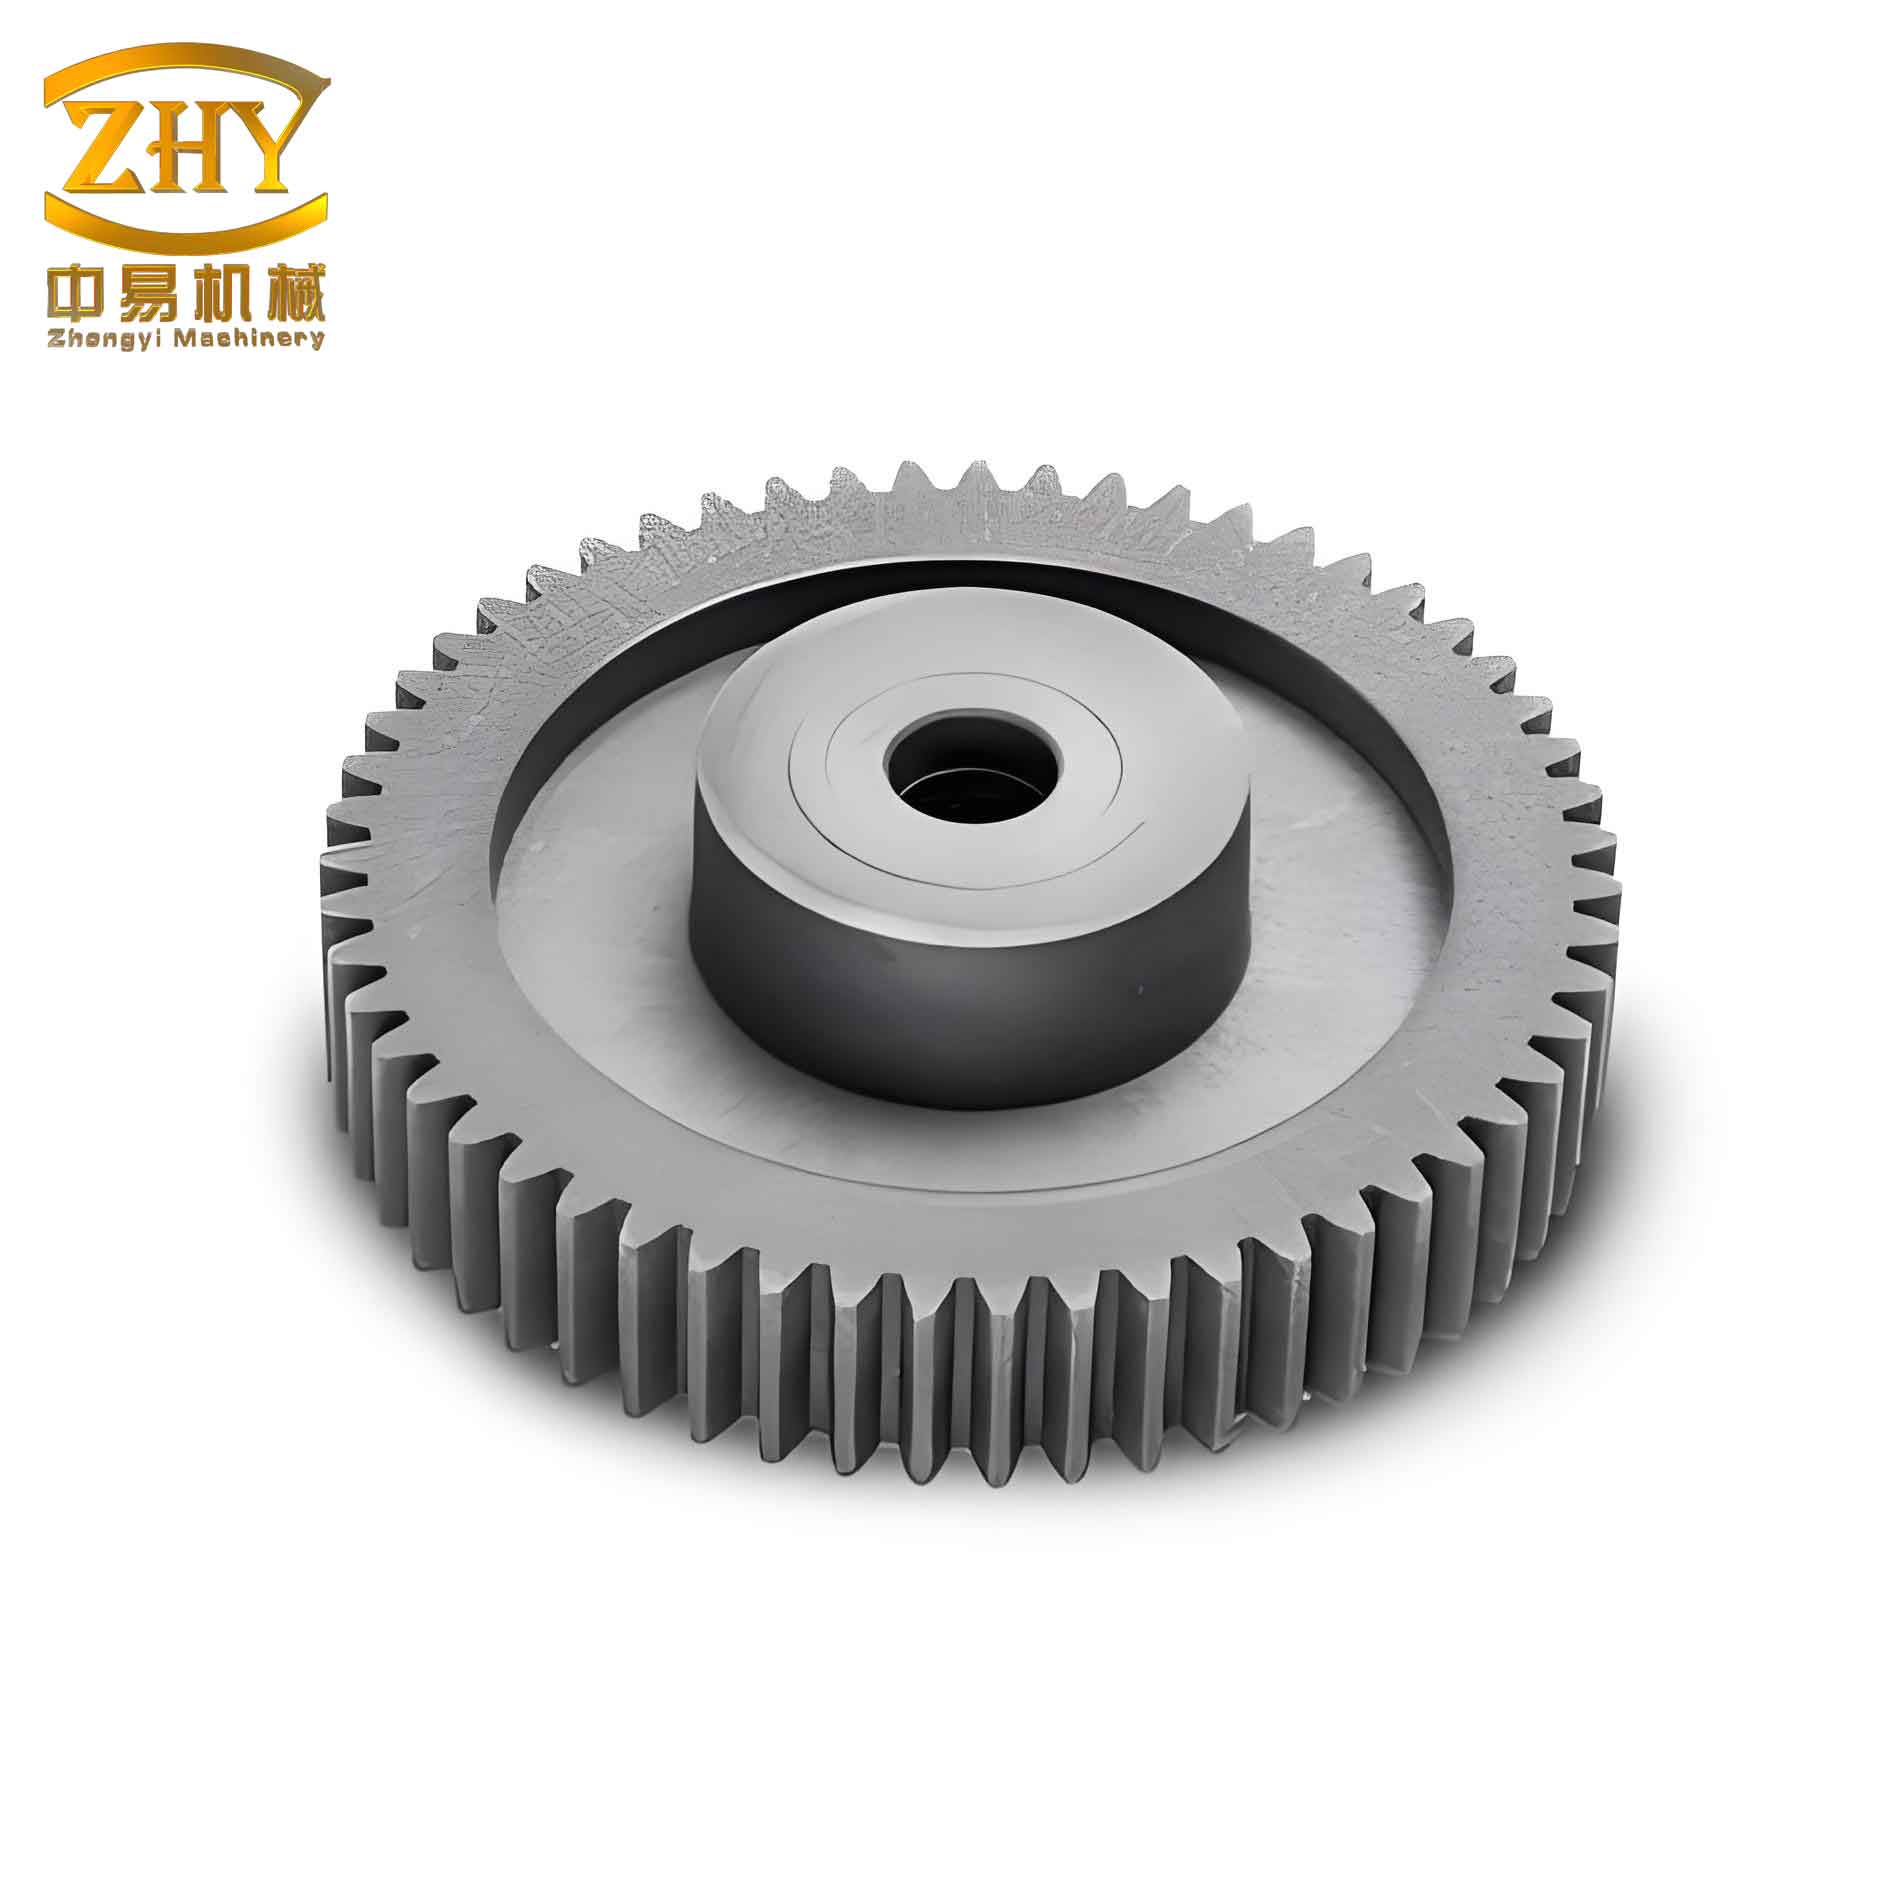
To understand the mechanics of cold forging for spur and pinion gears, it is essential to consider the material behavior and die design. The material used in this study is AISI-1045 steel, equivalent to 45 steel, which is commonly employed in gear manufacturing due to its balanced mechanical properties. The chemical composition and physical properties are summarized in Table 1. The dies are made of Cr12 steel, modeled as AISI-D3 in simulations, known for its high wear resistance and durability under forging conditions.
| Element | Mass Fraction (%) |
|---|---|
| C | 0.45 |
| Mn | 0.72 |
| Si | 0.30 |
| Cr | 0.25 |
| Ni | 0.18 |
| S | 0.03 |
| P | 0.03 |
| Fe | Balance |
Table 1: Chemical composition of AISI-1045 steel (45 steel) used for spur and pinion gear forging.
| Property | Value |
|---|---|
| Elastic Modulus (GPa) | 207 |
| Tensile Strength (MPa) | 650 |
| Density (g/cm³) | 7.85 |
| Poisson’s Ratio | 0.269 |
Table 2: Physical properties of AISI-1045 steel relevant to spur and pinion gear cold forging.
The cold forging process parameters include a temperature of 25°C, a punch loading rate of 6.5 mm/s, and a cylindrical billet shape. To reduce friction, the billet surface is treated with phosphate coating, resulting in a friction coefficient of 0.12 between the billet and die. These settings simulate real-world conditions and ensure accurate analysis of the forging behavior for spur and pinion gears.
The die structure plays a pivotal role in determining the forging pressure and final gear quality. In traditional cold forging dies for spur and pinion gears, the tooth cavity matches the gear profile without any additional features, leading to high stress concentrations and elevated forging forces. To address this, I investigate two modified die structures with apical shunt cavities: a square-shaped shunt cavity and a circular-shaped shunt cavity. These cavities are incorporated at the bottom of the tooth cavity to facilitate material flow and reduce resistance during forging. The primary goal is to compare these designs with the original non-shunt cavity die in terms of stress distribution, forging load, and material filling efficiency for spur and pinion gears.
The simulation setup involves using Deform software, where three-dimensional models of the spur and pinion gear and dies are created in Pro/E and imported as STL files. The finite element analysis (FEA) captures the complex interactions during forging. The governing equations for plastic deformation in cold forging can be expressed using the von Mises yield criterion and flow rule. The effective stress \(\sigma_e\) is given by:
$$ \sigma_e = \sqrt{\frac{1}{2}\left[(\sigma_1 – \sigma_2)^2 + (\sigma_2 – \sigma_3)^2 + (\sigma_3 – \sigma_1)^2\right]} $$
where \(\sigma_1, \sigma_2, \sigma_3\) are the principal stresses. The material flow stress \(\bar{\sigma}\) as a function of strain \(\bar{\epsilon}\) and strain rate \(\dot{\bar{\epsilon}}\) for AISI-1045 steel can be modeled using the Johnson-Cook equation:
$$ \bar{\sigma} = (A + B\bar{\epsilon}^n)(1 + C\ln\dot{\bar{\epsilon}}^*)(1 – T^{*m}) $$
where \(A, B, C, n, m\) are material constants, \(\dot{\bar{\epsilon}}^*\) is the dimensionless strain rate, and \(T^*\) is the homologous temperature. However, for cold forging at room temperature, the temperature term is negligible, simplifying the analysis. The forging load \(F\) can be estimated from the pressure \(P\) over the contact area \(A\):
$$ F = \int_A P \, dA $$
where \(P\) depends on the material yield strength and frictional conditions. By optimizing the die geometry, such as adding shunt cavities, the pressure distribution can be modified to lower the overall load for spur and pinion gear forming.
In the simulation results, the stress distributions for spur and pinion gears forged with different die cavities are analyzed. For the non-shunt cavity die, the maximum effective stress is concentrated in the tooth region, reaching approximately 930 MPa, while the core stress is around 880 MPa. The square shunt cavity die reduces the maximum stress to about 800 MPa in the teeth and 730 MPa in the core. The circular shunt cavity die shows a maximum stress of 850 MPa, scattered at the tooth tips and roots, with a core stress of 660 MPa. Although the square shunt cavity offers the lowest stress, it requires more material removal in post-processing due to its larger volume. This trade-off is critical for spur and pinion gear manufacturing where material efficiency is paramount.
The forging load over time for each die structure reveals significant differences. As shown in Table 3, the load progression is divided into three phases: slow increase, rapid increase, and sharp increase. The circular shunt cavity die exhibits the lowest final load of 1049.5 kN, compared to 1416.3 kN for the non-shunt cavity die and 1150.6 kN for the square shunt cavity die. This reduction in load not only lessens equipment wear but also enhances die life, making it advantageous for mass production of spur and pinion gears.
| Die Structure | Phase 1 (0-2.2 s) Load Acceleration (kN/s) | Phase 2 (2.2-3.8 s) Load Acceleration (kN/s) | Phase 3 (3.8-5 s) Load Acceleration (kN/s) | Final Load (kN) |
|---|---|---|---|---|
| Non-Shunt Cavity | 77.8 | 124.4 | 871.2 | 1416.3 |
| Square Shunt Cavity | 31.8 | 140.2 | 713.3 | 1150.6 |
| Circular Shunt Cavity | 36.2 | 130.6 | 634.2 | 1049.5 |
Table 3: Forging load characteristics for spur and pinion gear cold forging with different die structures.
Material filling is another crucial aspect of spur and pinion gear cold forging. The circular shunt cavity die ensures complete filling of the tooth tips, as visualized in the simulation, with no defects such as underfilling or laps. This is attributed to the streamlined flow path provided by the circular cavity, which reduces dead zones and promotes uniform material distribution. The filling efficiency \(\eta_f\) can be defined as the ratio of filled volume to designed volume:
$$ \eta_f = \frac{V_{\text{filled}}}{V_{\text{design}}} \times 100\% $$
For the circular shunt cavity die, \(\eta_f\) approaches 100%, indicating optimal performance for spur and pinion gear成形.
To further explore the benefits of shunt cavities, I analyze the strain distribution during forging. The effective strain \(\bar{\epsilon}\) is calculated from the deformation history, and higher strains in the tooth regions indicate more work hardening, which can improve gear strength. However, excessive strain may lead to cracking. The circular shunt cavity die shows a more uniform strain distribution compared to the non-shunt cavity die, reducing the risk of defects in spur and pinion gears. The strain energy \(U\) stored in the workpiece can be expressed as:
$$ U = \int_V \bar{\sigma} \, d\bar{\epsilon} \, dV $$
where \(V\) is the volume. Lower strain energy in the modified dies suggests less residual stress and better dimensional stability for spur and pinion gears after forging.
The design of shunt cavities involves geometric parameters such as cavity depth \(d_c\), width \(w_c\), and shape factor \(S_f\). For circular cavities, the radius \(r_c\) is key, and an optimal value can be derived from volume conservation principles. The volume of material flowing into the shunt cavity \(V_c\) should balance the excess material from the tooth formation to prevent flash or incomplete filling. For a spur and pinion gear with module \(m\) and number of teeth \(z\), the theoretical volume of teeth \(V_t\) is:
$$ V_t = \frac{\pi m^2 z}{4} \times \text{tooth height factor} $$
Assuming the shunt cavity volume \(V_c = \pi r_c^2 d_c\), the condition for optimal filling is:
$$ V_c \approx V_t \times k $$
where \(k\) is an empirical factor (typically 0.1-0.3). Through iterative simulations, I find that for the spur and pinion gear in this study, \(r_c = 1.5\) mm and \(d_c = 2\) mm yield the best results, minimizing forging load while ensuring full tooth filling.
In addition to stress and load, die wear is a critical consideration for spur and pinion gear cold forging. The contact pressure \(p_c\) between the billet and die influences wear rate, often modeled using Archard’s wear equation:
$$ W = K \frac{p_c v t}{H} $$
where \(W\) is wear volume, \(K\) is a wear coefficient, \(v\) is sliding velocity, \(t\) is time, and \(H\) is material hardness. The circular shunt cavity die reduces peak contact pressure by up to 20% compared to the non-shunt cavity die, as shown in Table 4, thereby extending die life for prolonged production of spur and pinion gears.
| Die Structure | Peak Contact Pressure (MPa) | Relative Reduction (%) |
|---|---|---|
| Non-Shunt Cavity | 1200 | 0 |
| Square Shunt Cavity | 980 | 18.3 |
| Circular Shunt Cavity | 960 | 20.0 |
Table 4: Peak contact pressure and wear reduction for spur and pinion gear cold forging dies.
The economic implications of die design cannot be overlooked. For spur and pinion gear manufacturing, material cost savings from net-shape forging must outweigh the initial tooling investment. The circular shunt cavity die, despite requiring slightly more complex machining, reduces forging energy consumption and scrap rates. The total cost \(C_{\text{total}}\) per gear can be estimated as:
$$ C_{\text{total}} = C_{\text{material}} + C_{\text{energy}} + C_{\text{tooling}} + C_{\text{machining}} $$
where \(C_{\text{material}}\) is proportional to billet volume, \(C_{\text{energy}}\) relates to forging load, \(C_{\text{tooling}}\) depends on die life, and \(C_{\text{machining}}\) covers post-forging operations. Simulation-based optimization of shunt cavities can lower \(C_{\text{energy}}\) and \(C_{\text{machining}}\), making cold forging more competitive for spur and pinion gear production.
From a broader perspective, the application of shunt cavity technology extends beyond spur and pinion gears to other cold-forged components like splines, helical gears, and automotive parts. The principles of material flow control and stress reduction are universally applicable, fostering advancements in green manufacturing. Future research could explore adaptive shunt cavities with variable geometries or hybrid processes combining cold forging with heat treatment for enhanced spur and pinion gear performance.
In conclusion, my analysis demonstrates that apical shunt cavity structures significantly improve the cold forging process for spur and pinion gears. The circular shunt cavity die emerges as the optimal design, offering a balance between stress reduction, forging load minimization, and material filling efficiency. By integrating simulation tools and mechanical principles, manufacturers can refine die geometries to achieve cost-effective and high-quality spur and pinion gear production. This study underscores the importance of innovative die design in advancing cold forging technology for precision components like spur and pinion gears.