
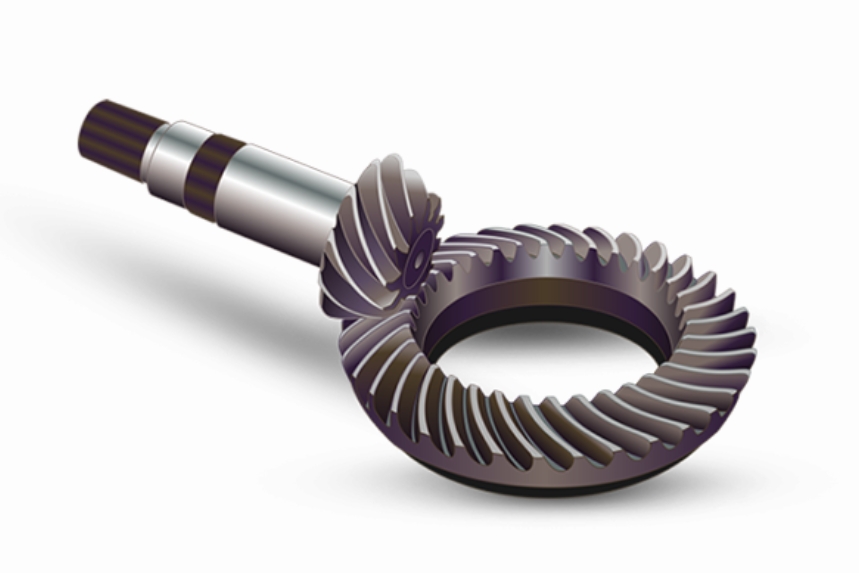
I have focused my investigation on the precision plastic forming of a driven spiral bevel gear used in an automotive drive axle. A spiral bevel gear has curved teeth, a gradual contact pattern, high load capacity, and smooth transmission characteristics. Compared with a straight bevel gear, the spiral bevel gear is much better at satisfying high-speed and heavy-load transmission requirements. For this reason, the spiral bevel gear is widely used in automobiles, construction machinery, machine tools, and similar fields. This creates a strong need for a forming method that can guarantee quality, raise efficiency, and reduce material waste. Plastic forming instead of cutting is one of the new technologies that I and many others in mechanical manufacturing continue to study. Compared with cutting, plastic forming gives higher material utilization, higher productivity, lower cost, and a continuous fiber flow line, which improves fatigue resistance. Precision plastic forming of straight bevel gears has already become a global trend. However, precision plastic forming of the spiral bevel gear for an automotive drive axle is still in the research and development stage.
To address the precision plastic forming problem of the spiral bevel gear, the traditional method is one-way enclosed die forging, in which pressure is applied from only one direction. In my work, I propose a new precision forming process for the driven spiral bevel gear. I study the fillability of the tooth cavity, the die design, the metal flow law, the load-stroke response, and the equivalent stress field. I use theoretical analysis and numerical simulation to verify the feasibility of the process. The results provide a scientific basis for further research on the spiral bevel gear.
Process Concept
I base the new process on the shape characteristics of the driven spiral bevel gear and the requirements of its forming process. During precision forming, the deformation of the billet mainly occurs at the tooth end face, while the mounting face almost does not deform. Therefore, I can stack two identical billets together and use two toothed punches to extrude the two billets simultaneously from the upper and lower ends in opposite directions. This two-way extrusion forms two spiral bevel gear parts in one cycle. It greatly improves production efficiency and reduces production cost.
For the process, I use an enclosed die. The tooling includes an upper punch, an upper billet, a core die, a lower billet, a lower punch, and a die insert. The enclosed forging die can be designed with single-action buffering or double-action buffering. I adopt the double-action buffering form. The basic working procedure is as follows: after the billets are loaded, pressure is applied simultaneously to the upper punch and the lower punch. The billets then flow in multiple directions and fill the die cavity to form the spiral bevel gear.
I summarize the basic parameters of the driven spiral bevel gear in Table 1. These parameters control the tooth geometry, the contact behavior, and the forming load.
| Parameter | Symbol | Value | Unit |
|---|---|---|---|
| Number of teeth | \(z\) | 41 | — |
| Face width | \(b\) | 30 | mm |
| Working normal pressure angle | \(\alpha_{nw}\) | 20 | \(^{\circ}\) |
| Non-working normal pressure angle | \(\alpha_{nn}\) | 20 | \(^{\circ}\) |
| Mid-point spiral angle | \(\beta_m\) | 37.13 | \(^{\circ}\) |
| Mounting distance | \(A\) | 60 | mm |
| Spiral direction | — | Left | — |
| Outer diameter | \(D_o\) | \(193 \pm 0.117\) | mm |
| Inner diameter reference | \(D_i\) | 145.00 | mm |
I treat the spiral bevel gear as a complex forging with a tooth cavity that must be filled precisely. The key difficulty is not only the global deformation of the billet but also the local filling of the tooth tips, tooth roots, and corner regions. The mounting face remains nearly rigid, so the tooth cavity is the active forming region. This is why the two-way extrusion arrangement is effective for the spiral bevel gear.
Fundamental Mechanics of the Spiral Bevel Gear Forming Process
I describe the plastic flow of the billet using the continuity equation. For an incompressible metal during hot forming, the density change is negligible, and the velocity field must satisfy
$$ \nabla \cdot \mathbf{v} = 0 $$
where \(\mathbf{v}\) is the velocity vector of the deforming material. The equilibrium equation for the plastic zone is
$$ \frac{\partial \sigma_{ij}}{\partial x_j} + f_i = 0 $$
where \(\sigma_{ij}\) is the stress tensor and \(f_i\) is the body force per unit volume. Since hot forging of the spiral bevel gear is dominated by plastic deformation, I use the Levy-Mises relation
$$ d\varepsilon_{ij} = d\lambda \, s_{ij} $$
where \(d\varepsilon_{ij}\) is the plastic strain increment, \(d\lambda\) is a positive scalar factor, and \(s_{ij}\) is the deviatoric stress tensor:
$$ s_{ij} = \sigma_{ij} – \frac{1}{3}\sigma_{kk}\delta_{ij} $$
The equivalent stress, or von Mises stress, is
$$ \sigma_{\mathrm{eq}} = \sqrt{\frac{1}{2}\left[(\sigma_1-\sigma_2)^2+(\sigma_2-\sigma_3)^2+(\sigma_3-\sigma_1)^2\right]} $$
The equivalent strain increment is
$$ d\bar{\varepsilon} = \sqrt{\frac{2}{3}d\varepsilon_{ij}d\varepsilon_{ij}} $$
For the hot forming of AISI-1045 steel at 1100 \(^{\circ}\)C, the flow stress can be represented in a general form as
$$ \sigma_f = K \bar{\varepsilon}^{n} \dot{\bar{\varepsilon}}^{m} \exp(\beta T) $$
where \(K\) is the strength coefficient, \(n\) is the strain-hardening exponent, \(m\) is the strain-rate sensitivity exponent, \(\beta\) is the temperature coefficient, and \(T\) is the absolute temperature. At high temperature, recovery and recrystallization reduce the flow stress, which helps the tooth cavity fill without excessive load on the spiral bevel gear die.
The friction condition at the billet-die interface follows the Coulomb friction model:
$$ \tau_f = \mu p $$
where \(\tau_f\) is the friction shear stress, \(\mu\) is the friction coefficient, and \(p\) is the normal contact pressure. I set \(\mu = 0.3\) in the simulation. This value is typical for hot forging with a lubricant and an oxidized steel surface.
The total forming load on the spiral bevel gear punch can be written as an integral over the contact area:
$$ F(s) = \int_{A_c(s)} p(x,s)\cos\theta(x,s)\,dA + \int_{A_f(s)} \tau_f(x,s)\sin\theta(x,s)\,dA $$
where \(s\) is the punch stroke, \(A_c\) is the contact area, \(A_f\) is the friction area, and \(\theta\) is the local inclination of the contact surface. The forming work is then
$$ W = \int_{0}^{s_{\max}} F(s)\,ds $$
I also use the fill ratio to quantify the cavity filling of the spiral bevel gear:
$$ R_f = \frac{V_{\mathrm{filled}}}{V_{\mathrm{cavity}}} \times 100\% $$
A value of \(R_f = 100\%\) means that the tooth cavity is completely filled. The maximum equivalent stress in the die must satisfy
$$ \sigma_{\max} \leq \sigma_{\mathrm{allow}} $$
and the safety factor is
$$ n_s = \frac{\sigma_{\mathrm{allow}}}{\sigma_{\max}} $$
These relations guide my evaluation of the two-way extrusion process for the spiral bevel gear.
Numerical Simulation Setup
I conduct the numerical simulation with the following initial conditions. The billet material is AISI-1045 steel. The billet temperature is 1100 \(^{\circ}\)C. The mesh consists of 300000 tetrahedral elements. The die temperature is 350 \(^{\circ}\)C. The friction coefficient is 0.3. The upper punch moves downward and the lower punch moves upward at a speed of 12.3 mm/s. I set the simulation step length to 0.1 mm, following the rule that the step should not exceed one third of the minimum element edge length. I complete the volume compensation setting before running the simulation. Table 2 lists the main parameters.
| Simulation parameter | Value | Unit |
|---|---|---|
| Billet material | AISI-1045 steel | — |
| Billet temperature | 1100 | \(^{\circ}\)C |
| Die temperature | 350 | \(^{\circ}\)C |
| Friction coefficient | 0.3 | — |
| Upper punch speed | 12.3 | mm/s |
| Lower punch speed | 12.3 | mm/s |
| Mesh type | Tetrahedral | — |
| Number of elements | 300000 | — |
| Step length | 0.1 | mm |
| Volume compensation | Enabled | — |
I use the simulation to examine the deformation at several typical punch strokes, including 25%, 87%, 98%, and 100% of the total stroke. I analyze the filling sequence, the load-stroke curve, and the equivalent stress distribution. I also compare the new two-way extrusion process with the traditional one-way enclosed die forging process. The comparison focuses on the maximum load and the stress state of the spiral bevel gear die.
Filling Behavior of the Spiral Bevel Gear Cavity
The simulation shows that the tooth cavity of the spiral bevel gear can be filled smoothly, and the formed tooth shape is good. When the metal begins to deform, the small end of the toothed punch contacts the billet first. Therefore, the billet first fills the small end of the punch and then fills the large end. At the beginning, the metal flows quickly. The metal at the tooth end face flows radially outward from the small end to the large end. Later, the deformation speed gradually decreases. This indicates that the corner filling at the large end of the punch is the key to complete filling of the tooth cavity. The mounting face of the billet hardly deforms from beginning to end. This agrees with my theoretical analysis.
I summarize the filling behavior in Table 3. The deformation process can be divided into three stages: free deformation, filling, and corner filling.
| Stroke level | Stage | Observed behavior | Load response |
|---|---|---|---|
| 25% | Free deformation | The billet surface starts to contact the die; local loading with global deformation. | The load rises gently. |
| 87% | Filling | The tooth cavity is gradually filled; the small end and middle region are nearly complete. | The load rises slowly for most of the stage. |
| 98% | Corner filling | The large-end corners of the tooth cavity require additional metal flow. | The load begins to rise rapidly. |
| 100% | Final corner filling | The cavity is completely filled; the tooth shape is fully formed. | The load reaches its maximum. |
The free deformation stage occurs from the initial state until the billet surface contacts the die. Because the billet size is slightly smaller than the die cavity, this stage is a free deformation process. It belongs to local loading with overall force transmission, and the load curve rises gently. The filling stage begins when the billet contacts the die and continues until the small end of the toothed punch and the middle part of the tooth cavity are basically filled. In this stage, the tooth cavity is gradually filled. It lasts the longest time, and the load-stroke curve rises slowly. The slope of the curve gradually increases in the later part of this stage, which means that the forming force increases faster and the metal flow becomes more difficult. The corner filling stage has a very small punch stroke, but the load curve rises rapidly. This is mainly because the tooth cavity has already been basically filled in the previous stage. The purpose of this stage is to complete the filling of the large-end corner of the toothed punch. Therefore, continued extrusion causes the forming force to rise rapidly until it reaches the maximum. The maximum load is 13.6 MN.
For the traditional one-way enclosed die forging process, the maximum load is 17.6 MN. Compared with the traditional process, the new two-way extrusion process reduces the maximum load by about 23%. I compute the reduction as
$$ \Delta F = \frac{F_{\mathrm{one-way}} – F_{\mathrm{two-way}}}{F_{\mathrm{one-way}}} \times 100\% $$
$$ \Delta F = \frac{17.6 – 13.6}{17.6} \times 100\% \approx 22.7\% $$
This load reduction is important because it lowers the required press capacity and reduces the risk of die failure. The lower load also means that the two-way extrusion process is more suitable for the spiral bevel gear, which has a large tooth cavity and a complex contact pattern.
| Forming process | Maximum load / MN | Load reduction / MN | Reduction ratio |
|---|---|---|---|
| One-way enclosed die forging | 17.6 | — | — |
| Two-way extrusion | 13.6 | 4.0 | 22.7% |
Load-Stroke Characteristics of the Spiral Bevel Gear
The load-stroke curve of the new process is normal and can be interpreted clearly. The curve can be divided into three stages: free deformation, filling, and corner filling. In the free deformation stage, the load increases slowly. In the filling stage, the load increases gradually, and the slope becomes larger near the end of the stage. In the corner filling stage, the load increases sharply. This behavior reflects the progressive filling of the spiral bevel gear tooth cavity.
I can approximate the load-stroke curve with a piecewise function. For the free deformation stage,
$$ F_1(s) = a_1 s + b_1, \quad 0 \leq s < s_1 $$
For the filling stage,
$$ F_2(s) = a_2 (s-s_1)^2 + b_2 (s-s_1) + c_2, \quad s_1 \leq s < s_2 $$
For the corner filling stage,
$$ F_3(s) = a_3 \exp\left[k_3(s-s_2)\right] + c_3, \quad s_2 \leq s \leq s_{\max} $$
where \(s_1\), \(s_2\), and \(s_{\max}\) are the stroke limits of the three stages. The exponential form in the last stage captures the rapid load rise when the corner regions of the spiral bevel gear are filled. The maximum load is reached at \(s = s_{\max}\).
The load-stroke behavior also shows that the two-way extrusion process distributes the deformation more evenly between the upper and lower parts of the billet stack. This reduces the tendency for one side to carry most of the load. In the case of the spiral bevel gear, this is especially useful because the tooth cavity is deep and the large-end corners are difficult to fill.
I also define an average forming pressure for the spiral bevel gear as
$$ p_{\mathrm{avg}} = \frac{F_{\max}}{A_{\mathrm{proj}}} $$
where \(A_{\mathrm{proj}}\) is the projected contact area. For the new process, the lower maximum load directly reduces \(p_{\mathrm{avg}}\), which in turn reduces the elastic deflection of the die and improves the dimensional accuracy of the spiral bevel gear.
Equivalent Stress and Die Loading
I analyze the equivalent stress field after forming the spiral bevel gear with the new process. Because the upper and lower parts are identical, I analyze only one of them. The largest stress region is mainly generated at the tooth root at both ends of the tooth profile. This is because the billet first contacts the tooth top of the toothed punch. The tooth top region of the punch corresponds to the tooth root region of the part. Moreover, the metal at both ends must pass through the tooth top region of the punch before entering the tooth cavity. This agrees with the metal deformation law in the actual two-way extrusion process.
The maximum stress appears at the tooth root corner of the tooth body, about 688 MPa. This is far below the allowable range of current die materials. The allowable stress of the die material is about 2500 MPa. Therefore, no failure occurs, and the new process is feasible. The safety factor is
$$ n_s = \frac{\sigma_{\mathrm{allow}}}{\sigma_{\max}} = \frac{2500}{688} \approx 3.63 $$
This safety factor shows that the die for the spiral bevel gear has sufficient strength under the two-way extrusion load. The equivalent stress distribution is summarized in Table 4.
| Stress quantity | Value | Unit |
|---|---|---|
| Minimum equivalent stress | 44.2 | MPa |
| Maximum equivalent stress | 688 | MPa |
| Allowable die stress | 2500 | MPa |
| Safety factor | 3.63 | — |
The equivalent stress results prove that the material flow is good and the new process is feasible. The stress concentrations at the tooth root corners are expected because these are the last regions to fill. However, the stress level remains safe for the die material. This means that the two-way extrusion process can be used for the spiral bevel gear without immediate risk of die fracture.
Comparison with One-Way Enclosed Die Forging
I compare the two-way extrusion process with the traditional one-way enclosed die forging process for the spiral bevel gear. The comparison is based on maximum load, load distribution, cavity filling, and equivalent stress. The results are summarized in Table 5.
| Index | One-way enclosed die forging | Two-way extrusion |
|---|---|---|
| Pressure application | One side | Upper and lower sides |
| Maximum load / MN | 17.6 | 13.6 |
| Load reduction | — | About 23% |
| Filling behavior | Tooth cavity fills from one end | Tooth cavity fills from both ends |
| Mounting face deformation | Small | Almost none |
| Production efficiency | One part per cycle | Two parts per cycle |
| Material utilization | Good | Good |
| Maximum equivalent stress / MPa | Higher | 688 |
| Die safety | Acceptable | Safe, \(n_s \approx 3.63\) |
The new process lowers the maximum load by about 23%. This is a direct benefit of the two-way extrusion arrangement. Because both punches move simultaneously, the deformation zone is more balanced, and the metal does not have to flow from only one side. For the spiral bevel gear, this balanced flow reduces the resistance at the large-end corners. As a result, the maximum load decreases, and the die experiences a more uniform stress state.
The traditional one-way enclosed die forging process applies pressure from one direction. The metal must flow a longer distance to fill the far end of the tooth cavity. This increases the load and can cause incomplete filling at the far corners of the spiral bevel gear. In contrast, the two-way extrusion process applies pressure from both ends. The metal flows from both sides toward the middle of the tooth cavity. The filling path is shorter, and the corner regions are easier to fill. This is why the new process produces a good tooth shape and a lower maximum load.
Metal Flow Law in the Spiral Bevel Gear Cavity
The metal flow law in the spiral bevel gear cavity can be described by the velocity field and the strain-rate field. I define the strain-rate tensor as
$$ \dot{\varepsilon}_{ij} = \frac{1}{2}\left(\frac{\partial v_i}{\partial x_j} + \frac{\partial v_j}{\partial x_i}\right) $$
The effective strain rate is
$$ \dot{\bar{\varepsilon}} = \sqrt{\frac{2}{3}\dot{\varepsilon}_{ij}\dot{\varepsilon}_{ij}} $$
In the free deformation stage, the strain rate is relatively uniform, and the metal flows mainly along the axial direction. In the filling stage, the strain rate becomes localized near the tooth cavity. The metal near the small end of the toothed punch flows first, and the flow front moves toward the large end. In the corner filling stage, the strain rate concentrates at the large-end corners. The effective strain rate increases sharply, which explains the rapid load rise.
I can express the volume flow rate through the tooth cavity as
$$ Q = \int_{A} \mathbf{v} \cdot \mathbf{n} \, dA $$
where \(\mathbf{n}\) is the outward normal vector. For an incompressible material, the volume flow rate entering the cavity must equal the volume rate of cavity filling. This relation helps me verify the simulation results. The filling sequence in the spiral bevel gear is consistent with the volume flow rate calculation.
The metal flow in the spiral bevel gear is also affected by the tooth geometry. The spiral angle \(\beta_m = 37.13^{\circ}\) causes the metal to flow along a curved path. The curved tooth path increases the flow resistance compared with a straight tooth. However, the two-way extrusion process reduces this resistance by splitting the flow into two opposite directions. This is a key advantage for the spiral bevel gear.
Temperature and Friction Effects
Temperature has a strong effect on the forming of the spiral bevel gear. At 1100 \(^{\circ}\)C, AISI-1045 steel has lower flow stress than at room temperature. The die temperature is 350 \(^{\circ}\)C. The temperature difference between the billet and the die causes heat transfer at the interface. I model this heat transfer using the interface heat transfer coefficient. The temperature field influences the flow stress and the load-stroke curve.
The friction coefficient is 0.3. Friction increases the load and can cause non-uniform flow in the spiral bevel gear cavity. In the two-way extrusion process, friction acts on both the upper and lower contact surfaces. Because the flow distance is shorter, the total friction work is lower than in the one-way process. This contributes to the lower maximum load.
I estimate the friction work as
$$ W_f = \int_{0}^{s_{\max}} \int_{A_f} \tau_f v_{\mathrm{rel}} \, dA \, ds $$
where \(v_{\mathrm{rel}}\) is the relative sliding velocity. A lower relative sliding velocity in the two-way process reduces \(W_f\). This is another reason why the two-way extrusion process is efficient for the spiral bevel gear.
Die Design Considerations for the Spiral Bevel Gear
I design the enclosed die for the spiral bevel gear with several important considerations. First, the die must withstand the maximum forming load. The equivalent stress analysis shows that the maximum stress is about 688 MPa, which is well below the allowable stress of 2500 MPa. Therefore, the die material can be selected from common hot forging die steels. Second, the die must allow the two billets to be loaded and ejected easily. The double-action buffering system helps with this. Third, the die must maintain alignment between the upper and lower punches. Misalignment would cause uneven filling of the spiral bevel gear and could damage the teeth.
I also consider the thermal expansion of the die and the billet. At high temperature, the die expands, and the formed spiral bevel gear contracts after cooling. The die cavity must be designed with the appropriate shrinkage allowance. The shrinkage factor can be approximated as
$$ \alpha_s = \frac{L_{\mathrm{die}} – L_{\mathrm{part}}}{L_{\mathrm{part}}} $$
where \(L_{\mathrm{die}}\) is the die dimension at the forming temperature and \(L_{\mathrm{part}}\) is the part dimension at room temperature. For AISI-1045 steel, the thermal expansion coefficient is about \(12 \times 10^{-6} \, \mathrm{K}^{-1}\). I use this value to adjust the die dimensions for the spiral bevel gear.
The die for the spiral bevel gear also needs proper venting. If air is trapped in the tooth cavity, it can prevent complete filling and cause defects. I place vents at the last-to-fill regions, which are the large-end corners of the tooth cavity. This ensures that the spiral bevel gear is filled completely without internal voids.
Feasibility and Advantages of the New Process
Based on my numerical simulation and theoretical analysis, I conclude that the two-way extrusion high-efficiency precision forming process is feasible for the driven spiral bevel gear. The tooth cavity fills smoothly, and the formed tooth shape is good. The load-stroke curve changes normally, and the deformation process can be divided into free deformation, filling, and corner filling. The maximum load is about 23% lower than that of the traditional one-way enclosed die forging process. The equivalent stress is within the allowable range of the die material, and no failure occurs. These results prove that the material flow is good and the new process is feasible.
The new process also has several practical advantages. It forms two spiral bevel gears in one cycle, which doubles productivity. It reduces the maximum load, which lowers the required press capacity and energy consumption. It improves the filling of the tooth cavity, which reduces the risk of incomplete filling. It reduces the load on the die, which extends die life. These advantages make the two-way extrusion process attractive for the industrial production of the spiral bevel gear.
Analytical Summary of the Spiral Bevel Gear Forming Process
I summarize the analytical relations for the spiral bevel gear forming process in Table 6. These relations can be used for preliminary design and for checking simulation results.
| Quantity | Relation | Meaning |
|---|---|---|
| Continuity | \(\nabla \cdot \mathbf{v} = 0\) | Incompressible metal flow |
| Equilibrium | \(\partial \sigma_{ij}/\partial x_j + f_i = 0\) | Force balance in the plastic zone |
| Levy-Mises | \(d\varepsilon_{ij} = d\lambda s_{ij}\) | Plastic strain-stress relation |
| Equivalent stress | \(\sigma_{\mathrm{eq}} = \sqrt{\frac{1}{2}[(\sigma_1-\sigma_2)^2+(\sigma_2-\sigma_3)^2+(\sigma_3-\sigma_1)^2]}\) | Von Mises stress |
| Equivalent strain | \(d\bar{\varepsilon} = \sqrt{\frac{2}{3}d\varepsilon_{ij}d\varepsilon_{ij}}\) | Effective plastic strain |
| Friction | \(\tau_f = \mu p\) | Interface shear stress |
| Forming load | \(F(s) = \int_{A_c} p\cos\theta\,dA + \int_{A_f} \tau_f\sin\theta\,dA\) | Load-stroke relation |
| Forming work | \(W = \int_0^{s_{\max}} F(s)\,ds\) | Energy required |
| Fill ratio | \(R_f = V_{\mathrm{filled}}/V_{\mathrm{cavity}} \times 100\%\) | Cavity filling quality |
| Safety factor | \(n_s = \sigma_{\mathrm{allow}}/\sigma_{\max}\) | Die strength margin |
These relations form a consistent framework for analyzing the spiral bevel gear forming process. I use them to interpret the simulation results and to support the conclusion that the two-way extrusion process is feasible.
Discussion of the Three Deformation Stages
The deformation of the spiral bevel gear can be divided into three stages. In the free deformation stage, the billet is compressed between the upper and lower punches. The billet surface has not yet contacted the die wall, so the deformation is free. The load is low, and the metal flow is not constrained by the tooth cavity. In the filling stage, the billet contacts the die wall, and the tooth cavity begins to fill. The metal flow becomes constrained, and the load increases gradually. In the corner filling stage, the tooth cavity is nearly full, and the remaining volume is at the large-end corners. The load rises rapidly because the metal must flow into narrow corner regions.
I can define the transition strokes \(s_1\) and \(s_2\) from the load-stroke curve. The value of \(s_1\) corresponds to the end of free deformation, and \(s_2\) corresponds to the end of the filling stage. The final stroke \(s_{\max}\) corresponds to complete filling. In my simulation, the stroke levels of 25%, 87%, 98%, and 100% represent these stages. At 25%, the process is in the free deformation stage. At 87%, the process is in the filling stage. At 98%, the process is in the corner filling stage. At 100%, the process is complete.
The three-stage behavior is important for the spiral bevel gear because it shows that most of the cavity fills at a moderate load. Only the final corner filling requires a high load. The two-way extrusion process reduces this final load by allowing the corners to fill from both ends. This is why the maximum load is lower than that of the one-way process.
Stress Concentration and Die Life
The maximum equivalent stress occurs at the tooth root corner. This is a stress concentration region. Although the maximum stress is 688 MPa, which is safe, I still recommend careful design of the die corner radii. A larger corner radius can reduce the stress concentration and further improve die life. The die material should have good hot hardness and thermal fatigue resistance. Common hot forging die steels can satisfy these requirements.
The die life for the spiral bevel gear can be estimated using the Coffin-Manson relation for low-cycle fatigue:
$$ \frac{\Delta \varepsilon_p}{2} = \varepsilon_f’ (2N_f)^c $$
where \(\Delta \varepsilon_p/2\) is the plastic strain amplitude, \(\varepsilon_f’\) is the fatigue ductility coefficient, \(N_f\) is the number of cycles to failure, and \(c\) is the fatigue ductility exponent. Because the maximum stress is well below the allowable stress, the die life is expected to be long. However, thermal cycling and friction also affect die life. Proper lubrication and cooling are necessary.
Process Window and Practical Implementation
I define the process window for the two-way extrusion of the spiral bevel gear in terms of billet temperature, die temperature, friction coefficient, and punch speed. The billet temperature should be high enough to reduce flow stress but not so high that grain growth or oxidation becomes excessive. The die temperature should be high enough to reduce thermal shock but not so high that die strength drops. The friction coefficient should be low to reduce load and improve flow. The punch speed should be moderate to allow complete filling without excessive strain rate.
I summarize the recommended process window in Table 7.
| Parameter | Recommended range | Reason |
|---|---|---|
| Billet temperature | 1050–1150 \(^{\circ}\)C | Low flow stress, acceptable grain size |
| Die temperature | 300–400 \(^{\circ}\)C | Reduce thermal shock, maintain strength |
| Friction coefficient | 0.2–0.4 | Balance flow and load |
| Punch speed | 10–15 mm/s | Complete filling without excessive strain rate |
| Lubrication | Graphite or glass-based | Reduce friction and die wear |
These ranges are based on my simulation and on common practice for hot forging of AISI-1045 steel. They can be adjusted for different press capacities and die materials. The key is to keep the load below the press limit and the stress below the die allowable stress while ensuring complete filling of the spiral bevel gear cavity.
Comparison with Alternative Forming Methods
I also compare the two-way extrusion process with other possible methods for the spiral bevel gear. These include one-way enclosed die forging, cold rotary forging, and machining. Table 8 gives a qualitative comparison.
| Method | Load level | Filling quality | Productivity | Material utilization |
|---|---|---|---|---|
| One-way enclosed die forging | High | Good | Medium | High |
| Two-way extrusion | Lower by about 23% | Very good | High | High |
| Cold rotary forging | High | Good | Medium | High |
| Machining | Low | Excellent | Low | Low |
The two-way extrusion process offers a good balance of load, filling quality, productivity, and material utilization. It is especially suitable for the spiral bevel gear because it reduces the maximum load while maintaining good tooth filling. This makes it a promising alternative to traditional one-way enclosed die forging.
Conclusion of the Study
I have proposed a new forming process for the driven spiral bevel gear: two-way extrusion high-efficiency precision forming. I used numerical simulation to study the filling process, the load-stroke curve, and the equivalent stress field. The results show that the tooth cavity of the spiral bevel gear can be filled smoothly, and the tooth shape is good. The load-stroke curve changes normally, and the deformation process can be divided into three stages: free deformation, filling, and corner filling. Compared with the traditional one-way enclosed die forging process, the maximum load is reduced by about 23%. The equivalent stress is within the allowable range of the die material, and no failure occurs. This proves that the material flow is good and the new process is feasible. The results provide a useful reference for the forming of the spiral bevel gear.
I conclude that the two-way extrusion process is a viable method for the precision forming of the spiral bevel gear. It improves productivity, reduces load, and ensures good filling. With further experimental validation and die optimization, this process can be applied to industrial production of the spiral bevel gear. The spiral bevel gear is a critical component in many transmissions, and the new process can help meet the growing demand for high-quality, low-cost, and energy-efficient manufacturing. I recommend further study on die wear, thermal management, and process control for the spiral bevel gear.