
In the field of wind energy, gearboxes play a critical role in ensuring the efficient operation of turbines. As an engineer specializing in heat treatment and material failure analysis, I have encountered various failure modes in wind power gear shafts. Among these, longitudinal cracking after carburizing and quenching is a particularly concerning issue, as it can lead to catastrophic failures and significant downtime. This article delves into a detailed investigation of such a crack in a wind power gear shaft, employing a first-person perspective to narrate the analytical journey. The focus is on understanding the root cause through comprehensive testing and theoretical evaluation, emphasizing the importance of material integrity and process control in manufacturing reliable gear shafts.
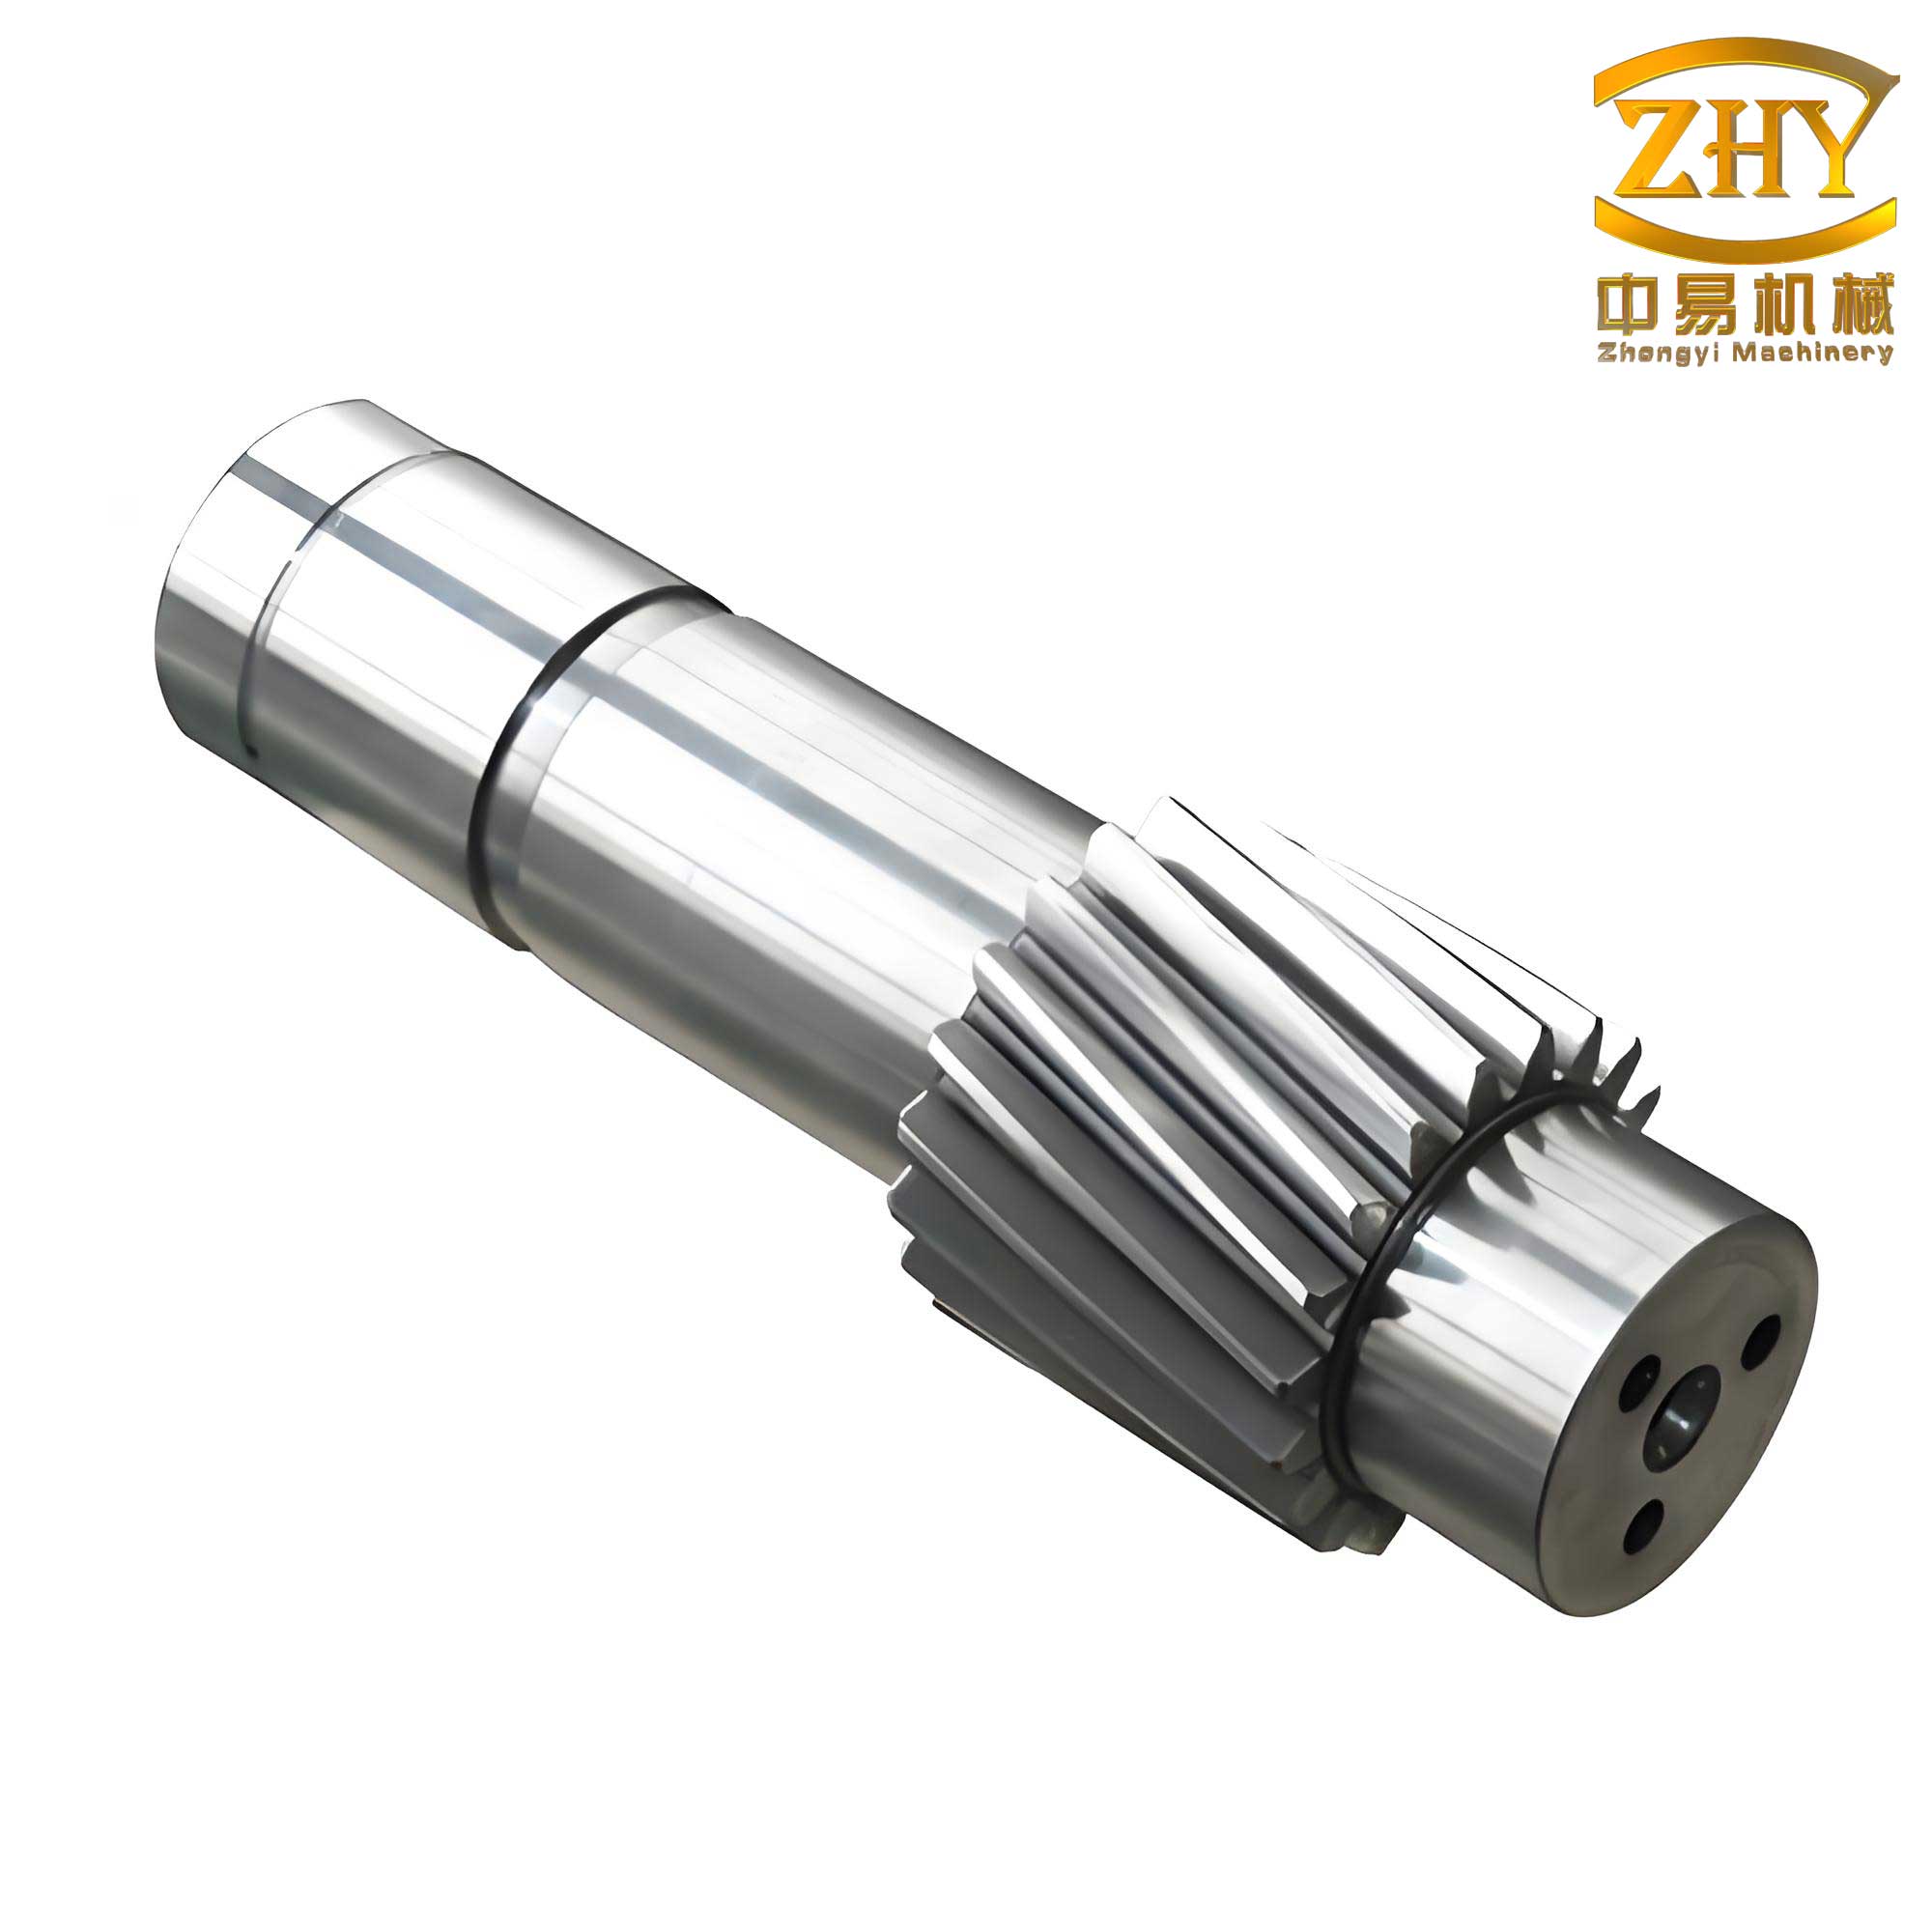
The gear shaft in question was manufactured from 18CrNiMo7-6 steel, following a standard processing route: rough turning, gear hobbing, carburizing/quenching/tempering, finish turning, and gear grinding. In a batch of 12 gear shafts subjected to the same heat treatment cycle, one unit developed a longitudinal crack after being left for two days post-tempering, prior to finish turning. The crack was approximately 1.5 mm wide and located in the middle of the shaft body, specifically on the smooth section near the gear. Over time, the crack propagated axially in both directions, occasionally emitting audible cracking sounds. Upon reaching stepped sections, the crack exhibited a stair-step pattern, and by the fourth day, it had extended through the entire shaft length, even crossing the central axis at the ends. This progressive failure hinted at a delayed cracking mechanism, likely driven by residual stresses.
To systematically unravel the cause, I initiated a multi-faceted experimental plan. The first step involved macro-examination of the fracture surface after splitting the gear shaft along its longitudinal axis. The fracture exhibited classic brittle characteristics, with radial ridges converging at a grayish-white region approximately 220 mm from the gear end face and 12 mm beneath the shaft surface. This region contained an elongated strip-like inclusion, about 5.50 mm in length and 0.40 mm in width, which served as the apparent crack origin. Chevron patterns were visible away from the origin, particularly near the shaft surface, indicating the crack propagation direction. The overall fracture morphology varied from relatively smooth near the surface to coarse at mid-radius and back to smooth near the core, suggesting differences in material properties and stress states.
Next, I performed material characterization on samples extracted from the crack origin vicinity. Chemical composition analysis confirmed that the gear shaft material met the specifications for 18CrNiMo7-6 steel. The results are summarized in Table 1.
| Element | C | Si | Mn | P | S | Cr | Mo | Ni | Cu | Al | Fe |
|---|---|---|---|---|---|---|---|---|---|---|---|
| Measured | 0.20 | 0.26 | 0.78 | 0.012 | 0.015 | 1.73 | 0.30 | 1.46 | 0.02 | 0.03 | Bal. |
| Requirement | 0.15-0.21 | ≤0.40 | 0.50-0.90 | ≤0.025 | ≤0.025 | 1.50-1.80 | 0.28-0.35 | 1.40-1.70 | ≤0.30 | ≤0.05 | Bal. |
Gas content analysis, particularly for hydrogen, is crucial in understanding hydrogen-assisted cracking. The results, shown in Table 2, indicated that the average hydrogen content was within acceptable limits, though localized hydrogen accumulation could not be ruled out.
| Gas | O2 | N2 | H2 |
|---|---|---|---|
| Measured | 12 | 100 | 2 |
| Requirement | ≤25 | 50-150 | ≤2.5 |
Non-metallic inclusion assessment according to standard ratings revealed no severe inclusion clusters in routine inspections (Table 3). However, this did not preclude the presence of large, isolated inclusions that might be missed by standard metallographic sampling.
| Type | A (Coarse) | A (Fine) | B (Coarse) | B (Fine) | C (Coarse) | C (Fine) | D (Coarse) | D (Fine) |
|---|---|---|---|---|---|---|---|---|
| Rating | 0 | 0.5 | 0 | 0.5 | 0 | 0 | 0 | 1.0 |
| Max Allowable | ≤3.0 | ≤3.0 | ≤1.5 | ≤2.5 | ≤1.5 | ≤2.5 | ≤1.5 | ≤2.0 |
Hardness profiling was conducted to evaluate the effectiveness of the carburizing process. Vickers hardness measurements from the crack origin area and various gear locations (tip, pitch, root) demonstrated that surface hardness and case depth complied with technical specifications, as detailed in Table 4. The consistent hardness values across different sections suggested that the heat treatment process was uniformly applied to the gear shafts.
| Location | Surface Hardness (HRC) | Case Depth (mm at 550 HV1) |
|---|---|---|
| Near Crack Origin | 59.7 | 1.85 |
| Gear Tip | 61.2 | 2.55 |
| Gear Pitch | 60.3 | 2.16 |
| Gear Root | 59.9 | 1.75 |
| Requirement | 58-62 | 1.52-2.80 |
Mechanical property tests, including tensile and impact tests on longitudinal specimens taken from the R/2 region near the crack origin, were performed. The results, presented in Table 5, indicated that the gear shaft material possessed adequate strength, ductility, and toughness, fulfilling all mechanical requirements. This suggested that the bulk material properties were not the primary cause of failure.
| Property | Tensile Strength (MPa) | Elongation δ5 (%) | Reduction of Area ψ (%) | Impact Energy (J) |
|---|---|---|---|---|
| Measured | 1230 | 15.1 | 63.7 | 122 |
| Requirement | ≥1080 | ≥11 | ≥35 | ≥25 |
Microstructural examination via optical microscopy revealed a typical carburized structure: a case region consisting of needle-like martensite with an average retained austenite content of 12% (within the specified limit of <20%), and a core region of lath martensite. No abnormalities such as excessive grain growth, decarburization, or non-martensitic transformation products were observed. This further supported the conclusion that the heat treatment process was correctly executed for these gear shafts.
The most revealing evidence came from scanning electron microscopy (SEM) of the fracture surface, specifically the origin region. The strip-like inclusion was composed of numerous particulate aggregates. Energy-dispersive X-ray spectroscopy (EDS) area scans and point analyses on these particles showed high concentrations of aluminum and oxygen, with traces of other elements. A representative EDS spectrum from a particle surface is summarized in Table 6, confirming the inclusion as aluminum oxide (Al2O3) slag.
| Element | C K | O K | Al K | Ti K | Cr K | Fe K | Total |
|---|---|---|---|---|---|---|---|
| Atomic % | 6.84 | 57.19 | 32.50 | 0.39 | 0.23 | 2.84 | 100.00 |
| Weight % | 3.98 | 44.34 | 42.50 | 0.91 | 0.59 | 7.68 | 100.00 |
Fractography near the origin exhibited classic intergranular fracture features with fine tear ridges on grain boundaries, indicative of hydrogen embrittlement. Moving away from the origin, the fracture mode transitioned to quasi-cleavage and finally to ductile dimpling in the core region. The carburized case predominantly showed intergranular fracture, aligning with the high hardness and susceptibility to environmentally assisted cracking.
To understand the failure mechanism, I delved into the interplay between residual stresses, material defects, and hydrogen. After carburizing and quenching, gear shafts develop a characteristic residual stress profile: the carburized surface is in compression, while the subsurface region experiences tensile stresses. The maximum tensile stress typically occurs just below the case-core interface. The crack origin in this gear shaft was located approximately 12 mm below the surface, precisely within this high tensile stress zone. The presence of a large, hard Al2O3 inclusion at this location created a severe stress concentrator. The stress intensity factor (K) at the tip of such an inclusion can be approximated for a semi-elliptical surface crack under mode I loading:
$$K_I = \sigma \sqrt{\pi a} \, F\left(\frac{a}{c}, \frac{a}{t}, \phi\right)$$
where $\sigma$ is the applied stress (here, the residual tensile stress), $a$ is the crack depth, $c$ is the crack half-length, $t$ is the thickness, and $F$ is a geometric correction factor. The inclusion effectively acts as an initial crack, significantly raising the local KI value.
Hydrogen, even in small average concentrations, can diffuse and accumulate at sites of high triaxial stress, such as inclusion tips or grain boundaries. The diffusion of hydrogen in steel is governed by Fick’s laws. The steady-state flux J is given by:
$$J = -D \frac{\partial C}{\partial x}$$
where D is the diffusion coefficient and C is the hydrogen concentration. In the presence of a stress gradient, an additional term drives hydrogen to the region of maximum hydrostatic tension:
$$J = -D \nabla C + \frac{D C}{RT} \bar{V}_H \nabla \sigma_h$$
where R is the gas constant, T is the absolute temperature, $\bar{V}_H$ is the partial molar volume of hydrogen, and $\sigma_h$ is the hydrostatic stress. This process leads to localized hydrogen enrichment at the inclusion tip, reducing the cohesive strength of the metal lattice or grain boundaries.
The critical combination of stress intensity and hydrogen concentration for crack initiation can be described by a threshold stress intensity factor for hydrogen-assisted cracking, KIH. When KI ≥ KIH, subcritical crack growth occurs. This phenomenon is responsible for delayed failure, as observed in the gear shaft which cracked days after heat treatment. The intergranular fracture morphology near the inclusion is a hallmark of hydrogen-induced cracking, where hydrogen accumulation at grain boundaries facilitates decohesion.
In this specific case, the large aluminum oxide slag inclusion served as a potent hydrogen trap and stress raiser. During the carburizing process, which involves exposure to hydrocarbon atmospheres, hydrogen can be introduced into the steel. Although the final average hydrogen content was low, the localized concentration at the inclusion tip could have been significantly higher. Post-quenching, the high residual tensile stress in the subsurface region provided the driving force. The synergistic effect of stress concentration from the inclusion and hydrogen embrittlement led to the initiation of an intergranular microcrack. Once initiated, the crack propagated under the residual stress field, following the path of least resistance. The crack path through the gear shaft was influenced by the microstructure and stress state: it propagated axially in the high-tensile-stress zone, deviating at geometric discontinuities like steps, and eventually traversing the entire cross-section.
The fact that only one out of twelve gear shafts in the same batch failed is highly significant. It points to a sporadic material defect rather than a systematic heat treatment error. Routine quality checks on raw materials, such as standard inclusion rating, might not detect isolated, macro-scale slag inclusions. This underscores the need for more sensitive non-destructive testing (NDT) methods, like ultrasonic testing, during the incoming inspection of forged or rolled bars for critical components like wind power gear shafts. Ultrasonic waves can reflect off large inclusions, providing a means to screen out defective material before costly machining and heat treatment.
Furthermore, heat treatment practices can be optimized to mitigate such risks. While timely tempering is essential to relieve quenching stresses and allow hydrogen to diffuse out, the tempering temperature and duration must be sufficient. For high-strength steels like 18CrNiMo7-6, a two-stage tempering or a longer holding time at an appropriate temperature (e.g., 180-200°C or higher, depending on hardness requirements) could be beneficial. The tempering process not only reduces residual stresses but also allows trapped hydrogen to escape, thereby lowering the risk of delayed cracking. The kinetics of hydrogen effusion during tempering can be modeled using the diffusion equation with appropriate boundary conditions. The approximate time t for a significant reduction in hydrogen content at a given depth x can be estimated from:
$$C(x,t) = C_0 \, \text{erfc}\left(\frac{x}{2\sqrt{Dt}}\right)$$
where C0 is the initial concentration and erfc is the complementary error function. Ensuring adequate tempering time is thus crucial for gear shafts.
In summary, the longitudinal crack in this wind power gear shaft was a classic case of hydrogen-assisted delayed fracture, instigated by a large exogenous aluminum oxide inclusion located in the subsurface tensile stress zone. The combination of a severe stress concentrator, residual tensile stresses from quenching, and locally elevated hydrogen concentration led to intergranular crack initiation and subsequent propagation. The material’s bulk chemistry, microstructure, hardness, and mechanical properties were all within specifications, confirming that the failure was due to a localized material flaw rather than a process deviation.
To prevent recurrence in future productions of gear shafts, I recommend a two-pronged approach: enhanced raw material screening and optimized heat treatment practices. First, implement mandatory ultrasonic testing for all incoming bar stock destined for high-stress components like gear shafts to detect and reject pieces containing large inclusions. Second, review and potentially extend the tempering cycle to ensure maximum stress relief and hydrogen removal, without compromising the required hardness. Additionally, considering the criticality of wind turbine gearboxes, statistical process control for all manufacturing steps, from forging to final grinding, is essential to ensure the reliability and longevity of gear shafts. Continuous research into cleaner steelmaking practices and advanced NDT technologies will further contribute to the production of defect-free gear shafts for the wind energy industry.