
In modern agricultural production, cotton pickers are essential machinery for harvesting cotton. The spindle bevel gear pair, a critical component within the picking head, plays a vital role in transmitting power from the spindle tube to the spindle, thereby driving the spindle’s rotation. During prolonged operation of the cotton picker, the failure rate of these bevel gears is notably high. Any malfunction in the bevel gear pair can halt the spindle’s operation, rendering the picking head ineffective and leading to incomplete cotton harvesting, resource waste, and increased costs due to the need for secondary harvesting. Traditionally, decisions to replace spindles were based on visual inspection of hook wear, without considering the fatigue and wear condition of the bevel gears. Therefore, analyzing the spindle bevel gear pair is crucial for maintenance personnel to understand the current state of the picking head, provide theoretical guidance for part replacement, reduce downtime during harvest seasons, ensure operational efficiency, and optimize the utilization of cotton pickers.
This study focuses on predicting the fatigue life of spindle bevel gears through a comprehensive approach involving three-dimensional modeling, finite element analysis (FEA), and fatigue life assessment. Initially, accurate three-dimensional models of the spindle bevel gear and the spindle tube bevel gear are developed. Subsequently, contact finite element analysis is performed using ABAQUS to obtain stress distributions. Finally, the FEA results are imported into the fatigue analysis software Femfat to compute fatigue life data, including cycle counts and service life. These data enable the prediction of the spindle bevel gear’s operational lifespan, facilitating proactive monitoring, maintenance, and replacement strategies.
The cotton picker model referenced in this study is the horizontal spindle-type 4MZ-5A, with all data aligned to this model. The picking head contains a large number of spindles, with each drum typically housing multiple spindle tubes. For instance, a single picking head may have up to 432 spindles, emphasizing the importance of each spindle bevel gear’s reliability. Given that all spindle bevel gears operate under similar conditions, a representative pair from the outermost position is selected for detailed simulation analysis.
Three-Dimensional Modeling of the Bevel Gear Pair
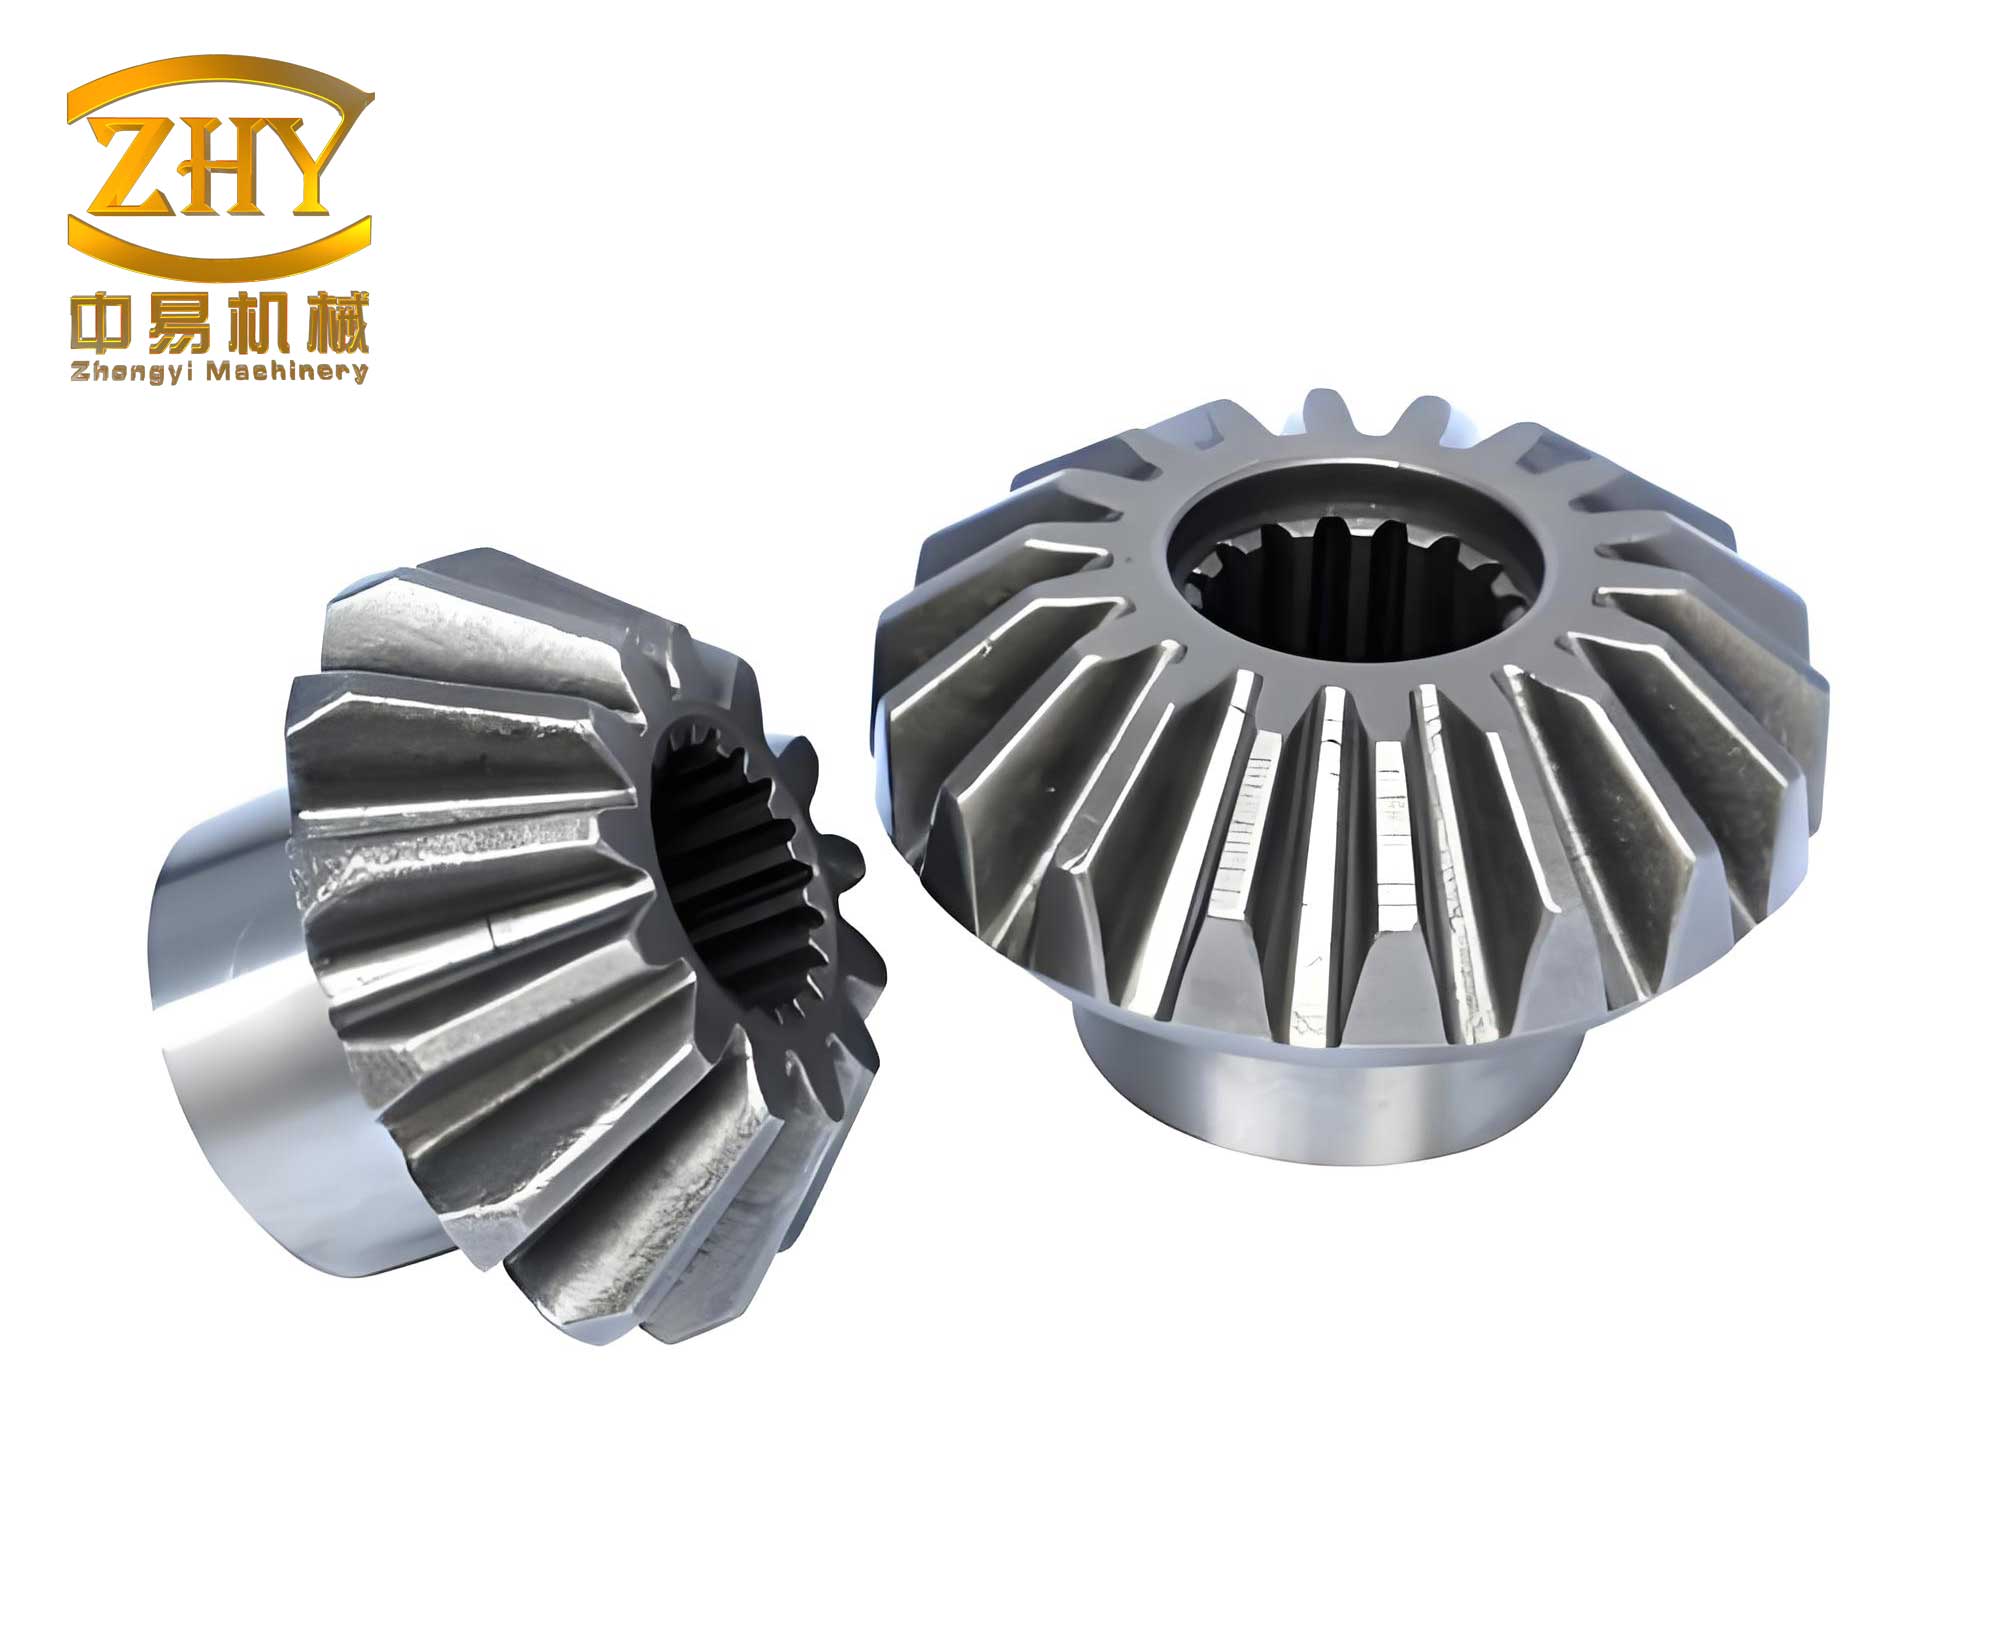
The first step involves creating precise geometric models of the spindle bevel gear and the spindle tube bevel gear. The gear parameters are derived from the actual components of the 4MZ-5A cotton picker. Using SolidWorks software, the Toolbox plugin is employed to generate straight bevel gears based on the specified parameters. The key parameters for the bevel gear pair are summarized in Table 1.
| Gear Type | Module (mm) | Number of Teeth | Pressure Angle (°) |
|---|---|---|---|
| Spindle Bevel Gear | 1.25 | 18 | 20 |
| Spindle Tube Bevel Gear | 1.25 | 20 | 20 |
After modeling, the gears are assembled to ensure proper meshing without interference. The assembly is then exported in x_t format for subsequent finite element analysis. The material selected for both bevel gears is 20CrMnTi, a common alloy steel used in gear applications due to its strength and durability. The material properties are as follows:
- Density: 7800 kg/m³
- Young’s Modulus: 210 GPa
- Poisson’s Ratio: 0.3
These properties are essential for accurate simulation of the bevel gear behavior under load.
Finite Element Analysis of the Bevel Gear Pair
The finite element analysis is conducted using ABAQUS/Standard module, which is suitable for static and low-speed dynamic problems requiring high stress accuracy, especially for contact simulations. The analysis aims to determine the stress distribution in the bevel gear pair under operational loads.
Mesh Generation
Mesh generation is a critical step in FEA, influencing both computational accuracy and efficiency. For the bevel gear pair, a hybrid meshing strategy is adopted. The gear teeth, which are the primary focus for stress analysis, are partitioned and meshed with hexahedral elements to achieve higher precision. The remaining parts of the gears are meshed with tetrahedral elements to reduce computational complexity. This approach ensures detailed stress analysis at the contact regions while maintaining reasonable computational time. The meshed model contains approximately 226,252 elements and 149,231 nodes, with refined hexahedral grids at the tooth surfaces as shown in Figure 3 (refer to image for visual).
Boundary Conditions and Load Application
To simulate the actual working conditions, appropriate boundary conditions and loads are applied. The spindle tube bevel gear is considered the driving gear, while the spindle bevel gear is the driven gear. Constraints are applied at the reference points located on the gear axes. For the driving bevel gear, five degrees of freedom are constrained, allowing only rotation about its axis. The rotational displacement is calculated based on the operational speed. For the driven bevel gear, all translational and rotational degrees of freedom are constrained except for the rotation about its axis, which is free to respond to the applied torque.
The load is derived from the power transmitted to the picking drum. The cotton picker’s drum power is P₀ = 4.4 kW, with a rotational speed of n₀ = 2200 rpm. Through a series of gear transmissions within the drum, the torque applied to the spindle bevel gear is calculated. The torque T on the spindle bevel gear can be expressed as:
$$ T = \frac{9550 \times P_0 \times \eta_1 \times \eta_2 \times \eta_3 \times \eta_4 \times \eta_5 \times i_1 \times i_2 \times i_3 \times i_4 \times i_5}{n} $$
where P₀ is the drum power, η₁ to η₅ are the transmission efficiencies between successive shafts, i₁ to i₅ are the gear ratios, and n is the rotational speed of the spindle bevel gear. After computation, the torque is found to be T = 7560 N·m, with a rotational speed of n = 140.7 rad/s.
To ensure a smooth simulation, the load is applied gradually using an amplitude curve that ramps from 0 to 0.0001 over the step time, representing a quasi-static application of force.
Stress Analysis Results
The FEA results reveal the stress distribution in the bevel gear pair. The maximum stress is concentrated at the tooth root fillet regions of both gears, indicating potential failure points. The stress contours show that the tooth surfaces and roots experience the highest stresses during meshing, as illustrated in Figures 6 and 7 (refer to image for visual). This alignment with theoretical expectations confirms that the bevel gear teeth are susceptible to fatigue damage, particularly at the stress concentration areas.
The equivalent stress (von Mises stress) is used to assess the yield criterion. For the bevel gear material 20CrMnTi, the yield strength is σ_s = 835 MPa, and the ultimate tensile strength is σ_b = 1080 MPa. The FEA shows that the maximum stress values are within the material limits under the applied load, but cyclic loading can lead to fatigue over time.
Fatigue Life Prediction of the Bevel Gear
Fatigue life prediction is performed using Femfat software, which incorporates advanced methodologies such as the FKM guideline, synthetic S-N curves, and local stress-strain approaches. The fatigue analysis requires input parameters including the fatigue strength limit, corresponding cycle numbers, yield strength, and tensile strength.
Material Data and S-N Curve
The material data for 20CrMnTi is configured in Femfat’s material generator. The basic properties are as follows:
| Property | Value |
|---|---|
| Tensile Strength (σ_b) | 1080 MPa |
| Yield Strength (σ_s) | 835 MPa |
| Fatigue Strength Limit (for bending) | Approx. 500 MPa (at 10⁶ cycles) |
The S-N curve, which relates stress amplitude to the number of cycles to failure, is generated based on these parameters. The curve is adjusted for factors such as surface finish, size, and loading conditions. The general form of the S-N curve for steels can be expressed as:
$$ S^m \cdot N = C $$
where S is the stress amplitude, N is the number of cycles, m is the slope exponent, and C is a material constant. For 20CrMnTi, the S-N curve is plotted with logarithmic scales, showing a decreasing stress capacity with increasing cycles, as depicted in Figure 8 (refer to image for visual).
Fatigue Analysis Setup and Results
The FEA stress results from ABAQUS are imported into Femfat. The analysis focuses on the spindle bevel gear, with a survival probability set to 90%. The fatigue life is computed based on the stress history from the static analysis, assuming cyclic loading corresponding to the operational conditions.
The fatigue analysis outputs the damage value and safety factors across the gear geometry. The critical location is identified at the tooth root, where the damage value exceeds the threshold. The fatigue life, expressed in cycles, is determined as the number of cycles at which the damage value reaches 1 (indicating failure). For the spindle bevel gear, the predicted fatigue life is approximately 4.04 × 10⁵ cycles. This means that after about 404,000 meshing cycles, the bevel gear is likely to develop fatigue cracks.
The safety factor contour plot (Figure 10, refer to image for visual) shows that regions with safety factors below 1 are concentrated at the tooth roots, corroborating the FEA stress concentrations. To extend the service life of the bevel gear, preventive measures such as lubrication are recommended. Regular application of grease can reduce friction and wear between the meshing teeth, thereby delaying fatigue initiation.
Discussion on Factors Influencing Bevel Gear Fatigue Life
The fatigue life of spindle bevel gears is influenced by multiple factors, including operational environment, load variations, material properties, and maintenance practices. In cotton pickers, the bevel gears operate under continuous high-speed rotation with intermittent shocks due to cotton plant interactions. These dynamic loads can accelerate fatigue damage.
Key parameters affecting fatigue life include:
- Load Magnitude and Fluctuations: Higher torques and variable loads reduce fatigue life. The torque calculated (7560 N·m) represents a typical operational load, but overload conditions during field operations can shorten life.
- Material Strength and Microstructure: The use of 20CrMnTi provides good fatigue resistance, but heat treatment processes like carburizing can enhance surface hardness and fatigue strength.
- Geometric Design: The tooth profile, pressure angle, and root fillet radius influence stress concentration. Optimizing these parameters can improve fatigue performance.
- Lubrication and Wear: Proper lubrication reduces surface pitting and wear, which are precursors to fatigue failure. Inadequate lubrication can lead to accelerated damage.
- Manufacturing Tolerances: Imperfections in gear manufacturing, such as misalignments or surface roughness, can introduce additional stresses.
To quantify some of these effects, empirical formulas can be used. For example, the modified Goodman relation for mean stress effect is:
$$ \frac{\sigma_a}{\sigma_f’} + \frac{\sigma_m}{\sigma_u} = 1 $$
where σ_a is the stress amplitude, σ_m is the mean stress, σ_f’ is the fatigue strength coefficient, and σ_u is the ultimate strength. This relation helps in assessing the impact of non-zero mean stresses on fatigue life.
Furthermore, the Palmgren-Miner linear damage rule is often applied for cumulative fatigue damage under varying loads:
$$ D = \sum_{i=1}^{k} \frac{n_i}{N_i} $$
where D is the total damage (failure when D ≥ 1), n_i is the number of cycles at stress level i, and N_i is the fatigue life at that stress level. For the spindle bevel gear, under constant amplitude loading, the damage accumulates linearly until reaching the predicted cycle count.
Conclusion
This study successfully establishes a simulation platform for fatigue life prediction of spindle bevel gears in cotton pickers by integrating SolidWorks, ABAQUS, and Femfat. The three-dimensional modeling, finite element analysis, and fatigue assessment provide a comprehensive understanding of the stress distribution and fatigue behavior of the bevel gear pair. The results indicate that the spindle bevel gear has a predicted fatigue life of approximately 4.04 × 10⁵ cycles under normal operational conditions, with critical fatigue sites located at the tooth roots. This information is valuable for scheduling maintenance, such as lubrication or replacement, to prevent unexpected failures and ensure efficient cotton harvesting. Future work could involve experimental validation, dynamic load analysis, and optimization of gear design to enhance fatigue resistance. Overall, this approach contributes to the reliability and cost-effectiveness of cotton pickers in agricultural applications.
By leveraging simulation tools, maintenance strategies can transition from reactive to proactive, minimizing downtime and maximizing productivity. The emphasis on bevel gear analysis underscores the importance of each component in complex machinery like cotton pickers, where numerous bevel gears work in unison to achieve seamless operation. Continued research in this area will further refine fatigue life predictions and extend the service life of critical agricultural equipment.