
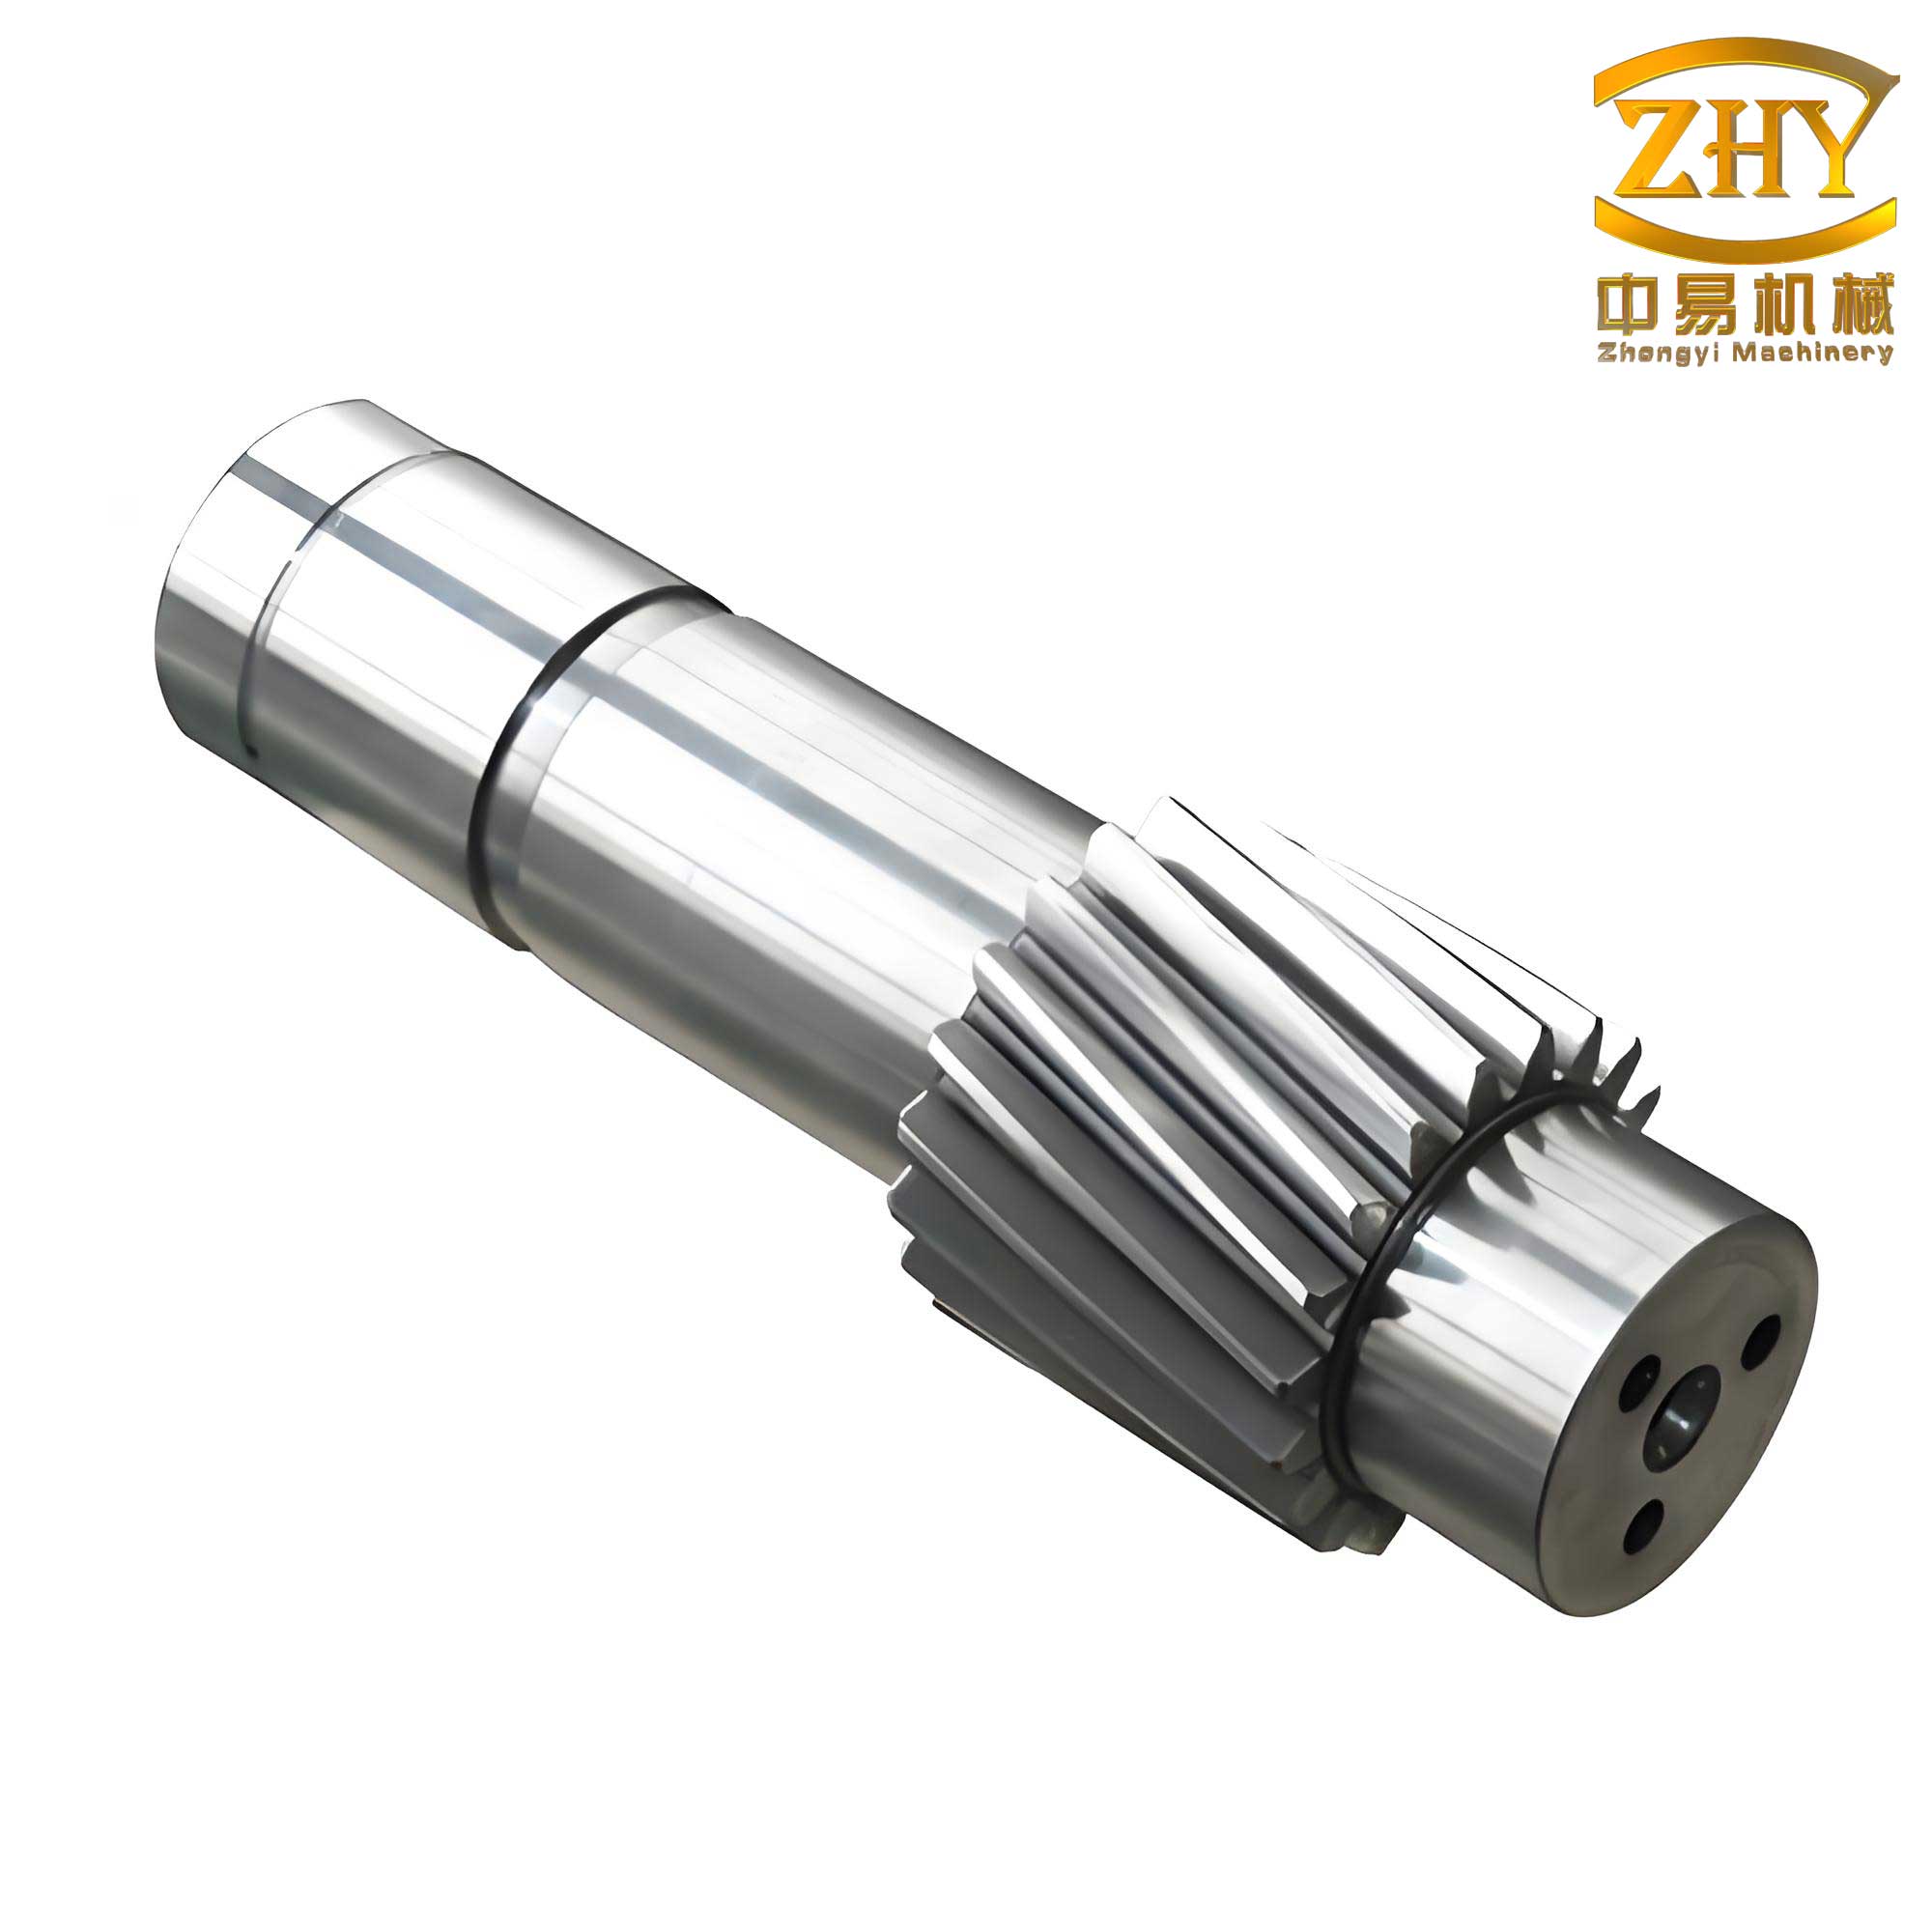
In the manufacturing of heavy machinery for power generation, metallurgy, petrochemicals, and mining, large forgings serve as critical foundational components. The performance and reliability of these massive parts directly influence the operational safety and efficiency of entire industrial systems. Among them, the large-section gear shaft forging is a paramount component within power transmission systems, such as those found in ball mills. These gear shafts operate under extremely complex and demanding conditions, often involving heavy loads, shock, and continuous stress cycles. Consequently, they are highly susceptible to failures like severe wear and catastrophic fracture. Such failures lead to extensive, unplanned downtime for maintenance, causing significant production losses and economic impact. A primary, and particularly insidious, cause of such failures is the presence of internal defects known as flakes, or white spots.
Flakes are internal micro-cracks that manifest on a fracture surface as small, bright, silvery-white areas. On a longitudinal section, they appear as round or oval spots, while on a transverse section, they look like fine, jagged cracks or hairline fissures. This defect is predominantly found in large forgings and heavy-gauge rolled steels with effective cross-sections exceeding 40 mm, with susceptibility increasing dramatically with part size. For a mission-critical component like a large-section gear shaft, the appearance of flakes is an absolute cause for rejection, as they act as potent stress concentrators and initiation points for fatigue cracks that can propagate under service loads, leading to sudden, brittle fracture. The insidious nature of flakes lies in their complete internal concealment; they are never open to the surface. This characteristic introduces a element of “delayed failure,” meaning a gear shaft that passes initial inspection and is shipped as合格 may still harbor this fatal flaw, posing a significant reliability risk. Therefore, systematic research into the mechanisms of flake formation and the development of robust preventive measures for large-section gear shaft forgings is of utmost importance for advancing manufacturing capability and quality control in heavy industry.
The material at the heart of this investigation is 17CrNiMo6 steel, a chromium-nickel-molybdenum alloy specifically designed for high-strength, tough, case-hardened components. The typical manufacturing route for a large 17CrNiMo6 gear shaft involves several critical stages: primary melting and secondary refining, forging, post-forging heat treatment (normalizing and tempering), case carburizing, and final quenching and tempering. The core philosophy is to create a component with a hard, wear-resistant surface and a tough, ductile core. The base carbon content (0.17-0.20%) provides good core toughness. Through carburizing, the surface layer (1-10 mm deep) is enriched with carbon, transforming it into a high-carbon steel. Subsequent quenching hardens this case to a high surface hardness (57-61 HRC), while the core achieves a lower, tougher hardness (34-38 HRC). However, this complex thermochemical processing also introduces challenges, primarily the risk of hydrogen absorption and the development of internal stresses, which are the two fundamental factors driving flake formation. The formation mechanism can be summarized by the pressure theory: atomic hydrogen (H) diffuses and accumulates in micro-voids or discontinuities within the steel matrix. Under the influence of transformational and thermal stresses, this molecular hydrogen (H₂) recombines, creating immense internal pressure that exceeds the local tensile strength of the material, resulting in the initiation of an internal crack—the flake. The susceptibility can be modeled as a function of hydrogen concentration, stress state, and material ductility:
$$ S_f = f([H], \sigma_{internal}, \frac{1}{\delta}) $$
Where \( S_f \) is flake susceptibility, \( [H] \) is the dissolved hydrogen concentration, \( \sigma_{internal} \) is the magnitude of internal stress, and \( \delta \) is the material’s ductility. The goal of process optimization is to minimize \( [H] \) and \( \sigma_{internal} \) while maximizing \( \delta \).
I. Optimizing the Melting and Refining Process
The battle against flakes begins at the very origin of the material: the melt shop. The initial hydrogen content dissolved in the liquid steel and the presence of certain elements that influence hydrogen trapping are crucial. The standard production route involves Electric Arc Furnace (EAF) melting, followed by Ladle Furnace (LF) refining, Vacuum Degassing (VD), and finally, vacuum stream casting. The VD process is the primary weapon for hydrogen removal, governed by the Sieverts’ law principle where the solubility of hydrogen in steel is proportional to the square root of its partial pressure above the melt:
$$ [H] \propto \sqrt{P_{H_2}} $$
By reducing the ambient pressure in the vacuum tank to a very low level (e.g., below 1 mbar), the equilibrium is shifted, forcing hydrogen out of the solution in the steel and into the vacuum exhaust. The kinetics of this removal are not instantaneous; they require time. The original process stipulated a VD holding time under full vacuum of ≥15 minutes. Analysis of scrap gear shaft components from multiple heats suggested this duration was insufficient for adequate dehydrogenation, especially for the large mass of steel required for a big gear shaft forging.
Furthermore, the role of micro-alloying elements like Niobium (Nb) and their interaction with nitrogen (N) was scrutinized. Niobium is sometimes added to refine the austenite grain size. However, in the presence of nitrogen, it forms very fine, stable nitride precipitates (NbN). While these can pin grain boundaries, they also create irreversible trapping sites for hydrogen. More critically, during the high-temperature forging and heat treatment cycles, these fine NbN precipitates can contribute to embrittlement and promote crack initiation under stress. The original practice involved a niobium addition of 0.03%. The objective of the optimized melting process was twofold: 1) Enhance hydrogen removal, and 2) Modify the matrix to reduce harmful nitride formation.
Optimized Melting Practice:
1. Extended Vacuum Degassing: The effective VD time under vacuum was increased to a minimum of ≥18 minutes. This extended period allows for more complete diffusion of hydrogen from the center of the molten bath to the surface where it can escape. The dehydrogenation rate can be approximated by a diffusion-controlled model:
$$ \frac{d[H]}{dt} = -D_{H} \cdot A \cdot \frac{[H]_{bulk} – [H]_{surface}}{L} $$
Where \( D_{H} \) is the diffusivity of H in liquid steel, \( A \) is the melt surface area, and \( L \) is a characteristic diffusion length. Increasing time \( t \) directly increases the total amount of hydrogen removed.
2. Reduced Niobium Addition: The Nb addition was carefully lowered to a target of 0.02%. This reduction aims to limit the formation of fine, detrimental NbN precipitates without completely eliminating the potential grain-refining benefit.
3. Promoted Formation of Benign Compounds: By allowing slightly higher levels of Silicon (Si) and through deliberate Aluminum (Al) killing (喂铝线), the formation of other compounds like SiC and AlN is encouraged. These compounds, particularly AlN, act as stronger, irreversible traps for hydrogen. Hydrogen trapped at these stable sites is rendered immobile and less likely to diffuse and coalesce into critical concentrations at stress concentrators. The change in chemical composition focus is clear in the comparison below.
| Element | Standard Range | Average Before Optimization (6 Heats) | Average After Optimization (6 Heats) | Key Change & Rationale |
|---|---|---|---|---|
| C | 0.17-0.20 | 0.18 | 0.17 | Maintained within spec. |
| Si | ≤0.40 | 0.03 | 0.25 | Increased. Promotes SiC formation. |
| Al | – | 0.002 | 0.012 | Increased significantly. For deoxidation and AlN formation (strong H trap). |
| Nb | 0.030 (aim) | 0.020 | 0.016 | Reduced. Limits harmful NbN precipitation. |
| S, P | ≤0.035 | <0.010 | <0.008 | Kept very low for purity. |
The results confirm the intended shift: Si and Al contents are notably higher in the optimized process, while Nb is lower. This chemical profile is more conducive to creating a matrix with benign hydrogen traps (AlN) and fewer embrittling phases (NbN), thereby intrinsically lowering the flake susceptibility of the gear shaft steel from the very beginning.
II. Optimizing the Forging and Post-Forging Heat Treatment
The forging process serves to consolidate the ingot structure, close shrinkage porosity, and shape the gear shaft preform. However, its most critical role in flake prevention is as the first and most effective opportunity for “hydrogen diffusion treatment.” After solidification, a significant amount of hydrogen remains in solid solution or in reversible traps. The high temperatures involved in forging and subsequent heat treatments increase hydrogen diffusivity exponentially, as described by the Arrhenius equation:
$$ D_H = D_0 \cdot \exp\left(-\frac{Q}{RT}\right) $$
Where \( D_H \) is the diffusion coefficient, \( D_0 \) is a pre-exponential factor, \( Q \) is the activation energy for diffusion, \( R \) is the gas constant, and \( T \) is the absolute temperature. The goal of post-forging heat treatment (PFHT) is to hold the forged gear shaft at an elevated temperature for a sufficiently long time to allow this highly mobile hydrogen to diffuse out of the steel entirely. The original PFHT cycle for the gear shaft involved two normalization steps followed by a very long, single high-temperature temper at 650°C for 60 hours (see simplified diagram: Fig.3 in source). While this was a substantial dehydrogenation effort, field failures indicated it was still inadequate for the massive cross-section of the gear shaft.
Optimized Forging & PFHT Practice:
1. Enhanced Normalizing Temperature: The normalizing temperature was increased from approximately 880-900°C to 950°C. Normalizing aims to refine the coarse as-forged grain structure and homogenize the microstructure. The higher temperature ensures complete austenitization and enhances the mobility of all alloying elements and hydrogen, promoting a more uniform starting condition before the prolonged temper. The grain growth at this temperature is controlled by the subsequent cool.
2. Drastically Extended Tempering Time: The single high-temperature temper (650°C) holding time was increased from 60 hours to 100 hours. This is the most impactful change. The diffusion distance \( x \) of hydrogen is related to time and temperature by:
$$ x \approx \sqrt{D_H \cdot t} $$
Doubling the time increases the effective diffusion distance by a factor of \( \sqrt{2} \approx 1.4 \). For a large-section gear shaft where the critical distance is from the center to the surface, this extended time is essential to ensure hydrogen from the core has enough time to reach the surface and desorb. The prolonged heating also significantly reduces internal residual stresses from forging.
| Process Stage | Original Parameters | Optimized Parameters | Intended Effect |
|---|---|---|---|
| Normalizing Temp. | ~880-900 °C | 950 °C | Complete homogenization, higher H mobility. |
| High-Temp Tempering | 650 °C / 60 h | 650 °C / 100 h | Maximizes H diffusion out of the gear shaft bulk; major stress relief. |
The metallographic examination of trial forgings revealed a stark improvement. Gear shaft preforms produced under the old工艺 often showed severe surface cracking and pronounced segregation bands. After optimization, the surface quality was excellent, with a fine, uniform microstructure and no significant cracking. This confirms that the combined effect of higher homogenization temperature and vastly extended tempering effectively reduced hydrogen concentration gradients and local aggregation, mitigating the primary drivers for flake formation at this early stage.
III. Optimizing the Case Carburizing, Quenching, and Tempering Process
The final heat treatment steps impart the necessary surface properties to the gear shaft but reintroduce risks. Case carburizing, typically performed at 930°C in an endothermic atmosphere with hydrocarbon enrichment, not only introduces carbon into the surface but also is a potent source of hydrogen (from the cracking of hydrocarbon gases). This process can recharge the surface layers of the gear shaft with hydrogen. Subsequent quenching, necessary to harden the case, generates enormous transformational stresses (both thermal and phase change). The combination of new hydrogen and high stress creates a perfect environment for flake initiation, often explaining why defects are discovered only after final machining and inspection.
Furthermore, the high carbon content in the case leads to a significant amount of retained austenite after quenching. Retained austenite is a metastable phase that is softer and can gradually transform to martensite under stress or during subsequent tempering, generating additional localized stresses. The original final heat treatment involved direct quenching from carburizing temperature (or a slightly lower temperature) followed by three low-temperature tempers at ~200°C (see Fig.5). This was designed for stress relief and dimensional stability but was insufficient for dealing with the hydrogen and retained austenite issues.
Optimized Carburizing & Hardening Practice:
1. Post-Quench Stabilization Hold: Immediately after the final quench, before any tempering, the gear shafts are held at 120-150°C for 6 hours. This stabilization allows the temperature to equalize throughout the massive cross-section of the gear shaft and permits the initial, most intense phase of the martensitic transformation to complete in a more controlled manner, reducing thermal gradients and associated stresses.
2. Modified Tempering Cycle: The tempering strategy was completely overhauled.
* Increased Temper Count and Temperature: Instead of three low tempers, the cycle now includes two high-temperature tempers (first at 300°C, then at 250°C) followed by two low-temperature stress-relief tempers. The higher temperature dramatically increases the driving force for hydrogen diffusion (\(D_H\) is much higher at 300°C than at 200°C).
* Extended Total Tempering Time: The cumulative holding time across all tempers was increased to over 110 hours. This prolonged exposure at elevated temperatures serves a dual purpose:
a) Hydrogen Removal: It provides an extended “baking” period to drive out the hydrogen absorbed during carburizing. The effective diffusion distance for hydrogen at these temperatures, over this duration, is sufficient to remove it from the case-hardened layer.
b) Retained Austenite Reduction: Tempering in the 250-300°C range promotes the decomposition of retained austenite into more stable ferrite and carbides. The transformation follows kinetics that benefit from extended time. The reduction in retained austenite content is directly observable in microstructure analysis, showing a significant decrease compared to the old工艺.
The efficacy of these changes can be modeled by considering the combined effect on the two key variables. The hydrogen concentration after final treatment \([H]_f\) is a function of initial content, uptake during carburizing, and removal during tempering:
$$ [H]_f = [H]_0 + \Delta[H]_{carb} – \int_{0}^{t_{temp}} k \cdot D_H(T_{temp}) \cdot [H](t) \, dt $$
The optimized cycle minimizes \( \Delta[H]_{carb} \) (through process control) and maximizes the integral (removal) via higher \( T_{temp} \) and longer \( t_{temp} \). Simultaneously, the volume fraction of retained austenite \( V_{RA} \) is reduced:
$$ V_{RA}^{final} = V_{RA}^{as-quenched} \cdot \exp(-K \cdot t_{temp}^n) $$
Where \( K \) is a rate constant strongly dependent on tempering temperature, and \( n \) is a time exponent. The higher tempering temperatures and extended times drive \( V_{RA}^{final} \) towards zero.
| Process Step | Original Parameters | Optimized Parameters | Intended Effect |
|---|---|---|---|
| Post-Quench Hold | None | 6 h at 120-150°C | Temperature/stress homogenization before temper. |
| Primary Tempering | 3 x ~200°C | 1 x 300°C + 1 x 250°C (long holds) + 2 x ~200°C |
High-temp for major H removal & RA reduction. Low-temp for final stress relief. |
| Total Tempering Time | ~60-70 h | >110 h | Maximizes integrated effect of H diffusion and RA transformation. |
IV. Conclusion and Integrated Effect
The prevention of flakes in large-section 17CrNiMo6 gear shaft forgings is not achievable through a single process adjustment but requires a holistic, multi-stage strategy targeting the root causes throughout the manufacturing chain. This experimental investigation systematically optimized five critical工艺 stages:
- Melting/Refining: Extended VD time and adjusted chemistry (higher Si/Al, lower Nb) to reduce initial hydrogen and create a matrix with benign hydrogen traps, lowering intrinsic flake sensitivity for the gear shaft material.
- Forging & PFHT: Increased normalizing temperature and, most importantly, drastically extended high-temperature tempering time (to 100 h) to exploit the peak hydrogen diffusivity, effectively removing the bulk of hydrogen inherited from melting before any subsequent processing.
- Carburizing & Final Hardening: Introduced a stabilization hold and a revised, prolonged tempering cycle featuring higher-temperature steps. This addresses the hydrogen recharged during carburizing and actively decomposes harmful retained austenite, thereby minimizing both the hydrogen concentration and the transformational stresses in the finished gear shaft.
The synergy of these optimizations can be expressed as a cumulative reduction in flake susceptibility factor \( S_f \):
$$ \Delta S_{f(total)} = \Delta S_{f(melt)} + \Delta S_{f(PFHT)} + \Delta S_{f(final)} < 0 $$
Each stage contributes a negative increment, progressively driving the total risk towards zero. Practice has conclusively proven that these integrated optimizations are highly effective. The incidence of flake-related scrap in large-section gear shaft forgings has been reduced to negligible levels, confirming that a scientific, process-based approach is fundamental to mastering the quality and reliability of these vital heavy industrial components. The principles established here—aggressive dehydrogenation at every possible stage, control of stress-inducing phases, and management of thermal gradients—are broadly applicable to the manufacture of other high-integrity, heavy-section alloy steel forgings.