
As an engineer specializing in mechanical transmissions, I have devoted considerable effort to the study of worm gears. Worm gears are a unique type of gearing used to transmit motion and power between two non‑intersecting, perpendicular shafts. They are widely applied in machinery, instruments, and heavy equipment due to their high reduction ratio, compactness, and smooth operation. In this article, I will thoroughly analyze the characteristics, types, efficiency, lubrication, thermal balance, installation, and maintenance of worm gears, supported by tables and formulas to provide a complete reference for practitioners.
1. Characteristics of Worm Gears
Compared with conventional gear drives, worm gears exhibit several distinct features that make them suitable for specific applications. I will summarize these characteristics in the table below.
| Feature | Description | Remarks |
|---|---|---|
| Large transmission ratio | Typically 10–80 in power transmission; up to 1000 for motion transmission. | Compact design compared to multi‑stage gear sets. |
| Low noise and vibration | Continuous line contact between worm and worm wheel yields smooth meshing. | Ideal for applications requiring quiet operation. |
| Self‑locking capability | Possible when the lead angle is less than the equivalent friction angle. | Useful in hoists and lifting mechanisms; prevents back‑driving. |
| Low efficiency | Typical efficiency 0.7–0.8; self‑locking types below 0.5. | High sliding friction generates heat; suited for moderate power. |
| Higher cost | Worm wheels often made of bronze to reduce friction and wear. | Worm is usually steel; material combination increases cost. |
From my perspective, understanding these characteristics is essential for selecting worm gears in design. The self‑locking property, for instance, is a double‑edged sword: it ensures safety in hoisting but drastically reduces efficiency.
2. Types and Structure of Worm Gears
2.1 Types of Worm Gears
Worm gears can be classified based on worm geometry. I regularly encounter three main types: cylindrical worm gears, hourglass (enveloping) worm gears, and cone (conical) worm gears. The following table provides a comparative overview.
| Type | Sub‑types / Description | Advantages | Disadvantages |
|---|---|---|---|
| Cylindrical (普通圆柱蜗杆) | Archimedes (ZA), Involute (ZI), Normal Straight‑sided (ZN); Arc‑tooth (ZC) versions exist. | Widely used; easy to manufacture; arc‑tooth type has higher load capacity (50–100% more) and efficiency >90%. | Higher sensitivity to center distance errors in arc type. |
| Hourglass (环面蜗杆) | Both worm and wheel have concave profiles; multiple teeth in mesh simultaneously. | Very high load capacity (2–4 times that of Archimedes); efficiency 85–90%; good oil film formation. | Requires high manufacturing and installation precision. |
| Cone (锥蜗杆) | Teeth on conical surfaces; also called conical worm and wheel. | High load capacity, large speed ratio range (10–360), good efficiency, compact. | Asymmetric; forward/reverse performance differs. |
Among these, cylindrical worm gears dominate in industry. I will focus on the Archimedes type for most of the analysis, as it is the most fundamental.
2.2 Structure of Worm Gears
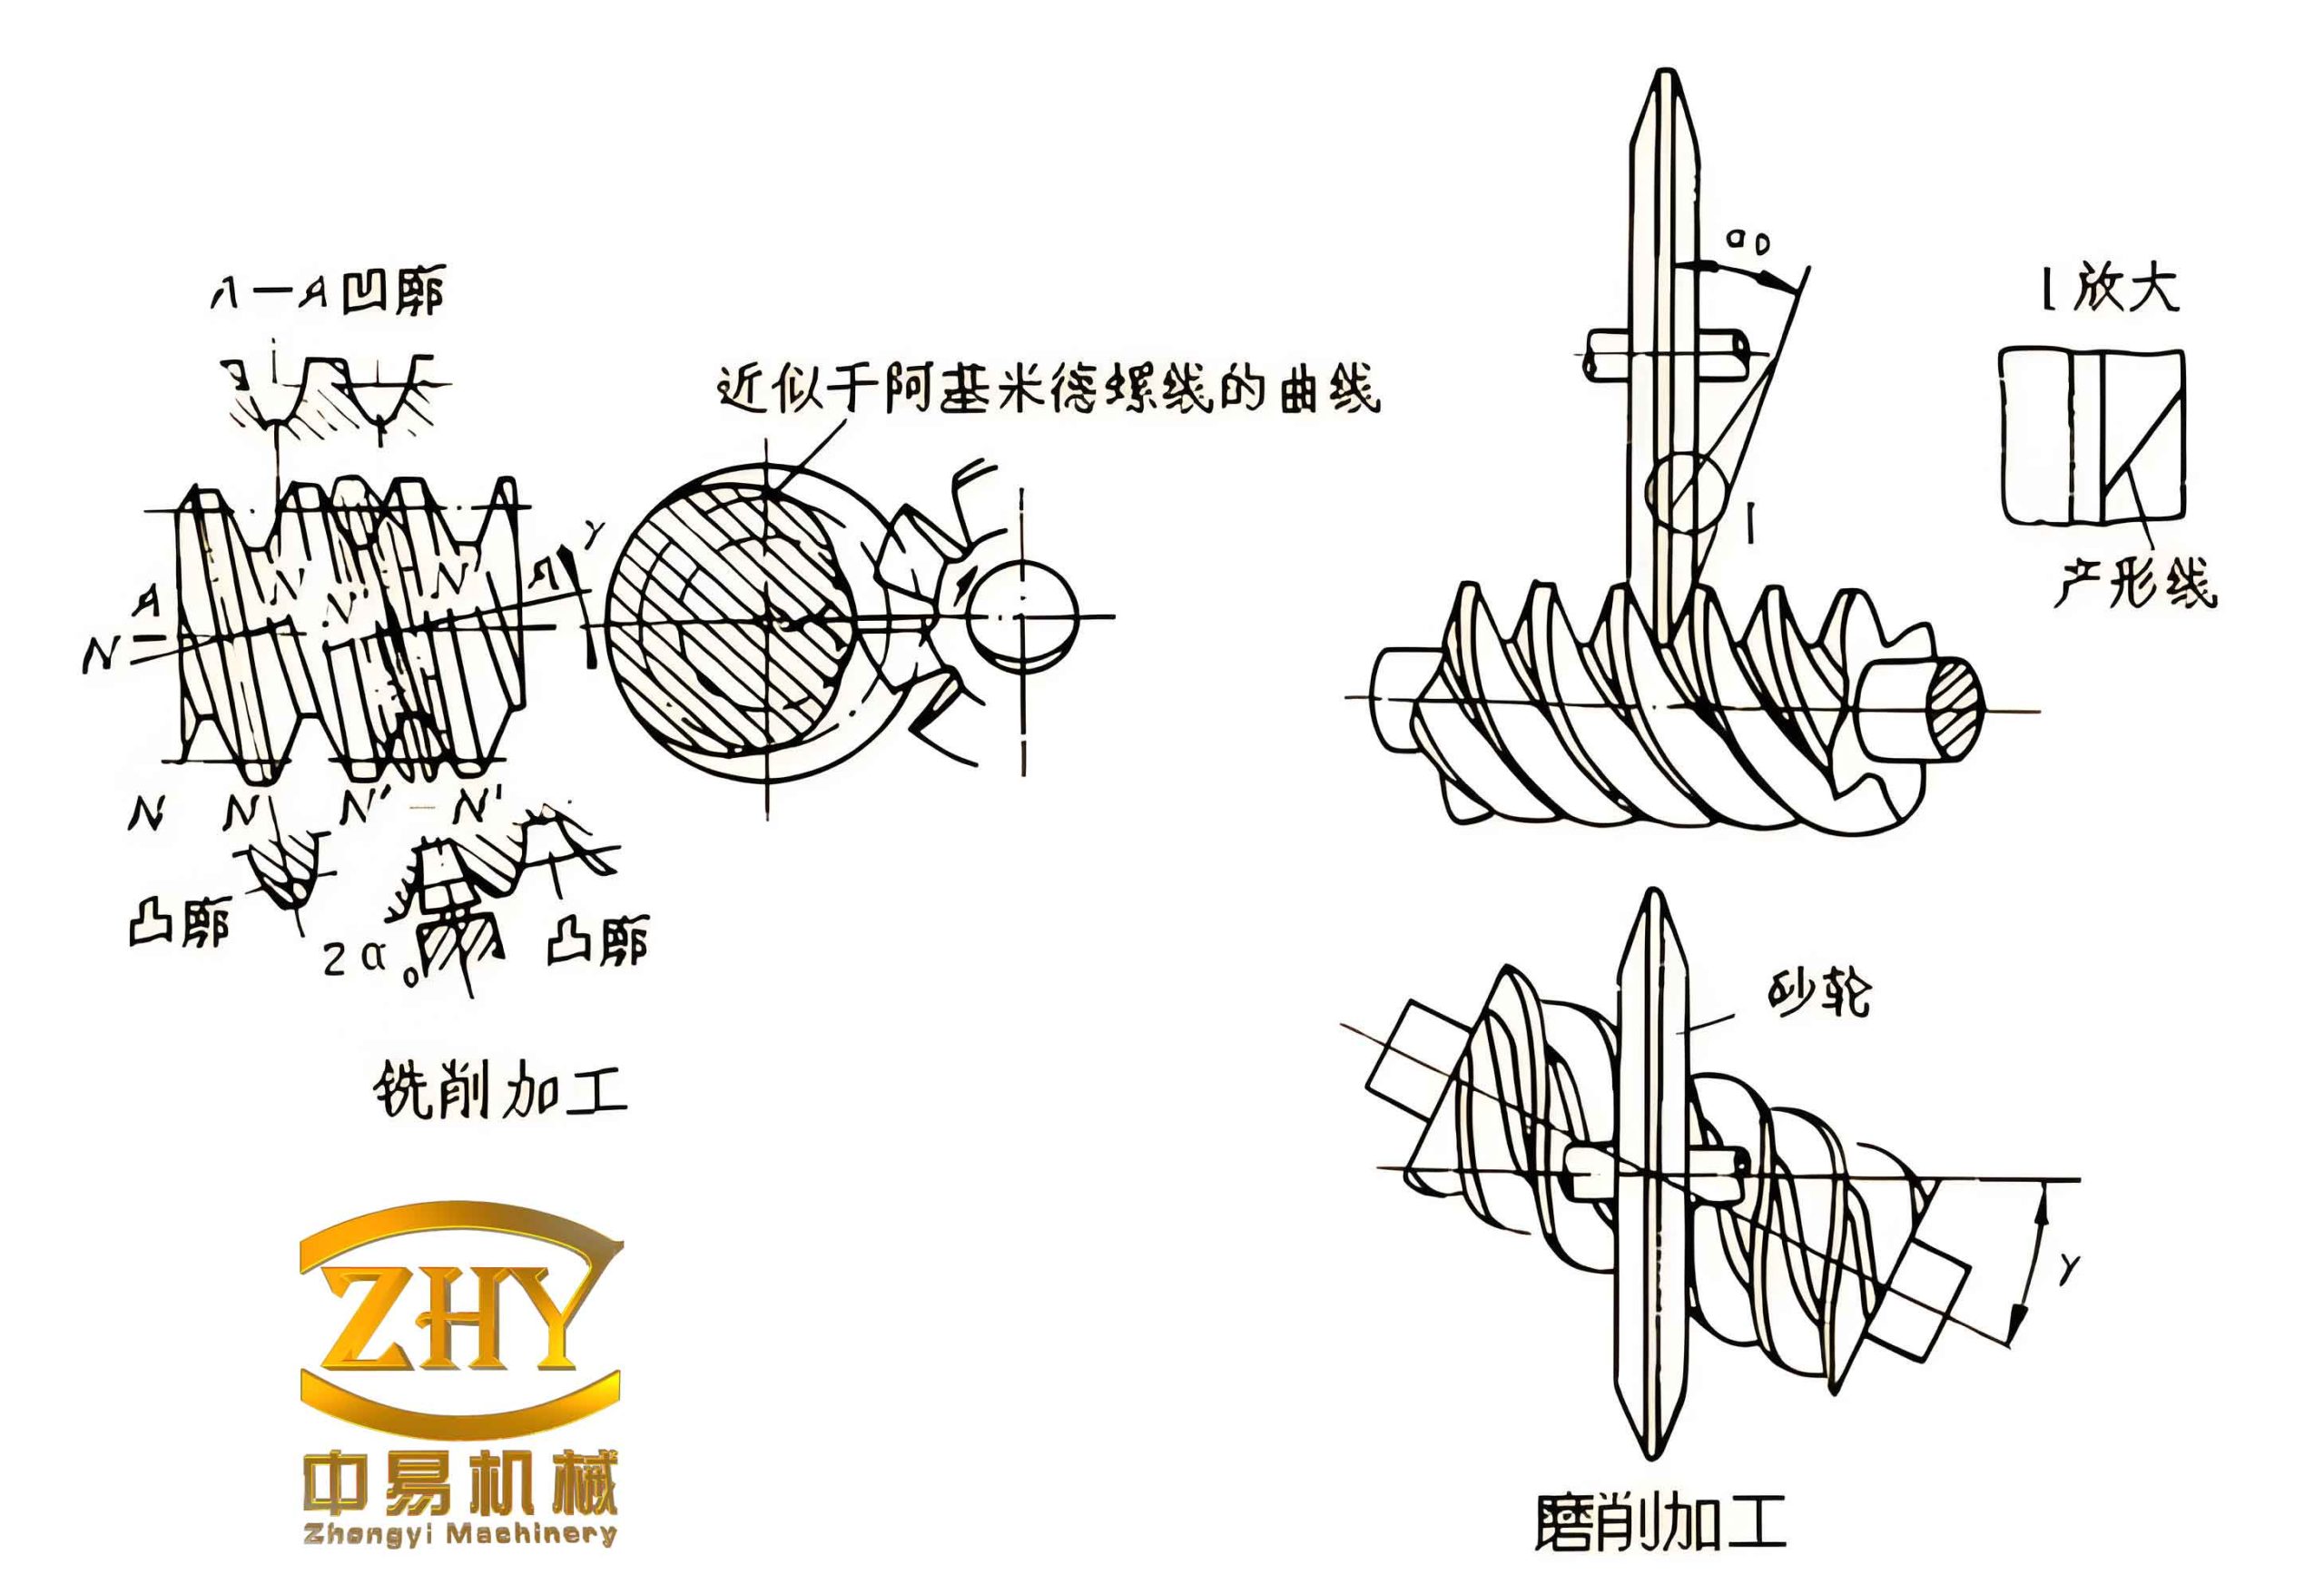
The worm is generally manufactured integrally with the shaft, forming a worm shaft. It can be cut by turning or milling, and is usually made of carbon steel or alloy steel followed by heat treatment. The worm wheel may be a one‑piece casting (for small diameters or cast iron) or a composite structure (bronze ring on a cast iron/steel hub) to save precious material. Common joining methods include interference fit, bolting, or casting the bronze onto the hub.
Note: The above figure illustrates a typical worm gear set used in industrial applications.
3. Efficiency of Worm Gears
Efficiency is a critical parameter for worm gears. The total power loss consists of three components: meshing loss, bearing loss, and oil churning loss. Therefore, total efficiency is given by
$$ \eta = \eta_1 \eta_2 \eta_3 $$
where:
- $\eta_1$ – meshing efficiency (dominant term)
- $\eta_2$ – bearing efficiency (usually 0.95–0.96)
- $\eta_3$ – oil churning efficiency (included in the product)
For a worm driving, the meshing efficiency can be approximated by the formula for a screw thread:
$$ \eta_1 = \frac{\tan\lambda}{\tan(\lambda + \rho_v)} $$
where:
- $\lambda$ – lead angle of the worm
- $\rho_v$ – equivalent friction angle, $\rho_v = \arctan f_v$
The equivalent friction coefficient $f_v$ decreases as the sliding velocity $v_s$ increases, because a thicker oil film forms. Typically, $\rho_v$ is obtained from empirical charts based on $v_s$.
From my experience, the lead angle $\lambda$ strongly influences $\eta_1$. For small $\lambda$, efficiency is low, and self‑locking occurs when $\lambda \le \rho_v$. Increasing $\lambda$ raises efficiency, but after about 27° the gain is marginal, and manufacturing becomes difficult. Therefore, most power‑transmitting worm gears have $\lambda \le 27°$, and multi‑start worms (with larger $\lambda$) are preferred for higher efficiency.
The following table provides estimated total efficiency values for preliminary design, based on the number of worm starts $z_1$.
| Transmission type | Number of worm starts $z_1$ | Total efficiency $\eta$ |
|---|---|---|
| Closed (enclosed) | 1 | 0.70 – 0.75 |
| 2 | 0.75 – 0.82 | |
| 4 | 0.82 – 0.92 | |
| Open (exposed) | 1, 2 | 0.60 – 0.70 |
4. Lubrication of Worm Gears
Due to the high sliding velocity in worm gears, effective lubrication is paramount to reduce wear and prevent scoring. I always recommend using high‑viscosity lubricants to enhance the oil film strength and anti‑scoring properties. The choice of lubrication method depends primarily on the sliding speed $v_s$ and the load type.
For enclosed worm drives, two common methods are:
- Oil bath lubrication: Used when the worm is located below the wheel (Figure 1a of the original reference). The immersion depth should be approximately one tooth height of the worm, but not exceeding the lowest rolling element center of the worm bearings. When $v_s > 5$ m/s, oil churning losses become excessive, so the worm should be placed above the wheel (Figure 1c).
- Pressure spray lubrication: Employed for high‑speed applications; oil is injected directly into the mesh.
For open drives, high‑viscosity gear oil or grease is applied periodically.
I have summarized typical lubrication guidelines in the table below.
| Sliding velocity $v_s$ (m/s) | Lubrication method | Oil viscosity (ISO VG) at 40°C |
|---|---|---|
| ≤ 2 | Oil bath (worm below) | 460 – 680 |
| 2 – 5 | Oil bath (worm below) or spray | 320 – 460 |
| 5 – 10 | Spray lubrication (worm above) | 220 – 320 |
| 10 – 15 | Spray lubrication with cooling | 150 – 220 |
| > 15 | Pressurized spray with oil cooler | 100 – 150 |
5. Thermal Balance Calculation
Because worm gears have inherently low efficiency, heat generation is significant. If the heat cannot be dissipated adequately, the oil temperature rises, reducing viscosity and leading to lubrication failure, scoring, or even seizure. Therefore, I always perform a thermal balance check to ensure the steady‑state oil temperature stays within an acceptable range (typically 70–90 °C).
The heat generated per unit time (in Watts) is:
$$ Q_1 = P_1 (1 – \eta) \times 1000 $$
where:
- $P_1$ – input power (kW)
- $\eta$ – total efficiency
The heat dissipated from the gearbox housing to the ambient air (in Watts) is:
$$ Q_2 = K_s A (t_1 – t_0) $$
where:
- $K_s$ – overall heat transfer coefficient (W/(m²·°C)), typically 10–17; use higher value for good ventilation
- $A$ – effective heat‑dissipating surface area of the housing (m²); include fins and flanges at 50% of their actual area
- $t_1$ – oil temperature (°C)
- $t_0$ – ambient temperature (°C), usually taken as 20 °C
At thermal equilibrium, $Q_1 = Q_2$, so the oil temperature is:
$$ t_1 = \frac{1000 (1 – \eta) P_1}{K_s A} + t_0 $$
This calculated $t_1$ must not exceed the allowable limit $[t_1] = 70$–90 °C. If it does, additional cooling measures are required, such as:
- Adding cooling fins to increase $A$.
- Mounting a fan on the worm shaft to increase $K_s$.
- Installing a cooling coil inside the oil sump (circulating water).
- Using a forced oil circulation system with an external cooler.
I have compiled a typical calculation example in the following table.
| Parameter | Symbol | Value | Unit |
|---|---|---|---|
| Input power | $P_1$ | 10 | kW |
| Total efficiency | $\eta$ | 0.75 | – |
| Heat generation | $Q_1$ | $10 \times (1-0.75) \times 1000 = 2500$ | W |
| Dissipation coefficient | $K_s$ | 15 | W/(m²·°C) |
| Effective area | $A$ | 1.5 | m² |
| Ambient temperature | $t_0$ | 20 | °C |
| Calculated oil temp | $t_1$ | $2500/(15 \times 1.5) + 20 = 131.1$ | °C |
In this example, $t_1$ exceeds 90 °C, so additional cooling (e.g., fan or coil) is mandatory.
6. Installation and Maintenance of Worm Gears
6.1 Installation
Proper installation is critical for the performance and life of worm gears. The most important requirement is that the intermediate plane of the worm wheel must coincide with the worm axis. This ensures correct meshing and uniform load distribution. Misalignment leads to premature wear and noise.
During installation, I follow these steps:
- Mount the worm shaft and bearings with precise alignment.
- Position the worm wheel so that its center plane passes through the worm axis. Adjust the axial position of the wheel using shims or adjustable spacer sleeves.
- After initial positioning, run the drive at low speed (50–100 rpm) for a break‑in period of 1–5 hours, gradually increasing load. Check contact pattern; if bronze smears appear on the worm, stop and remove it with fine sandpaper.
- After break‑in, clean the gearbox, replace the oil, and mark the relative axial positions of worm and wheel for future reference.
I often emphasize that for new machines, a no‑load run should precede the load test.
6.2 Maintenance
Because worm gears generate significant heat, continuous monitoring of oil temperature is essential. If the temperature exceeds the design limit, the drive must be stopped or cooling improved. Regular inspection of tooth surfaces (especially the worm wheel) for pitting, wear, or scoring is mandatory.
Lubrication quality degrades over time. I recommend changing the oil every 2000–4000 operating hours, using the same brand and grade. Never mix different brands or viscosities. The oil level should be checked periodically, and the breather vents cleaned to prevent pressure buildup.
By adhering to these installation and maintenance practices, the service life of worm gears can be significantly extended.
7. Conclusion
Through this comprehensive analysis, I have demonstrated that worm gears are a versatile and indispensable component in mechanical systems. Their unique combination of high reduction ratio, compactness, smooth operation, and self‑locking capability makes them ideal for many applications, despite the drawbacks of lower efficiency and higher cost. Mastery of the topics covered – types, efficiency, lubrication, thermal balance, and installation – is essential for any engineer working with worm gears. I hope the tables and formulas provided here serve as a practical reference for both design and troubleshooting.