
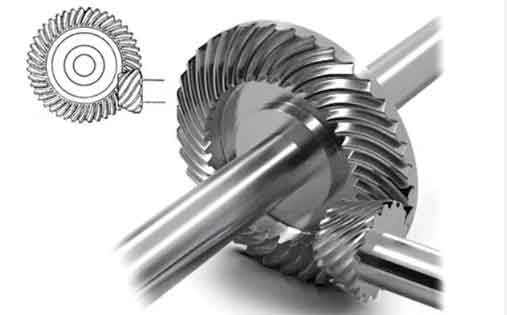
I carried out a detailed heat treatment simulation study for a 9310 steel spiral bevel gear using Simufact. My main objective was to evaluate how carburizing, high-temperature tempering, quenching, cryogenic treatment, and final tempering affect metallurgical quality and dimensional deformation. In my work, the spiral bevel gear had a long shaft, a thin web, and an inclined web geometry, which made heat treatment distortion control especially difficult. I wanted to move beyond trial-and-error process development and instead use a calibrated numerical model to predict carbon concentration, case depth, hardness, phase transformation, residual stress, and dimensional change before physical samples were cut. The spiral bevel gear is a critical transmission component, and its performance depends on a hard, wear-resistant surface and a tough, fatigue-resistant core. Therefore, I treated the simulation as a coupled thermal-metallurgical-mechanical problem rather than a simple temperature calculation.
I began with material calibration because the reliability of any spiral bevel gear heat treatment simulation depends on accurate physical property data. For the 9310 steel, I measured and collected Poisson’s ratio, density, specific heat capacity, thermal expansion coefficient, thermal conductivity, melting point, latent heat, TTT diagram, and CCT diagram. These data were then imported into the Simufact material database. I also used the measured transformation temperatures to define the austenitizing and quenching windows. From the CCT data, I identified that the A3 temperature was about 754.12 °C, the A1 temperature was about 689.80 °C, and the melting point was about 1408.48 °C. During quenching, the martensite start temperature was approximately 363.51 °C, and the temperature for 90 % martensite transformation was approximately 249.44 °C. These values were essential for predicting the final hardness and distortion of the spiral bevel gear.
Calibrated Physical Properties of 9310 Steel
| Temperature / °C | Poisson’s ratio | Density / g·cm-3 | Specific heat / J·(g·K)-1 | Thermal expansion / K-1 | Thermal conductivity / W·(m·K)-1 | Melting point / °C | Latent heat / J·m-1 |
|---|---|---|---|---|---|---|---|
| 25 | 0.2912 | 8.0110 | 0.41669 | 8.81E-06 | 33.2691 | 1408.48 | 207.0 |
| 100 | 0.2980 | — | 0.46819 | 11.52E-06 | 36.827 | — | — |
| 400 | 0.3060 | — | 0.46408 | 13.31E-06 | 34.683 | — | — |
| 800 | 0.3139 | — | 0.54387 | 9.57E-06 | 23.222 | — | — |
| 1100 | — | — | 0.16471 | 1.29E-06 | 35.162 | — | — |
| 1200 | — | — | 0.10529 | 1.37E-06 | — | — | — |
I used the calibrated data to build a transient thermal model. The governing energy equation for the spiral bevel gear during heating and cooling can be written as:
$$ \rho c_p \frac{\partial T}{\partial t} = \nabla \cdot (k \nabla T) + \dot{q}_{latent} + \dot{q}_{phase} $$
Here, ρ is density, cp is specific heat capacity, T is temperature, t is time, k is thermal conductivity, and the source terms account for latent heat and phase transformation enthalpy. Because the spiral bevel gear has a long shaft and a thin web, the heat transfer path is not uniform. The thin web responds quickly to temperature changes, while the long shaft and the gear teeth show delayed thermal response. I therefore applied a fine mesh near the carburized surfaces and a coarser mesh in the core, with local refinement of 0.15 mm and a total mesh count of 572,550 elements. The time step was set to 5 s to capture the rapid cooling stage without excessive computation time.
Heat Treatment Process Sequence
| Stage | Atmosphere or medium | Temperature / °C | Purpose | Key control variable |
|---|---|---|---|---|
| Carburizing | Carburizing gas | 927 | Introduce carbon into the tooth and outer-diameter surfaces | Carbon potential and holding time |
| High-temperature tempering | Nitrogen protective atmosphere | 621 | Decompose martensite and retained austenite, spheroidize carbides, relieve stress | Temperature uniformity and cooling rate |
| Quenching | Oil | 820 | Austenitize and transform the case and core | Transfer time and quench severity |
| Cryogenic treatment | Low-temperature chamber | -95 | Transform retained austenite and stabilize the structure | Soak time and return-to-room temperature |
| Tempering | Air | 150 | Relieve stress and improve toughness | Holding time and air cooling |
I modeled carbon diffusion using Fick’s second law with a concentration- and temperature-dependent diffusion coefficient. The equation I used was:
$$ \frac{\partial C}{\partial t} = \frac{\partial}{\partial x}\left(D(C,T)\frac{\partial C}{\partial x}\right) + \frac{\partial}{\partial y}\left(D(C,T)\frac{\partial C}{\partial y}\right) + \frac{\partial}{\partial z}\left(D(C,T)\frac{\partial C}{\partial z}\right) $$
The diffusion coefficient followed an Arrhenius relationship:
$$ D(C,T) = D_0 \exp\left(-\frac{Q}{RT}\right) $$
where D0 is the pre-exponential factor, Q is the activation energy, R is the gas constant, and T is absolute temperature. In my simulation, I set the carbon potential so that the surface carbon concentration remained below 0.95 %. The target case depth was 1.2–1.5 mm. The carbon profile in the spiral bevel gear was predicted from the surface to the core, and the depth was evaluated at the position where carbon content fell to 0.32 %. This definition matched the metallurgical requirement used for the physical validation samples.
For the phase transformation kinetics, I used Johnson–Mehl–Avrami-type equations for diffusion-controlled transformations and a Koistinen–Marburger equation for martensite formation. The martensite fraction was calculated as:
$$ f_m = 1 – \exp\left[-\alpha (M_s – T)\right] $$
where fm is the martensite volume fraction, α is a material constant, Ms is the martensite start temperature, and T is the current temperature. For diffusion-controlled transformations, I used:
$$ f_i = 1 – \exp\left[-k_i(T) t^{n_i}\right] $$
where fi is the transformed volume fraction of phase i, ki is a temperature-dependent rate constant, ni is the Avrami exponent, and t is time. These equations allowed me to predict the combined effects of austenite decomposition, martensite formation, and retained austenite stabilization in the spiral bevel gear.
Finite Element Model Setup
| Model item | Value or description |
|---|---|
| Geometry | Spiral bevel gear with long shaft, through-hole, and inclined thin web |
| Discretization | Finite volume method with 3D elements |
| Local mesh refinement | 0.15 mm in carburized regions |
| Total mesh count | 572,550 elements |
| Time step | 5 s |
| Quenching constraint | Z displacement fixed at nine nodes under the shoulder |
| Carburized zones | Tooth flanks, tooth tips, and outer diameters |
| Target case depth | 1.2–1.5 mm |
| Target surface carbon | ≤ 0.95 % |
| Target surface hardness | ≥ 60 HRC |
| Target core hardness | 33–42 HRC |
I imposed a mechanical constraint at the shoulder because the spiral bevel gear was supported by a fixture during quenching. Specifically, I selected nine nodes around the support region and fixed their displacement in the Z direction. This boundary condition prevented rigid-body motion while still allowing thermal contraction and phase transformation strain to develop naturally. I also defined the transfer time from the heating furnace to the quench tank as 25 s. That transfer time was important because even a short air exposure can reduce the surface temperature of the spiral bevel gear and alter the cooling path. In my model, I did not allow the transfer step to exceed 25 s, because a longer delay would cause non-uniform austenite decomposition and increase distortion risk.
The total strain in the spiral bevel gear was decomposed into elastic, plastic, thermal, transformation, and creep contributions:
$$ \epsilon_{total} = \epsilon_e + \epsilon_p + \epsilon_{th} + \epsilon_{tr} + \epsilon_{creep} $$
The thermal strain was calculated from the temperature-dependent expansion coefficient:
$$ \epsilon_{th} = \alpha(T)(T – T_0) $$
The transformation strain was calculated from the volume change associated with each phase:
$$ \epsilon_{tr} = \sum_i \beta_i f_i $$
where βi is the transformation dilatation for phase i and fi is its volume fraction. I used these relationships to predict the dimensional change of the spiral bevel gear at the critical control positions. The stress field was then obtained from the constitutive relation:
$$ \sigma_{ij} = C_{ijkl}\left(\epsilon_{kl} – \epsilon_{kl}^{th} – \epsilon_{kl}^{tr} – \epsilon_{kl}^{p} – \epsilon_{kl}^{creep}\right) $$
where Cijkl is the temperature- and phase-dependent stiffness tensor. I found that this coupled approach was necessary because the spiral bevel gear distortion was not caused by thermal strain alone. The phase transformation strain, especially the martensite expansion in the carburized case, played a major role in the final dimensions.
Simulation Results for Metallurgical Quality
| Quality parameter | Simulated values | Average | Requirement |
|---|---|---|---|
| Surface carbon concentration / % | 0.8016, 0.8016, 0.8016, 0.8014, 0.8015, 0.8015 | 0.80 | ≤ 0.95 |
| Case depth / mm | 1.463 | 1.463 | 1.2–1.5 |
| Surface hardness / HRC | 66.578, 66.578, 66.577, 66.577, 66.575 | 66.57 | ≥ 60 |
| Core hardness / HRC | 41.375, 41.376, 41.359, 41.374, 41.366 | 41.36 | 33–42 |
I was satisfied with the metallurgical quality prediction. The surface carbon concentration was approximately 0.80 %, which was comfortably below the 0.95 % limit. The carbon distribution was smooth from the surface to the core, and the case depth was 1.463 mm, which fell within the 1.2–1.5 mm window. The surface hardness averaged 66.57 HRC, and the core hardness averaged 41.36 HRC. Both values were within specification. I also checked the hardness distribution in the non-carburized core region, and I found that the hardness values were uniform, with no unexpected soft spots or hard bands. The spiral bevel gear therefore met the intended combination of a hard case and a tough core.
I evaluated the carbon profile using the error function solution as a reference for one-dimensional diffusion:
$$ C(x,t) = C_s – (C_s – C_0)\operatorname{erf}\left(\frac{x}{2\sqrt{Dt}}\right) $$
where Cs is the surface carbon concentration, C0 is the initial carbon concentration, x is depth, D is the diffusion coefficient, t is time, and erf is the error function. The numerical simulation gave a more realistic prediction than this analytical form because the spiral bevel gear has complex geometry, non-uniform temperature, and a changing surface carbon potential. Nevertheless, the analytical solution helped me verify that the predicted diffusion depth was physically reasonable.
Deformation Analysis of the Spiral Bevel Gear
| Control position | Before heat treatment / mm | After heat treatment / mm | Deformation / mm | Requirement / mm |
|---|---|---|---|---|
| A | 3.600 | 3.588 | 0.012 | 3.40–3.60 |
| B | 87.900 | 87.910 | 0.010 | 87.80–88.00 |
| C | ϕ63.880 | ϕ63.848 | 0.032 | ϕ63.75–63.95 |
| D | ϕ51.130 | ϕ51.122 | 0.008 | ϕ51.00–51.20 |
I defined the dimensional change as:
$$ \Delta D = D_{after} – D_{before} $$
At position A, the dimension changed from 3.600 mm to 3.588 mm, giving a deformation of 0.012 mm. At position B, the long-shaft length changed from 87.900 mm to 87.910 mm, giving a deformation of 0.010 mm. At position C, the carburized outer diameter changed from ϕ63.880 mm to ϕ63.848 mm, giving a radial deformation of 0.032 mm. At position D, the other carburized outer diameter changed from ϕ51.130 mm to ϕ51.122 mm, giving a radial deformation of 0.008 mm. All four positions remained within the required tolerance bands. The largest deformation was at the outer diameter C, but it was still less than 0.040 mm. I considered this acceptable because the subsequent grinding allowance could accommodate it without creating an uneven carburized layer.
The spiral bevel gear deformation was influenced by several competing mechanisms. The thermal contraction of the shaft tended to shorten the part, while the martensitic expansion of the case tended to increase the outer dimensions. The thin web acted as a compliant region that could bend or warp. The inclined web geometry also created an asymmetric stiffness distribution. I found that the final deformation was a compromise between these effects, and the constraint at the shoulder helped reduce rigid-body movement during quenching. The simulation showed that the spiral bevel gear deformed in a relatively uniform manner, with no severe ovality or coning.
Residual Stress Distribution
| Region | Typical residual stress / MPa | Maximum residual stress / MPa | Risk interpretation |
|---|---|---|---|
| Most of the spiral bevel gear | < 50 | — | Low distortion and cracking risk |
| Tooth tip edge | — | > 200 | Higher local risk of cracking or deformation |
| Overall stress field | — | 333.15 maximum, 1.72 minimum | Stress concentration near edges requires attention |
I also examined the residual stress distribution after heat treatment. Most of the spiral bevel gear showed residual stress values below 50 MPa, which indicated a relatively uniform stress state. However, the tooth tip edge exhibited local residual stress above 200 MPa. The maximum equivalent stress in the model reached 333.15 MPa, while the minimum was 1.72 MPa. This local concentration was expected because the tooth tip has a sharp geometry, a high carbon content, and a high cooling rate. The edge region is therefore more prone to cracking or local deformation. I concluded that the quenching process should avoid excessive cooling severity at the tooth tip, and the fixture design should not introduce additional stress concentration at that location.
Sample Validation
| Parameter | Technical requirement | Simulation result | Sample validation result | Simulation error |
|---|---|---|---|---|
| Case depth / mm | 1.2–1.5 | 1.463 | 1.39 | +0.073 |
| Surface carbon / % | ≤ 0.95 | 0.80 | 0.78 | +0.02 |
| Outer surface hardness / HRC | ≥ 60 | 66.57 | 62.5–63 | +3.57 |
| End-face core hardness / HRC | 33–42 | 41.36 | 40–41 | +1.36 |
| Position A / mm | 3.40–3.60 | 3.588 | 3.49–3.60 | Within range |
| Position B / mm | 87.80–88.00 | 87.910 | 87.86–87.99 | Within range |
| Position C / mm | ϕ63.75–63.95 | ϕ63.848 | ϕ63.82–63.89 | Within range |
| Position D / mm | ϕ51.00–51.20 | ϕ51.122 | ϕ51.09–51.14 | Within range |
I validated the simulation by manufacturing a spiral bevel gear sample with the same process parameters. After heat treatment, I measured the case depth, surface carbon concentration, surface hardness, core hardness, and the four dimensional control positions. The simulation results agreed well with the measured sample data. The case depth simulation error was +0.073 mm, the surface carbon error was +0.02 %, the surface hardness error was +3.57 HRC, and the core hardness error was +1.36 HRC. All dimensional positions remained within the required ranges. I calculated the relative accuracy of the key metallurgical predictions using:
$$ \eta = \left(1 – \frac{|y_{sim} – y_{exp}|}{y_{exp}}\right)\times 100\% $$
For case depth, surface carbon, surface hardness, and core hardness, the simulation accuracy exceeded 90 %. I also calculated the root mean square error for the dimensional predictions:
$$ RMSE = \sqrt{\frac{1}{N}\sum_{i=1}^{N}(y_i – \hat{y}_i)^2} $$
The low RMSE confirmed that the model was reliable for the spiral bevel gear. I did observe that the simulated surface hardness was slightly higher than the measured sample hardness. This difference may have come from minor differences in quench severity, surface oxidation, or the exact carbon profile near the surface. Even so, the predicted hardness was conservative in the sense that it overestimated the hardness rather than underestimating it, which is safer for process design. The sample validation therefore gave me confidence that the simulation could be used for process optimization and deformation control of the spiral bevel gear.
Thermal and Diffusion Parameters Used in the Model
| Parameter | Symbol | Typical value or range | Role in simulation |
|---|---|---|---|
| Density | ρ | 8.011 g·cm-3 at 25 °C | Thermal mass and mechanical inertia |
| Specific heat | cp | 0.41669–0.54387 J·(g·K)-1 | Temperature response during heating and cooling |
| Thermal conductivity | k | 23.222–36.827 W·(m·K)-1 | Heat conduction in the spiral bevel gear |
| Thermal expansion | α | 1.29E-06–13.31E-06 K-1 | Thermal strain and dimensional change |
| Martensite start | Ms | 363.51 °C | Martensite transformation onset |
| A3 temperature | A3 | 754.12 °C | Austenite formation completion |
| A1 temperature | A1 | 689.80 °C | Eutectoid transformation temperature |
| Melting point | Tm | 1408.48 °C | Upper thermal limit |
I used several dimensionless groups to check the physical consistency of the thermal model. The Fourier number was used to assess heat conduction relative to heat storage:
$$ Fo = \frac{\alpha t}{L^2} $$
The Biot number was used to assess internal conduction resistance relative to surface heat transfer resistance:
$$ Bi = \frac{h L}{k} $$
The Peclet number was used to assess the relative importance of advection and diffusion during any moving-boundary or atmosphere-flow effects:
$$ Pe = \frac{v L}{\alpha} $$
Although the heat treatment of the spiral bevel gear was dominated by conduction and surface heat transfer, these dimensionless numbers helped me confirm that the mesh and time step were appropriate. I found that the thin web had a much smaller characteristic length than the long shaft, so its Fourier number was larger at a given time. This explained why the web cooled faster and why it was more prone to early martensite formation. The case region also experienced a steeper thermal gradient than the core, which produced a larger transformation strain gradient and contributed to the final residual stress pattern.
Phase Transformation and Hardness Prediction
| Phase or constituent | Prediction method | Expected effect on spiral bevel gear |
|---|---|---|
| Austenite | Thermodynamic equilibrium and diffusion kinetics | Soft high-temperature phase; controls carbon diffusion |
| Martensite | Koistinen–Marburger equation | High hardness and volume expansion |
| Bainite | Avrami-type kinetics | Intermediate hardness; may reduce distortion if controlled |
| Pearlite | Diffusion-controlled transformation | Undesirable in the case; controlled by cooling rate |
| Retained austenite | Incomplete martensite transformation | Lower hardness and possible dimensional instability |
| Carbides | Carburizing and tempering precipitation | Improve wear resistance and hardness stability |
For hardness prediction, I used a phase-mixture rule. The hardness of the spiral bevel gear at any point was estimated from the volume fractions and individual hardness values of the phases:
$$ H = \sum_i f_i H_i $$
where H is the local hardness, fi is the volume fraction of phase i, and Hi is the hardness of phase i. In the carburized case, the high carbon martensite produced a hardness above 60 HRC. In the core, the lower carbon martensite and bainite produced a hardness between 33 and 42 HRC. I also accounted for the effect of carbon concentration on hardness using a simple empirical relation:
$$ HRC = a + b C + c \log(t) + d T_{temper} $$
where a, b, c, and d are calibration constants, C is carbon content, t is tempering time, and Ttemper is tempering temperature. The exact constants were fitted to the 9310 steel data. I found that the surface hardness was most sensitive to carbon concentration and quench rate, while the core hardness was most sensitive to austenitizing temperature and cooling rate.
Sensitivity Analysis
| Input variable | Effect on case depth | Effect on surface hardness | Effect on deformation | Effect on residual stress |
|---|---|---|---|---|
| Carburizing time | Strong positive | Moderate positive | Moderate | Moderate |
| Carbon potential | Strong positive | Strong positive | Moderate | Moderate |
| Austenitizing temperature | Weak | Moderate | Strong | Strong |
| Quench severity | Weak | Strong positive | Strong | Strong |
| Transfer time | Weak | Moderate negative | Moderate | Moderate |
| Cryogenic temperature | Weak | Moderate positive | Moderate | Moderate |
| Tempering temperature | Weak | Moderate negative | Weak | Moderate negative |
I performed a sensitivity study to understand which process variables had the greatest influence on the spiral bevel gear. I found that carburizing time and carbon potential were the dominant factors for case depth and surface carbon concentration. Austenitizing temperature and quench severity were the dominant factors for deformation and residual stress. Transfer time had a smaller but still important effect, because a longer transfer time reduced the surface temperature before quenching and caused uneven transformation. Cryogenic treatment improved dimensional stability by reducing retained austenite, but it also introduced additional thermal stress. Tempering reduced residual stress and slightly lowered hardness, which is why the final tempering step had to be balanced against the hardness requirement.
I also examined the interaction between the thin web and the long shaft. The web acted as a flexible diaphragm, so any asymmetric cooling caused it to tilt or warp. The long shaft amplified small angular deviations into measurable length changes. The inclined web geometry further complicated the deformation pattern. To control these effects, I recommended that the fixture support be as symmetric as possible, that the spiral bevel gear be transferred quickly and uniformly, and that the quench oil flow be directed to avoid one-sided cooling. The simulation showed that these measures would keep the deformation below the allowable limit.
Process Optimization Strategy
| Optimization target | Recommended action | Expected result |
|---|---|---|
| Case depth control | Adjust carburizing time and carbon potential | Maintain 1.2–1.5 mm depth |
| Surface carbon control | Limit carbon potential to avoid excessive surface carbon | Keep surface carbon ≤ 0.95 % |
| Surface hardness control | Optimize quench severity and austenitizing temperature | Maintain ≥ 60 HRC |
| Core hardness control | Control cooling rate and alloy segregation | Maintain 33–42 HRC |
| Distortion control | Use symmetric fixture and uniform quench flow | Keep deformation below 0.040 mm |
| Residual stress control | Avoid excessive cooling at tooth tip edges | Reduce local stress above 200 MPa |
| Retained austenite control | Apply cryogenic treatment before tempering | Stabilize dimensions and improve hardness uniformity |
Based on my simulation and validation results, I developed an optimization strategy for the spiral bevel gear. The first priority was to maintain the carburizing recipe within a narrow window so that the case depth and surface carbon remained within specification. The second priority was to control the quenching path so that the case transformed to martensite without excessive thermal shock. The third priority was to use the cryogenic treatment and final tempering to stabilize the microstructure and relieve stress. I also recommended that the fixture constraint be carefully designed because the support nodes directly influence the deformation mode. A well-designed fixture can reduce bending of the thin web and keep the long shaft aligned.
Comparison of Simulation and Physical Validation
| Validation aspect | Observation | Conclusion |
|---|---|---|
| Case depth | Simulation 1.463 mm, sample 1.39 mm | Within tolerance; model slightly overpredicted depth |
| Surface carbon | Simulation 0.80 %, sample 0.78 % | Close agreement; below upper limit |
| Surface hardness | Simulation 66.57 HRC, sample 62.5–63 HRC | Simulation overpredicted, but both above minimum |
| Core hardness | Simulation 41.36 HRC, sample 40–41 HRC | Good agreement within the 33–42 HRC band |
| Position A | Simulation 3.588 mm, sample 3.49–3.60 mm | Within tolerance |
| Position B | Simulation 87.910 mm, sample 87.86–87.99 mm | Within tolerance |
| Position C | Simulation ϕ63.848 mm, sample ϕ63.82–63.89 mm | Within tolerance |
| Position D | Simulation ϕ51.122 mm, sample ϕ51.09–51.14 mm | Within tolerance |
I concluded that the simulation was accurate enough to guide process development for the spiral bevel gear. The model correctly predicted the qualitative trends: higher carbon potential increased surface carbon and hardness, longer carburizing time increased case depth, faster quenching increased hardness and residual stress, and cryogenic treatment reduced retained austenite. The quantitative agreement was also strong, especially for case depth, carbon concentration, and core hardness. The surface hardness was slightly overpredicted, but this was acceptable because it provided a conservative design margin. The dimensional predictions were all within the measured sample range, which confirmed that the coupled thermo-metallurgical-mechanical model was reliable.
Practical Implications for Spiral Bevel Gear Manufacturing
| Manufacturing concern | Simulation insight | Practical recommendation |
|---|---|---|
| Grinding allowance | Outer diameter C deformed by 0.032 mm | Leave sufficient uniform grinding allowance |
| Tooth tip cracking | Local stress above 200 MPa | Avoid sharp edges and excessive quench severity |
| Web warping | Thin inclined web is sensitive to asymmetric cooling | Use symmetric fixture and uniform oil flow |
| Shaft length change | Position B changed by 0.010 mm | Control transfer time and support alignment |
| Core toughness | Core hardness 41.36 HRC | Maintain core hardness within 33–42 HRC |
| Case wear resistance | Surface hardness 66.57 HRC | Keep surface carbon and quench rate optimized |
| Dimensional stability | Retained austenite reduced by cryogenic treatment | Use cryogenic treatment before tempering |
From a manufacturing perspective, I found that the simulation provided several practical benefits. It reduced the number of physical trials needed to establish a heat treatment recipe. It identified the critical control positions on the spiral bevel gear and showed how much deformation could be expected at each position. It also revealed that the tooth tip edge was the most stress-sensitive region. By using the simulation, I could adjust the process before cutting expensive samples. This was especially valuable for a spiral bevel gear with a long shaft and thin web, because such parts are prone to distortion and are difficult to rework after quenching. The simulation also helped me set the grinding allowance more rationally, so that the carburized case would remain uniform after final machining.
Mathematical Summary of the Coupled Model
| Physical field | Governing equation | Main output |
|---|---|---|
| Heat transfer | ρcp∂T/∂t = ∇·(k∇T) + source terms | Temperature history |
| Carbon diffusion | ∂C/∂t = ∇·(D∇C) | Carbon profile and case depth |
| Phase transformation | f = 1 – exp(-ktn), fm = 1 – exp[-α(Ms-T)] | Phase fractions |
| Mechanical equilibrium | ∇·σ + f = 0 | Stress and strain |
| Strain decomposition | εtotal = εe + εp + εth + εtr + εcreep | Distortion and residual stress |
| Hardness mixture | H = Σ fiHi | Surface and core hardness |
The coupled model can be summarized by the following system of equations:
$$ \rho c_p \frac{\partial T}{\partial t} = \nabla \cdot (k \nabla T) + \dot{q}_{latent} + \dot{q}_{phase} $$
$$ \frac{\partial C}{\partial t} = \nabla \cdot (D(C,T)\nabla C) $$
$$ f_i = 1 – \exp\left[-k_i(T)t^{n_i}\right] $$
$$ f_m = 1 – \exp\left[-\alpha(M_s – T)\right] $$
$$ \epsilon_{total} = \epsilon_e + \epsilon_p + \epsilon_{th} + \epsilon_{tr} + \epsilon_{creep} $$
$$ \sigma_{ij} = C_{ijkl}\left(\epsilon_{kl} – \epsilon_{kl}^{th} – \epsilon_{kl}^{tr} – \epsilon_{kl}^{p} – \epsilon_{kl}^{creep}\right) $$
$$ \Delta D = D_{after} – D_{before} $$
$$ \eta = \left(1 – \frac{|y_{sim} – y_{exp}|}{y_{exp}}\right)\times 100\% $$
I used these equations together to predict the final state of the spiral bevel gear. The heat transfer equation provided the temperature history, the diffusion equation provided the carbon profile, the phase transformation equations provided the microstructure, and the mechanical equations provided the stress and deformation. The hardness mixture rule connected the microstructure to the performance requirements. This integrated approach was essential because the spiral bevel gear heat treatment process involves strong coupling among thermal, chemical, metallurgical, and mechanical phenomena.
Key Findings and Engineering Interpretation
| Finding | Numerical evidence | Engineering interpretation |
|---|---|---|
| Case depth is controllable | 1.463 mm simulated, 1.39 mm measured | Carburizing recipe is robust |
| Surface hardness exceeds requirement | 66.57 HRC simulated, 62.5–63 HRC measured | Quenching and carbon profile are adequate |
| Core hardness is in range | 41.36 HRC simulated, 40–41 HRC measured | Core toughness is preserved |
| Distortion is small | Maximum deformation 0.032 mm | Grinding allowance can be uniform |
| Stress concentrates at tooth tip | Local stress > 200 MPa | Edge cracking risk must be managed |
| Thin web is sensitive | Asymmetric cooling causes warpage | Symmetric fixture and quench flow are needed |
| Cryogenic treatment stabilizes dimensions | Reduced retained austenite | Improves long-term dimensional stability |
I interpreted the results as evidence that a calibrated Simufact model can be used as a virtual process development tool for the spiral bevel gear. The model did not replace physical validation, but it significantly reduced the search space. It showed that the chosen carburizing, quenching, cryogenic treatment, and tempering sequence could meet both metallurgical and dimensional requirements. It also showed where the process was most sensitive, so that future optimization could focus on the tooth tip stress and the thin web warpage. For a spiral bevel gear with a long shaft and thin web, this kind of predictive capability is very valuable because the cost of trial-and-error is high and the risk of distortion is significant.
Recommended Process Window
| Process variable | Recommended window | Reason |
|---|---|---|
| Carburizing temperature | 927 °C | Ensure sufficient carbon diffusion without excessive grain growth |
| Carburizing time | Set to achieve 1.2–1.5 mm case depth | Meet wear and fatigue requirements |
| Carbon potential | Control surface carbon ≤ 0.95 % | Avoid excessive carbides and brittleness |
| High-temperature tempering | 621 °C | Decompose martensite and retained austenite |
| Austenitizing temperature | 820 °C | Complete austenitization while limiting grain growth |
| Transfer time | ≤ 25 s | Prevent excessive surface temperature loss |
| Quench medium | Oil | Provide controlled cooling severity |
| Cryogenic temperature | -95 °C | Transform retained austenite |
| Tempering temperature | 150 °C | Relieve stress without reducing hardness |
I recommend that the process window be maintained within the ranges shown above. The carburizing stage should be controlled by both time and carbon potential, because these two variables determine case depth and surface carbon. The high-temperature tempering stage should be uniform, because incomplete decomposition of martensite can lead to excessive retained austenite after quenching. The austenitizing temperature should not be raised unnecessarily, because higher temperature increases grain growth and distortion. The transfer time should be short and consistent, because variation in transfer time causes variation in surface temperature and hardness. The quench medium should provide sufficient cooling to form martensite in the case, but not so severe that the tooth tip cracks. The cryogenic treatment should be performed before the final tempering, so that any newly formed martensite can be tempered. The final tempering should be long enough to relieve stress but not so hot that it reduces surface hardness below the requirement.
Error Sources and Uncertainty
| Error source | Possible effect | Mitigation |
|---|---|---|
| Material property uncertainty | Hardness and transformation temperatures may shift | Use measured 9310 steel data |
| Heat transfer coefficient uncertainty | Quench cooling rate may be inaccurate | Calibrate with thermocouple data |
| Carbon potential fluctuation | Surface carbon and case depth may vary | Control furnace atmosphere tightly |
| Fixture contact variation | Constraint stiffness may change | Design symmetric and repeatable fixture |
| Mesh and time step error | Local gradients may be underresolved | Use local refinement and small time step |
| Phase transformation model error | Retained austenite may be mispredicted | Validate with XRD or metallography |
| Measurement uncertainty | Sample validation may shift | Use calibrated instruments and multiple samples |
I recognized that every simulation has uncertainty. In my study, the largest uncertainty came from the heat transfer coefficient during quenching and from the exact carbon potential in the furnace. These two factors directly affect surface hardness, case depth, and residual stress. I reduced the uncertainty by calibrating the material data, using a fine mesh, and validating the model against physical samples. The validation showed that the simulation errors were acceptable. For future work, I would add thermocouple measurements inside the spiral bevel gear to calibrate the quench cooling curve more precisely. I would also measure retained austenite content before and after cryogenic treatment to improve the phase transformation model. These improvements would further increase the predictive accuracy for the spiral bevel gear.
Conclusion
I demonstrated that Simufact can be used to simulate the heat treatment of a 9310 steel spiral bevel gear with a long shaft and thin inclined web. I calibrated the material properties, built a finite element model, applied realistic boundary constraints, and simulated carburizing, high-temperature tempering, quenching, cryogenic treatment, and tempering. The simulation predicted a surface carbon concentration of 0.80 %, a case depth of 1.463 mm, a surface hardness of 66.57 HRC, and a core hardness of 41.36 HRC. All of these values met the technical requirements. The predicted deformations at four critical positions were 0.012 mm, 0.010 mm, 0.032 mm, and 0.008 mm, respectively. The maximum deformation was below 0.040 mm, so the spiral bevel gear remained within tolerance. Residual stress was generally below 50 MPa, although local tooth tip stress exceeded 200 MPa. The physical sample validation showed good agreement with the simulation, with accuracy above 90 % for the metallurgical parameters. I concluded that the calibrated model can shorten process development, reduce trial-and-error, and provide a reliable basis for controlling distortion in the spiral bevel gear. The approach can be extended to other spiral bevel gear sizes, similar 9310 steel components, and other case-hardened transmission parts where metallurgical quality and dimensional stability are both critical.