
In modern manufacturing and construction, gear milling plays a pivotal role in producing precision components for machinery, automotive systems, and industrial equipment. As a seasoned engineer with extensive experience in gear machining, I have witnessed firsthand how the selection of appropriate gear milling cutters can drastically impact productivity, quality, and cost-effectiveness. This article delves into the comparative analysis of various gear milling cutters, drawing parallels from applications in foundation engineering but focusing exclusively on gear milling processes. Gear milling involves the use of rotary cutters to remove material from a workpiece, forming gear teeth with high accuracy. The choice of cutter—whether standard, conical, or spherical—depends on factors such as material hardness, machining speed, precision requirements, and economic constraints. Through this first-person perspective, I aim to share insights on optimizing gear milling operations, supported by tables, formulas, and practical examples to guide professionals in the field.
Gear milling is a subtractive manufacturing process where a milling machine, equipped with specialized cutters, shapes gear teeth into metal or composite materials. The principle revolves around the interaction between the cutter’s teeth and the workpiece, with the cutter rotating at high speeds to chip away material. This process is essential for creating gears used in transmissions, engines, and other mechanical systems. Common types of gear milling machines include horizontal milling machines, vertical milling machines, and CNC-based systems, each offering unique advantages for different applications. For instance, CNC gear milling machines enable automated, high-precision operations, while manual machines provide flexibility for small batches. The core of gear milling lies in the cutters, which must be selected based on the material’s properties—similar to how milling teeth are chosen for rock excavation in diaphragm wall construction. In this context, gear milling requires careful consideration of cutter geometry, material composition, and machining parameters to achieve optimal results.
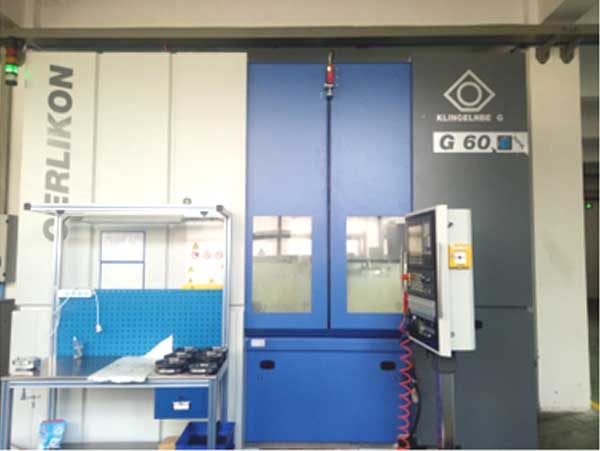
The efficiency of gear milling hinges on the cutter’s design. Standard gear milling cutters are typically used for soft to medium-hard materials, such as aluminum or mild steel, with tensile strengths up to 500 MPa. These cutters feature flat-tooth profiles that facilitate rapid material removal, making them ideal for high-speed machining where precision is secondary to productivity. Conical gear milling cutters, on the other hand, are engineered for harder materials like alloy steels or cast iron, with tensile strengths ranging from 500 to 1000 MPa. Their tapered design allows for deeper cuts and better heat dissipation, reducing tool wear in demanding gear milling applications. Spherical gear milling cutters are reserved for ultra-hard materials, such as hardened steel or titanium alloys, exceeding 1000 MPa in strength. With rounded tips, these cutters minimize stress concentrations and enhance durability, though at a higher cost. To quantify these differences, consider the material removal rate (MRR) formula in gear milling: $$MRR = f \times d \times v$$ where \( f \) is the feed rate (mm/tooth), \( d \) is the depth of cut (mm), and \( v \) is the cutting speed (m/min). This formula underscores how cutter selection influences machining efficiency—for example, spherical cutters may require lower feed rates to maintain tool life, affecting overall MRR.
In gear milling, the choice of cutter is not arbitrary; it depends on multiple factors that mirror those in construction milling. First, the material type—akin to geological conditions—dictates cutter suitability. Soft materials like plastics or non-ferrous metals allow for standard cutters, while hardened steels necessitate conical or spherical options. Second, machining progress, or productivity, is critical. Standard cutters in gear milling can achieve feed rates of 0.2–0.5 mm/tooth, enabling fast production for bulk orders. Conical cutters, used in medium-hard materials, might reduce feed rates to 0.1–0.3 mm/tooth to preserve accuracy, whereas spherical cutters in ultra-hard scenarios often operate at 0.05–0.1 mm/tooth, prioritizing tool longevity over speed. Third, precision, analogous to vertical control in excavation, is paramount in gear milling. Gear accuracy is measured by parameters like profile error and pitch deviation, which can be expressed as: $$ \Delta P = |P_{actual} – P_{nominal}| $$ where \( \Delta P \) is the pitch deviation (mm). Standard cutters may introduce errors up to 0.1 mm in soft materials, but conical and spherical cutters can reduce this to 0.05 mm or less in harder substrates due to their robust designs. Fourth, economic factors play a role; standard gear milling cutters cost around $50–$100 per unit, conical ones $150–$300, and spherical versions $500–$1000, influencing total project budgets. To illustrate, Table 1 summarizes these aspects for common gear milling scenarios.
| Cutter Type | Material Hardness (Tensile Strength, MPa) | Typical Feed Rate (mm/tooth) | Precision (Max Error, mm) | Cost per Unit (USD) | Recommended Gear Milling Applications |
|---|---|---|---|---|---|
| Standard Cutter | 0–500 | 0.2–0.5 | 0.1 | 50–100 | Soft metals, plastics, prototyping |
| Conical Cutter | 500–1000 | 0.1–0.3 | 0.05 | 150–300 | Alloy steels, industrial gears |
| Spherical Cutter | >1000 | 0.05–0.1 | 0.02 | 500–1000 | Hardened steels, aerospace components |
Beyond material and economic considerations, gear milling involves complex dynamics that affect cutter performance. The cutting force \( F_c \) in gear milling can be modeled using the formula: $$ F_c = K_c \times A_c $$ where \( K_c \) is the specific cutting force (N/mm²) and \( A_c \) is the cross-sectional area of cut (mm²). This force varies with cutter type; for instance, spherical cutters distribute force more evenly, reducing \( K_c \) by 10–20% compared to standard cutters in hard materials. Additionally, tool life in gear milling is a critical metric, often estimated via Taylor’s tool life equation: $$ V T^n = C $$ where \( V \) is the cutting speed (m/min), \( T \) is the tool life (minutes), \( n \) is the Taylor exponent (typically 0.1–0.3 for carbide cutters), and \( C \) is a constant. In practice, spherical cutters may exhibit higher \( C \) values due to their wear resistance, extending tool life in aggressive gear milling operations. Heat generation is another concern; excessive temperatures can anneal the workpiece or degrade the cutter. The heat flux \( Q \) during gear milling is given by: $$ Q = F_c \times v $$ where \( v \) is the cutting speed. Conical cutters, with their tapered design, often dissipate heat better, keeping \( Q \) lower than standard cutters at similar speeds. These formulas highlight the engineering rationale behind cutter selection, emphasizing that gear milling is not just about removing material but optimizing the entire machining ecosystem.
Common issues in gear milling cutter usage mirror those in construction milling, such as installation angles and material quality. For example, the helix angle of a gear milling cutter—typically 10–30 degrees—must be precise to ensure smooth chip evacuation and reduce vibration. If misaligned, it can cause chatter, leading to surface finish defects in gears. The formula for helix angle effect on cutting stability is: $$ \theta_h = \tan^{-1}\left(\frac{L}{\pi D}\right) $$ where \( \theta_h \) is the helix angle (degrees), \( L \) is the lead (mm), and \( D \) is the cutter diameter (mm). Another problem is cutter material quality; tungsten carbide tips must have high hardness (≥90 HRA) and toughness to withstand gear milling stresses. Poor-quality tips can fracture, increasing downtime and costs. Fixation methods also matter: cutters are often mounted via shrink-fit or hydraulic chucks, and improper fixation can cause runout, degrading gear accuracy. A runout error \( \delta_r \) can be calculated as: $$ \delta_r = \sqrt{(x_e – x_c)^2 + (y_e – y_c)^2} $$ where \( (x_e, y_e) \) are the actual cutter center coordinates and \( (x_c, y_c) \) are the ideal coordinates. Regular maintenance, such as sharpening and coating reapplication, mitigates these issues, ensuring consistent performance in gear milling tasks.
To contextualize these principles, consider application cases from my experience. In a project involving automotive transmission gears, made from medium-carbon steel (tensile strength 600 MPa), we used conical gear milling cutters. The goal was to achieve a production rate of 100 gears per hour with a pitch error under 0.06 mm. By setting a feed rate of 0.15 mm/tooth and a cutting speed of 200 m/min, we maintained tool life of 8 hours per cutter, balancing efficiency and cost. In contrast, for aerospace gear milling using maraging steel (tensile strength 1200 MPa), spherical cutters were employed. Despite a slower feed rate of 0.08 mm/tooth, they ensured precision within 0.02 mm and extended tool life to 12 hours, justifying their higher upfront cost. These cases demonstrate how tailored cutter selection in gear milling can meet diverse industrial demands, from high-volume manufacturing to precision-critical applications.
Economic analysis further refines cutter choice in gear milling. Total machining cost \( C_{total} \) includes cutter cost, labor, and downtime, expressed as: $$ C_{total} = N_c \times C_c + t_m \times R_l + t_d \times R_d $$ where \( N_c \) is the number of cutters used, \( C_c \) is the cutter unit cost, \( t_m \) is the machining time (hours), \( R_l \) is the labor rate ($/hour), \( t_d \) is the downtime for tool changes (hours), and \( R_d \) is the downtime cost rate ($/hour). For standard cutters in soft materials, \( N_c \) might be low due to fast wear, but \( t_m \) is reduced, lowering overall cost. In hard-material gear milling, spherical cutters reduce \( N_c \) and \( t_d \) but increase \( C_c \), requiring a break-even analysis. For instance, if a spherical cutter lasts three times longer than a conical one, its higher cost may be offset by reduced changeovers. Table 2 provides a simplified cost comparison for a sample gear milling job producing 1000 gears.
| Cutter Type | Unit Cost (USD) | Cutters Needed | Machining Time (hours) | Downtime (hours) | Total Cost (USD) |
|---|---|---|---|---|---|
| Standard | 75 | 10 | 50 | 5 | 4,250 |
| Conical | 225 | 4 | 60 | 3 | 3,900 |
| Spherical | 750 | 2 | 70 | 2 | 4,400 |
This table assumes labor and downtime rates of $50/hour and $100/hour, respectively. It shows that conical cutters offer the lowest total cost for this scenario, highlighting the importance of holistic evaluation in gear milling economics. Such analyses empower engineers to make data-driven decisions, optimizing both technical and financial outcomes.
Looking ahead, advancements in gear milling technology continue to evolve cutter designs. Coatings like titanium nitride (TiN) or diamond-like carbon (DLC) enhance wear resistance, allowing standard cutters to handle harder materials, blurring traditional boundaries. Moreover, adaptive machining systems use real-time sensors to adjust feed rates dynamically, improving efficiency across cutter types. The integration of AI in gear milling can predict tool failure, reducing unplanned downtime. These innovations underscore that gear milling is a dynamic field where cutter selection is just one part of a broader optimization strategy. As I reflect on my experiences, the key takeaway is that successful gear milling hinges on understanding the interplay between cutter properties, material behavior, and operational constraints.
In conclusion, gear milling cutter selection is a multifaceted decision influenced by material hardness, desired progress, precision requirements, and economic factors. Standard cutters excel in soft materials for fast, cost-effective gear milling, while conical cutters balance performance in medium-hard substrates. Spherical cutters, though expensive, are indispensable for ultra-hard materials where precision and tool life are paramount. By applying formulas for cutting forces, tool life, and costs, and by learning from practical cases, engineers can navigate these choices effectively. As gear milling advances, embracing new technologies will further refine this process, driving innovation in manufacturing. Ultimately, whether in foundation engineering or precision machining, the principles of adaptability and analysis remain universal, guiding us toward more efficient and reliable solutions.