
In my extensive experience with mechanical component failures, I have encountered numerous cases of gear shafts exhibiting abnormal cracking. These gear shafts, often used in heavy-duty applications, have presented significant challenges due to sudden failures after assembly, load testing, or even post-shipment. This analysis delves into the root causes of such cracking in large-sized gear shafts, based on a detailed investigation of multiple failed specimens. The primary focus is on understanding the interplay between material defects,热处理-induced stresses, and operational conditions that lead to catastrophic failures. Throughout this article, the term “gear shafts” will be emphasized to highlight the criticality of these components in industrial systems.
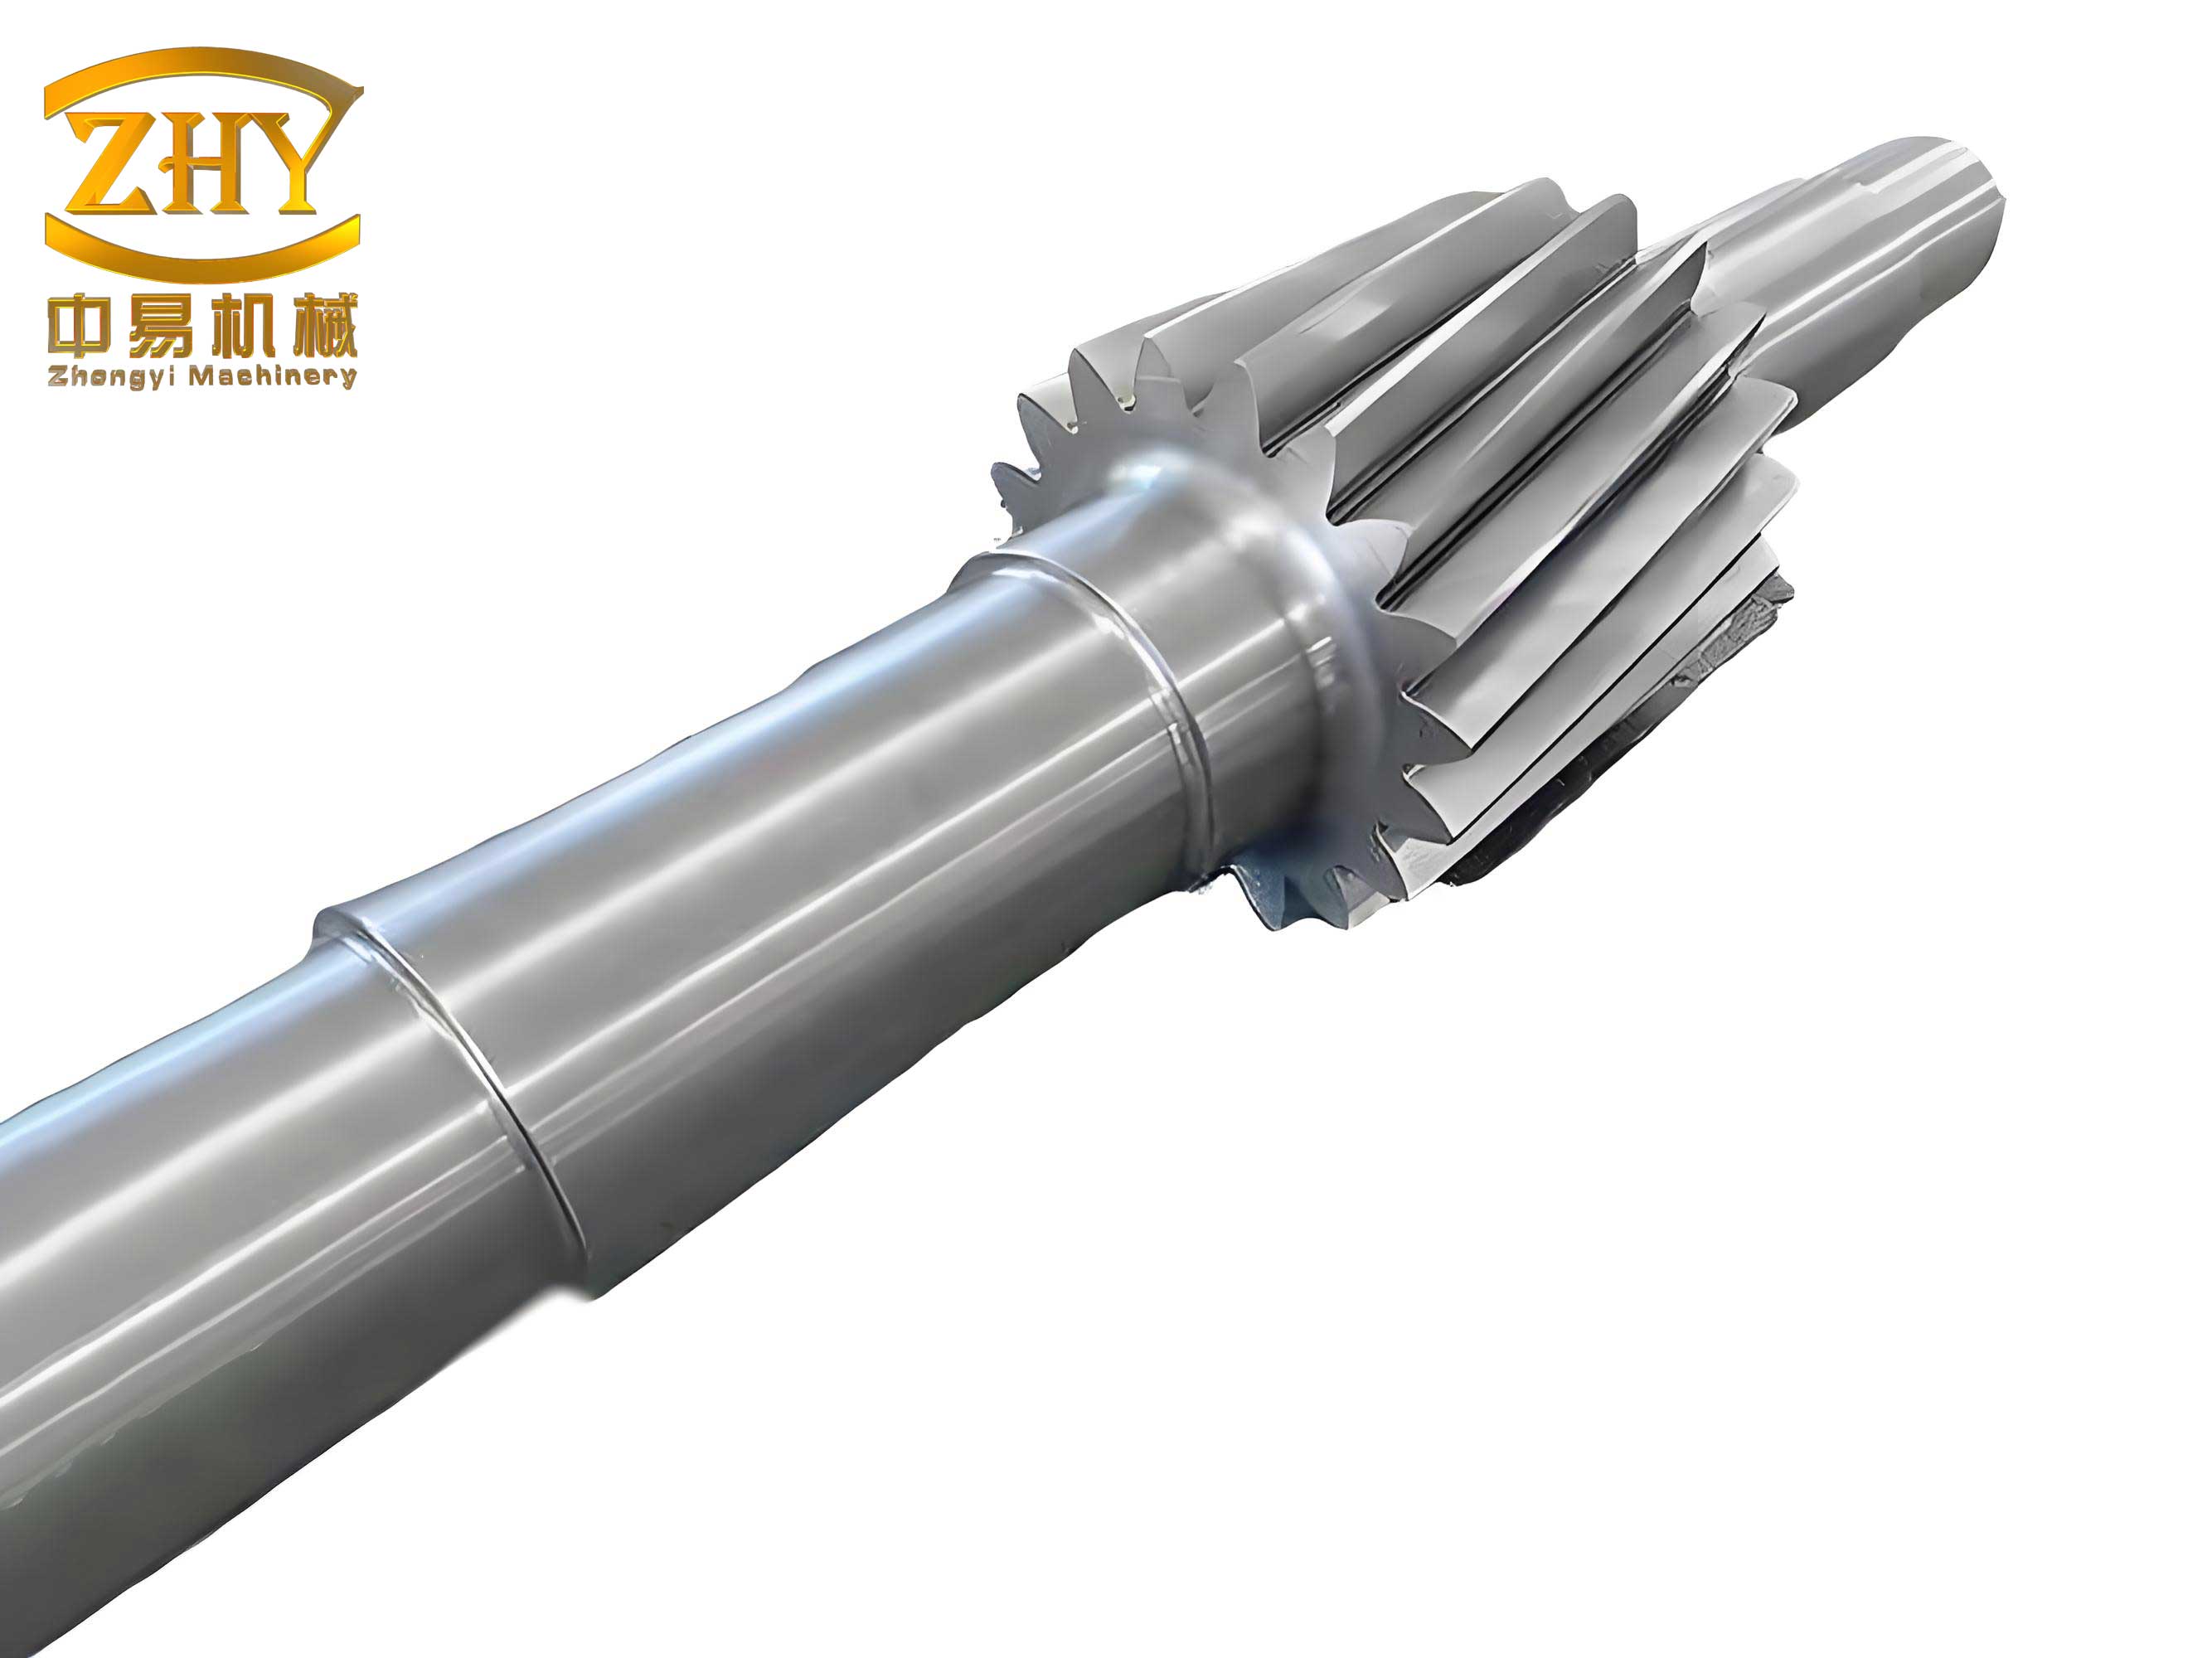
My investigation began with the systematic dissection of three cracked gear shafts that had undergone similar manufacturing processes. These gear shafts were fabricated from round bars with diameters ranging from 140 mm to 190 mm, machined through turning, grinding, and milling, followed by surface carburizing and quenching-tempering treatments. The carburizing was conducted at 940°C, quenching at 840°C, and tempering at 170°C. After non-destructive testing, the gear shafts were assembled for load testing, which involved stepwise power increases up to 1660 kW. Interestingly, all cracked gear shafts had passed these load tests, indicating that the failure mechanism was not due to immediate overload but rather a time-dependent process. This observation prompted a thorough analysis of the fracture surfaces, material chemistry, microstructure, hardness profiles, and residual stresses to pinpoint the exact causes of cracking in these gear shafts.
The methodology I employed encompassed a multi-faceted approach. First, I conducted chemical composition analysis using spectrometry to verify material conformity. Second, I performed macroscopic and microscopic fractography via scanning electron microscopy (SEM) to identify crack initiation sites and propagation modes. Third, I examined the metallographic structure at both low and high magnifications to assess grain size, segregation, and non-metallic inclusions. Fourth, I measured the hardness depth profile using micro-Vickers hardness testing to evaluate the carburized layer’s effectiveness. Fifth, I analyzed residual stresses using X-ray diffraction and estimated initial stresses based on crack opening displacements. Each of these steps was critical in building a comprehensive understanding of why these gear shafts failed.
Chemical Composition Analysis
The material of the gear shafts was specified as equivalent to 18CrNiMo7-6 steel, a low-alloy case-hardening grade. I sampled the base material from the failed gear shafts and analyzed its chemical composition. The results, compared against standard requirements, are summarized in Table 1. All elements, including carbon, silicon, manganese, chromium, nickel, and molybdenum, were within specified limits. Notably, the hydrogen content was below 2 ppm, which is generally considered low and not typically a direct cause of hydrogen embrittlement in such contexts. This confirmed that the material chemistry was not the primary culprit for the cracking observed in these gear shafts.
| Element | Tested Sample | 18CrNiMo7-6 Standard |
|---|---|---|
| C | 0.15 | 0.15–0.20 |
| Si | 0.23 | ≤0.40 |
| Mn | 0.53 | 0.50–0.90 |
| P | 0.007 | ≤0.020 |
| S | <0.005 | ≤0.025 |
| Cr | 1.69 | 1.50–1.80 |
| Ni | 1.52 | 1.40–1.70 |
| Mo | 0.26 | 0.25–0.35 |
| Al | 0.048 | 0.02–0.05 |
| Cu | 0.092 | ≤0.25 |
| Sn | 0.0052 | ≤0.030 |
| Sb | 0.0020 | ≤0.008 |
| H (ppm) | 0.7 | ≤2 |
Crack Morphology and Fractographic Features
Upon visual inspection, all cracked gear shafts exhibited longitudinal cracks that ran parallel to the axis, penetrating through the helical gears and spanning the entire length of the shafts. The cracks appeared straight and rigid, with significant opening at the surface, characteristic of quench-induced residual stress cracks. In cross-section, the cracks propagated radially inward from the surface, reaching the core of the gear shafts without branching. This morphology suggested a high tensile stress state driving the crack growth.
I opened the cracks to examine the fracture surfaces. The initiation sites were located subsurface, at depths ranging from a few millimeters to over ten millimeters below the surface, typically in the thicker diameter sections or near gear root regions. Table 2 details the crack source dimensions for the three gear shafts analyzed. The crack sources were associated with oversized non-metallic inclusions, primarily aluminum oxides, which acted as stress concentrators. As the depth of the crack source increased, the size of the inclusion also increased, indicating a correlation between stress state and critical flaw size.
| Sample ID | Crack Source Location | Depth from Surface (mm) | Inclusion Length (mm) | Inclusion Width (μm) |
|---|---|---|---|---|
| 1 | Helical Gear Section | 2.2 | 1.2 | 55 |
| 2 | Relief Groove Section | 12 | 3.0 | 250 |
| 3 | Relief Groove Section | 13 | 4.3 | 430 |
Under SEM, the fracture surfaces revealed distinct zones. The carburized surface layer exhibited primarily intergranular fracture, indicative of brittle failure due to high carbon content and residual stresses. In contrast, the non-carburized core regions showed transgranular quasi-cleavage fracture. Notably, the areas around the inclusion-initiated crack sources, even in the non-carburized zones, displayed intergranular features, suggesting a delayed cracking mechanism influenced by hydrogen or stress corrosion. No fatigue striations were observed, ruling out cyclic loading as a direct cause. The presence of these inclusions created localized stress intensification, which can be quantified using the stress intensity factor formula for an embedded flaw:
$$K_I = \sigma \sqrt{\pi a}$$
where \(K_I\) is the mode I stress intensity factor, \(\sigma\) is the applied tensile stress, and \(a\) is the effective crack length (inclusion size). When \(K_I\) exceeds the material’s fracture toughness, crack propagation ensues. For these gear shafts, the residual tensile stresses, combined with the inclusion size, likely resulted in \(K_I\) values sufficient to initiate cracks over time.
Microstructural and Macrostructural Examination
I conducted low-magnification examination of transverse sections, which revealed a relatively uniform macrostructure with only slight ingot-type segregation. No other macro-defects were detected. However, high-magnification metallography of longitudinal sections showed the presence of non-metallic inclusions classified as Type B (clustered alumina) and Type D (globular oxides) according to standard grading systems. While oversized inclusions were observed, none matched the extreme sizes found at the crack origins, highlighting the statistical nature of inclusion distribution and the challenge of detection.
The microstructure of the gear shafts consisted of a carburized surface layer with acicular martensite and a core of lath martensite. The prior austenite grain size in the core was measured as 8.0 on the ASTM scale, meeting the requirement of finer than grade 5. However, I observed severe banding in the microstructure, characterized by alternating ferrite and pearlite bands after an 860°C annealing treatment. This banding was rated as level 4 per GB/T13299-91, indicating significant microsegregation of alloying elements. The banding can degrade transverse mechanical properties and exacerbate residual stress inhomogeneity. The hardness variation due to banding can be described by a simple model:
$$H_{\text{band}} = H_{\text{base}} + \Delta H \sin\left(\frac{2\pi y}{\lambda}\right)$$
where \(H_{\text{band}}\) is the hardness at position \(y\), \(H_{\text{base}}\) is the average base hardness, \(\Delta H\) is the hardness amplitude, and \(\lambda\) is the wavelength of the banding. This inhomogeneity contributes to uneven stress distribution during quenching, increasing the risk of crack initiation in gear shafts.
Surface Hardness Depth Profile
To assess the effectiveness of carburizing, I performed micro-Vickers hardness tests from the tooth root surface inward. The hardness profile, plotted in Figure 8 (described narratively), showed that the effective case depth, defined as the depth where hardness exceeds 550 HV, was approximately 1.4 mm. The region with noticeably higher hardness than the core extended to about 2.5 mm. The core hardness averaged 430 HV0.5 but ranged from 350 to 450 HV0.5 due to microstructural banding. This variability in hardness can be modeled using an exponential decay function:
$$H(d) = H_c + (H_s – H_c) e^{-k d}$$
where \(H(d)\) is the hardness at depth \(d\), \(H_s\) is the surface hardness, \(H_c\) is the core hardness, and \(k\) is a constant related to carburizing diffusion. For these gear shafts, the gradient in hardness corresponds to a gradient in carbon content and transformation-induced volume changes, which directly influence residual stress generation. The high core hardness, coupled with banding, elevated the susceptibility to delayed fracture in these gear shafts.
| Depth from Surface (mm) | Hardness (HV0.5) | Region Classification |
|---|---|---|
| 0.0 | 750 | Carburized Surface |
| 0.5 | 700 | Carburized Layer |
| 1.0 | 650 | Carburized Layer |
| 1.4 | 550 | Effective Case Depth Limit |
| 2.0 | 500 | Transition Zone |
| 2.5 | 450 | Near-Core Transition |
| 5.0 | 430 | Core (Average) |
| 10.0 | 420 | Core |
Residual Stress Analysis
Using X-ray diffraction, I measured the circumferential residual stresses on transverse sections at various depths. After cracking, the stresses were tensile, ranging from 50 MPa to 120 MPa, with higher values near the core. However, this post-failure state does not reflect the initial condition. To estimate the original residual stresses, I measured the crack opening displacement and applied elastic strain theory. Assuming the crack opened due to the release of tensile stress, the initial circumferential residual stress \(\sigma_r\) can be approximated by:
$$\sigma_r = \frac{E \cdot \delta}{2 \pi r}$$
where \(E\) is Young’s modulus (approximately 210 GPa for steel), \(\delta\) is the crack opening displacement, and \(r\) is the radius of the gear shaft. My calculations yielded an initial residual tensile stress of about 500 MPa in the region of crack initiation. This high tensile stress arises from the differential volume expansion during martensitic transformation: the carburized surface layer expands more than the core, leading to compressive stresses at the surface and tensile stresses in the subsurface zone. The stress distribution can be modeled as:
$$\sigma(z) = \sigma_{\text{max}} \left(1 – \frac{z}{d_t}\right) \quad \text{for} \quad 0 \leq z \leq d_t$$
where \(\sigma(z)\) is the residual stress at depth \(z\), \(\sigma_{\text{max}}\) is the maximum tensile stress (around 500 MPa), and \(d_t\) is the depth of the tensile zone (approximately 2.5 mm). This stress field, when superimposed on applied loads, creates a critical environment for crack initiation at inclusions in gear shafts.
Discussion on Crack Formation Mechanisms
My analysis clearly indicates that the cracking in these gear shafts was a delayed failure driven by热处理-induced residual tensile stresses. The cracks initiated at oversized non-metallic inclusions located in the high tensile stress region beneath the carburized layer. The delay phenomenon is characteristic of stress corrosion cracking or hydrogen-assisted cracking, where time-dependent processes like hydrogen diffusion or corrosive agent penetration reduce the local fracture strength. The absence of fatigue features suggests that the load tests did not cause immediate cracking but may have accelerated the delayed failure by promoting hydrogen redistribution or increasing stress intensities.
The role of inclusions cannot be overstated. In gear shafts, non-metallic inclusions act as stress concentrators, reducing the effective load-bearing area and initiating microcracks under tensile stresses. The critical inclusion size for crack initiation depends on the local stress state and material toughness. From fracture mechanics, the threshold stress intensity factor \(K_{\text{th}}\) for delayed cracking can be expressed as:
$$K_{\text{th}} = \sigma_{\text{th}} \sqrt{\pi a_{\text{crit}}}$$
where \(\sigma_{\text{th}}\) is the threshold stress and \(a_{\text{crit}}\) is the critical inclusion size. For the gear shafts analyzed, \(a_{\text{crit}}\) decreased with depth as the tensile stress increased, explaining why smaller inclusions sufficed for cracking near the surface. Additionally, the severe microstructural banding exacerbated the problem by creating anisotropic mechanical properties and localized stress gradients. Banding reduces transverse ductility and fracture toughness, making gear shafts more prone to brittle fracture along the segregation bands.
The high core hardness (430 HV0.5) further increased susceptibility. Harder martensitic structures have lower fracture toughness and higher sensitivity to hydrogen embrittlement. Although hydrogen content was low, even trace amounts can accumulate at inclusions or high-stress regions, facilitating delayed crack growth. The combined effect of residual stress, inclusions, banding, and high hardness created a perfect storm for failure in these gear shafts.
Conclusions and Recommendations
Based on my detailed investigation, I conclude that the cracking of gear shafts was primarily due to delayed fracture initiated by oversized non-metallic inclusions in regions of high热处理-induced residual tensile stress. Contributing factors included severe microstructural banding, high core hardness, and inhomogeneous hardness distribution. These issues collectively reduced the fracture resistance and promoted crack propagation under static or quasi-static loading conditions.
To prevent future failures in gear shafts, I recommend a two-pronged approach. First, enhance raw material quality control by implementing ultrasonic non-destructive testing to detect oversized subsurface inclusions. Standard metallographic methods are insufficient for capturing maximum inclusion sizes; thus, statistical process control coupled with advanced NDT techniques is essential. Additionally, enforce strict limits on microstructural banding, aiming for levels below grade 2 per relevant standards. Second, optimize heat treatment parameters, specifically by increasing the tempering temperature to reduce residual stresses and lower the core hardness. A tempering temperature of 200–220°C, for instance, could alleviate tensile stresses while maintaining adequate strength. The relationship between tempering temperature \(T\) and residual stress reduction can be approximated by:
$$\sigma_r(T) = \sigma_{r0} e^{-k_T (T – T_0)}$$
where \(\sigma_{r0}\) is the initial residual stress at tempering temperature \(T_0\), and \(k_T\) is a material constant. Higher tempering also improves toughness, reducing delayed fracture susceptibility. Furthermore, consider modifying carburizing cycles to achieve a smoother hardness gradient, which can mitigate stress concentrations. Implementing these measures will significantly enhance the reliability and longevity of gear shafts in service.
In summary, the failure analysis of these gear shafts underscores the importance of holistic material and process control. By addressing inclusion size, microstructure homogeneity, and residual stress management, manufacturers can produce more durable gear shafts capable of withstanding operational demands. Continuous monitoring and advanced testing protocols are key to ensuring the integrity of such critical components in industrial machinery.