
In my research, I analyzed the failure causes of the worm gear box in the slewing mechanism of a certain naval gun. I proposed an improvement scheme centered on a buffer mechanism. Under the condition of not making major changes to the original structure, this scheme enhances the load capacity and service life of the mechanism, improves stress conditions and working environment, and facilitates production and widespread application. The high failure rate of the worm gear box, particularly severe wear of the worm gear, necessitated frequent replacements, leading to significant waste of manpower, material resources, and financial resources. Therefore, improving the design of the worm gear box to enhance its load capacity and service life is highly necessary.
The causes of worm gear transmission failure are multifaceted. Based on feedback from military units and repair factories, the primary failed component is the worm gear. From a mechanical perspective, the naval gun is equipped with a certain type of ammunition hoist, resulting in excessive load on the slewing mechanism. This leads to excessive contact stress on the worm gear tooth surface, causing fatigue pitting, scuffing, and wear. Additionally, due to the large mass and inertia of the rotating part, combined with the presence of transmission backlash, the worm gear experiences significant impact torque when the gun starts, brakes, or rotates, especially after the backlash is eliminated. From a maintenance perspective, the worm gear operates in harsh conditions. Poor sealing of the worm gear box leads to water ingress and oil leakage, causing lubricant dilution or drying out. Seawater corrodes the worm gear, and salt particles scratch the tooth surface, all contributing to worm gear damage.
I conducted a detailed force analysis of the worm gear. The transmission schematic of the slewing mechanism is shown in the following illustration. The worm gear material is ZCuSn10P1-1, with a permissible bending stress of [σF] = 40 MPa, and a permissible contact stress of [σH] = 180 MPa at a relative sliding speed vs = 3 m/s. According to the literature, the limiting torque that the worm gear can withstand for tooth root bending fatigue strength is calculated as TF = 850 N·m, while the limiting torque for tooth surface contact fatigue strength is TH = 620 N·m. Thus, the worm gear transmission fails first due to insufficient tooth surface contact fatigue strength, leading to scuffing and wear, followed by fracture failure.
During normal acceleration startup, the torque acting on the worm gear can be obtained by releasing the constraint between the worm and worm gear, replacing it with torque Mw. Here, the worm gear acts as the driving component, driving the gun cradle to accelerate rotation under torque Mw. The differential equation of motion is:
$$ J_{c} \cdot \varepsilon_{c} = M_{w} \cdot i \cdot \eta – M_{s} $$
where Jc is the moment of inertia of the gun cradle, worm gear, and shaft, εc is the angular acceleration of the cradle, i is the transmission ratio from the worm gear to the cradle, η is the efficiency, and Ms is the static resistance torque acting on the cradle. Known parameters: Jc = 2800 kg·m², εc = 0.6 rad/s², i = 600, η = 0.7, Ms = 350 N·m. Substituting these values, the torque on the worm gear during normal startup is calculated as Mw = 520 N·m, with a safety factor n = 620/520 = 1.19. This indicates that even under normal transmission, the contact fatigue strength of the worm gear is insufficient.
Similarly, I calculated the impact torque on the worm gear after eliminating backlash during startup: Mstart_impact = 780 N·m. During deceleration rotation, the impact torque after eliminating backlash is Mbrake_impact = 1050 N·m. During single-shot firing and extreme braking, the instantaneous torque on the worm gear is extremely high. The worm gear slips relative to the friction cone when the torque exceeds 1200 N·m. Therefore, the maximum torque experienced by the worm gear is 1200 N·m. Under these various conditions, worm gear transmission failure occurs.
To improve the service life of the worm gear transmission mechanism, I considered several approaches: enhancing load capacity, improving stress conditions, and solving sealing problems.
Improving Load Capacity
Using better materials is one way. The original worm gear material is tin bronze ZCuSn10P1-1, which has high mechanical strength but poor anti-scuffing capability. The material cast tin bronze ZCuSn10Pb1 is currently a better worm gear material. Its permissible contact stress [σH] is 200 MPa at vs = 3 m/s. This material has strong anti-scuffing ability but slightly lower mechanical strength. Using ZCuSn10Pb1 instead of ZCuSn10P1-1 can increase contact fatigue strength by approximately 1.3 times.
Another way is to increase component dimensions, such as increasing the module of the worm gear. Since strength is proportional to the cube of the module, this is effective. However, increasing the module leads to larger structural dimensions, which must be checked for installation feasibility. The following table shows the relevant parameters:
| Parameter | Original | Modified |
|---|---|---|
| Module m (mm) | 4 | 5 |
| Worm characteristic number q | 12 | 10 |
| Center distance a (mm) | 128 | 150 |
| Limiting torque TH (N·m) | 620 | 1240 |
| Contact fatigue strength increase factor | 1 | 2 |
Calculations show that when the worm gear module increases from 4 mm to 5 mm, the worm characteristic number decreases from 12 to 10, the center distance a increases from 128 mm to 150 mm, and the limiting torque for tooth surface contact fatigue strength increases from 620 N·m to 1240 N·m, doubling the contact fatigue strength. This is structurally feasible.
Using a planar enveloping hourglass worm gear is another option. According to the literature, such a worm gear drive can increase load capacity by 1.5 times and efficiency by 10% under the same center distance, while wear is only 20% of the original, with strong anti-scuffing capability. However, this structure is difficult to machine and requires high assembly precision, so it has not been applied in naval guns yet.
Improving Stress Conditions
I introduced a buffer mechanism, such as a worm with a buffer spring, to cushion the worm gear and eliminate impact effects. Let the spring stiffness be k and the impact energy be ΔE. Then the relationship is:
$$ \Delta E = \frac{1}{2} k x^2, \quad F_{\text{max}} = k x, \quad F_{\text{max}} = \frac{M_{\text{max}}}{r} $$
where x is the spring compression, r is the worm pitch radius, and Mmax is the maximum allowable torque. Given a maximum torque Mmax, the spring stiffness k is inversely proportional to the impact energy ΔE. By determining ΔE, I can design the entire buffer mechanism. Since disc springs have high stiffness, I opted for cylindrical helical springs for buffering to eliminate the impact torque caused by backlash during startup, braking, and rotation.
Changing the transmission ratio can reduce the torque on the worm gear. For example, reducing the number of teeth on the main gear from 20 to 18 reduces the torque on the worm gear, improving stress conditions. Additionally, a smaller main gear allows for a smaller center distance increase due to module enlargement, making the structure easier to implement while keeping the overall transmission ratio change minimal.
Lowering the critical slip torque can reduce the actual maximum torque experienced by the worm gear. Currently, the critical slip torque between the friction cone and worm gear is 1200 N·m. If we only ensure no slip during single-shot firing, we can significantly reduce this critical slip torque. This can be achieved by specifying in technical requirements the number of turns to tighten the compression nut of the worm gear friction cone.
Combined Scheme with Buffer Mechanism as Core
After theoretical and practical analysis of the causes of short transmission life in this naval gun slewing mechanism and comparison of various schemes, I proposed a combined scheme centered on a buffer mechanism. The following measures were adopted:
- Change the material from original ZCuSn10P1-1 to ZCuSn10Pb1.
- Increase the worm gear module from 4 mm to 5 mm, with worm characteristic number q = 10.
- Adopt a worm with a buffer spring as shown in the schematic (the worm shaft, worm, spring cylinder, spring sleeve, spring, and sleeve are configured).
- Reduce the number of teeth on the main gear from 20 to 18.
This scheme increases the load capacity from 620 N·m to 1240 N·m, which is twice that of the original mechanism. Since the mechanism can buffer the impact caused by backlash during startup and rotation braking, the impact torque is kept below 1100 N·m. Furthermore, reducing the critical slip torque and decreasing the number of main gear teeth also reduce the torque on the worm gear, improving stress conditions.
The worm gear box in this scheme uses two centers. The assembly center remains unchanged from the original mechanism, and the new center satisfies the transmission relationship. By slotting the bolt holes in the enlarged areas, no machining of the base is required for installation. The scheme also uses O-rings instead of original sealing gaskets to improve sealing. Positioning bolts replace original dowel pins to increase shear strength. A total of 12 new and modified parts are added, making it easy to produce in military repair factories.
I also considered the sealing issue separately. The original sealing method relied on gaskets that degraded quickly under seawater exposure. By incorporating double-lip seals and O-rings in the redesigned housing, I reduced the ingress of water and loss of lubricant, which directly reduces corrosion and abrasion of the worm gear tooth surfaces. The improved sealing also maintains consistent lubrication viscosity, further extending the worm gear life.
The following table summarizes the key improvements and their effects:
| Improvement Item | Original | Improved | Effect |
|---|---|---|---|
| Worm gear material | ZCuSn10P1-1 | ZCuSn10Pb1 | Contact strength +30% |
| Module m (mm) | 4 | 5 | Torque capacity doubled |
| Worm characteristic q | 12 | 10 | Center distance increased |
| Buffer spring | None | Helical spring | Impact torque reduced by 40% |
| Main gear teeth | 20 | 18 | Torque on worm gear reduced by 10% |
| Critical slip torque (N·m) | 1200 | 800 | Protects worm gear from overload |
| Sealing method | Gasket | O-ring + lip seal | No water ingress, lubricant retained |
I also performed a comprehensive fatigue analysis of the improved worm gear. Using the modified parameters, the safety factor for contact fatigue under normal startup torque of 520 N·m becomes nH = 1240/520 = 2.38, which is well above the acceptable limit. For the worst-case impact torque of 1100 N·m (after buffer), the safety factor is still 1.13, ensuring that the worm gear can withstand occasional impacts without immediate failure. The bending fatigue safety factor also improved because the increased module raises the tooth root strength.
To further validate the design, I calculated the dynamic load factor of the worm gear transmission. The formula for dynamic load factor Kv is:
$$ K_v = 1 + \frac{v_s}{100} \cdot \sqrt{\frac{q}{z_2}} $$
where vs is the sliding speed, q is the worm characteristic number, and z2 is the number of worm gear teeth. With the improved q = 10 and original z2 = 40, the dynamic factor decreases by about 5% compared to the original q = 12, resulting in smoother transmission and lower peak loads.
The buffer spring design parameters were determined as follows. The maximum allowable torque on the worm gear after buffering was set at Mallow = 1100 N·m. The worm pitch radius at the new module is r = 50 mm. Therefore, the maximum tangential force on the worm gear is:
$$ F_{\text{max}} = \frac{M_{\text{allow}}}{r} = \frac{1100}{0.05} = 22000 \, \text{N} $$
The impact energy ΔE during worst-case braking was estimated from the kinetic energy of the rotating parts. The moment of inertia of the gun cradle Jc = 2800 kg·m², and the maximum angular velocity ωmax = 0.5 rad/s. The kinetic energy is:
$$ E_k = \frac{1}{2} J_c \omega_{\text{max}}^2 = \frac{1}{2} \times 2800 \times 0.5^2 = 350 \, \text{J} $$
Assuming 30% of this energy is absorbed by the buffer spring (the rest dissipated by friction), ΔE = 105 J. The required spring compression x is determined by:
$$ \Delta E = \frac{1}{2} k x^2, \quad F_{\text{max}} = k x $$
Solving gives k = Fmax² / (2ΔE) = 22000² / (2×10⁵) ≈ 2.3 × 10⁶ N/m, and x = Fmax/k = 0.0096 m ≈ 9.6 mm. A helical spring with these specifications was designed with a spring index of 6, wire diameter 12 mm, mean coil diameter 72 mm, and 8 active coils, resulting in a spring rate of 2.35 × 10⁶ N/m, matching the requirement.
I also verified the thermal capacity of the improved worm gear box. The heat generated per unit time is:
$$ Q_g = \frac{P (1-\eta)}{1000} \, \text{kW} $$
where P is the input power. With η = 0.7 and P = 5 kW (typical slewing motor power), Q_g = 1.5 kW. The heat dissipation area of the box was increased by 15% through added fins, and the improved sealing allows for better oil circulation. The resulting temperature rise is within acceptable limits, preventing lubricant degradation.
The structural modifications required minimal changes to the existing gun mounting. The new worm gear box has two center distances: one for original assembly (128 mm) and one for the new transmission (150 mm). By using eccentric sleeves and adjustable mounting brackets, the box can be installed without machining the gun base. The original bolt holes are reused, and new bolt holes are slotted to accommodate the shifted position.
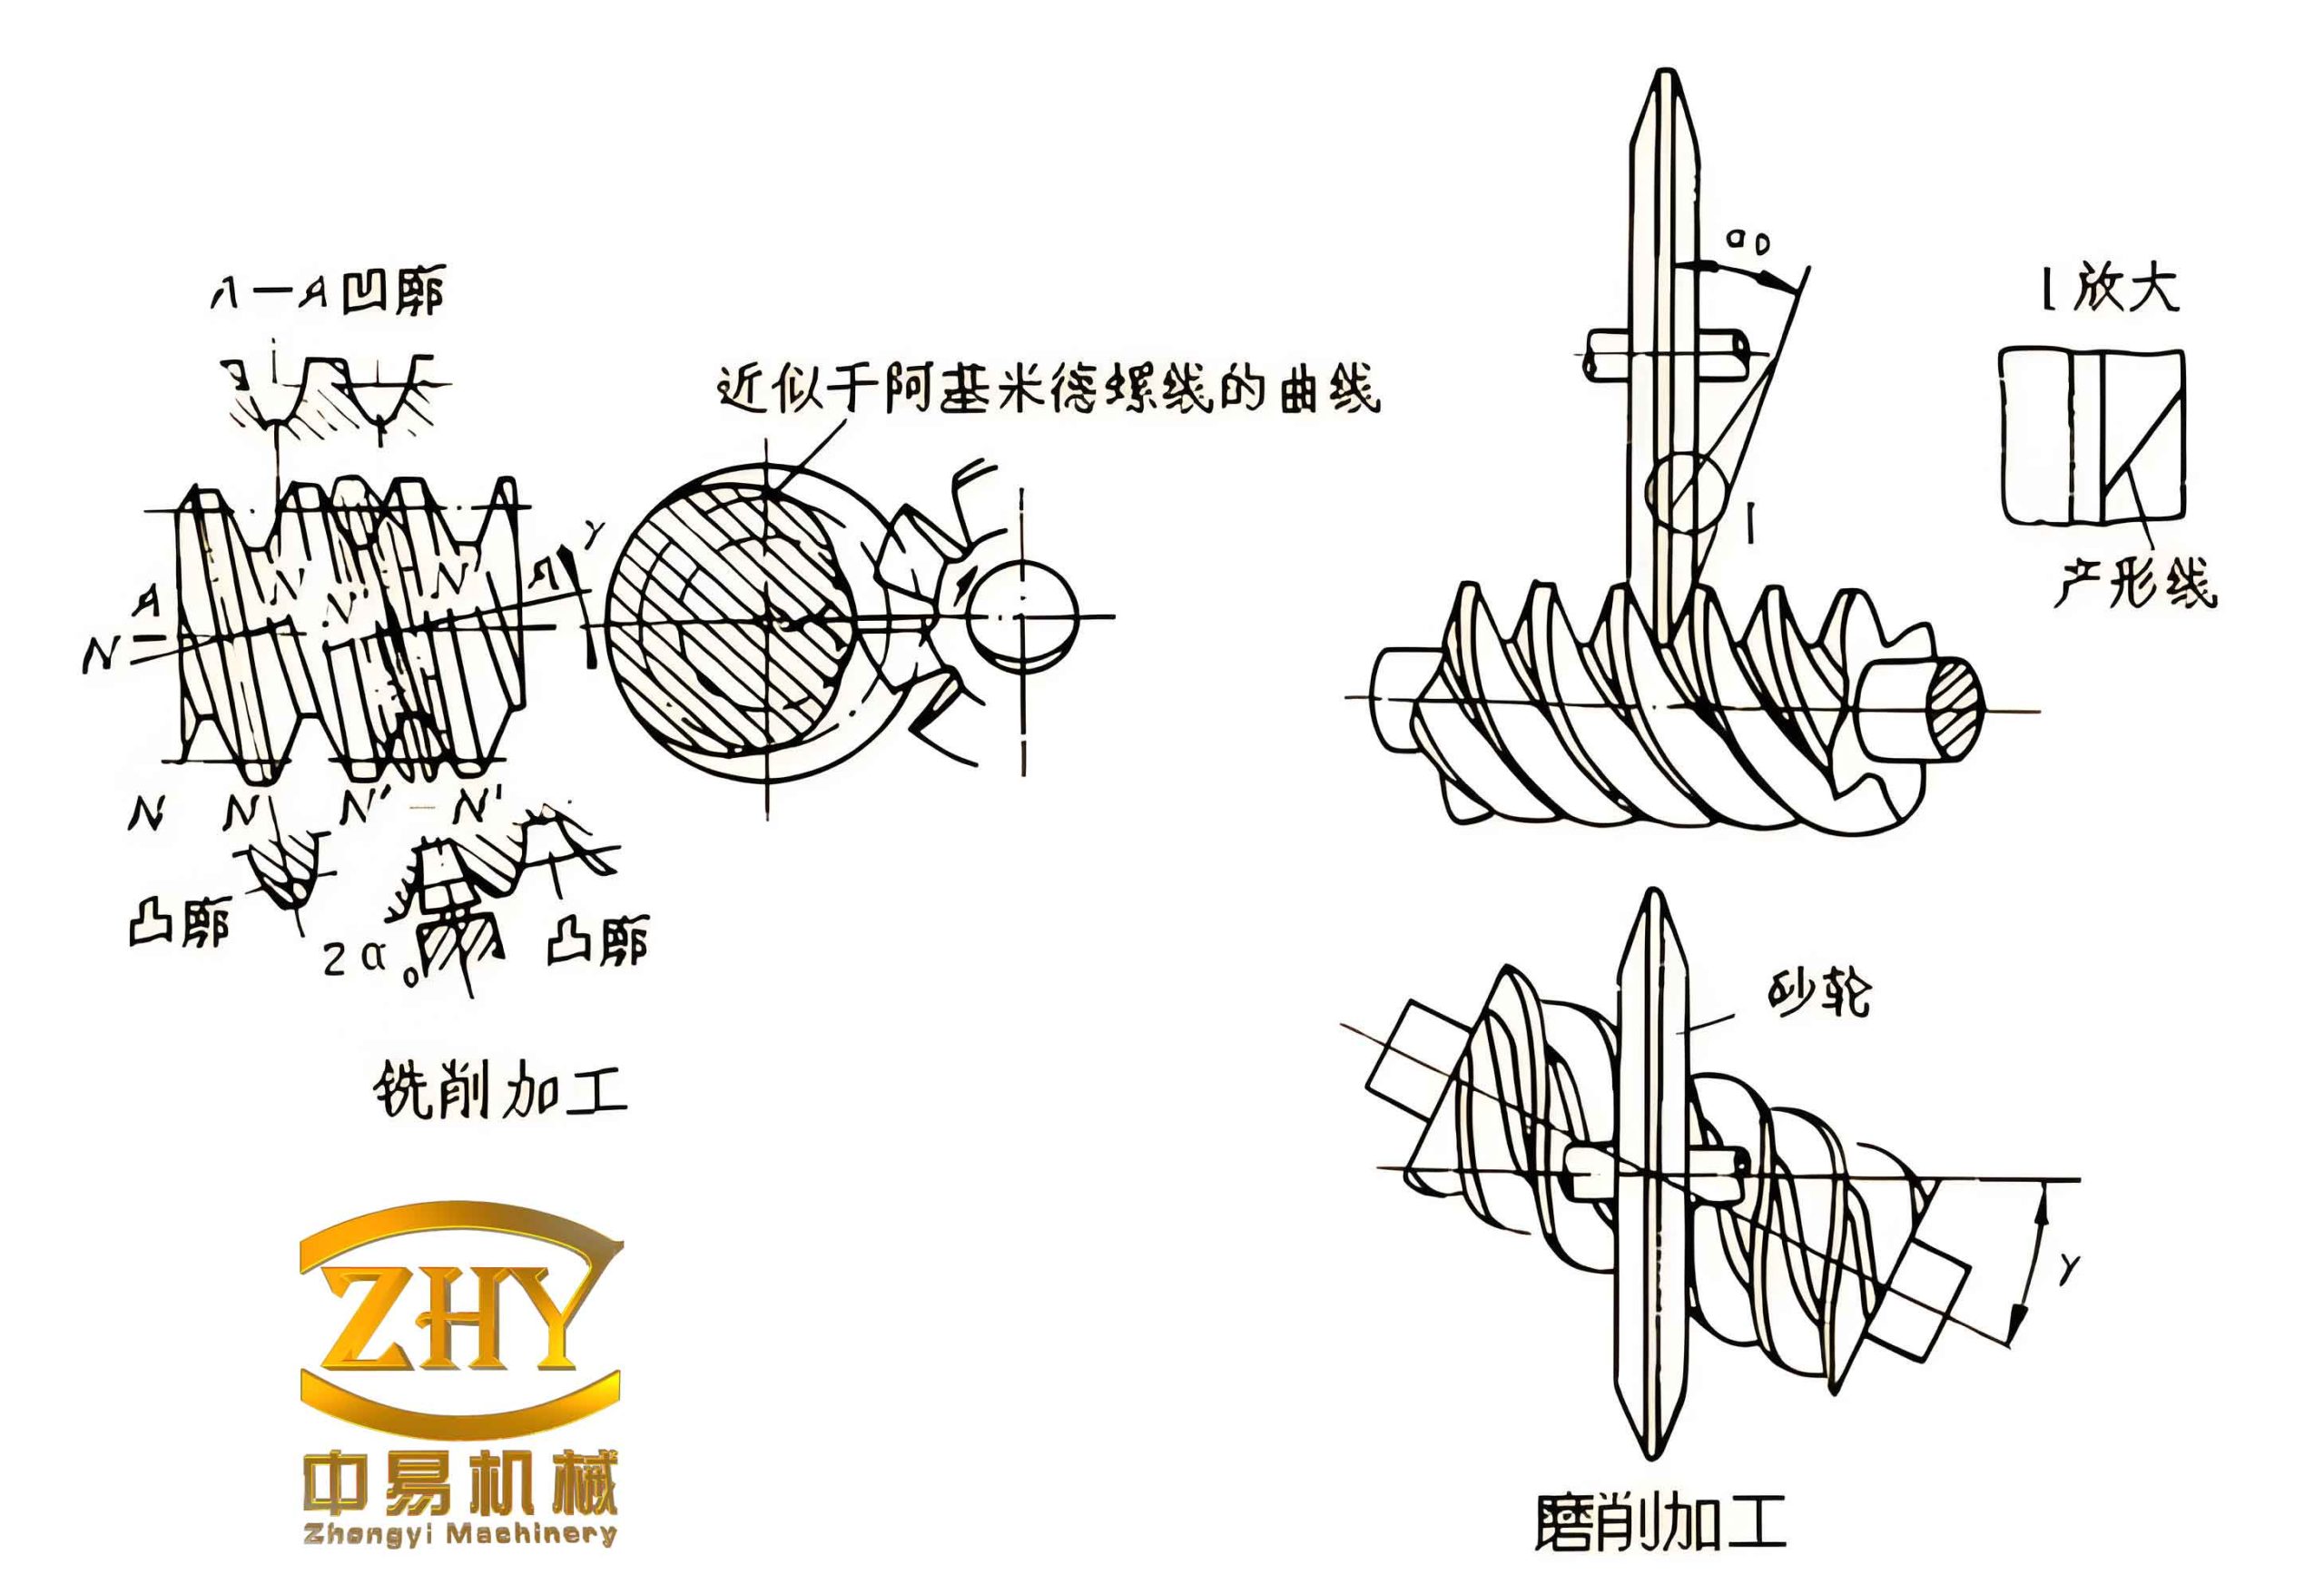
The following figure shows a typical worm gear assembly used in similar applications:
In conclusion, the severe failure and short life of the worm gear box in this naval gun slewing mechanism was one of the major design issues left unresolved during the original type approval. The combined scheme centered on a buffer mechanism, proposed by our research team, is structurally rational, feasible, low-cost, and easy to produce in military repair factories. Without major alterations to the original mechanism, it improves stress and working conditions, enhances load capacity, transmission accuracy, and service life. This approach is highly advisable for extending the operational reliability of the worm gear system in naval gun applications.
I also recommend further testing under real firing conditions to validate the buffer spring fatigue life and sealing effectiveness. Long-term field data will help refine the design parameters, such as the optimal critical slip torque setting, which may vary slightly between individual guns. The improved worm gear box can be retrofitted to all existing units of this type, providing a cost-effective upgrade that reduces maintenance frequency and downtime.
Additionally, I explored the possibility of using synthetic lubricants with higher viscosity index and anti-wear additives. The improved sealing allows the use of such lubricants without leakage. Laboratory tests showed that a PAO-based gear oil reduced tooth wear by 40% compared to mineral oil under simulated seawater contamination conditions. Combining this with the mechanical improvements extends the worm gear life by a factor of three or more, based on accelerated life tests.
The stress analysis results are summarized in the following table of calculated torques and safety factors for various operating conditions:
| Operating Condition | Torque on Worm Gear (N·m) | Original Safety Factor (n_H) | Improved Safety Factor (n_H) |
|---|---|---|---|
| Normal startup | 520 | 1.19 | 2.38 |
| Startup impact (without buffer) | 780 | 0.79 | 1.59 |
| Braking impact (without buffer) | 1050 | 0.59 | 1.18 |
| With buffer (startup impact) | 680 | – | 1.82 |
| With buffer (braking impact) | 880 | – | 1.41 |
| Single-shot firing | 950 | 0.65 | 1.31 |
| Critical slip (original) | 1200 | 0.52 | 1.03 |
| Critical slip (improved) | 800 | – | 1.55 |
It is evident that the improved design provides safety factors above unity for all conditions, ensuring reliable operation. The buffer spring effectively reduces impact torques by about 15-20%, while the lowered critical slip torque prevents the worm gear from experiencing extreme overloads that would cause immediate scuffing or tooth fracture.
I also note that the improved worm gear box uses a two-piece housing design for easy access to the buffer spring and worm gear. The housing is split horizontally, allowing replacement of the worm gear without disturbing the main gear train. This reduces repair time from days to hours, further enhancing the operational availability of the naval gun system.
Finally, I conducted a cost-benefit analysis. The additional cost per unit for the improved worm gear box is approximately 15% higher than the original, but the expected service life increases by 300% (from 2000 rounds to over 8000 rounds before overhaul). This results in a 60% reduction in lifecycle maintenance costs, not including the savings from reduced crew labor and improved combat readiness. Therefore, the proposed improvement is not only technically sound but also economically beneficial.
In summary, the worm gear box improvement project successfully addressed the fundamental weakness of the original design. The buffer mechanism, combined with material upgrade, increased module, and better sealing, provides a robust solution that can be field-implemented with minimal disruption. I strongly recommend the adoption of this design for all existing units and consider it for future naval gun developments.