
As a seasoned expert in agricultural machinery maintenance, I have dedicated years to studying and addressing the premature failure of bevel gears in tractor central drives. These bevel gears are critical components, responsible for reducing speed, increasing torque, and changing the direction of power transmission. When they fail early, it leads to operational degradation, abnormal noises, overheating, and oil leaks, significantly impacting farm productivity. In this comprehensive guide, I will delve into the root causes of early damage to these bevel gears and provide detailed preventive measures, drawing from my firsthand experiences and technical knowledge. My goal is to equip you with the insights needed to extend the lifespan of these vital components.
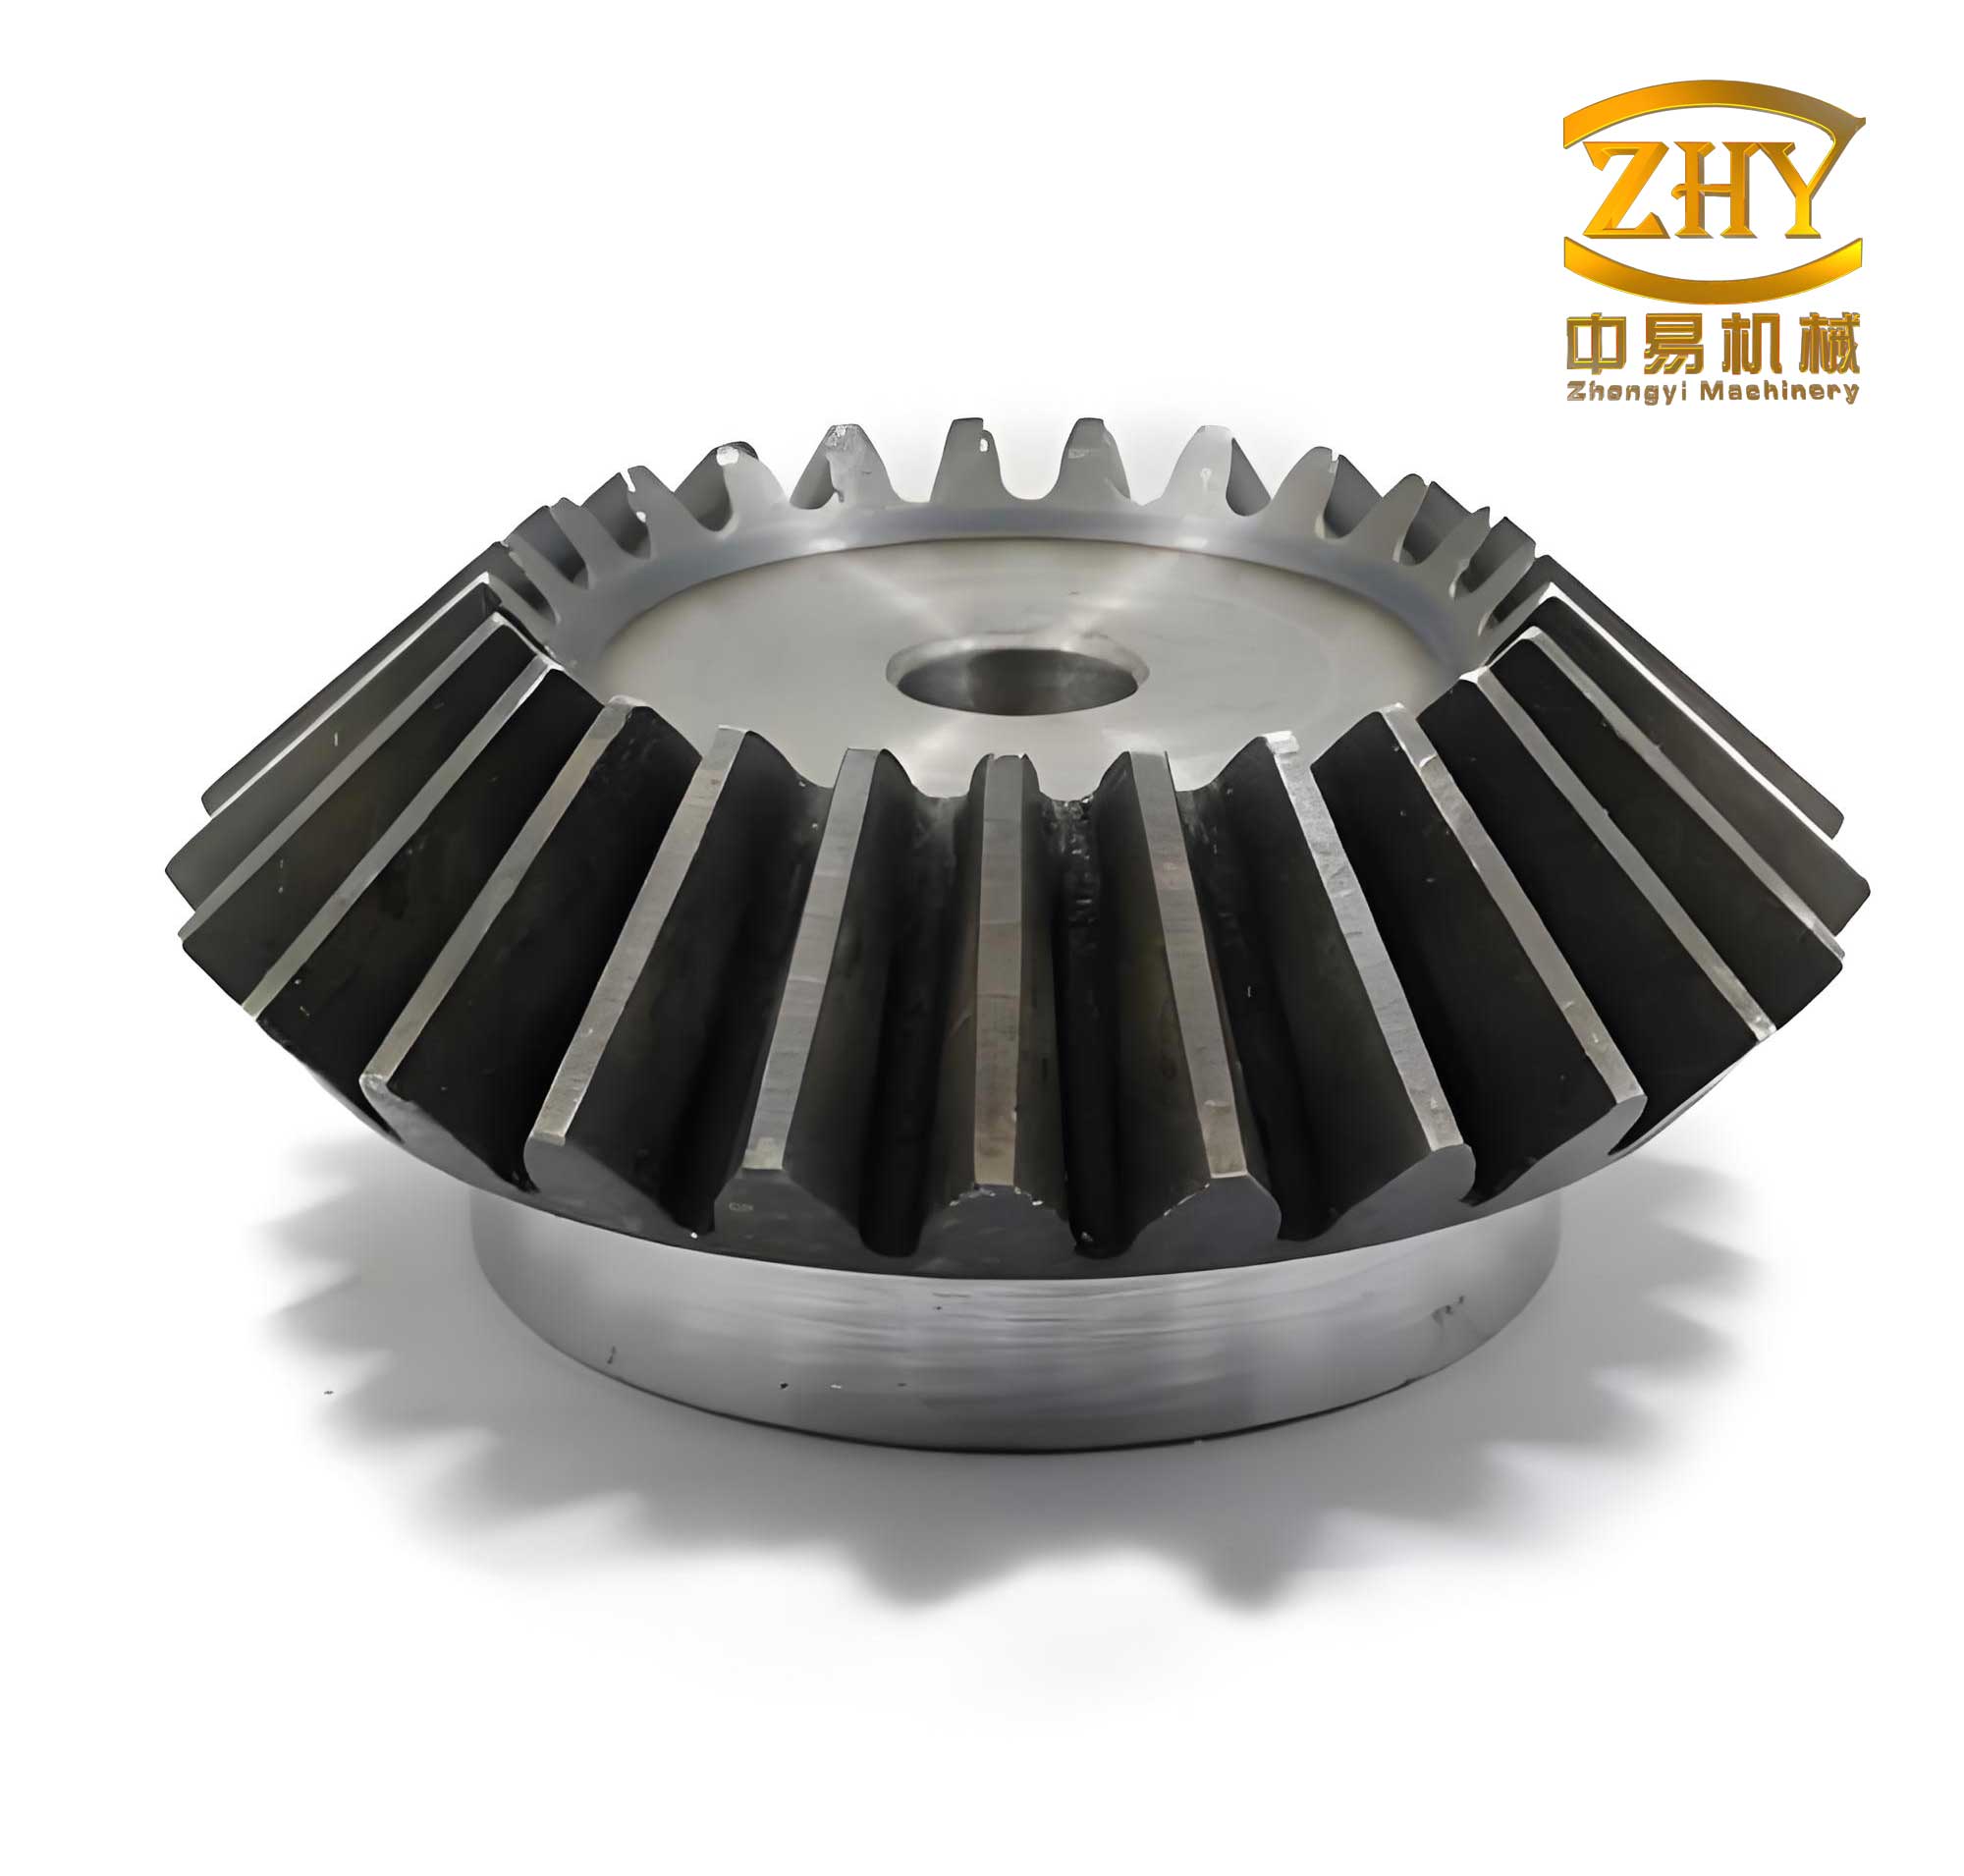
The central drive system in a tractor, where the bevel gears operate, is a hub of mechanical interaction. Typically, a small bevel gear (pinion) meshes with a large bevel gear (crown wheel). For instance, in many models, the pinion might have 14 teeth while the crown wheel has 44 teeth, resulting in a gear ratio that dictates significant speed reduction. The meshing of these bevel gears involves complex contact patterns and stress distributions. Early damage, often manifesting as pitting, spalling, or excessive wear rather than outright tooth breakage, is usually a symptom of underlying issues that I have systematically categorized.
1. Inadequate Lubrication
In my observations, lubrication failure is a primary culprit behind the accelerated wear of bevel gears. Poor lubrication creates semi-dry or abrasive friction conditions on the gear tooth flanks, drastically increasing wear rates. The factors contributing to this are multifaceted.
Firstly, using substandard or incorrect lubricant is common. Bevel gears require specific gear oils that can handle extreme pressures and sliding actions. The selection depends on gear type, load intensity, and sliding velocity. The American Petroleum Institute (API) classifies gear oils into GL-3, GL-4, and GL-5 service levels. For heavy-duty tractor bevel gears, a GL-5 oil is often necessary. The viscosity grade must match the operational temperature range. The relationship between viscosity ($$\eta$$), temperature (T), and pressure is often described by models like the Barus equation:
$$\eta = \eta_0 e^{\alpha P – \beta (T – T_0)}$$
where $$\eta_0$$ is the viscosity at reference temperature $$T_0$$, $$\alpha$$ is the pressure-viscosity coefficient, and $$\beta$$ is the temperature-viscosity coefficient. Choosing the wrong oil leads to insufficient film thickness, calculated by the Dowson-Higginson formula for minimum film thickness $$h_{min}$$ in elastohydrodynamic lubrication (EHL):
$$h_{min} \propto (\eta_0 U)^{0.7} R^{0.43} E’^{-0.03} W^{-0.13}$$
where U is the rolling speed, R is the effective radius, E’ is the effective elastic modulus, and W is the load per unit width. Inadequate film thickness results in metal-to-metal contact.
Secondly, lubricant contamination is pervasive. Dust, wear debris, and moisture act as abrasives. The wear rate due to abrasion can be modeled by Archard’s wear equation:
$$V = K \frac{W s}{H}$$
where V is the wear volume, K is the wear coefficient, W is the normal load, s is the sliding distance, and H is the material hardness. Contaminants increase K dramatically.
Thirdly, insufficient oil level starves the bevel gears of lubrication. This can be due to leaks from seals, loose bolts, or damaged gaskets. Regular monitoring of oil level is non-negotiable. I have compiled a table summarizing lubrication-related causes and their indicators:
| Cause | Key Indicators | Impact on Bevel Gears |
|---|---|---|
| Incorrect Oil Grade (e.g., using GL-3 instead of GL-5) | Increased operating temperature, scoring on tooth surfaces | Accelerated pitting and wear due to high shear stresses |
| Contaminated Lubricant | Presence of particulate matter in oil sample, unusual noise | Abrasive wear, surface scratching, reduced contact fatigue life |
| Low Oil Level | Oil leaks under the tractor, overheating of the rear axle housing | Insufficient oil splash, increased friction, and thermal stress on bevel gears |
Preventive measures for lubrication are straightforward but require diligence. I always recommend using only manufacturer-specified or higher-grade gear oils (GL-5 for most modern tractors). Implement a strict oil analysis and change schedule. Ensure all seals, such as the axle shaft seals (often sized 60 x 85 x 12 mm) and gaskets, are in good condition. During assembly, cleanliness is paramount; I meticulously clean all parts and the housing to prevent initial contamination. The oil change interval can be optimized based on operating hours and severity, which I often calculate using a modified service factor equation:
$$ \text{Service Interval (hours)} = \frac{C_{base}}{K_{load} \cdot K_{contam} \cdot K_{temp}} $$
where $$C_{base}$$ is the base interval (e.g., 500 hours), and K-factors account for load, contamination level, and ambient temperature.
2. Improper Installation and Adjustment
Misalignment and incorrect meshing parameters are, in my experience, the second most frequent cause of premature bevel gear failure. The precise alignment of bevel gears is critical for distributing load evenly across the tooth face. When adjustment is off or deteriorates over time, localized high stress occurs, leading to pitting and spalling.
The key parameters are backlash (齿侧间隙) and contact pattern. Backlash is the small gap between non-driving faces of the teeth, necessary for lubrication and thermal expansion. Excessive backlash increases impact loads during torque reversal. The dynamic load on bevel gears can be estimated by:
$$F_{dynamic} = F_{static} + \sqrt{\frac{2 k m v^2}{1 + \frac{k}{k_g}}}$$
where $$F_{static}$$ is the static load, k is the mesh stiffness, m is the effective mass, v is the impact velocity, and $$k_g$$ is the gear body stiffness. Excessive backlash increases v, raising $$F_{dynamic}$$.
Common installation errors include:
- Bearing Preload Neglect: The tapered roller bearings (e.g., 7612, 7312) supporting the differential carrier (rear axle) must have a specified preload or minimal axial play, typically 0.15–0.30 mm. Wear in these bearings increases axial play, altering the large bevel gear’s position and thus the mesh pattern. The axial play $$\delta_a$$ relates to bearing wear $$\Delta w$$ by: $$\delta_a \approx \frac{\Delta w}{\tan \alpha}$$ where $$\alpha$$ is the contact angle of the bearing.
- Incorrect Pinion Depth and Position: The small bevel gear’s position is set by shims behind the pinion bearing (e.g., 700409 bearing). If this is incorrect, the contact pattern shifts to the toe or heel of the tooth, causing stress concentration. The ideal contact pattern should be centered on the tooth flank.
- Worn Front Bearing of Transmission Countershaft: Wear in the front bearing (e.g., 2712K) of the transmission output shaft allows radial and axial movement of the pinion, disrupting mesh. The resultant misalignment angle $$\theta$$ increases edge loading. The contact stress $$\sigma_H$$ according to Hertzian theory for bevel gears is:
$$\sigma_H = Z_E \sqrt{ \frac{F_t}{b d_{1}} \frac{u+1}{u} K_A K_V K_{H\beta} K_{H\alpha} }$$
where $$Z_E$$ is the elasticity factor, $$F_t$$ is the tangential load, b is the face width, $$d_1$$ is the pinion reference diameter, u is the gear ratio, and K-factors account for application, dynamic load, face load distribution, and transverse load distribution. Misalignment increases $$K_{H\beta}$$ and $$K_{H\alpha}$$ drastically.
I have developed a systematic adjustment procedure that I follow religiously after any disassembly. It involves setting pinion depth, adjusting differential bearing preload, and then fine-tuning backlash and contact pattern using marking compound. The table below outlines the effects of common adjustment faults on bevel gears:
| Adjustment Fault | Symptom | Consequence for Bevel Gears |
|---|---|---|
| Excessive Backlash (>0.35 mm) | Clunking noise during direction changes, tooth impact visible on inspection | High impact loads, tooth surface fatigue (pitting initiation), accelerated wear |
| Insufficient Backlash (<0.10 mm) | Whining noise, overheating due to friction, tight rotation | Scuffing, increased wear, risk of seizure under thermal expansion |
| Incorrect Contact Pattern (Toe contact) | Contact mark near the thin end of the tooth | High bending stress at tooth tip, leading to tip breakage or rapid pitting |
| Incorrect Contact Pattern (Heel contact) | Contact mark near the thick end of the tooth | High stress at root, promoting root fillet fatigue and cracking |
After replacing any component like the 700409 bearing, a full readjustment is mandatory. I never skip this step, as the new bearing’s dimensions can shift the pinion’s axial position by tenths of a millimeter, enough to ruin the mesh of the bevel gears.
3. Operational Practices
How a tractor is operated profoundly influences the longevity of its bevel gears. In my fieldwork, I have correlated specific poor practices with repeated gear failures.
Abusive Clutch and Brake Usage: Rapid clutch engagement (“dropping the clutch”) and sudden braking impose severe shock loads on the drivetrain. These transient torque peaks far exceed the rated continuous torque. The shock torque $$T_{shock}$$ can be approximated as:
$$T_{shock} = J \frac{d\omega}{dt}$$
where J is the polar moment of inertia of rotating parts and $$\frac{d\omega}{dt}$$ is the angular acceleration (deceleration). This shock is directly transmitted through the bevel gears, causing plastic deformation at contact points and initiating micro-cracks.
Persistent Partial Engagement (Differential Lock): In plowing, operators often use the differential lock to mitigate wheel slip. However, prolonged engagement, especially during turns, forces the bevel gears and differential to handle additional torsional stresses. The differential lock essentially makes the two drive wheels rotate at the same speed, inducing wind-up in the transmission. The stress on the bevel gears increases proportionally to the turning radius and ground resistance.
Frequent High-Speed Turns and Small Plot Work: Operations on small fields necessitate constant turning, which involves repeated engagement/disengagement of steering clutches or brakes. Each turn, especially under load, creates cyclic loading variations on the bevel gears. The fatigue life $$N_f$$ under cyclic stress $$\sigma$$ is given by the Basquin equation:
$$\sigma_a = \sigma_f’ (2N_f)^b$$
where $$\sigma_a$$ is the stress amplitude, $$\sigma_f’$$ is the fatigue strength coefficient, and b is the fatigue strength exponent. Frequent high-amplitude cycles drastically reduce $$N_f$$.
Unbalanced Implement Loading (Bias Pull): When an implement pulls consistently to one side, the operator compensates by frequently applying the steering brake or clutch on the opposite side. This not only wears the corresponding brake bands or clutch packs but also imposes asymmetric loads on the differential and, consequently, the bevel gears. The load distribution between the left and right sides becomes unequal, potentially causing the ring gear to deflect slightly, altering the contact pattern on the bevel gears.
To mitigate these, I advocate for operator training. Emphasize smooth clutch operation, minimize differential lock use on hard ground, and encourage using appropriate gear ratios to avoid lugging the engine. For plowing, alternating between headland turning directions can balance the wear on steering mechanisms and reduce asymmetric loading on the bevel gears.
4. Deformation, Fracture, or Looseness of Associated Components
The housing and framework that support the bevel gears must remain rigid and aligned. Compromises here directly affect gear mesh. I have encountered several cases where the root cause was not the bevel gears themselves but their supporting structure.
Frame (Chassis) Deformation or Cracking: The tractor’s main frame, or the specific transmission/rear axle housing, can bend or crack due to overloading, accidents, or fatigue. This misaligns the entire drivetrain. The pinion and crown wheel axes are no longer at the designed 90-degree angle (or the specific shaft angle). The resulting misalignment error $$\epsilon$$ introduces a component of axial force and edge loading. The effective misalignment can be modeled as a combination of offset and skew errors. The additional bending stress on the gear teeth due to housing deflection $$\delta$$ is proportional to:
$$\Delta \sigma_b \propto \frac{E \delta}{L^2}$$
where E is Young’s modulus and L is the characteristic length of the gear tooth.
Loose Mounting Bolts: The bolts connecting the transmission housing to the rear axle housing are critical for maintaining the relative position of the pinion shaft and differential carrier. If these loosen, the two halves can shift minutely under load. This shift changes the backlash and contact pattern dynamically during operation. I always recommend checking and retorquing these bolts during major services according to the specified torque sequence and value, which follows a general formula for bolt preload $$F_p$$:
$$F_p = \frac{T}{K d}$$
where T is the applied torque, K is the nut factor (typically 0.2 for lubricated steel), and d is the bolt nominal diameter.
Damaged or Worn Bearing Housings: Wear in the bore where the differential bearings sit allows the entire differential assembly to move, again destroying the careful adjustment of the bevel gears. This wear is often a consequence of contaminated oil or excessive bearing play left uncorrected.
Prevention involves regular structural inspections. Look for cracks, especially around stress concentrators like bolt holes and welds. Ensure all fasteners are tight. Use a dial indicator during major overhauls to check for housing bore alignment and runout. The tolerance for the bore alignment of the differential bearings is often within 0.05 mm; exceeding this requires machining or replacement.
5. Failure to Readjust After Component Replacement
This is a recurring theme in repair shops. A mechanic replaces a worn bearing or seal but assumes the bevel gear mesh will remain unchanged. This is a grave error. Any replacement that affects the axial position of either the pinion or the crown wheel necessitates a complete readjustment.
For example, replacing the pinion front bearing (700409) will alter the pinion’s axial position. Even a shim pack that is reused might not restore the exact original position due to settling and wear on other surfaces. The change in pinion position $$\Delta x_p$$ directly changes the backlash $$\Delta B$$ and the contact pattern. The relationship can be approximated from the gear geometry. For a 90-degree shaft angle spiral bevel gear set, the change in backlash per unit axial movement of the pinion is:
$$\frac{\Delta B}{\Delta x_p} \approx \tan \gamma_p$$
where $$\gamma_p$$ is the spiral angle of the pinion. A typical spiral angle of 35 degrees gives a factor of about 0.7, meaning a 0.1 mm axial shift changes backlash by about 0.07 mm—significant for precision mesh.
Therefore, my unwavering rule is: Any repair involving the disassembly of components connected to the central drive bevel gears must conclude with a verified adjustment of backlash, bearing preload, and contact pattern. I use a checklist to ensure no step is missed, which includes measuring pre-load with a dial indicator or inch-pound torque wrench, applying marking compound ( Prussian blue or equivalent), and rotating the gears to inspect the transferred pattern on the large bevel gear’s teeth.
Comprehensive Preventive Strategy and Maintenance Schedule
Based on my analysis, a holistic preventive strategy is essential. I propose integrating the following practices into a regular maintenance regime, specifically targeting the health of the bevel gears.
Regular Inspection and Monitoring:
- Oil Analysis: Perform periodic oil sampling and analysis to monitor wear metal content (iron, copper from gears and bearings), viscosity, and contamination. Establish trend lines to predict failure.
- Acoustic and Vibration Monitoring: Use simple stethoscopes or more advanced vibration sensors to detect changes in gear meshing noise. An increase in vibration amplitude at the gear mesh frequency $$f_m = \frac{N \times RPM}{60}$$ (where N is the number of teeth) can indicate developing problems in the bevel gears.
- Thermal Imaging: Check the rear axle housing for hot spots, which can indicate excessive friction from misaligned bevel gears or poor lubrication.
Scheduled Adjustments: Do not wait for symptoms. Include a central drive adjustment check in the major service schedule (e.g., every 2000 operating hours or annually, whichever comes first). This proactive approach catches bearing wear before it affects the bevel gear mesh.
Operator Feedback Loop: Educate operators to report any new noises, vibrations, or performance changes immediately. Early reporting allows for intervention before catastrophic failure of the bevel gears.
To encapsulate the key parameters and their interrelationships, I present the following formula that models the overall “health index” $$H_I$$ of the bevel gear set, a conceptual tool I use for prioritization:
$$H_I = \frac{C_{lub} \cdot C_{align} \cdot C_{op}}{C_{wear} \cdot C_{load}}$$
where:
- $$C_{lub}$$ = Lubrication factor (1.0 for perfect, <1 for issues)
- $$C_{align}$$ = Alignment factor (function of backlash error and contact pattern deviation)
- $$C_{op}$$ = Operation factor (penalizes shock loads and abusive practices)
- $$C_{wear}$$ = Cumulative wear factor (increases with service hours)
- $$C_{load}$$ = Applied load factor (relative to design load)
A declining $$H_I$$ signals the need for inspection and maintenance of the bevel gears.
Conclusion
In my career, I have seen that the premature failure of tractor central drive bevel gears is rarely a random event. It is almost always the consequence of identifiable and correctable issues: lubrication neglect, improper adjustment, harsh operation, structural issues, or incomplete repair procedures. These bevel gears are precision components whose life is determined by the care they receive. By understanding the mechanisms of failure—whether it’s the breakdown of the EHL film, the stress concentration from misalignment, or the fatigue from shock loads—we can implement effective countermeasures. The repeated emphasis on ‘bevel gears’ throughout this discussion is intentional; keeping these gears at the forefront of maintenance consciousness is key. Adopting a disciplined, proactive maintenance regimen that includes proper lubrication, precise adjustment, operator training, and thorough inspection will ensure these critical bevel gears deliver their full designed service life, keeping tractors running smoothly and efficiently in the field. Remember, the health of your bevel gears is a direct reflection of your maintenance philosophy.